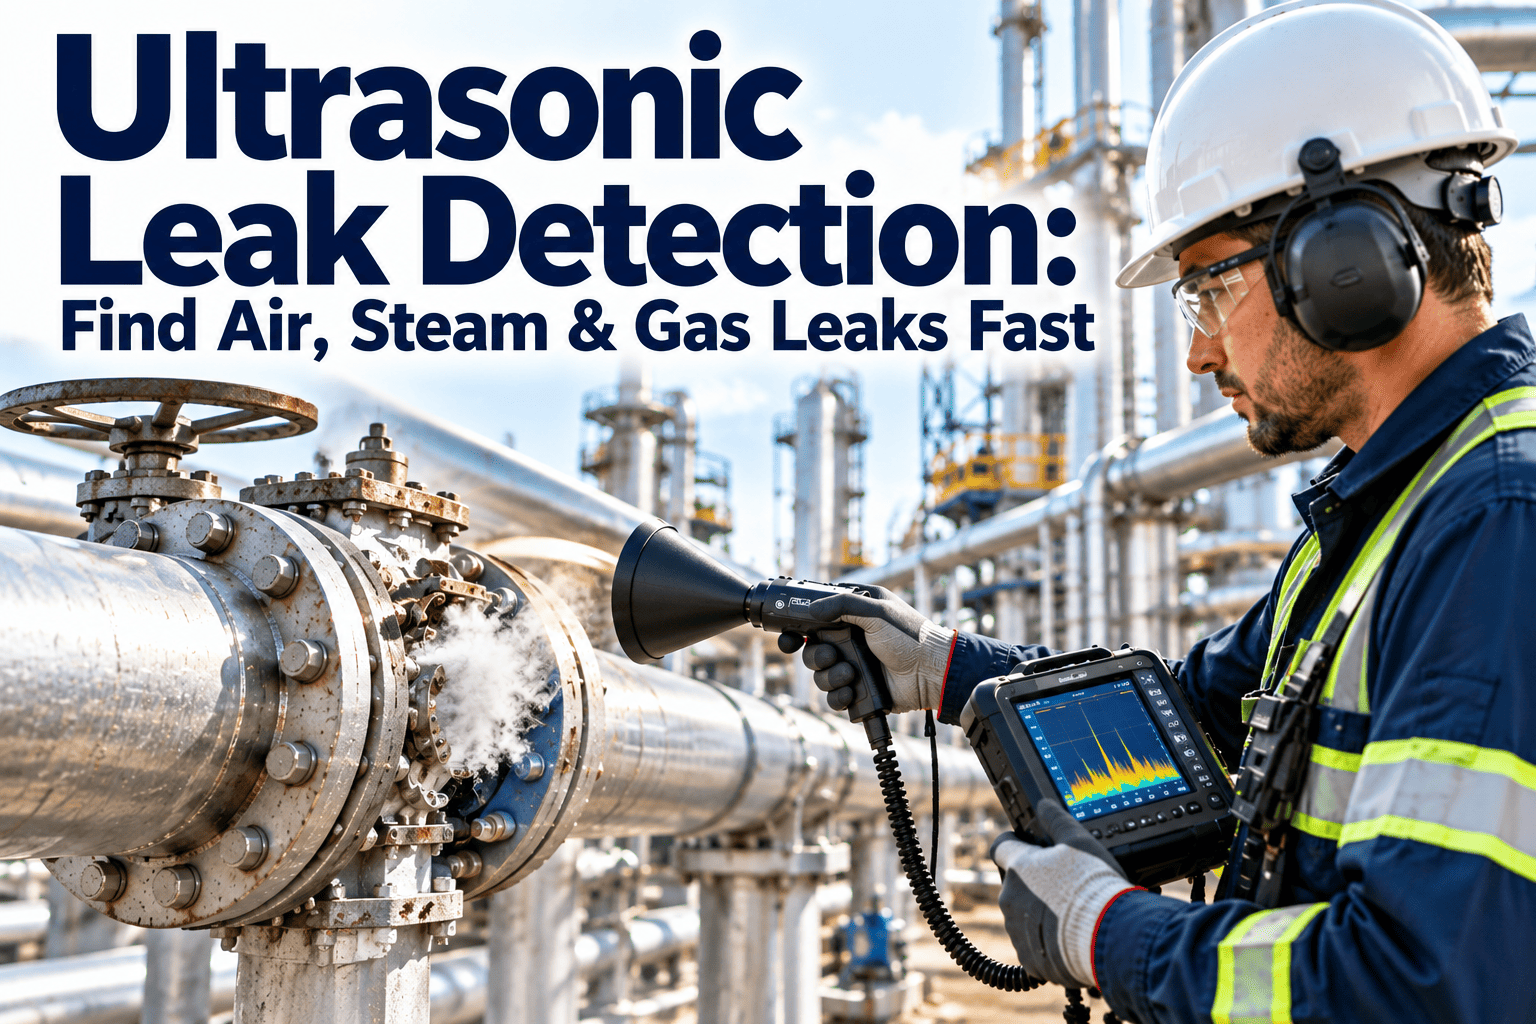
A hissing steam trap on the third floor, a cracked solenoid fitting behind a rooftop AHU, a slow gas leak in a boiler room manifold — none of these announce themselves over the noise of a working facility. They just cost money, degrade equipment, and occasionally turn into safety incidents, all while sitting in plain sight of a walkthrough inspection that can't hear them. Ultrasonic leak detection closes that gap by picking up the high-frequency turbulence every pressurized leak produces, long before it's loud enough for a human ear or large enough to fail an asset. Facilities that build a structured ultrasonic survey program routinely recover energy costs that a purely visual PM routine never catches, and the last section of this guide covers how Start Free Trial turns those findings into tracked, closed-loop work orders.
The leaks your facility can't hear are the ones draining your utility budget
Compressed air, steam, and gas leaks escape as ultrasonic turbulence 20,000 Hz and above — well outside human hearing range. Ultrasonic detectors translate that turbulence into an audible, locatable signal, letting facility teams find and log leaks a walkthrough would miss entirely.
What an unmanaged leak survey program is actually costing you
These figures are national averages, and the gap between a well-run facility and a neglected one is almost entirely a function of survey discipline rather than equipment age. A plant with a ten-year-old compressor and a disciplined quarterly ultrasonic route routinely beats a plant with a brand-new compressor and no leak program at all, because leaks accumulate continuously regardless of how new the source equipment is.
How ultrasonic detection finds what a walkthrough can't
Every pressurized leak — air, steam, or gas — creates turbulent flow as it crosses from high pressure to atmosphere. That turbulence generates a broadband ultrasonic signature, typically strongest between 25 kHz and 40 kHz, regardless of the ambient plant noise a technician hears at ground level.
Pressurized system — compressed air line, steam trap, valve, gas fitting
Turbulent flow generates ultrasonic frequencies from roughly 20 kHz to 100 kHz
Ultrasonic sensor heterodynes the signal down into an audible, directional tone
Technician tags location, logs dB intensity, and files a corrective work order
Because ultrasonic sensors are directional and largely unaffected by background noise, the same handheld unit works in a loud mechanical room, a quiet server hall, or an open rooftop — three environments where visual and soap-bubble testing behave very differently. Most detectors let the operator narrow the focus cone as they get closer to a suspected source, which is what allows a technician to pinpoint one leaking fitting out of a dozen identical ones on a manifold rather than just confirming that a leak exists somewhere in the vicinity.
Compressed air, steam, and gas leaks behave differently — your survey should too
| Leak type | Common failure points | Ultrasonic signature | Primary risk if missed |
|---|---|---|---|
| Compressed air | Quick disconnects, FRLs, threaded fittings, worn hose ends, the last 30 feet of drop legs at equipment | Steady hiss, consistent amplitude | Wasted compressor energy, pressure drop at point of use |
| Steam | Failed steam traps, packing glands, flanged joints, insulation breaches | Sharp broadband signature, often intermittent with cycling traps | Water hammer, burns, condensate loss, boiler efficiency drop |
| Refrigerant / process gas | Schrader valves, brazed joints, service ports, solenoid seats | Higher-pitched, lower-amplitude signal, needs closer scan distance | Compliance exposure, system capacity loss, EPA reporting obligations |
| Natural gas / combustion | Union fittings, regulator vents, appliance connectors, meter sets | Variable amplitude depending on line pressure | Fire and explosion risk, requires immediate isolation, not just a work order |
Compressed air and gas leaks are the most consistent, easiest signature to scan for, since the pressure differential rarely changes over the course of a shift. Steam leaks are noisier to interpret because many steam traps cycle open and closed as part of normal operation, so a technician has to distinguish a trap that's venting correctly from one that's failed open and continuously blowing live steam — a distinction usually made by combining the ultrasonic reading with a surface temperature check at the trap outlet.
Building a repeatable ultrasonic leak survey routine
Map the pressurized systems and set the survey route
Build an asset list of every compressed air header, steam distribution branch, and gas line in the facility, then sequence a walking route that a technician can complete in a single shift without backtracking.
Scan and grade each find by intensity
Log the dB reading and estimated leak rate for every location. A quiet 60 dB fitting leak can wait for a scheduled shutdown; an 85+ dB leak on a critical air header gets flagged for same-week repair.
Tag, photograph, and route to a work order
A leak found without a tracked repair path just gets rediscovered next quarter. Every logged leak should generate a corrective work order with a location tag, photo, and priority so it doesn't disappear into a spreadsheet.
Verify repairs and re-baseline
Re-scan repaired locations on the following survey cycle to confirm the fix held, and track total leak count and estimated CFM loss over time as a facility-level trend, not a one-time audit result.
What one quarter of surveys typically finds
A 140,000-square-foot manufacturing facility running two 200 HP compressors starts its first structured ultrasonic survey after years of visual-only inspection. The initial quarterly pass turns up 38 active air leaks, ranging from a barely audible 58 dB fitting to a 91 dB coupling failure on a critical header. Using DOE's standard leak-cost estimate, the technician logs the total loss at roughly 62 CFM, worth an estimated $54,000 a year in wasted compressor output at the facility's electricity rate. Half of that loss traces to just six leaks above 80 dB, which get same-week repair priority. By the third quarterly survey, the leak count drops to 14 and estimated annual loss falls below $19,000, with the remaining leaks scheduled around a planned shutdown rather than chased individually.
The pattern holds across most facilities that start a program from zero: a small number of high-amplitude leaks account for most of the dollar loss, and finding them first produces the fastest payback, even before the full survey route is complete.
Matching the detector to the facility, and training the team that carries it
Handheld ultrasonic detectors range from basic single-frequency units to multi-sensor devices that pair ultrasonic detection with infrared imaging for leak confirmation. The right tier depends on facility size, the mix of air/steam/gas systems, and how often the survey runs. Buying more sensor than the facility needs mostly wastes budget; buying less than the facility needs shows up later as leaks a technician swore weren't there, because a low-end unit simply couldn't pick up a faint signal at survey walking speed.
Single-sensor handheld units
- Best for small facilities with primarily compressed air systems
- Manual dB readout, no data logging
- Requires a trained operator to interpret readings consistently
Data-logging ultrasonic scanners
- Stores GPS or asset-tagged location with each reading
- Estimates CFM loss and annualized cost per leak
- Suited to multi-building campuses running quarterly surveys
Combined ultrasonic and thermal imaging units
- Confirms gas and steam leaks visually alongside the acoustic signal
- Reduces false positives in high-ambient-noise mechanical rooms
- Justified for facilities with combustion gas lines or critical steam distribution
Training matters as much as the hardware. A technician who has never calibrated a detector against a known reference leak will under-report low-amplitude finds, which is exactly the population of leaks that compounds into the biggest annual loss. Most detector manufacturers and ultrasound trade associations offer a one- to two-day certification course covering calibration, ambient noise discrimination, and dB-to-CFM estimation, and facilities running their own survey program in-house should budget for at least one certified operator per shift rather than treating the skill as something anyone can pick up from the manual.
Where facility leak survey programs lose their savings
A leak survey program rarely fails because the detector was wrong. It fails because the process around the detector — scheduling, tracking, and prioritization — quietly breaks down after the first enthusiastic quarter, and the leak count creeps back toward where it started.
Running the survey once and stopping
- A single audit catches the leaks that exist that day, not the ones that develop next quarter
- Vibration and thermal cycling reopen repaired joints over time
- Recurring surveys are what turn a one-time savings number into a sustained budget line
Logging finds without routing repairs
- A leak documented in a report but never assigned to a technician gets rediscovered next survey
- Without a closed-loop work order, repair status is invisible to facility leadership
- Verification scans after repair are the only way to confirm a fix actually held
Treating every leak as equal priority
- A 58 dB leak on a non-critical branch line can wait for a scheduled shutdown
- An 85+ dB leak on a critical header or a suspected gas leak needs same-day response
- Grading by intensity keeps the repair backlog focused on the leaks actually driving cost
Turn every ultrasonic find into a tracked, closed work order
See how OxMaint logs leak surveys, tags locations against your asset hierarchy, and routes repairs automatically — book a walkthrough with your own facility data.
Running the leak survey program inside a CMMS instead of a spreadsheet
Ultrasonic surveys generate a lot of small, easily lost data points — a dB reading, a photo, a location tag — that only add up to savings if every find gets tracked to repair. OxMaint gives facility teams a structured way to run that loop.
Mobile leak logging
Technicians log leak location, intensity, and photo evidence from a phone during the survey walk, tagged directly to the asset or system in the register.
Automated corrective work orders
Every logged leak above your intensity threshold generates a work order automatically, with priority set by dB reading and system criticality.
Recurring survey scheduling
Set the ultrasonic survey as a recurring inspection by building, zone, or system so quarterly or monthly cadences never get skipped.
Leak trend reporting
Dashboards track leak count, estimated CFM loss, and repair closure time over successive surveys, giving facility leadership a defensible energy-savings number.
Ultrasonic leak detection: frequently asked questions
How often should a facility run an ultrasonic leak survey?
Most facilities with significant compressed air or steam systems run a full survey quarterly, with critical production or data hall air headers checked monthly, and a broader annual survey covering every branch line and drop leg on the property. Facilities can schedule recurring survey work orders in OxMaint so the cadence doesn't depend on someone remembering.
Can ultrasonic detectors find both leaks and mechanical faults?
Yes. The same handheld units used for leak surveys also detect early bearing wear and electrical arcing, since both produce ultrasonic signatures distinct from a gas or air leak's steady hiss.
Is ultrasonic detection safe to use near natural gas lines?
Ultrasonic detectors are passive listening devices and do not introduce ignition risk, which is why they're a standard tool for gas leak surveys. Any confirmed gas leak should still trigger immediate isolation procedures, not just a maintenance ticket.
What's the difference between ultrasonic detection and soap-bubble testing?
Soap-bubble testing only works on accessible, visible fittings and requires the leak to be large enough to form a bubble, which means it typically finds the leaks a facility already suspects rather than the ones hiding on overhead runs or behind equipment. Ultrasonic detection finds leaks at a distance, in noisy environments, and on components that are difficult to reach or see directly, which is why most structured survey programs use it as the primary method and reserve soap-bubble testing for confirming an exact leak point once ultrasonic has narrowed the search.
How much does an ultrasonic leak survey program typically save?
Facilities moving from no formal program to a quarterly ultrasonic survey commonly cut leakage from the 20–30% DOE benchmark down toward the well-maintained system range of under 10%. Book a demo at calendly.com/oxmaintapp/30min to estimate savings for your system size.
Stop losing utility budget to leaks you can't hear
Build a repeatable ultrasonic survey program, log every find against your asset register, and close the loop with tracked repair work orders — all inside one platform.