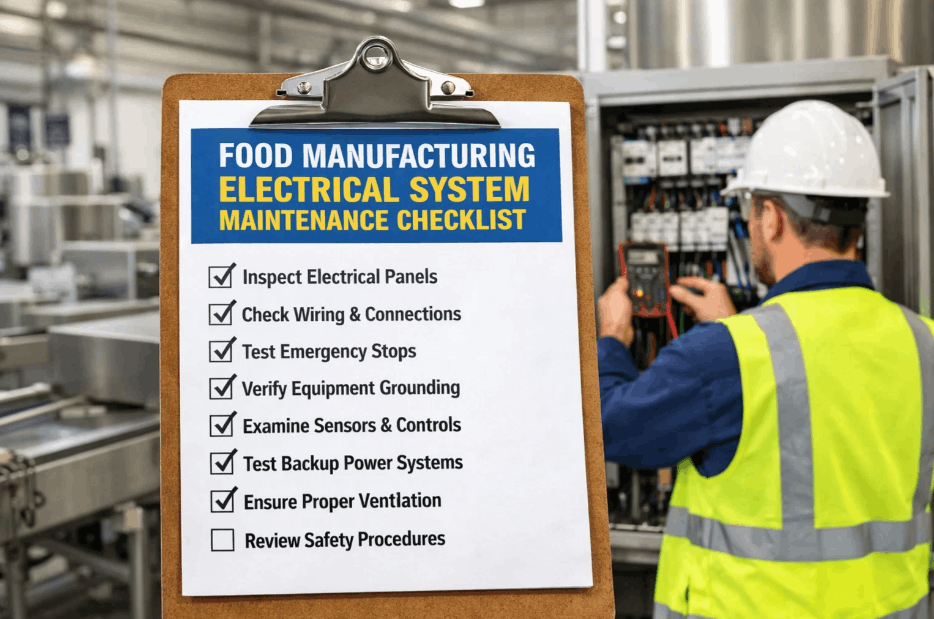
Food plant electrical system maintenance is no longer a reactive discipline — it is a precision-driven operational strategy that determines uptime, workforce safety, and regulatory compliance across every production shift. For facility engineers and maintenance managers overseeing industrial electrical panels, three-phase motors, and variable frequency drives (VFDs) in high-throughput food manufacturing environments, unplanned electrical failures translate directly into contamination risk, OSHA citations, and production losses that can reach tens of thousands of dollars per hour. The facilities that sustain reliable output across their UK, Canadian, German, and UAE operations share one common discipline: a structured, data-backed approach to food plant electrical maintenance built on predictive monitoring, CMMS automation, and NFPA 70E-aligned safety protocols.
Automate Your Electrical Maintenance Program
OxMaint's CMMS platform delivers predictive maintenance scheduling, panel inspection workflows, VFD health monitoring, and audit-ready documentation — all from one centralized system purpose-built for food manufacturing environments.
Why Electrical System Maintenance Is Critical in Food Manufacturing
Food processing facilities operate under electrical loads that cycle intensively — refrigeration compressors, conveyors, mixers, packaging lines, and HVAC systems drawing continuous power across multiple shifts. This operational profile creates cumulative stress on switchgear, motor windings, and drive electronics that conventional time-based maintenance schedules fail to detect before failure occurs. OxMaint's CMMS catches these failures before they happen — start your journey free today and put your team ahead of every breakdown.
Beyond production continuity, electrical system integrity is a food safety issue. Arc flash events, overheated motor control centers, and tripped VFDs mid-cycle can introduce foreign material contamination, disrupt temperature-controlled environments, and trigger unplanned production holds that require full sanitation restart. In FSMA-regulated US facilities, BRCGS-certified UK plants, HACCP-compliant Canadian operations, and DIN EN ISO-governed German factories, electrical system failures generate documentation requirements that extend well beyond the maintenance department.
The UAE's rapidly expanding food processing sector — driven by import substitution investment and free zone manufacturing growth — increasingly mirrors the compliance expectations of European and North American markets, making structured electrical asset management essential for facilities seeking export certifications.
Industrial Electrical Panel Maintenance: The Control Hub of Every Production Line
Electrical panels — main distribution boards, motor control centers (MCCs), and sub-panels — are the central nervous system of food plant operations. Panel failures cascade instantly: a single tripped breaker in the wrong circuit can halt an entire production line, compromise cold chain integrity, or disable critical ventilation in confined processing zones. Sign Up Free to see how OxMaint schedules and tracks every panel inspection in one place.
Thermal Imaging Inspection Cycles
Infrared thermography is the gold standard for non-invasive panel inspection, detecting hotspots in bus bars, breaker connections, and neutral terminals before they escalate to failures. Quarterly thermal scans of all panel interiors — conducted under load by qualified electricians in appropriate PPE per NFPA 70E arc flash requirements — provide objective condition data that neither visual inspection nor periodic testing alone can replicate. Results should be logged in the CMMS with trend photography for year-over-year comparison.
Torque Verification and Connection Tightening
Thermal cycling from production load variations causes connection hardware to loosen over time — a primary cause of arcing faults in food plant panels. Annual torque verification programs, using manufacturer-specified torque values for every terminal type, eliminate the high-resistance connections that thermal imaging will eventually detect. Document torque check completion in CMMS work orders with technician certification records attached.
Breaker Testing and Trip Curve Verification
Circuit breakers in food plant environments are subject to moisture, vibration, and contamination that can impair trip mechanisms over time. Primary injection testing of critical breakers — particularly those protecting motors, refrigeration compressors, and clean-in-place systems — verifies that trip curves match original specifications and that protective devices will respond correctly during fault conditions. This testing requirement appears in both NFPA 70B and IEC 60364 maintenance frameworks applicable across North American and European facilities respectively.
Enclosure Integrity and Contamination Control
Food plant environments introduce unique contamination threats to electrical enclosures: steam, washdown moisture, cleaning chemical aerosols, and condensation cycles that corrode terminals and degrade insulation. IP/NEMA rating verification during inspections — checking gaskets, cable entry seals, and door latching — prevents the moisture ingress that causes insulation breakdown and nuisance tripping in production areas.
Motor Maintenance in Food Manufacturing: Preventing the Most Common Failure Mode
Three-phase induction motors drive virtually every mechanical system in a food plant — conveyors, pumps, fans, mixers, and compressors. Motor failures are the single most common cause of unplanned electrical downtime in manufacturing facilities globally, and food processing environments accelerate the failure mechanisms that standard motor maintenance programs are designed to prevent.
High-pressure washdown, thermal shock from temperature-controlled zones, food-grade lubricant requirements, and variable load profiles combine to create motor operating conditions that shorten winding life, accelerate bearing wear, and increase vibration-induced shaft fatigue. A comprehensive motor maintenance manufacturing program addresses all four failure pathways through scheduled inspection, condition monitoring, and proactive intervention triggered by data — not failure events. Book a Demo to see how OxMaint's motor maintenance workflows work in practice.
Detects bearing defects, imbalance, and misalignment weeks before failure. Sensors feed CMMS condition modules — enabling planned bearing replacement instead of emergency shutdowns.
Annual megohmmeter testing measures moisture ingress and winding degradation. Trending results against IEEE 43 criteria lets teams schedule rewinds before in-service failure occurs.
Food plants require NSF H1-rated grease at OEM intervals. CMMS work orders specify the correct grease type and quantity per motor — eliminating technician guesswork that causes premature wear.
Detects rotor and mechanical faults by analyzing supply current — with no motor disconnection required. Ideal for food plants where continuous production limits offline testing opportunities.
VFD Maintenance in Industrial Food Plants: Protecting Your Most Sensitive Electrical Assets
Variable frequency drives are the most electronically complex and environmentally sensitive components in food plant electrical systems. VFDs manage motor speed, torque, and energy consumption across conveyor systems, pump arrays, and processing equipment — but their power electronics, cooling systems, and control circuits are vulnerable to the temperature, vibration, and contamination conditions that food plant environments generate continuously.
VFD maintenance industrial programs must address three distinct failure pathways: cooling system degradation, DC bus capacitor aging, and control circuit contamination — each requiring different inspection techniques and replacement intervals that standard electrical maintenance schedules rarely capture with sufficient precision. Sign Up Free and configure VFD inspection work orders with built-in checklists for every failure pathway.
Clean heat sink fins and inspect cooling fans every quarter. Blocked fins cause thermal shutdowns during production. Replace fan bearings every 3–5 years to prevent IGBT module damage and full drive failure.
Capacitors degrade over time due to heat and ripple current. Check capacitor health parameters through the drive's diagnostics at each annual inspection — and schedule replacement before end-of-life threshold is reached.
Food plant aerosols and condensation corrode control boards. Inspect and purge with clean air annually. For high-contamination areas, install positive pressure filtered ventilation as a long-term solution.
Lost parameter files mean hours of re-commissioning after a drive failure. CMMS-triggered backups after every change and on annual schedule ensure same-day production restart when a drive needs replacement.
How AI Vision Enhances Food Plant Electrical System Maintenance
Artificial intelligence and computer vision are transforming how food manufacturers monitor, inspect, and maintain electrical infrastructure — moving beyond scheduled human inspections toward continuous automated surveillance that detects developing faults in real time without interrupting production.
For maintenance managers in UK food factories, Canadian processing plants, German manufacturing facilities, and fast-growing UAE industrial zones, AI-powered electrical monitoring delivers the anomaly detection capability that human inspection cycles — no matter how well-structured — cannot provide between scheduled visits.
Fixed thermal cameras scan panels and bus bars 24/7. AI detects hotspots between scheduled inspections — catching faults in energized equipment that can't be manually checked during active production.
IoT sensors establish each motor's normal vibration profile. AI flags deviations weeks before failure and delivers plain-language fault descriptions — no specialist analyst needed to interpret the data.
AI correlates current, temperature, and voltage trends to identify multi-parameter failure signatures. Teams get remaining useful life estimates and targeted action recommendations before disruptions occur.
Computer vision classifies thermal findings and generates condition reports with severity rankings — automatically creating CMMS work orders. No manual data entry. No anomaly goes undocumented.
Predictive Maintenance for Electrical Systems: Moving Beyond Time-Based Schedules
Predictive maintenance electrical systems strategies use real-time condition data to trigger maintenance interventions based on actual equipment health rather than fixed time intervals. For food plant electrical assets — which experience highly variable load profiles, environmental stress cycles, and contamination exposure — predictive approaches consistently outperform calendar-based programs in both cost effectiveness and failure prevention. Want to shift from reactive to predictive? Book a Demo and we'll show you exactly how OxMaint builds this into your existing workflow.
CMMS Platforms for Electrical Maintenance: Centralizing Asset Management
A CMMS electrical maintenance platform transforms electrical maintenance from a reactive, paper-based discipline into a data-driven program with scheduled work orders, condition-based triggers, asset history tracking, and compliance documentation built into every maintenance interaction. For food plant electrical teams managing hundreds of assets across multiple production zones, CMMS automation eliminates the scheduling gaps and documentation failures that reactive maintenance programs cannot avoid. OxMaint gives you all of this in one platform — start your journey free and see your entire asset program come together in minutes.
Sign Up Free to explore OxMaint's electrical asset management tools and see how structured CMMS automation closes the maintenance gaps that drive unplanned downtime in food manufacturing environments.
| Maintenance Activity | Asset Type | Recommended Frequency | Detection Method | CMMS Integration |
|---|---|---|---|---|
| Thermal Imaging Scan | Panels, MCCs, Switchgear | Quarterly | Infrared camera / AI vision | Photo attachment, hotspot trending |
| Torque Verification | All panel terminations | Annual | Calibrated torque wrench | Work order checklist, sign-off |
| Vibration Analysis | All process motors | Monthly / Continuous | Handheld / IoT sensor + AI | Trending charts, alert triggers |
| Insulation Resistance Test | Motors, cables | Annual | Megohmmeter (IEEE 43) | Test result logging, trend alerts |
| VFD Cooling Inspection | All variable frequency drives | Quarterly | Visual + thermal | Inspection checklist, photo record |
| Capacitor Health Check | VFDs (DC bus) | Annual | Drive diagnostic parameters | Parameter log, replacement trigger |
| Breaker Trip Testing | Critical circuit breakers | Every 3–5 years | Primary injection testing | Test certificate attachment |
| Motor Lubrication | All greased-bearing motors | Per OEM schedule | Interval / condition trigger | Lube type, quantity, technician ID |
NFPA 70E Electrical Safety Compliance in Food Plant Environments
Electrical safety compliance NFPA 70E governs arc flash hazard analysis, safe work practices, PPE requirements, and energized work permit procedures for electrical maintenance in US food manufacturing facilities. In Canadian plants, CSA Z462 mirrors NFPA 70E requirements; UK facilities operate under BS 7671 (IET Wiring Regulations) and the Electricity at Work Regulations 1989; German plants follow DIN VDE standards and DGUV Regulation 3.
Across all regulatory frameworks, the core requirements are consistent: electrical hazard analysis before every maintenance task, appropriate PPE selection based on incident energy calculations, and documented energized work authorizations when de-energization is not feasible. CMMS platforms enforce these requirements by embedding PPE checklists, arc flash boundary reminders, and permit-to-work authorization steps directly into electrical maintenance work orders — making compliance procedurally unavoidable rather than dependent on technician memory. Book a Demo to see OxMaint's permit-to-work and compliance workflows live.
Common Electrical Maintenance Failures and How CMMS Prevents Them
Most electrical failures in food plants are not caused by bad equipment — they are caused by maintenance programs that rely on memory, paper, and manual follow-up. OxMaint eliminates every one of these gaps automatically. Book a Demo to see how facilities like yours have stopped these failures for good.
Inspection Intervals Missed During Peak Production
Quarterly thermal scans and annual motor tests are routinely deferred during high-production periods when maintenance resources are redirected to reactive work. CMMS automated scheduling generates inspection work orders independently of production pressure — and escalates overdue tasks to supervisors before the inspection window closes, making deferred inspections visible rather than silently accumulating.
Undocumented VFD Parameter Changes
VFD parameters adjusted during production troubleshooting are frequently not backed up or documented — creating a situation where the drive's current configuration exists only in the drive's memory, not in any retrievable record. CMMS change management workflows require documentation of every parameter modification with before-and-after values, creating the configuration control record that enables accurate drive replacement and audit trail compliance.
Incomplete Arc Flash PPE Documentation
NFPA 70E-required PPE selection records for energized electrical work are frequently verbal decisions that never enter a documentation system. CMMS energized work permits require documented PPE selection and supervisor authorization before work orders can be closed — creating the compliance record that protects facilities during OSHA inspections and incident investigations.
Motor Failure Without Historical Data
When a motor fails without a complete maintenance history in the asset record, root cause analysis is impossible and recurrence prevention is guesswork. CMMS asset history — capturing every inspection result, lubrication event, and vibration reading for each motor's operational life — transforms failure investigation from speculation into evidence-based analysis, supporting both immediate corrective action and long-term reliability improvement.
Best Practices for Food Plant Electrical Maintenance Programs
Register every panel, motor, VFD, and cable in the CMMS with model, install date, and location. A complete asset register is the foundation of every scheduled task and compliance record.
Score assets by production impact and failure consequence. Focus monitoring investment on high-criticality equipment — not every motor needs the same inspection frequency.
Sensor data only creates value when it triggers action. Connect monitoring outputs to CMMS alert thresholds so work orders generate automatically when readings exceed safe limits.
Track MTBF, planned vs. unplanned ratio, and overdue task counts monthly. Share results with operations leadership to catch program drift before it becomes a failure event.
Ready to Build a Smarter Electrical Maintenance Program?
OxMaint gives food plant maintenance teams automated scheduling, condition monitoring integration, NFPA 70E compliance workflows, and real-time asset health visibility — purpose-built for industrial food manufacturing operations.
Frequently Asked Questions: Food Plant Electrical System Maintenance
How often should electrical panels be thermally inspected in a food plant?
Industry best practice, aligned with NFPA 70B and IEC maintenance frameworks, recommends quarterly thermal imaging inspection of all energized electrical panels in food plant environments. Facilities with high humidity, frequent washdown exposure, or panels supporting critical refrigeration or processing systems should consider semi-annual scans. All thermal inspections should be conducted under representative load conditions — ideally above 40% of rated capacity — to ensure that thermal anomalies are detectable in the scan data.
What are the most common causes of VFD failure in food manufacturing?
The leading causes of VFD failure in food plant environments are cooling system failures (blocked heat sinks and failed cooling fans), DC bus capacitor aging accelerated by high ambient temperatures, control board contamination from cleaning chemical aerosols and condensation, input power quality problems including voltage transients and harmonics, and improper installation practices including inadequate clearance and missing line reactors. A CMMS-driven maintenance program addressing all five failure pathways typically extends VFD service life by 30 to 50 percent compared to reactive maintenance approaches.
What NFPA 70E documentation is required for food plant electrical maintenance?
NFPA 70E requires documentation of arc flash hazard analysis results for all equipment where energized work may occur, energized electrical work permits for any work performed inside the restricted approach boundary, PPE selection basis for each task category, and lockout/tagout verification records. Food plants operating in Canada, the UK, and Germany face equivalent requirements under CSA Z462, the Electricity at Work Regulations, and DGUV Regulation 3 respectively. CMMS platforms can embed all required documentation steps into electrical work order workflows to enforce systematic compliance.
How does predictive maintenance differ from preventive maintenance for electrical systems?
Preventive maintenance is time-based — inspections and replacements occur on fixed calendar intervals regardless of actual equipment condition. Predictive maintenance is condition-based — interventions are triggered by measured condition indicators such as vibration amplitude, insulation resistance trending, thermal anomalies, or capacitor health parameters that indicate approaching failure. Predictive programs reduce unnecessary maintenance activity on healthy assets while ensuring that genuinely degraded assets receive attention before failure occurs — consistently delivering lower total maintenance cost and higher equipment availability than time-based programs alone.
What electrical maintenance KPIs should food plant maintenance managers track?
Essential electrical maintenance KPIs include mean time between electrical failures (MTBF) by asset class, planned to unplanned maintenance ratio, thermal inspection defect rate per panel, motor vibration exceedance rate, VFD fault frequency trend, work order completion rate against schedule, corrective action closure time for identified defects, and arc flash incident frequency rate. Tracking these metrics through a CMMS dashboard allows maintenance managers to demonstrate program effectiveness, justify capital investment in condition monitoring technology, and identify asset classes requiring program adjustments before failure patterns emerge.
Can CMMS systems integrate with industrial IoT sensors for electrical monitoring?
Yes. Modern CMMS platforms including OxMaint support integration with industrial IoT sensor networks via API connections, MQTT protocols, and OPC-UA data exchange — enabling continuous vibration, temperature, current, and power quality data from field sensors to feed directly into the CMMS asset history and trigger condition-based work orders when predefined thresholds are exceeded. This integration eliminates manual data entry from condition monitoring rounds and ensures that sensor-detected anomalies generate maintenance responses within the same system that manages all scheduled and corrective maintenance activity.