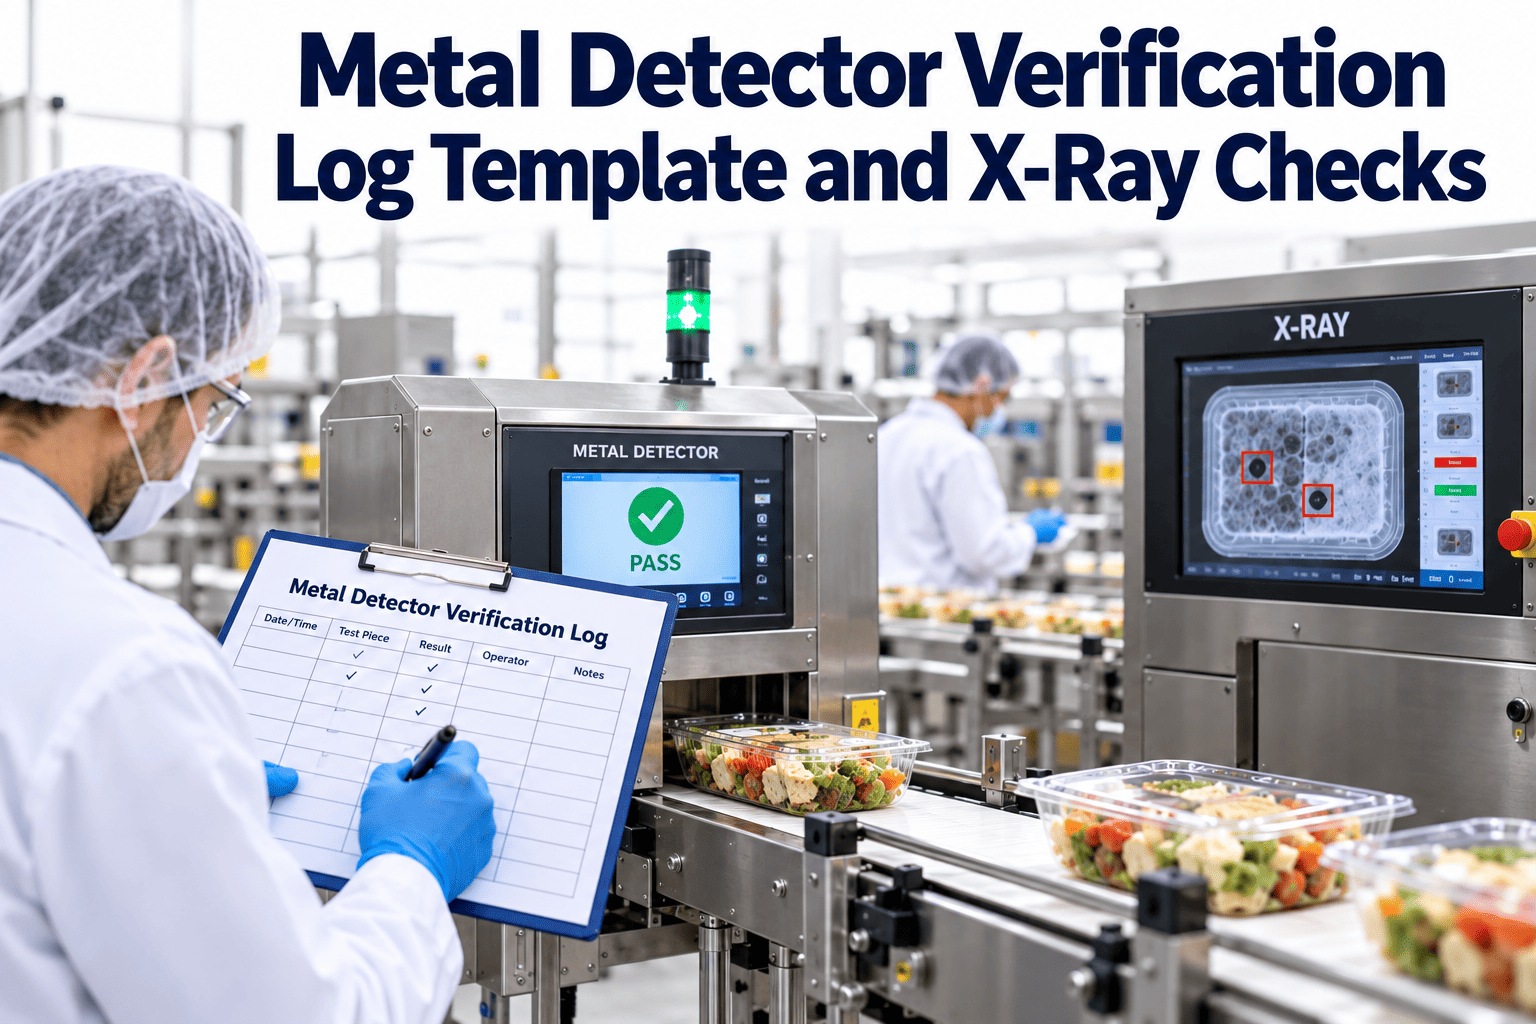
A metal detector that passes its test piece at 6 a.m. tells you little about the pack that ran through at 2 p.m. unless someone checked it again and wrote the result down. Verification logs are the proof that foreign material controls work, and weak logs are a common audit finding. This guide gives you a ready-to-adapt log layout for metal detectors and X-ray systems, explains what each column is for and shows how to handle failed checks, using a maintenance and inspection platform to keep the records.
Metal Detector Verification Log Template and X-Ray Checks
Record every test piece result, reject confirmation and corrective action in a layout that auditors can read in seconds and operators can complete in under a minute.
What a verification log must prove
The detector can detect
Test pieces of defined size and type were detected at the agreed sensitivity, in the defined position.
The reject system can reject
Contaminated product was diverted or stopped and held where only authorised staff can reach it.
Failures were handled
When a check failed, product was controlled, the cause found and the line released by a named person.
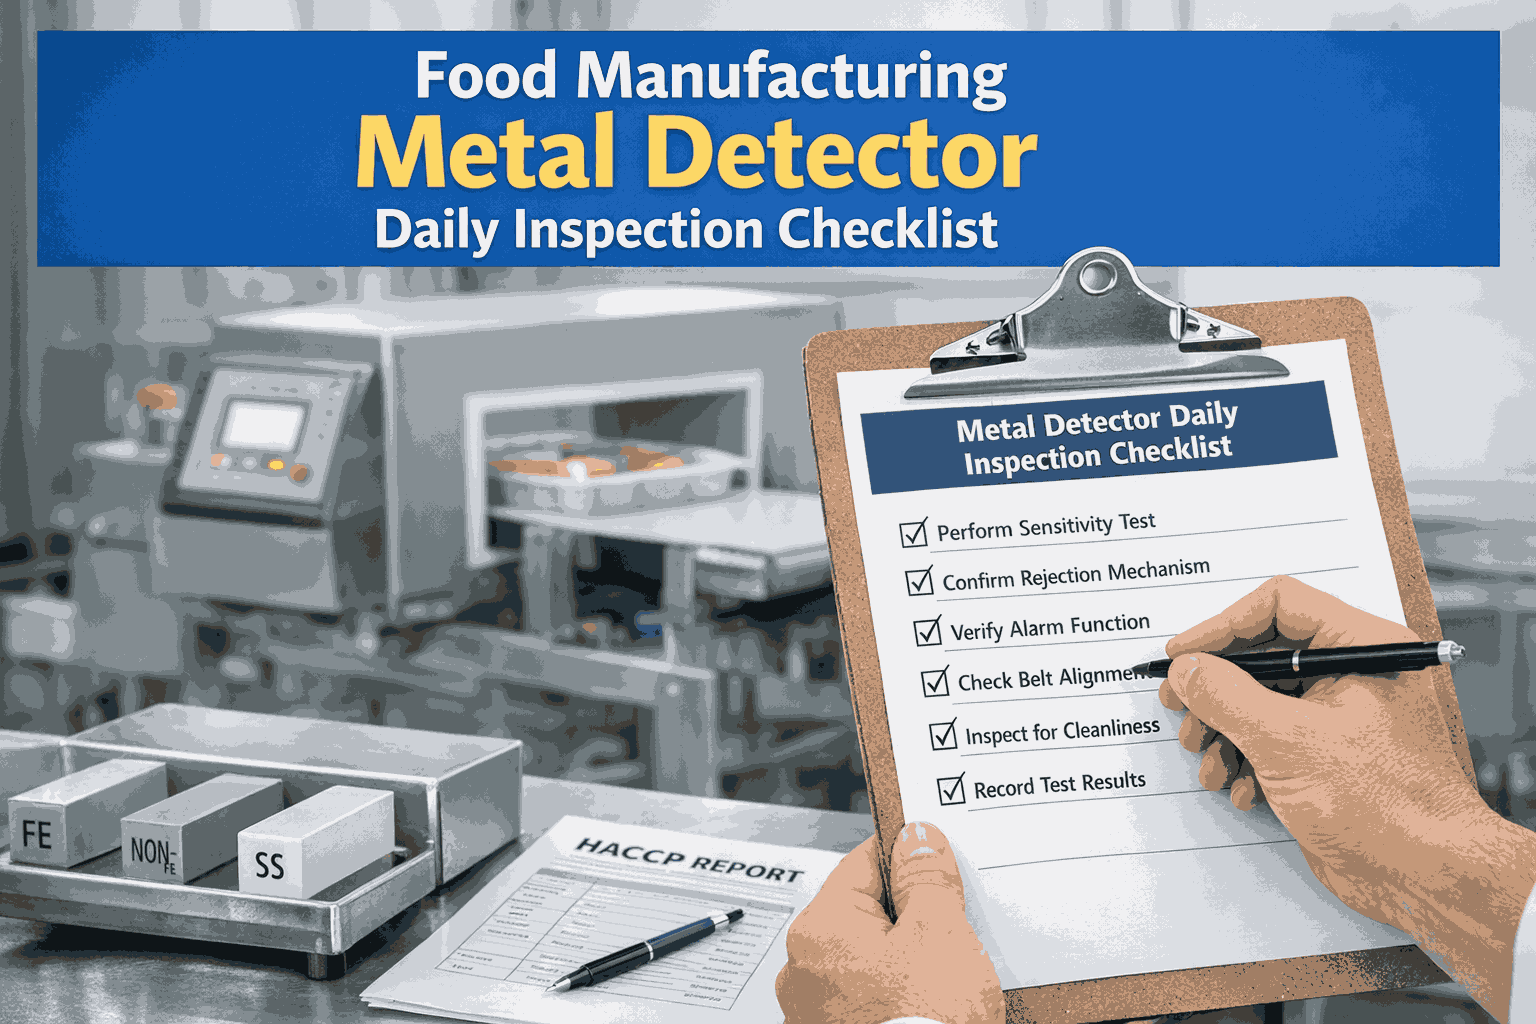
The log template, column by column
Copy this layout into your own controlled document or digital form. Adapt the fields to your site procedure, customer requirements and certification scheme.
| Column | What to enter | Why it is there |
|---|---|---|
| Date, shift and line | Calendar date, shift name and line or detector ID. | Ties each check to a place and production window. |
| Product and batch | Product name, code and lot or batch running. | Product effect changes sensitivity, so results are product specific. |
| Check type | Start up, scheduled, changeover, after repair, end of run. | Shows checks happen when risk changes, not only on a clock. |
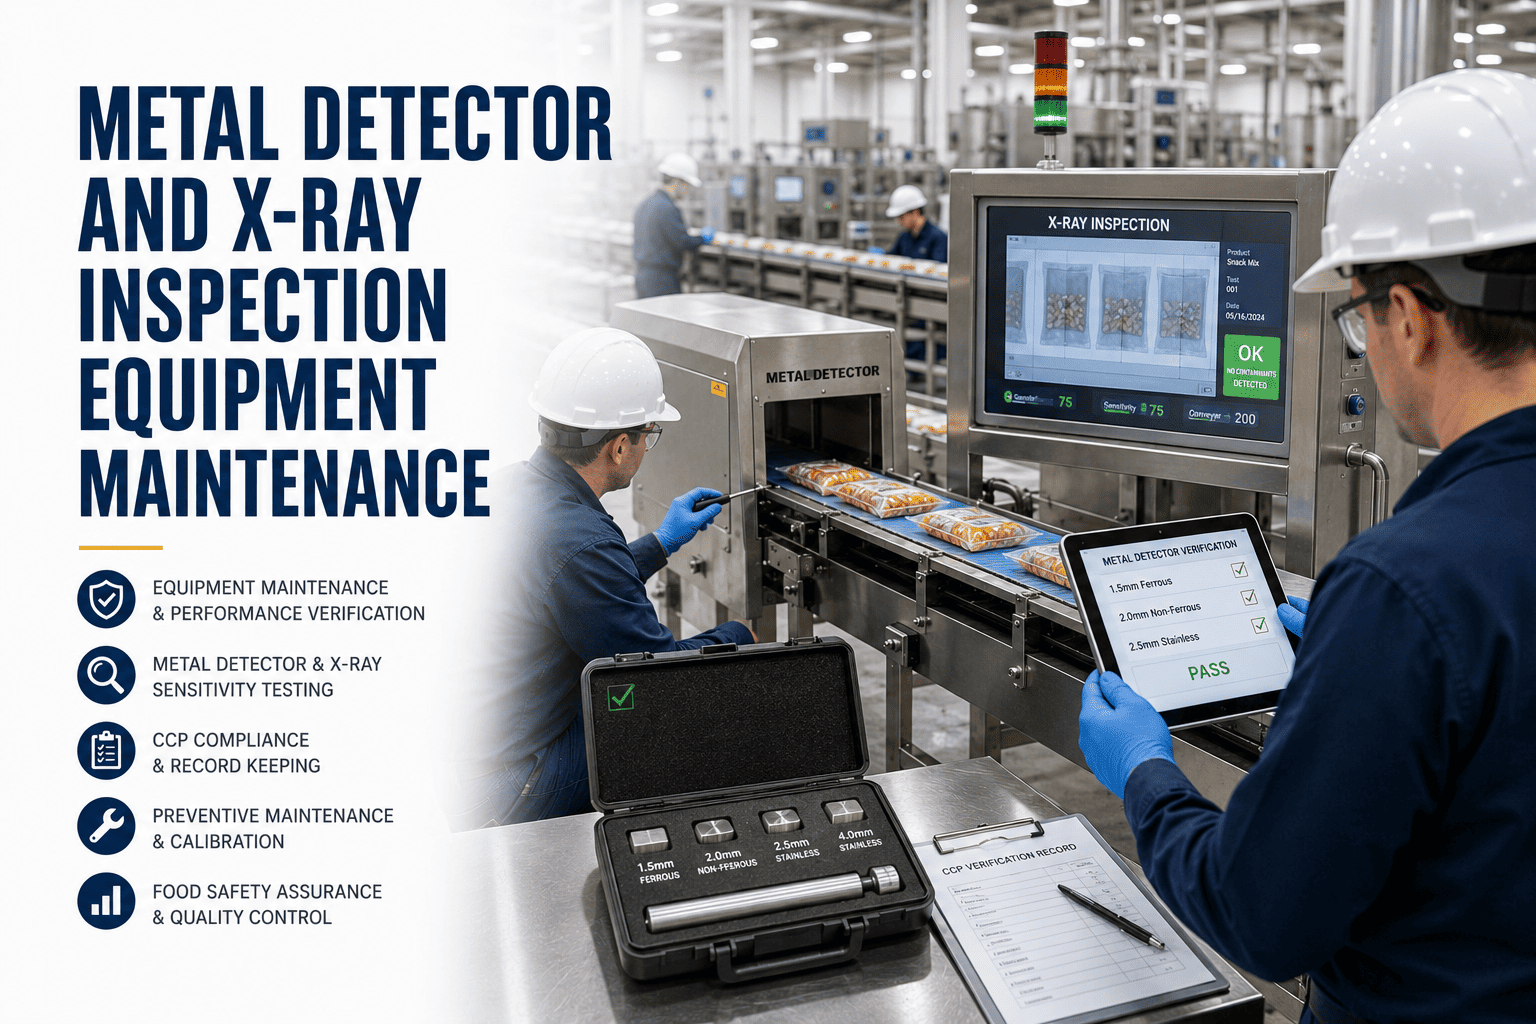
| Test piece ID and size | Ferrous, non-ferrous and stainless steel pieces with their stated sizes. | Proves the checks used the agreed standard pieces. |
| Test position | Where the piece passed through, for example centre or edge of the aperture. | Detection varies across the aperture, so position matters. |
| Detected and rejected | Yes or no for detection and for reject action. | Separates a sensing problem from a rejecting problem. |
| Alarm and fail safe checks | Confirmation that alarms, belt stop and bin lock work as designed. | Shows the system fails safe, not silently. |
| Result and action | Pass or fail, with the action taken and product disposition. | Closes the loop on every failure. |
| Operator and verifier | Initials of the tester and of a supervisor or quality reviewer. | Provides accountability and independent review. |
A completed log, shown with invented example entries
These rows are fictional and exist only to show the level of detail that makes a record defensible. Sizes and times are placeholders.
| Time | Check type | Piece | Result | Action and notes | Initials |
|---|---|---|---|---|---|
| 06:05 | Start up | Ferrous, non-ferrous, stainless | Pass | All pieces detected and rejected at centre position. | AB / CD |
| 09:30 | Changeover | All three | Pass | New product program loaded and tested before restart. | AB / CD |
| 12:10 | Scheduled | Stainless | Fail | Not rejected. Line stopped, product since 09:30 held, maintenance called. | EF |
| 12:55 | After repair | All three | Pass | Reject pusher air line replaced. Held product re-run through detector. | EF / GH |
| 14:40 | End of run | All three | Pass | Final check complete. Log reviewed by quality. | AB / GH |
Choosing and handling test pieces
Test pieces are the measuring standard for the whole check. Damaged, unlabelled or swapped pieces undermine every result that follows.
Typical categories
- Ferrous: iron based metal, usually the easiest to detect.
- Non-ferrous: metals such as aluminium and copper, harder to detect than ferrous.
- Stainless steel: usually the most difficult of the three, so it often sets the working sensitivity.
Handling rules
Use certified pieces with a unique ID, keep them in a controlled location and inspect them for damage. Use pieces that are food safe and visible, such as colour coded, so a lost piece is easy to find.
Set sizes from the right sources
- Follow your hazard analysis, customer specifications and detector supplier guidance.
- Record the approved sizes per product on the log header.
- Review sizes when products or packaging change.
Replace paper logs with checks nobody can skip
Oxmaint schedules recurring inspections, collects results on mobile and raises corrective work orders the moment a check fails.
When to test: events that should trigger a check
Time based
- Start of production
- At a fixed interval during the run, set by risk assessment
- End of production
Event based
- Product or pack changeover
- After cleaning or maintenance on the detector
- After any fault, alarm or belt jam
Condition based
- After a change in operating settings
- When product temperature or moisture shifts sharply
- When an unexpected reject rate appears
There is no single correct interval. Your own risk assessment, customer requirements and certification standard set the minimum, and most plants add event based checks on top.
- Write the frequency in the procedure
- Show it on the log header
What to do when a check fails
Stop and secure
Stop the line or divert product and isolate everything made since the last passing check.
Repeat the test
Confirm the failure with the correct test pieces and note exactly which piece, position and result.
Investigate
Check settings, reject device, air supply, belt condition and recent product changes.
Re-inspect held product
Pass held product back through a working detector according to the written procedure.
Release and record
Restart only after a passing check, and record the cause, action and approver.
Metal detector or X-ray: what each log needs to show
| Aspect | Metal detector | X-ray inspection |
|---|---|---|
| What it finds | Metal contaminants. | Dense foreign material such as metal, glass, stone and some bone or hard plastic, depending on the system and product. |
| Verification standard | Ferrous, non-ferrous and stainless test pieces. | Test pieces or test cards of the relevant materials and sizes. |
| Product effect | Wet, salty or warm product can affect sensitivity. | Product density and pack geometry affect detection limits. |
| Extra checks | Reject confirmation, alarms, bin lock. | Image quality, reject confirmation, safety interlocks and any radiation safety checks required locally. |
| Additional log fields | Sensitivity setting, product program. | Program name, detection settings, image check outcome. |
Whichever technology you use, the principle is the same: prove detection, prove rejection and show what happened when either failed.
Training operators to run the check properly
Know the purpose
Operators who understand the hazard take the check seriously and are less likely to log a result they did not witness.
Use the right piece
Practise selecting the correct piece, handling it safely and passing it through at the defined position.
Read the response
Teach what a correct alarm, reject and bin result looks like, and what a partial result means.
Act on a fail
Make stopping the line and isolating product an expected response with no blame attached.
Record honestly
Explain that a recorded fail with good action is a success for the system, while a hidden fail is a serious problem.
Refresh regularly
Repeat the training for new starters, after procedure changes and when audits show drift.
Reject system checks that get missed
Symptom
Detector alarms but product still reaches the pack.
Typical cause to check
Reject timing, air pressure, worn pusher or blocked reject chute.
Symptom
Frequent false rejects with no contamination.
Typical cause to check
Product effect, vibration, loose mounting, wet aperture or nearby metal.
Symptom
Sensitivity drifts between checks.
Typical cause to check
Temperature change, electrical interference, damaged cable or setting changes.
Symptom
Belt stops or slips during a test.
Typical cause to check
Belt wear, tracking, tension or drive fault, which maintenance should record.
Maintaining the detector so the log stays green
Aperture and head
Keep the search head clean, dry and free of damage, and check mounting and cables for wear.
Belt and rollers
Inspect belt condition, tracking and splices, since worn belt fragments can themselves become a contamination risk.
Reject device
Check air supply, pushers, flaps and timing, and test the lockable collection bin.
Controls and settings
Control access to settings and log any change with who approved it and why.
Service and calibration
Schedule supplier service visits and keep the reports against the asset record.
Spares
Hold critical spares such as belts and reject parts so a fault does not leave the line unprotected.
Monthly review: turn the log into improvement
Count the failures
Group failed checks by line, shift, product and cause. Repeats point to a maintenance or setup problem.
Review reject trends
Look at what the reject bin actually contained, and whether false rejects are hiding a developing fault.
Close the loop
Turn recurring causes into preventive tasks, spare parts decisions or procedure changes, and record them.
Position of the detector in the process
A detector only protects against contamination that happens upstream of it. Where it sits in the line shapes what it can catch and what still needs other controls.
Questions to review with engineering
- Is the detector as close to the end of the process as practical?
- What sources of metal exist downstream, such as sealing jaws or packaging machinery?
- Do metal frames or conveyors near the aperture reduce sensitivity?
- Is there a second control point on high risk lines, such as raw material screening?
Layered controls
- Sieves, magnets and filters can complement detectors.
- Maintenance practices such as tool control reduce the source risk.
- Document how each layer is verified.
Reviewing the log: signals worth acting on
Warning signs in a log
- Every result is a pass with identical handwriting.
- Checks are logged at suspiciously regular times.
- Failures appear without an action or product disposition.
- Test piece IDs are blank or repeated incorrectly.
- Verifier initials are added days later.
Signs of a healthy log
- Checks follow both the schedule and real events.
- Failures have a clear cause, action and release approval.
- Trends in rejects are reviewed and explained.
- Sensitivity changes are controlled and justified.
- Quality reviews completed logs on a set cycle.
Common mistakes in verification practice
Testing only one piece type
Passing a ferrous piece says little about stainless steel, which is usually harder to detect.
Testing with the product absent
Product effect changes sensitivity, so checks should reflect the product that is actually running.
Confirming detection but not rejection
An alarm that does not divert the pack gives false comfort. Always confirm the reject action.
Skipping the repeat after repairs
Any maintenance on the detector or reject unit should be followed by a full verification before restart.
Leaving settings uncontrolled
Unrecorded sensitivity changes make later results impossible to interpret.
Logging after the fact
Filling in the sheet at the end of the shift loses accuracy and invites copied entries.
Keeping the records ready for audit
Auditors usually sample a few days of logs, then follow one failure from the log to the corrective action and the product disposition. Make that path short and obvious, and keep completed logs for the period your scheme, customers and procedures require.
- File logs by line and month
- Link each failure to its work order
- Keep test piece certificates with the log set
- Store service reports against the detector record
How Oxmaint supports foreign material control records
Verification is an inspection task, and the detector is an asset that needs maintenance. A maintenance management system can hold both in one place.
Relevant capabilities
- Recurring inspection tasks with required fields for each check type
- Mobile entry so results are logged at the line, not later
- Automatic corrective work orders when a check is marked as failed
- Asset history for each detector, including repairs and service reports
- Preventive maintenance for belts, reject devices and air supply
- Reports on missed checks and repeat failures by line
Scope note
- Oxmaint records checks and maintenance. It does not replace the detector or your hazard analysis.
- Product hold and release decisions stay with your quality procedure.
Frequently asked questions
How often should a metal detector be verified?
The interval comes from your risk assessment, customer needs and certification scheme. Most plants test at start up, at set intervals, at changeover and after repairs.
Which test pieces should be used?
Typically ferrous, non-ferrous and stainless steel pieces, in sizes set for each product. Use certified, identified pieces and follow your procedure.
What if the detector fails a check?
Stop or divert, isolate product since the last pass, find the cause, re-inspect held product and release only after a passing check, with every step recorded.
Does an X-ray system need the same log?
The same principles apply, with extra fields for programs, image checks and local safety requirements. You can book a demo to see inspection logs built for your lines.
Can the log be kept in a CMMS?
Yes. Recurring inspection tasks, mobile entry and corrective work orders suit verification records well, alongside the detector's maintenance history.
Make every verification check count
Adopt a clear log layout, tie checks to real risk events and connect failures to corrective action and maintenance. Start with one line and expand once the routine is solid.