A single seized idler bearing on your longest conveyor line can shut down an entire production floor in under four minutes — and the ripple effect through downstream processes means that fulfillment centers lose up to $20,000 per hour during unplanned conveyor outages. Yet 37% of companies still experience maintenance-related conveyor downtime regularly, most of it caused by the same three failure modes — belt mistracking, motor and drive faults, and roller seizure — all of which are detectable weeks in advance through structured inspection and Start automated PM scheduling that never misses an interval with Oxmaint.
Material Handling Maintenance Guide 2026
Stop Reacting to Conveyor Failures. Start Predicting Them.
Belt mistracking, motor overheating, and roller seizure account for the vast majority of unplanned conveyor stops. All three are preventable. This guide shows you exactly how.
$20K/hr
Cost of unplanned conveyor outage in fulfillment
40%
Downtime reduction with predictive monitoring
30–40%
Of stoppages caused by electric drive faults
98%+
Uptime achievable with structured PM program
The Anatomy of a Conveyor Failure
Most conveyor failures don't happen suddenly — they build through a predictable sequence of neglected warning signs. Understanding where failures originate is the first step to building a maintenance program that stops them before they shut you down.
Conveyor System Failure Mode Map
Belt System
28% of failures
Mistracking / Edge Wear
Warning: belt drifting, material spilling off one side
Splice Failure
Warning: fastener heads visible, edge lifting at joint
Belt Slippage
Warning: burning rubber smell, belt vibrating at startup
Motor and Drive System
30–40% of failures
Bearing Overheating
Warning: rising motor temperature trend, abnormal vibration
Gearbox Oil Degradation
Warning: excessive noise, heat from gearbox housing
Drive Belt Wear
Warning: inconsistent belt speed, glazed belt surface
Rollers and Idlers
24% of failures
Roller Seizure
Warning: grinding or squealing, flat spot worn into belt cover
Bearing Contamination
Warning: dry bearing noise, excessive heat at roller end
Material Buildup on Rollers
Warning: increased motor load, visible encrustation
Pulleys and Structure
18% of failures
Pulley Lagging Wear
Warning: belt slippage on drive pulley, uneven wear pattern
Frame Misalignment
Warning: consistent belt drift over long distances
Structural Fastener Loosening
Warning: vibration increasing, visible frame flex under load
High risk — detected in daily walk-through
Medium risk — detected in weekly inspection
Standard risk — detected in monthly deep check
Belt Tracking: The Most Misunderstood Maintenance Problem
Belt mistracking is the single most common cause of premature belt replacement in material handling operations. It destroys belt edges, damages frames, spills material, and strains motors — yet most shops treat it as a recurring nuisance rather than a solvable maintenance problem. Track every belt adjustment and alignment check in Oxmaint to build the history that reveals the true root cause.
Belt drifts consistently to one side along entire length
Root cause: Misaligned pulley or crooked frame structure
Fix: Measure frame diagonals, square drive/tail pulley to ±1mm
Belt drifts only in one localized section
Root cause: Misaligned or seized idler in that section
Fix: Start adjustment 15–20m upstream of drift point. Adjust idler 1/4 turn increments.
Belt runs off-center on return side only
Root cause: Material carryback on return rollers creating irregular crown
Fix: Clean all return rollers. Adjust scraper blade tension to prevent carryback.
Belt tracks correctly when empty, drifts under load
Root cause: Off-center loading at the feed point
Fix: Reposition feed chute to center material on belt width. Check for uneven flow.
Belt runs in bow or banana shape
Root cause: Belt not joined squarely or excessive belt camber
Fix: Re-splice with square ends. Use self-aligning idlers. Increase tension if belt is too stiff to conform.
01
Always start with return run adjustments, working toward the tail pulley. Then adjust top run in the direction of belt travel.
02
Make small, incremental idler adjustments — no more than 1/4 to 1/2 turn at a time. Let the belt run 3 full revolutions before evaluating the result.
03
The belt moves toward whichever end of an idler is advanced in the direction of belt travel. Advance the side where the belt is drifting to pull it back to center.
04
Only adjust drive or tail pulleys after all idler adjustments have been attempted. Pulley adjustments affect the entire system — never adjust both sides simultaneously.
05
Cleanliness is foundational. Material buildup on rollers and pulleys creates a new, irregular surface that overrides all alignment adjustments.
Conveyor PM Schedule: What to Check and When
Effective conveyor maintenance is not a single annual event — it is a layered system of checks at increasing depth, each designed to catch a different category of failure at its earliest and least expensive stage. Book a demo to see how Oxmaint auto-generates every work order below at the right interval for every conveyor line in your facility.
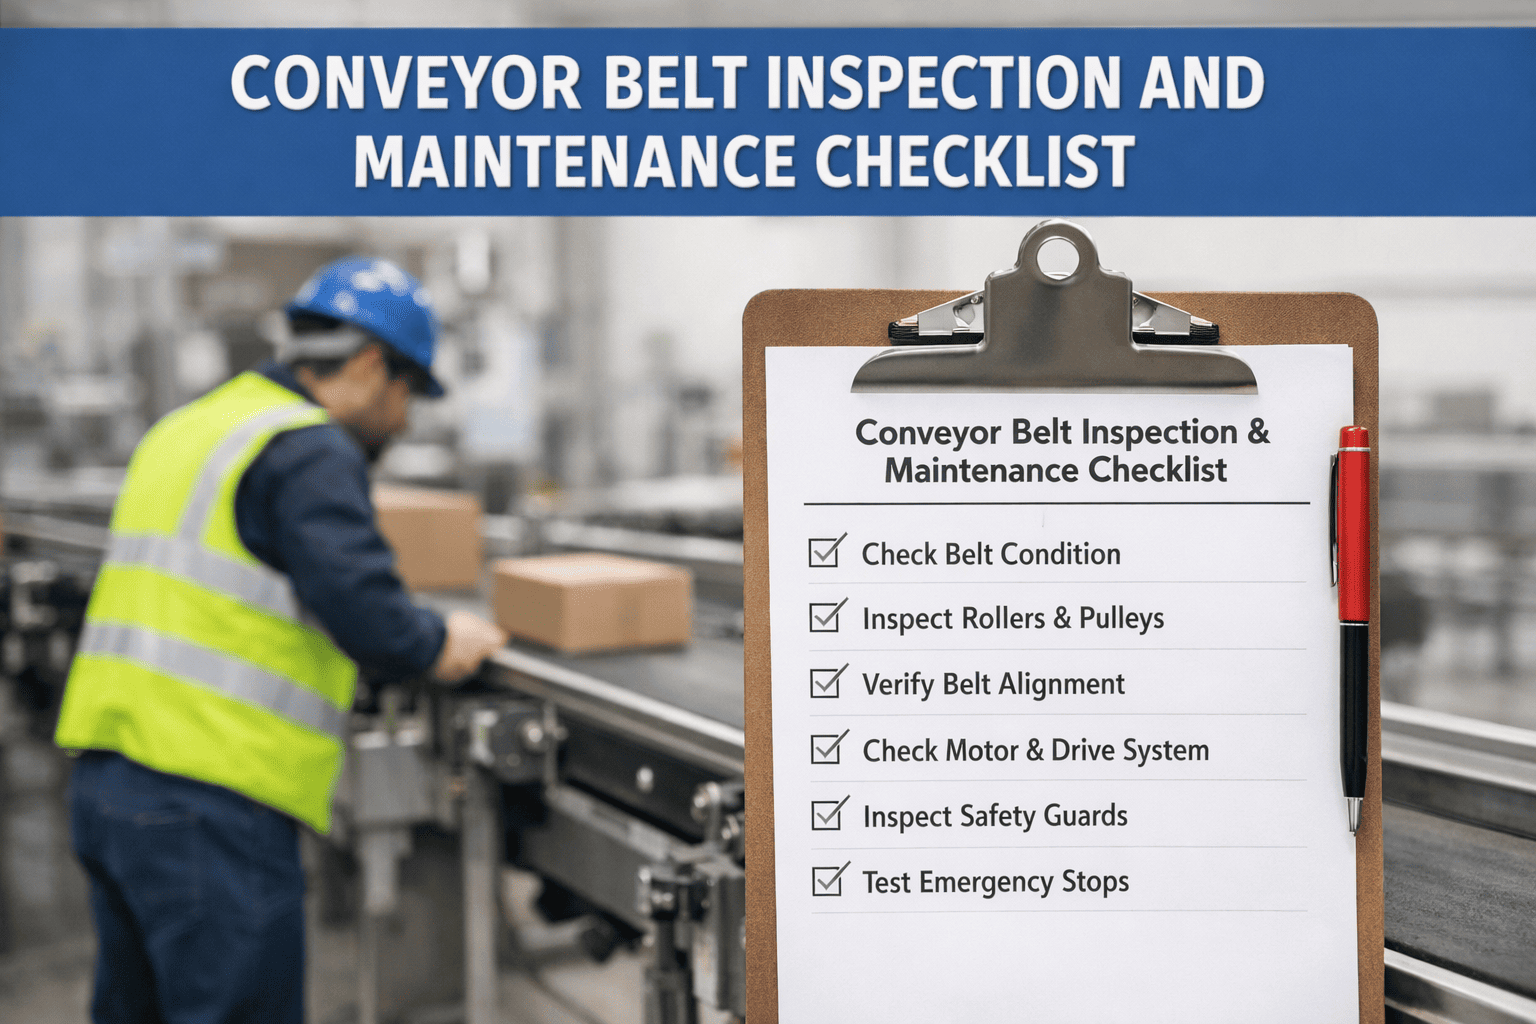
Daily Checks
Belt Surface and Tracking
Walk the full length on both sides. Look for cuts, tears, fraying, and edge damage. Confirm belt runs centered on all pulleys — any visible drift to one side requires immediate investigation before it destroys belt edges.
Auditory Walk-Through for Rollers
Listen for grinding, squealing, or rattling from any idler or return roller. A seized roller creates friction that burns flat spots into belt covers overnight — early detection means a $50 roller replacement instead of a full belt replacement.
Motor Temperature and Drive Noise
Check motor housing temperature by touch or thermometer. Listen for unusual noise from gearboxes. Electric drives cause 30–40% of unexpected conveyor halts — daily monitoring catches bearing or alignment faults weeks before failure.
Material Spillage and Carryback
Check under transfer points and along return side for accumulated material. Carryback buildup on return rollers causes tracking issues and creates fire hazards in dusty or dry material environments.
Emergency Stops and Safety Guards
Verify all pull-cord emergency stops are accessible and unobstructed. Confirm all guards and covers are in place. Safety system failures create regulatory violations and liability that dwarf any maintenance cost.
Weekly Checks
Belt Tension Measurement
For screw take-up systems, measure deflection using a tension meter at the midpoint between idlers. Belt sag between carry idlers should not exceed 2–3% of idler spacing. Insufficient tension causes slippage; excess tension overloads bearings and shortens belt life.
Idler Rotation Test
Walk the carry side and physically spin each accessible idler. Every roller should rotate freely with no resistance, wobble, or flat spots. Mark seized rollers for immediate replacement — do not wait for the next scheduled shutdown.
Bearing Lubrication Check
Verify all grease points received lubrication per the OEM schedule. Check for dry bearing noise or heat at critical bearings on drive pulleys and high-load idlers. Apply lubricant at prescribed intervals — over-lubrication attracts debris as damaging as under-lubrication.
Belt Scraper and Cleaner Inspection
Check primary and secondary scraper blade contact pressure and wear. Ineffective scrapers allow carryback that gradually builds on return rollers, causing tracking drift and creating the secondary wear that is usually misdiagnosed as a tracking problem.
Splice Integrity Check
Visually and tactilely inspect mechanical splice fasteners for heads pulling through the belt carcass. Check vulcanized joints for edge lifting or elongation. A deteriorating splice can snap mid-shift without warning, stopping the entire line for hours.
Monthly Deep Inspection
Full Conveyor Frame Alignment Check
Stretch a string line along both sides of the conveyor frame to check for structural straightness. Frame distortion from foundation settling or impact damage causes persistent belt drift that no amount of idler adjustment will correct.
Pulley Lagging Condition Assessment
Inspect drive pulley lagging for wear grooves, glazing, cracking, or delamination. Worn lagging reduces the friction coefficient — causing belt slippage that strains the motor, generates heat, and accelerates belt cover wear simultaneously.
Motor and Gearbox Vibration Analysis
Use a vibration meter on motor and gearbox housings. Vibration analysis catches bearing or alignment faults weeks before they cause failure — motor monitoring posts a 4.78% CAGR specifically because electric drives cause 30–40% of all unexpected conveyor halts.
Gearbox Oil Level and Condition
Check oil level via sight glass. Inspect oil color — cloudy or dark brown indicates contamination or severe oxidation. Change gearbox oil per manufacturer interval. Degraded oil is the primary cause of premature gear tooth and bearing failure in the drive system.
Belt Cover Thickness Measurement
Measure belt cover thickness at multiple points across the width using a calibrated gauge. Replace belt when cover is worn past 75% of original gauge. Tracking this metric monthly builds the trend data needed to schedule belt replacement during planned downtime rather than emergency stops.
Annual Full Overhaul
Complete Belt Performance Assessment
Evaluate overall belt speed, load capacity, energy consumption, and surface condition with the system both loaded and unloaded. Compare performance against commissioning baseline. Plan belt replacement based on wear analysis — not when it breaks.
Full Mechanical and Electrical Inspection
Conduct a complete inspection of all motors, electrical components, control panels, and drive systems. Replace components at or near end of service life rather than waiting for failure during production. Review all past maintenance logs for recurring failure patterns.
Component Replacement Planning
Audit spare parts consumption from the past year. Update critical spares inventory. Plan major belt repairs, pulley re-lagging, or complete belt replacement based on wear analysis. A well-stocked spares kit reduces repair downtime from days to hours.
Your Conveyor Lines Need More Than a Paper Checklist
Oxmaint auto-generates every PM work order above at the correct frequency — daily through annual — and sends mobile alerts before intervals lapse. Every completion is timestamped and photographed. Every missed task is flagged before it becomes a failure.
Industry Impact: What Unplanned Conveyor Downtime Actually Costs
Predictive vs. Preventive: How to Layer Both for Maximum Uptime
The highest-uptime conveyor operations use preventive maintenance as their foundation — structured, scheduled, documented — and layer predictive monitoring on top for the highest-cost failure modes. Oxmaint supports both approaches with a single CMMS platform that connects sensor alerts to automated work orders and tracks every intervention.
Preventive Maintenance
Your Foundation Layer
Scheduled at fixed time or usage intervals
Performed regardless of visible condition
Covers all components systematically
Cost: predictable, budgetable
Best for: belts, lubrication, scrapers, safety checks
Reduces unplanned stops from routine wear by up to 50%
Predictive Monitoring
Your High-Value Layer
Condition-based — acts on real sensor data
15–30 minutes of warning before critical failure
Vibration analysis catches bearing faults weeks early
Cost: higher setup, lower per-event response
Best for: motors, bearings, belt integrity, gearboxes
Reduces residual unplanned stops by further 40% on monitored components
Combined Result
98%+
System uptime achievable with layered PM plus predictive monitoring — matching best-in-class fulfillment center performance
Frequently Asked Questions
What causes conveyor belt mistracking and how do I fix it permanently?
Mistracking has five primary causes: misaligned pulleys or frame structure, misaligned or seized idlers in a localized section, material carryback buildup creating an irregular roller surface, off-center loading at the feed point, and a belt that was not joined squarely at the splice. Temporary idler adjustments treat symptoms — permanent correction requires identifying the specific cause and addressing it structurally. The key is to always start with return run adjustments working upstream, make incremental 1/4-turn idler changes, and wait 3 full belt revolutions before evaluating.
Oxmaint tracks every belt tracking adjustment with timestamps and photos, building the history needed to diagnose and eliminate root causes.
How often should conveyor bearings be lubricated and what lubricant should be used?
Follow the OEM-specified interval, which typically ranges from every 40 operating hours for high-speed or high-load bearings to quarterly for standard carry idlers. Use only the manufacturer-specified lubricant type — wrong viscosity either fails to provide an adequate film or attracts debris that accelerates wear. Apply lubricant at clean, protected grease points. Over-lubrication is as damaging as under-lubrication — excess grease purges past seals, collecting dust and forming an abrasive compound inside the bearing. Mark each lubricated point with a date tag or color code.
Book a demo to see how Oxmaint schedules and records every bearing lubrication event automatically.
How do I know when a conveyor belt needs replacement rather than repair?
Replace the belt when: cover is worn past 75% of original gauge, the carcass — fabric or steel cord — is visible through wear or damage, edge fraying has penetrated more than 10% of the belt width, or splice repair history shows more than two vulcanized repairs on the same section. Track belt cover thickness monthly using a calibrated gauge at multiple points across the width. Trending this data lets you schedule belt replacement during a planned shutdown rather than reacting to a catastrophic failure mid-shift.
Oxmaint logs every belt thickness measurement and automatically flags when replacement thresholds are approaching.
What is the most cost-effective conveyor maintenance improvement for a plant with limited resources?
Start with a daily auditory walk-through of every active conveyor line. The combination of listening for seized rollers, watching belt tracking, and noting material spillage takes 15–20 minutes and prevents the three failure modes — roller seizure, belt mistracking, and splice failure — that together account for the majority of unplanned stops. This single practice, consistently documented and actioned, delivers measurable downtime reduction within 30 days at near-zero cost. The next highest-return investment is standardizing your lubrication schedule in a CMMS so intervals are never missed.
Start tracking conveyor PM free with Oxmaint — set up in 15 minutes, no credit card required.
How does predictive maintenance for conveyors differ from standard preventive maintenance?
Preventive maintenance operates on fixed schedules — you service the equipment at defined intervals regardless of its current condition. Predictive maintenance uses real-time data from vibration sensors, temperature monitors, and current meters to flag specific components approaching failure — typically providing 15–30 minutes of advance warning before critical failure. Predictive systems are particularly valuable for motors and bearings, where vibration analysis detects faults weeks early. The most effective programs use preventive maintenance as the foundation for routine components and predictive monitoring for high-cost failure modes like drives and gearboxes.
Oxmaint connects sensor-generated alerts directly to PM work orders so predictions translate into scheduled actions automatically.
Material Handling Reliability Starts Here
Every Conveyor Line Deserves a Maintenance Program That Never Sleeps
Oxmaint turns your conveyor maintenance from memory-based spot checks into a structured, automated PM program — auto-scheduling inspections, capturing digital completion records, and surfacing failure patterns before they become shutdowns. Build the uptime your operation depends on.