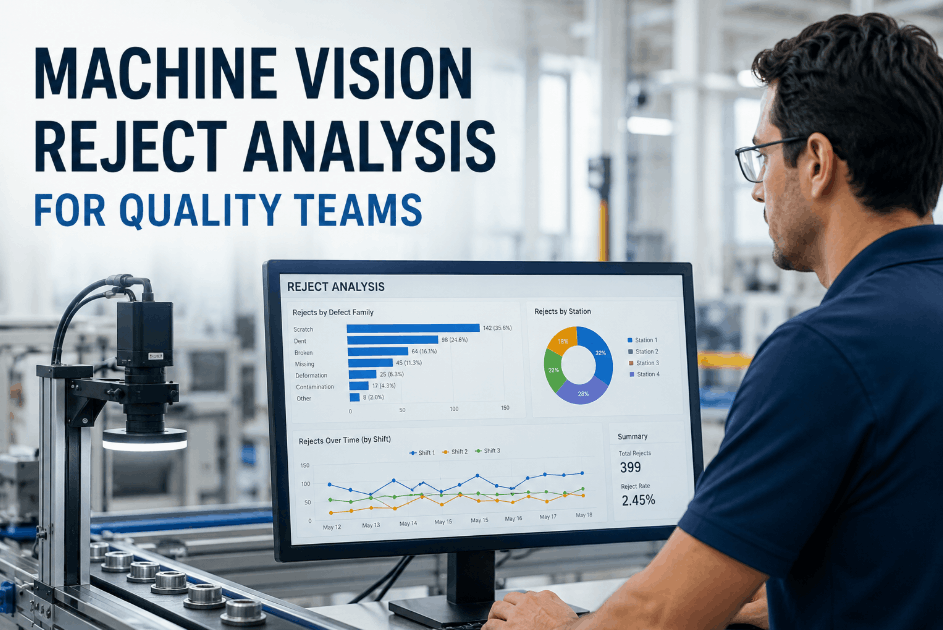
Machine vision systems generate reject signals at speed — but the data behind each rejection is only useful if quality teams can break it down by defect family, inspection station, and shift. Without structured reject analysis, a spike in rejections looks the same whether it comes from a miscalibrated camera, a worn tooling insert, or a process temperature drift. Sign Up Free to connect your inspection records to Oxmaint and start separating camera-driven false rejects from genuine process escapes. Oxmaint AI links machine vision reject events to maintenance work orders and equipment records — giving quality teams the classification layer needed to act on reject data rather than just accumulate it. Book a Demo to see how defect family mapping flows from vision system outputs into Oxmaint quality dashboards.
Turn Reject Signals into Actionable Quality Intelligence
Oxmaint AI classifies machine vision rejects by defect family, station, and shift — giving quality teams the data to separate camera faults from process variation and close quality loops faster.
Why Machine Vision Reject Data Stays Unanalyzed in Most Quality Operations
Gap #1
No Defect Family Classification
Rejects are counted but not categorized — surface scratches, dimensional deviations, and color mismatches all appear as a single reject total, hiding which defect class is actually driving the rate.
Gap #2
Camera vs Process Not Distinguished
False rejects from lighting drift, lens contamination, or calibration shift get mixed with real process escapes — inflating reject rates and sending quality teams chasing process changes that don't exist.
Gap #3
Station-Level Patterns Invisible
Reject data is aggregated at line level rather than per inspection station — masking whether one camera or fixture is responsible for the majority of events while others perform correctly.
Gap #4
Shift Variation Unreported
Reject rates that change between shifts indicate operator, setup, or changeover issues — but without shift-segmented reporting, this pattern goes undetected and the root cause remains unaddressed.
Gap #5
No Link to Maintenance Records
Vision system reject spikes often follow equipment maintenance events — but without a link between inspection data and work order records, quality teams cannot correlate reject increases to recent maintenance activity.
Gap #6
Trend Analysis Requires Manual Export
Reject trend analysis depends on manual data exports from vision controllers into spreadsheets — creating reporting lag and preventing real-time quality response during active production runs.
How Oxmaint AI Structures Machine Vision Reject Analysis
01
Reject Event Capture
Vision system reject events are logged in Oxmaint with station ID, defect type, part reference, and timestamp — creating a structured inspection record for every rejection event across the production line.
→
02
Defect Family Mapping
Reject events are classified into defect families — surface, dimensional, assembly, cosmetic — enabling quality teams to track defect mix trends separately from overall reject volume.
→
03
Station and Shift Segmentation
Oxmaint segments reject data by inspection station and production shift — surfacing which stations generate concentrated reject events and whether rate patterns correlate with specific shift crews or changeover sequences.
→
04
Camera vs Process Separation
By linking reject spikes to maintenance and calibration records, Oxmaint helps quality teams identify camera-attributable false reject patterns versus reject increases driven by genuine process variation.
What Oxmaint Captures Per Vision Reject Analysis Record
Defect Classification
Reject event classified by defect family per occurrence
Defect mix tracked as percentage of total rejects over time
New defect families flagged when classification thresholds exceeded
Station Analysis
Reject rate calculated per inspection station per production run
Station-level reject trends compared across time periods
Camera maintenance events linked to station reject rate changes
Shift Reporting
Reject rates segmented by shift for direct comparison
Shift-specific defect patterns surfaced automatically
Changeover and setup events correlated with post-event reject spikes
Quality Outcome
Camera fault vs process variation separated with data evidence
Quality team response targeted to actual reject root cause
Inspection system calibration schedule informed by reject pattern data
38%
Of machine vision rejects in high-volume lines are attributable to camera calibration drift rather than genuine process defects
3.1×
Faster root cause identification when reject data is segmented by station, shift, and defect family simultaneously
48hrs
Typical Oxmaint deployment time before structured reject analysis begins capturing classified inspection data
90days
Average period to establish statistically reliable defect family baseline after Oxmaint quality tracking deployment
Oxmaint AI vs Standard CMMS for Vision Reject Visibility
Standard CMMS — Limited Reject Insight
Reject counts recorded without defect family classification or pattern context
Camera calibration and maintenance events stored separately from inspection reject data
No station-level segmentation — reject totals mask which inspection point is underperforming
Shift variation in reject rates requires manual comparison across exported spreadsheets
False reject identification depends on operator judgment rather than structured data comparison
Quality team response to reject spikes delayed by manual data assembly and reporting lag
Oxmaint AI — Structured Reject Intelligence
Every reject classified by defect family — surface, dimensional, assembly, cosmetic — automatically — Sign Up Free
Camera maintenance and calibration events linked to station reject rate changes in real time
Station-level reject rates calculated per run — high-contributing stations identified immediately
Shift-segmented reject reporting surfaces operator and setup pattern differences automatically
Camera vs process separation supported by maintenance record correlation — Book a Demo
Live quality dashboards give teams real-time visibility without manual data extraction
6 KPIs to Measure Machine Vision Reject Analysis Quality
These KPIs give quality teams the metrics to distinguish camera performance from process variation, identify high-contributing inspection stations, and build reject analysis that supports faster corrective action. Book a Demo to see how Oxmaint tracks all six from linked inspection and maintenance records.
KPI 01
Defect Family Reject Rate
Reject volume broken down by defect classification — surface, dimensional, assembly, cosmetic — tracked as a percentage of total rejects over time to identify which defect type is trending upward.
Defect Classification
KPI 02
Station Reject Concentration
Percentage of total line rejects generated per inspection station. High station concentration indicates a localized camera, fixture, or process issue rather than a line-wide quality problem.
Station Analysis
KPI 03
Shift Reject Variance
Difference in reject rate between production shifts for equivalent products and stations. Persistent shift variance signals a setup, operator, or changeover practice issue rather than an equipment or process problem.
Shift Analysis
KPI 04
False Reject Identification Rate
Percentage of total rejects confirmed as false positives — items rejected by the vision system that pass manual quality inspection. Tracks camera calibration performance and inspection threshold accuracy over time.
Camera Performance
KPI 05
Post-Maintenance Reject Spike Rate
Frequency of reject rate increases observed in the period immediately following camera or fixture maintenance events. Identifies maintenance activities that introduce calibration variation or alignment errors.
Maintenance Correlation
KPI 06
Reject Trend Response Time
Average time from a statistically significant reject rate increase to a confirmed quality team corrective action. Measures how quickly reject analysis data translates into production intervention and root cause resolution.
Response Speed
Industries Using Oxmaint for Machine Vision Quality Analysis
Automotive Assembly
Station-Level Reject Tracking on Body and Trim Lines
Automotive plants use Oxmaint to track vision reject data by station and defect family across body panel, trim, and powertrain assembly lines — separating fixture-related reject spikes from genuine weld and fit defects that require process intervention. Sign Up Free for your plant.
Electronics Manufacturing
PCB Inspection Reject Analysis by Defect Class
Electronics manufacturers use Oxmaint to classify AOI and 3D SPI reject events by defect family — tracking solder, component placement, and pad exposure defects separately to distinguish paste printer variation from pick-and-place process drift. Book a Demo for your SMT line.
Food and Beverage
Label and Fill Inspection Reject Segmentation
F&B producers track vision reject events on packaging, label placement, and fill level inspection stations through Oxmaint — identifying whether reject spikes originate from vision system sensitivity drift or actual packaging process variation requiring line intervention.
Pharmaceutical
Compliance-Critical Reject Classification for Regulated Lines
Pharmaceutical manufacturers use Oxmaint to maintain structured reject classification records for vision inspection events on tablet, capsule, and blister pack lines — supporting GMP documentation requirements and providing the audit-ready defect family data needed for quality system reviews.
Your Vision System Rejects Fast. Does Your Analysis Keep Up?
Oxmaint AI classifies machine vision reject events by defect family, inspection station, and shift — giving quality teams the structured data to separate camera issues from process issues and respond to reject trends before they become escapes. Book a Demo to see reject analysis applied to your inspection workflow.
Frequently Asked Questions
What is defect family classification in machine vision reject analysis?
Defect family classification groups vision rejects into categories — surface, dimensional, assembly, cosmetic — so quality teams can track each defect type separately rather than treating all rejects as a single undifferentiated count.
How does Oxmaint separate camera issues from process defects?
Oxmaint links reject rate changes to camera maintenance and calibration records — identifying spikes that coincide with maintenance events as likely camera-attributable rather than process-driven, directing quality response to the correct root cause.
Can Oxmaint track reject rates by production shift?
Yes. Oxmaint segments reject data by shift automatically — surfacing rate differences between crews, identifying setup or changeover practices that contribute to elevated rejects on specific shifts.
How quickly can Oxmaint begin capturing structured vision reject data?
Oxmaint typically deploys within 48 hours. Structured reject classification and station-level reporting begin capturing data immediately after deployment, with statistically meaningful baseline trends available within 90 days.
Does Oxmaint support vision reject tracking across multiple production lines?
Yes. Oxmaint aggregates reject data across all lines and inspection stations in a single dashboard — enabling quality managers to compare defect family trends, station performance, and shift variation across the entire production operation.
Stop Treating All Rejects the Same.
Oxmaint AI gives quality teams the defect family, station, and shift segmentation needed to separate camera faults from process variation — and close quality loops with evidence, not guesswork.