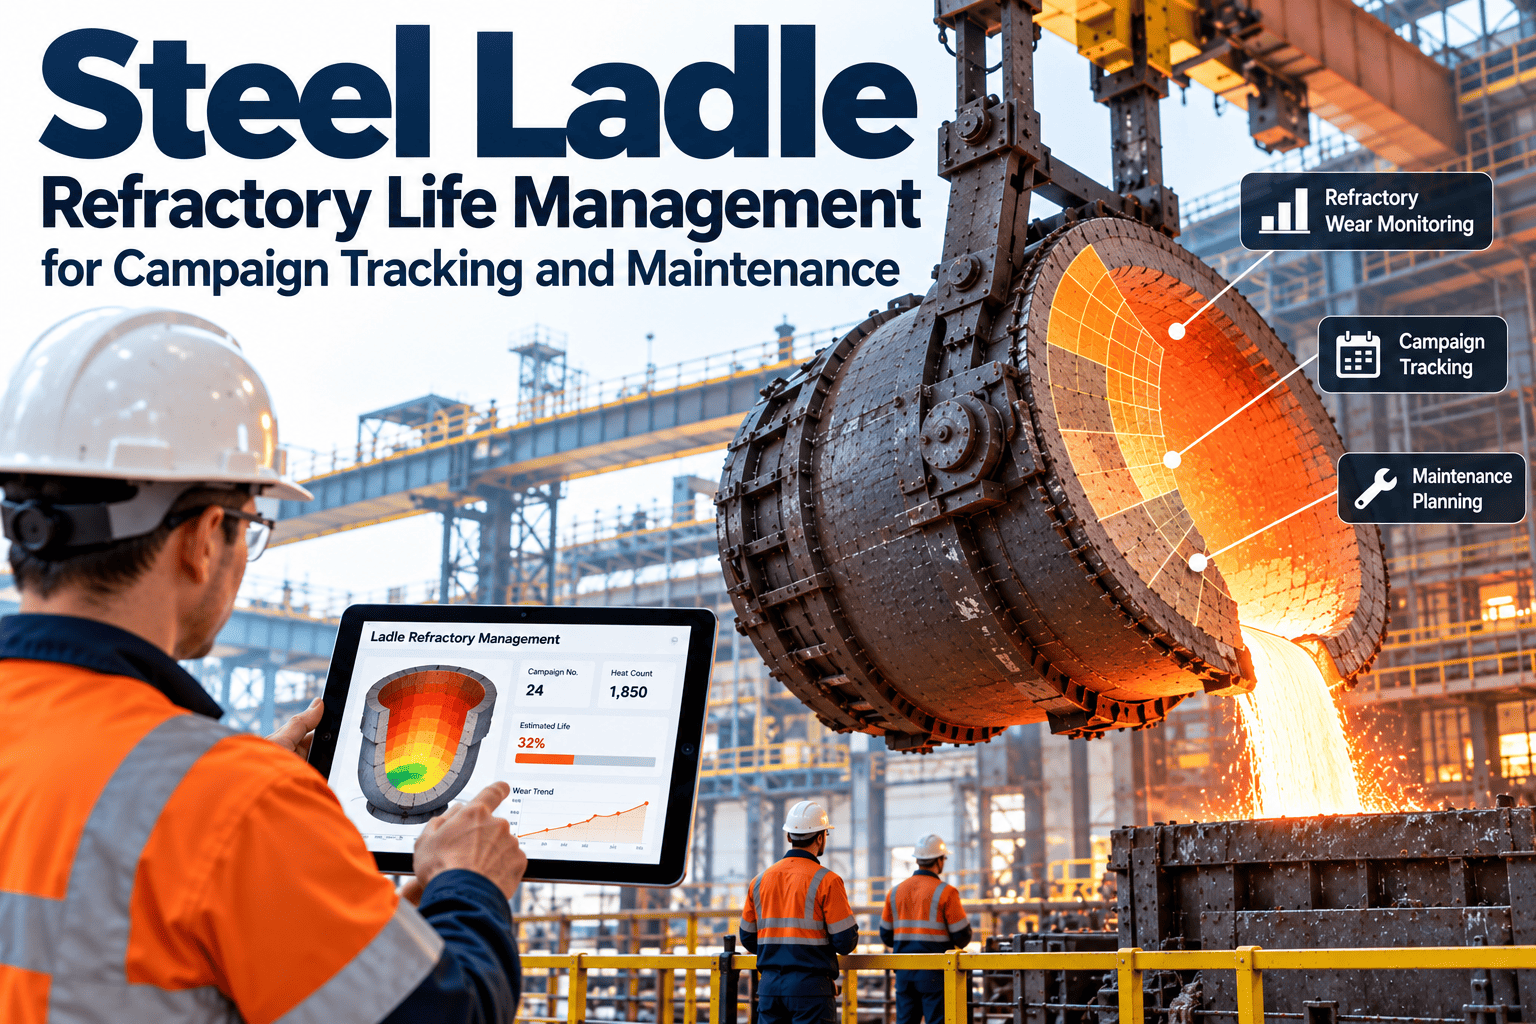
A steel ladle is not one refractory lining wearing down at one rate — it is a stack of zones, each eroding for a different reason and on a different schedule, which is exactly why a whiteboard with a single heat count next to each ladle number tends to get the reline decision wrong in both directions. Track the vessel as one number and the plant either pulls a ladle for reline while its barrel and bottom still have a third of their life left, or runs the fastest-wearing zone past a safe margin because nobody was watching it specifically. Campaign tracking that separates slag line, impact pad, barrel and well block wear is what turns refractory spend from a recurring surprise into a scheduled, budgeted line item — something a CMMS built for steel plants can carry automatically once heat counts and inspection data are tied to the ladle asset record.
Your ladle has four wear clocks running at once
Slag line brick, impact pad, barrel lining and well block all wear at different rates for different reasons — yet most plants still track a ladle campaign as a single heat count. Zone-level tracking is what lets a reline get scheduled instead of discovered.
Why one heat counter hides the real story
A ladle campaign is usually reported as a single figure — heats since last reline — measured against a vendor-recommended campaign length. That number is useful for scheduling a demo crew, but it says nothing about which zone is actually approaching its limit.
The slag line, in direct contact with corrosive slag chemistry, typically erodes several times faster than the barrel lining under molten steel contact. When only the vessel-level count is tracked, the reline decision gets made when the fastest zone becomes visibly thin — often on a shop-floor visual call rather than a measured trigger — while the slower zones are discarded with real life still in them.
The cost of that pattern compounds across a fleet. A melt shop running twenty or more ladles that all default to a full reline whenever the slag line hits its limit is effectively paying full refractory replacement cost every time, rather than the lower cost of a targeted slag-line gunning or patch. Multiplied across a full year of campaigns, the gap between "reline everything when the fastest zone fails" and "repair the fast zone, keep the slow zones running" is one of the larger controllable line items in a melt shop's consumables budget.
The four wear zones and what drives each one
Fastest-wearing, campaign-limiting zone
Magnesia-carbon brick in direct contact with corrosive slag. This zone almost always reaches its minimum thickness before any other, and is frequently gunned or repaired mid-campaign to extend the barrel's life without a full reline.
Erosion from tap stream energy
Absorbs the kinetic energy of the molten steel stream during tapping. High-alumina or MgO-C brick is typically specified thicker here to withstand repeated mechanical impact rather than chemical attack.
Slowest-wearing structural zone
High-alumina brick or alumina-magnesia castable handling sustained temperatures above typical tapping heat. Erosion per heat is a fraction of the slag line's rate, which is exactly why tracking it separately protects real remaining life.
Short-life consumable, safety-critical
Governs flow control at the bottom of the ladle and must be replaced on its own, much shorter cycle — running it past its limit is a direct path to a bottom breakout risk.
Matching replacement cycles to each zone
Because each zone wears at a different rate, each one needs its own tracked cycle rather than being bundled into the vessel's overall campaign figure.
| Zone | Primary Wear Mechanism | Typical Replacement Trigger | Consequence If Untracked |
|---|---|---|---|
| Slag line | Chemical erosion from slag contact | Measured thickness against minimum safe margin | Runs to visual failure; drives whole-vessel reline early |
| Impact pad | Mechanical erosion from tap stream | Periodic thickness check tied to heat count | Localized thin spot missed until inspection |
| Barrel / sidewall | Thermal cycling, slow chemical attack | Thickness survey at defined campaign milestones | Life discarded early when reline is triggered by slag line alone |
| Well block / slide gate | Flow erosion, thermal shock at pour | Fixed-cycle replacement independent of vessel campaign | Bottom breakout risk if run past design life |
| Porous / stir plugs | Gas flow erosion, thermal shock | Usage-count replacement, shortest cycle in the ladle | Loss of stirring control, argon plug failure risk |
Measuring wear: modeled estimate versus physical check
Zone-level tracking works on two complementary inputs, and programs that lean on only one of them tend to drift over time.
Erosion rate applied per heat
A per-zone erosion rate, calibrated against historical teardown findings, is applied automatically as each heat completes. This gives a continuously updated remaining-life figure without needing a physical measurement after every cast.
Physical confirmation at intervals
Non-destructive thickness measurement taken at defined heat-count checkpoints confirms or corrects the modeled estimate, catching cases where an unusually aggressive slag chemistry or extended holding time accelerated wear faster than the model assumed.
Catches what instruments miss
Cracking, localized spalling and joint separation are often easier to spot by eye than by thickness reading alone, which is why a scheduled visual pass remains part of the discipline even in a fully instrumented program.
Shell temperature as an early flag
A rising shell temperature at a specific point on the ladle exterior can indicate the working lining has thinned enough that heat is reaching the steel shell faster than normal — a useful cross-check between scheduled ultrasonic surveys.
Relying on the model alone eventually drifts from reality, since no erosion-rate formula perfectly captures every grade and slag chemistry a ladle actually sees. Relying on physical checks alone means the plant only learns about a problem at the next scheduled inspection, which may be heats too late for a zone that wore faster than expected. Running both together — model for the day-to-day estimate, physical checks for periodic ground truth — is what keeps the reline schedule both proactive and accurate, and gives the refractory supplier and internal planners a shared, defensible number to schedule against rather than two competing opinions about how much life is really left.
From heat count to a reline decision
Turning zone-level wear data into a scheduled reline rather than an emergency one is a workflow, not just a measurement habit.
Cast cycle completion auto-increments the ladle's heat counter per zone
Zone-specific erosion rate applied against measured or modeled thickness
Ultrasonic or visual check at defined heat-count intervals verifies the estimate
Work order and refractory material staged for a planned outage window, not a floor emergency
Rotating the fleet to even out wear
A melt shop rarely runs one ladle — it runs a fleet, and the same zone-level data that schedules a single reline also drives fleet rotation so that ladles do not all approach their limit in the same week.
Without per-zone visibility, rotation decisions default to "next available ladle," which tends to load wear unevenly and forces multiple ladles into reline within the same week — exactly the scheduling collision that turns a planned outage into a production bottleneck.
The scheduling collision is worse than it first sounds, because a melt shop rarely has spare reline capacity sitting idle for the weeks it does not need it. When three or four ladles all cross their slag-line limit in the same window, the refractory crew either works overtime to clear the backlog or the shop runs short on available ladles mid-week, which cascades into delayed taps and idle furnace time elsewhere in the plant. Spreading that same wear evenly across the fleet, using the zone data the plant already has, turns an unpredictable pile-up into a steady, budgetable cadence of relines.
Stop discarding barrel life to save a slag-line brick
Track every ladle zone independently and let the reline schedule follow measured wear instead of a whiteboard heat count.
Where the porous plug and slide gate fit into the picture
It is easy for a campaign tracking conversation to focus entirely on brick and castable, since those are the largest cost items in a reline. But the shortest-life components in a ladle are the porous plugs and the slide gate well block, and they carry outsized safety consequences relative to their replacement cost.
A porous plug that has exceeded its usage life does not fail gracefully — it loses gas permeability unevenly, which degrades stirring control exactly when a heat needs it most for temperature and composition homogenization. A worn slide gate well block raises the risk of an uncontrolled flow event during tapping. Both components are inexpensive relative to a full reline, which is precisely why tracking their usage independently, rather than assuming they will get replaced "at the next reline," closes one of the more preventable gaps in ladle safety.
Before and after zone-level tracking
- One heat count per ladle, checked against a vendor average
- Reline timing decided by visual inspection at the slag line only
- Well block and porous plug life tracked informally, if at all
- Fleet rotation based on which ladle is next available, not remaining life
- Emergency relines cluster unpredictably across the fleet
- Slag line, impact pad, barrel and well block each carry their own wear count
- Ultrasonic thickness checks confirm the modeled estimate at set intervals
- Porous plugs and slide gates replaced on their own short cycle, tracked as sub-components
- Fleet rotation routes aggressive-slag heats away from ladles nearing their slag-line limit
- Relines land in planned outage windows with material staged in advance
KPIs that show campaign tracking is paying off
A handful of metrics separate a program that is genuinely extending campaign life from one that has simply added more spreadsheets to the same reline decisions.
| Metric | What Good Looks Like |
|---|---|
| Average heats per full campaign, fleet-wide | Trending upward as zone-level gunning replaces early full relines |
| Emergency relines versus planned relines | Emergency events falling as a share of total relines each quarter |
| Refractory cost per heat | Declining as barrel and bottom life is fully consumed instead of discarded early |
| Ladles reaching slag-line limit within the same week | Spread out over time rather than clustering, reflecting effective fleet rotation |
| Well block and porous plug near-miss count | Falling toward zero as sub-component cycles are tracked independently of the vessel campaign |
What a CMMS needs to support campaign tracking
Oxmaint tracks each ladle as a multi-zone asset rather than a single heat counter, logging slag line, impact pad, barrel and well block wear independently, cross-checking modeled erosion against ultrasonic readings, and auto-generating the reline work order with the right refractory materials staged before the vessel actually needs it.
Frequently Asked Questions
Why does the slag line usually limit ladle campaign life instead of the barrel?
The slag line sits in direct contact with corrosive slag chemistry, which erodes magnesia-carbon brick far faster than the thermal cycling the barrel lining experiences under molten steel alone.
Can a ladle be relined in one zone without a full reline?
Yes — gunning or patching the slag line mid-campaign is common practice to extend the barrel and bottom's usable life without discarding refractory that still has margin left.
How often should well blocks and porous plugs be checked?
These components run on a much shorter cycle than the vessel lining and should be tracked on their own usage count, since running either past its design life raises direct breakout and flow-control risk.
Does Oxmaint support tracking multiple ladles as a rotating fleet?
Yes — heat counts, zone wear and grade history are tracked per ladle so casts can be routed to the vessel with the most remaining life for that grade. Book a Demo to see fleet rotation configured for your melt shop.
What happens if zone wear is only estimated and never physically checked?
A modeled estimate without periodic ultrasonic or visual confirmation drifts from reality over a campaign, which is why inspection checkpoints at set heat-count intervals remain part of the tracking discipline even with automated counters.
Track every zone, schedule every reline, stop guessing
Move your ladle fleet from a single heat count to zone-level campaign tracking with Oxmaint.
Free trial available · No credit card required