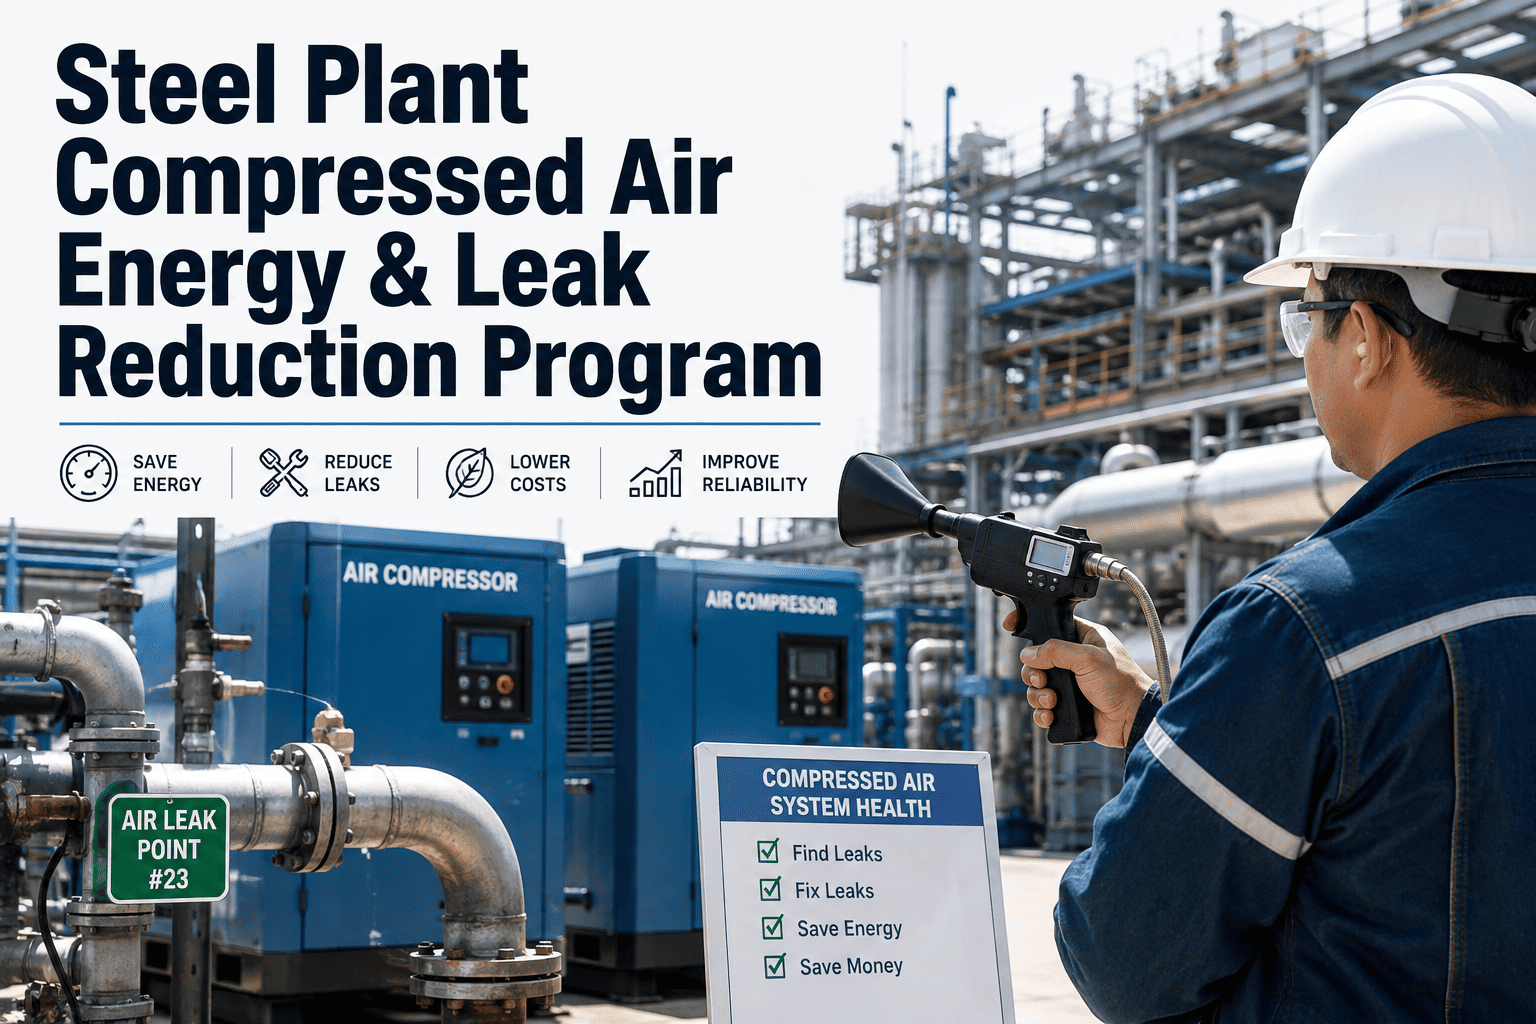
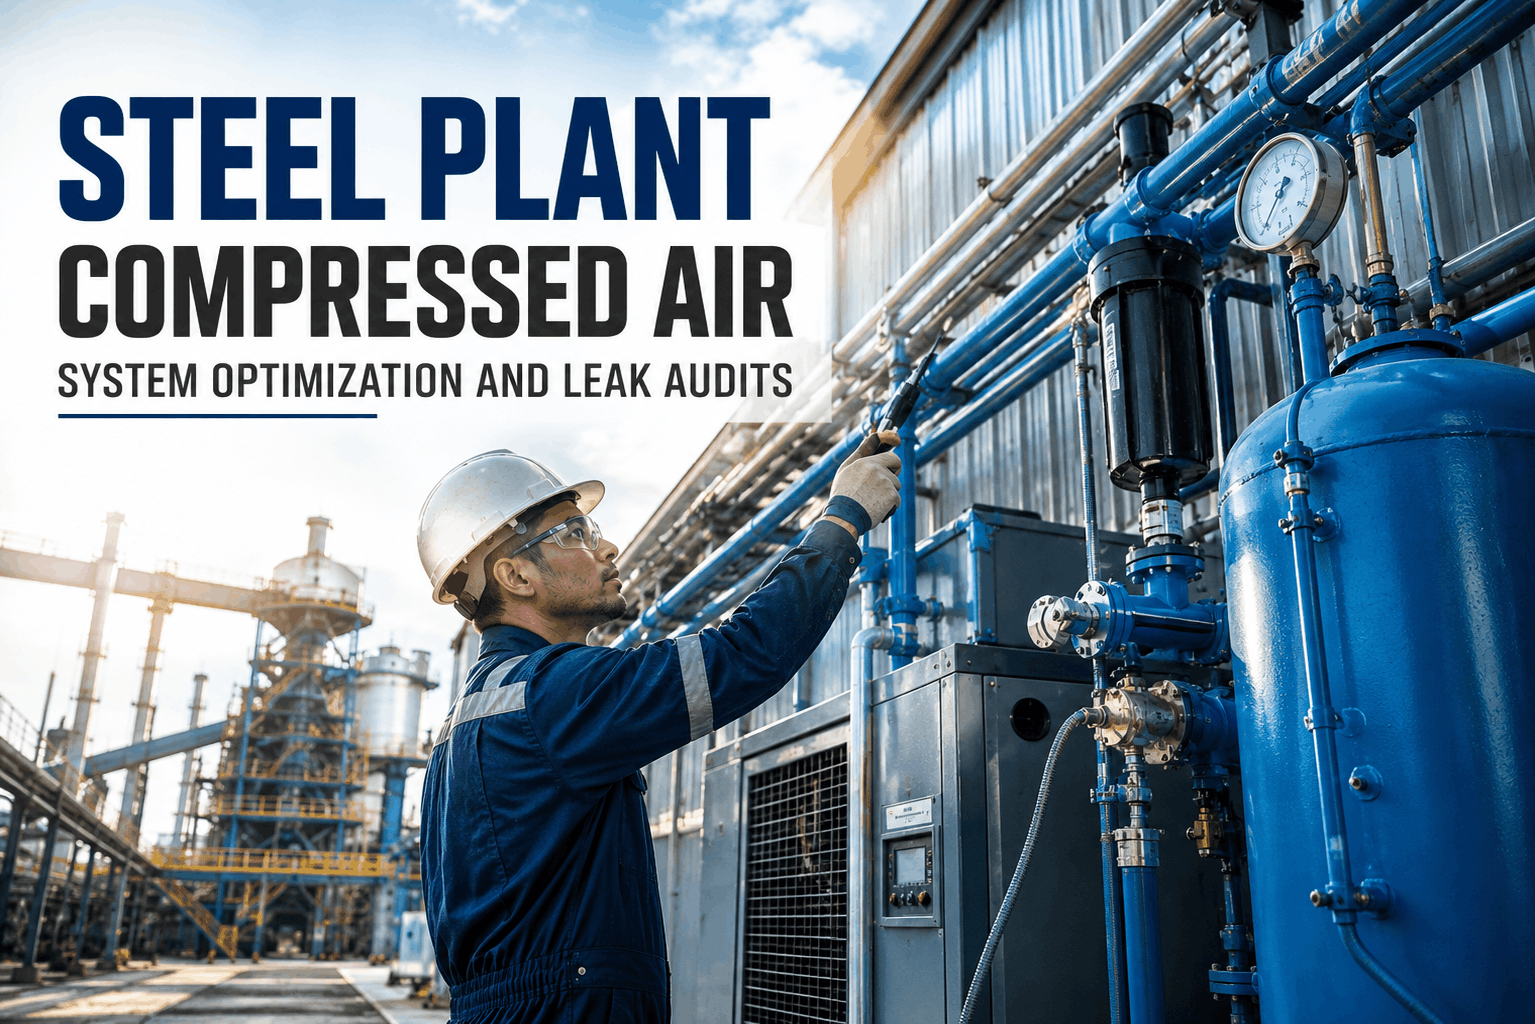
Compressed air is called the fourth utility for a reason — steel plants pay to generate it, pay again when it leaks, and rarely measure either cost. A single quarter-inch leak at header pressure can waste enough air daily to cost thousands of dollars a year, and most mills have dozens of them hissing quietly behind panels, hose reels, and quick-disconnects nobody has walked past with a listening device in months. Descaling headers, EAF door actuators, pickling line dampers, and cut-to-length pneumatic clamps all depend on stable header pressure, so every leak is also a production-risk problem, not just a utility bill problem. Start a free trial of Oxmaint to turn leak surveys and compressor PM into a tracked, dollar-quantified maintenance program.
COMPRESSED AIR ENERGY · LEAK DETECTION · COMPRESSOR PM · CMMS SAVINGS TRACKING
Find the Leaks. Track the Savings. Prove the ROI.
Run a CMMS-based compressed air leak and energy program built for steel plant header pressures, compressor rooms, and pneumatic-heavy process lines — and turn every repaired leak into a documented dollar figure.
20–30%Of compressor output typically lost to leaks in an unmanaged system
10–15%Overall efficiency of a typical compressed air system, most energy lost as heat
76%Share of a compressed air system's lifecycle cost that comes from electricity alone
$1,200+Annual cost of a single 1/8-inch leak left unrepaired at typical header pressure
Why Compressed Air Waste Hits Steel Plants Harder
Most plants treat compressed air as a background utility until a caster spray header loses pressure or a descaling nozzle stops clearing scale mid-pass. Steel plants run compressed air through some of the harshest conditions in any industrial facility — vibration near shakers and screens loosens fittings, radiant heat near casters and furnaces degrades hose and seals faster than in a normal machine shop, and long header runs across a mill footprint create dozens of joints that can work loose over a single campaign. Studies of hundreds of industrial sites have found that only about half of all compressed air produced in a typical plant is actually used productively, with the rest lost to leaks, artificial demand, and inefficient end uses. In a steel mill, that waste is compounding — you're paying compressor electricity twice: once for the air you use, and once for the air that never reaches the tool, cylinder, or nozzle it was meant for.
Where Steel Plants Typically Lose Compressed Air
01
Quick Disconnects & Hose Fittings
High-frequency connect points near cut-to-length lines and portable tools; seals wear from repeated coupling cycles.
02
FRL Units & Solenoid Valves
Filter-regulator-lubricator assemblies on EAF door and damper actuators degrade from heat cycling and contamination.
03
Header Joints Near Vibration Sources
Threaded and flanged joints along runs near shakers, screens, and roll tables loosen gradually and go undetected without an ultrasonic survey.
04
Flexible Hose Near Heat Sources
Hose runs near casters, furnaces, and ladle stations degrade faster than rated life, developing pinhole leaks under jacket wear.
A plant that has gone without regular leak maintenance will typically run a leak rate equal to around 20% of total compressor output, while proactive detection and repair can bring that down below 10%.
The True Cost of a Leak Nobody Fixed
Leak cost scales fast with orifice size, and most maintenance teams underestimate it because a hiss sounds small next to a breakdown. A quarter-inch leak at 100 PSI can waste on the order of 100 CFM continuously, which works out to roughly $36 a day in energy cost alone — and that is one leak, on one header, in one part of the plant. The table below shows how quickly small openings compound into real annual spend.
| Leak Opening Size | Approx. Air Lost | Estimated Annual Cost | Typical Steel Plant Location |
|---|
| 1/16 inch | ~6 CFM | $300 – $450 | Instrument air tubing, small solenoids |
| 1/8 inch | ~25 CFM | $1,200 – $1,800 | FRL units, quick-disconnect couplers |
| 3/16 inch | ~55 CFM | $2,000 – $2,800 | Header joints, flexible hose fittings |
| 1/4 inch | ~100 CFM | $2,500 – $3,600 | Cylinder seals, damper actuator lines |
Multiply even a conservative mix of these across a plant-wide header network and unrepaired leaks routinely account for tens of thousands of dollars a year in a mid-sized mill — money that never shows up on a single line item, because it is spread invisibly across the electric bill.
Put a Number on Every Leak You Fix
Log leak tags, repair work orders, and CFM-to-dollar estimates in one place so your energy savings are provable, not anecdotal.
Building a Leak Detection & Repair Program That Actually Runs
A one-time leak hunt finds problems; a program prevents them from coming back. The best-performing plants treat leak detection as a recurring maintenance route, not a special project, and tag every leak with an ID, location, and estimated cost the moment it's found.
1
Run a Baseline Ultrasonic SurveyWalk every header, drop, and pneumatic device with an ultrasonic detector during a low-noise window and tag each leak found with location and estimated flow.
2
Rank Leaks by Cost, Not Just SizeConvert tagged leaks into estimated annual dollar cost so repair priority follows the biggest financial impact first, not just accessibility.
3
Assign and Track Repair Work OrdersConvert every tagged leak into a CMMS work order with parts, labor, and a target completion date instead of a note on a clipboard.
4
Re-Survey on a Fixed IntervalRe-walk the same routes quarterly. Leak rate should trend down over time — if it climbs back up, it flags a maintenance or vibration issue upstream.
Compressor Room Maintenance: The Other Half of the Savings
Fixing leaks recovers wasted air; maintaining the compressor room recovers wasted generation. Dirty intake filters, saturated dryers, and stuck condensate drains all force compressors to work harder for the same delivered air, and most of that loss never gets diagnosed because pressure at the gauge still looks normal.
Intake & Line Filters
Clogged filters increase pressure drop and force the compressor to work harder per CFM delivered. Replace on a scheduled interval, not just on visible fouling.
Dryers & Condensate Drains
A stuck-open solenoid drain can leak air continuously around the clock. Test drain cycling on every PM round — this is one of the most overlooked leak sources in a compressor room.
System Pressure Setpoint
Every extra 2 PSI of header pressure adds roughly 1% to compressor energy draw. Right-sizing pressure to actual process need is one of the fastest paybacks available.
Belt, Bearing & Vibration Checks
Standard rotating-equipment PM on the compressor package itself — belts, bearings, and vibration trending — prevents efficiency drift long before failure.
Frequently Asked Questions
How much can a steel plant realistically save from a leak program?
Most plants without an active leak program run leak rates of 20–30% of compressor output, and structured survey-and-repair work typically brings that under 10%. On a plant running multiple large compressors, that gap is routinely worth tens of thousands of dollars a year.
Book a demo to see how the savings get tracked automatically.
How often should a leak survey be repeated?
Quarterly is a common cadence for high-vibration areas like caster and roll table zones, with a full plant-wide survey at least twice a year. Areas near heat sources or heavy vibration may justify a tighter interval.
What's the fastest way to estimate leak cost without a full audit?
Orifice-size-to-CFM tables combined with your local electricity rate give a workable estimate for prioritization.
Oxmaint can log tagged leaks with estimated CFM and auto-calculate annual dollar impact per leak.
Does lowering header pressure actually save meaningful energy?
Yes — small pressure reductions compound because compressor energy draw scales with discharge pressure. Right-sizing pressure to the actual minimum needed by the most pressure-sensitive process is often the single fastest payback in a compressed air program.
Can leak detection and compressor PM run in the same CMMS program?
Yes — leak tags, repair work orders, and compressor room PM should live in one system so leak rate and compressor efficiency can be tracked together instead of as separate initiatives with no shared history.
Stop Paying to Generate Air That Never Does Work
Tag leaks, assign repairs, track compressor PM, and turn every fixed leak into a documented dollar figure — all inside one CMMS built for plant maintenance teams.