Energy loss in a steel plant seldom announces itself. It hides in a compressed-air leak that has hissed for months, a motor running at a fraction of its rated load, a cooling pump throttled by a half-closed valve or a conveyor that runs empty through the night. Each loss looks small, yet together they push up energy per tonne. A repeatable checklist makes the search systematic, and steel plant maintenance software turns each finding into a tracked repair rather than a forgotten note.
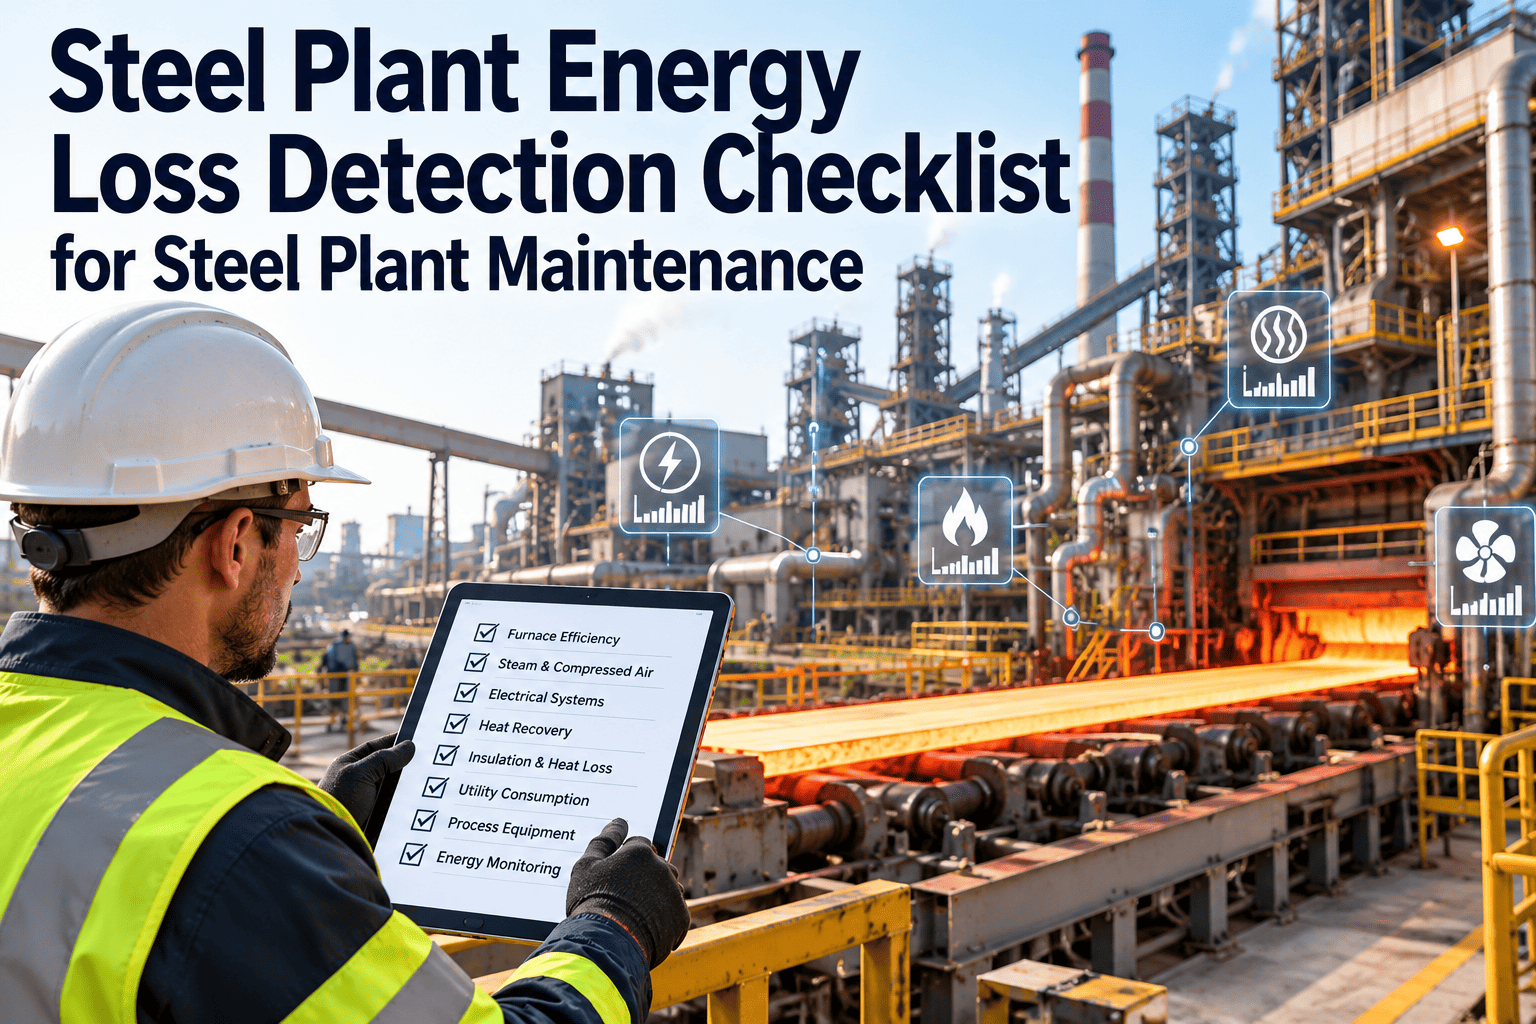
Steel Plant Energy Loss Detection Checklist for Maintenance Teams
Investigate compressed-air leaks, inefficient motors, cooling losses, idle equipment and abnormal energy use with a digital checklist that links every loss to a work order.
Illustrative loss map. Bar length shows relative focus areas, not measured values.
Why Maintenance Owns Part of the Energy Problem
Many energy losses are maintenance conditions, not process choices. Worn seals, fouled exchangers and misaligned drives all consume extra power.
Reactive energy habits
- Energy reviewed only when the bill arrives
- Leaks fixed when they become loud
- Idle equipment left running for convenience
- No link between meter data and asset condition
Maintenance-led detection
- Routine walkdowns find losses early
- Every leak is tagged and ticketed
- Idle rules checked on each round
- Energy trends reviewed beside work history
Investigation Flow: From Signal to Fix
Follow the same path every time, so findings are comparable and nothing stops at the observation stage.
Compressed-Air Leak Checklist
Compressed air is costly to produce, so leaks and misuse waste a lot of electricity relative to the work delivered.
- Scan pipework, couplings, drains, hoses, regulators and cylinders with an ultrasonic leak detector at a set interval.
- Tag every leak at its location with a number, and record size, location and likely cause in the maintenance system.
- Check automatic drains for stuck-open valves, which can leak continuously and are easy to miss.
- Confirm system pressure is no higher than the lowest practical requirement, since higher pressure raises both leakage and compressor load.
- Look for open-ended blowing, air guns used for cleaning and air-driven tools running while idle.
- Verify compressor loading, unloading and sequencing, and check that no machine runs unloaded for long periods.
- Inspect filters and dryers for high pressure drop that forces the system to run at a higher setpoint.
- Check air demand during a non-production period, and investigate any consumption that should be zero.
Motor and Drive Efficiency Checklist
Motors drive fans, pumps, conveyors and mills, so small efficiency gaps repeat across hundreds of machines.
- Compare measured motor current with nameplate current to spot oversized motors running at light load.
- Check fans and pumps that use throttling dampers or valves, and note candidates for variable speed drives.
- Inspect belts for slip and incorrect tension, and check pulley wear that wastes drive power.
- Verify coupling alignment and bearing condition, because friction and misalignment raise absorbed power.
- Look for motors that are hot, noisy or drawing unbalanced phase current, which may signal winding or supply issues.
- Confirm cooling air paths on motors are clear of dust and scale so they do not run hotter than needed.
- Review rewound or repaired motors and record whether efficiency was maintained or lost.
- List motors with long run hours and low load factor as candidates for replacement or right-sizing.
Never Lose a Tagged Leak Again
Log each loss against its asset, assign an owner and track it until the repair is confirmed.
Cooling System Loss Checklist
Cooling circuits use pumps, fans and heat exchangers continuously, so fouling and over-supply carry a steady energy penalty.
- Compare cooling water flow and temperature rise with design values for each circuit.
- Check for throttled valves and bypass lines left open, which waste pump energy.
- Inspect heat exchangers and spray nozzles for scale and blockage that force higher flow.
- Look at cooling tower fans, fill and basin for fouling, damaged fill or fans running when not needed.
- Check furnace, ladle and duct insulation and refractory hot spots, since extra surface heat is lost energy.
- Verify temperature controls and sensors for drift that causes overcooling.
- Inspect piping and valve insulation, and confirm steam or hot water leaks are tagged for repair.
Idle Equipment Checklist
Equipment that runs without producing is the easiest loss to remove, once someone checks for it.
- Walk the area during planned stops and breaks, and list conveyors, fans, pumps and lighting still running.
- Check hydraulic power packs and lube units that stay at full duty when the line is idle.
- Confirm interlocks and sequences shut downstream equipment after upstream machines stop.
- Review start-stop rules for long conveyors and fans so they do not run empty between charges.
- Look for standby motors and heaters left energised unintentionally.
- Record each idle finding with area, equipment and the rule that should have stopped it.
Abnormal Energy Use Checklist
Meters point to where to look. The checklist confirms what is actually wrong.
- Confirm submeters cover major areas and utilities, and check meter calibration and data gaps.
- Track energy per tonne by area, and compare against a baseline adjusted for production and product mix.
- Set alert thresholds on deviation from the baseline, and record who reviews each alert.
- Compare consumption across identical machines to find units that draw more than their peers.
- Check power factor, demand peaks and unplanned start-ups that raise peak charges.
- Link each anomaly to recent maintenance or process changes before deciding on a cause.
Prioritising What You Find
Not every loss deserves a shutdown. Rank findings by repair effort and expected benefit, then schedule accordingly.
Loss Sources and Maintenance Actions
| Loss Source | Typical Cause | Detection Method | Maintenance Action |
|---|---|---|---|
| Compressed-air leak | Worn fittings, hoses, drains | Ultrasonic scan, off-shift demand check | Repair, tag and verify |
| Oversized motor | Conservative original sizing | Current versus nameplate | Right-size at replacement |
| Throttled fan or pump | Damper or valve control | Valve position, power draw | Evaluate variable speed drive |
| Fouled heat exchanger | Scale, deposits | Temperature approach, flow rise | Clean and treat water |
| Idle running | Missing interlock or habit | Walkdown during stops | Fix logic, add stop rule |
| Insulation damage | Heat, mechanical damage | Thermography | Repair insulation or refractory |
Running Energy Loss Detection in Oxmaint
Detection only saves energy if repairs follow. Oxmaint connects inspection to action.
- Inspections: mobile walkdown checklists per area and utility, with photos and readings.
- Work orders: corrective jobs raised directly from a failed or flagged checklist item.
- Preventive maintenance: recurring leak surveys, exchanger cleaning and motor checks.
- Asset management: history of motors, drives and utilities beside their repair records.
- Inventory: keep hoses, fittings, belts and drain valves available for quick repair.
- Dashboards: open loss tickets, overdue repairs and recurring problem areas.
Metrics to Prove the Checklist Works
Common Detection Mistakes
- Looking at total plant energy without normalising for production.
- Finding leaks but never tagging, ticketing or verifying the repair.
- Surveying once a year instead of building a repeating schedule.
- Replacing motors without checking load, speed control and alignment first.
- Counting savings without a before and after meter reading.
Energy Loss Checklist FAQs
How often should compressed-air leak surveys run?
Many plants survey quarterly and re-check after major work. Set the interval from leak recurrence in your own records.
What is the best first step in finding energy losses?
Normalise energy per tonne by area, then walk down the area that deviates most from its baseline.
How do I find idle equipment waste?
Walk the plant during planned stops and log what still runs. Record findings as tickets for follow-up.
Which motors should be replaced first?
Start with long-running motors at low load factor, then review throttled fans and pumps for speed control.
Can Oxmaint track energy loss repairs?
Yes. It links inspections to work orders and history. Book a demo to see the workflow.
Find the Loss, Fix It and Prove It
Move energy loss detection from occasional audits to a routine checklist with owned repairs and measurable results across your steel plant.