Energy is the largest controllable cost in steelmaking, often consuming 50-80% of a plant's total operating budget across blast furnaces, electric arc furnaces, reheat furnaces, and rolling mills. Yet most of that spend is not fixed by process design — it is decided day to day by how well the equipment behind it is maintained. A reheat furnace running high excess air can burn 10-15% more fuel than it should, a single one-inch compressed air leak drains $8,000-$14,000 a year, and every 1% drop in blast furnace thermal efficiency adds roughly $180,000 in annual fuel cost at a 1 MTPA scale. These losses rarely announce themselves as one event — they build silently across thousands of assets until the energy bill becomes unexplainable. Closing that gap starts with linking maintenance activity directly to energy performance instead of managing them as separate programs. See how Oxmaint connects maintenance to energy savings across every furnace, motor, and utility in your plant.
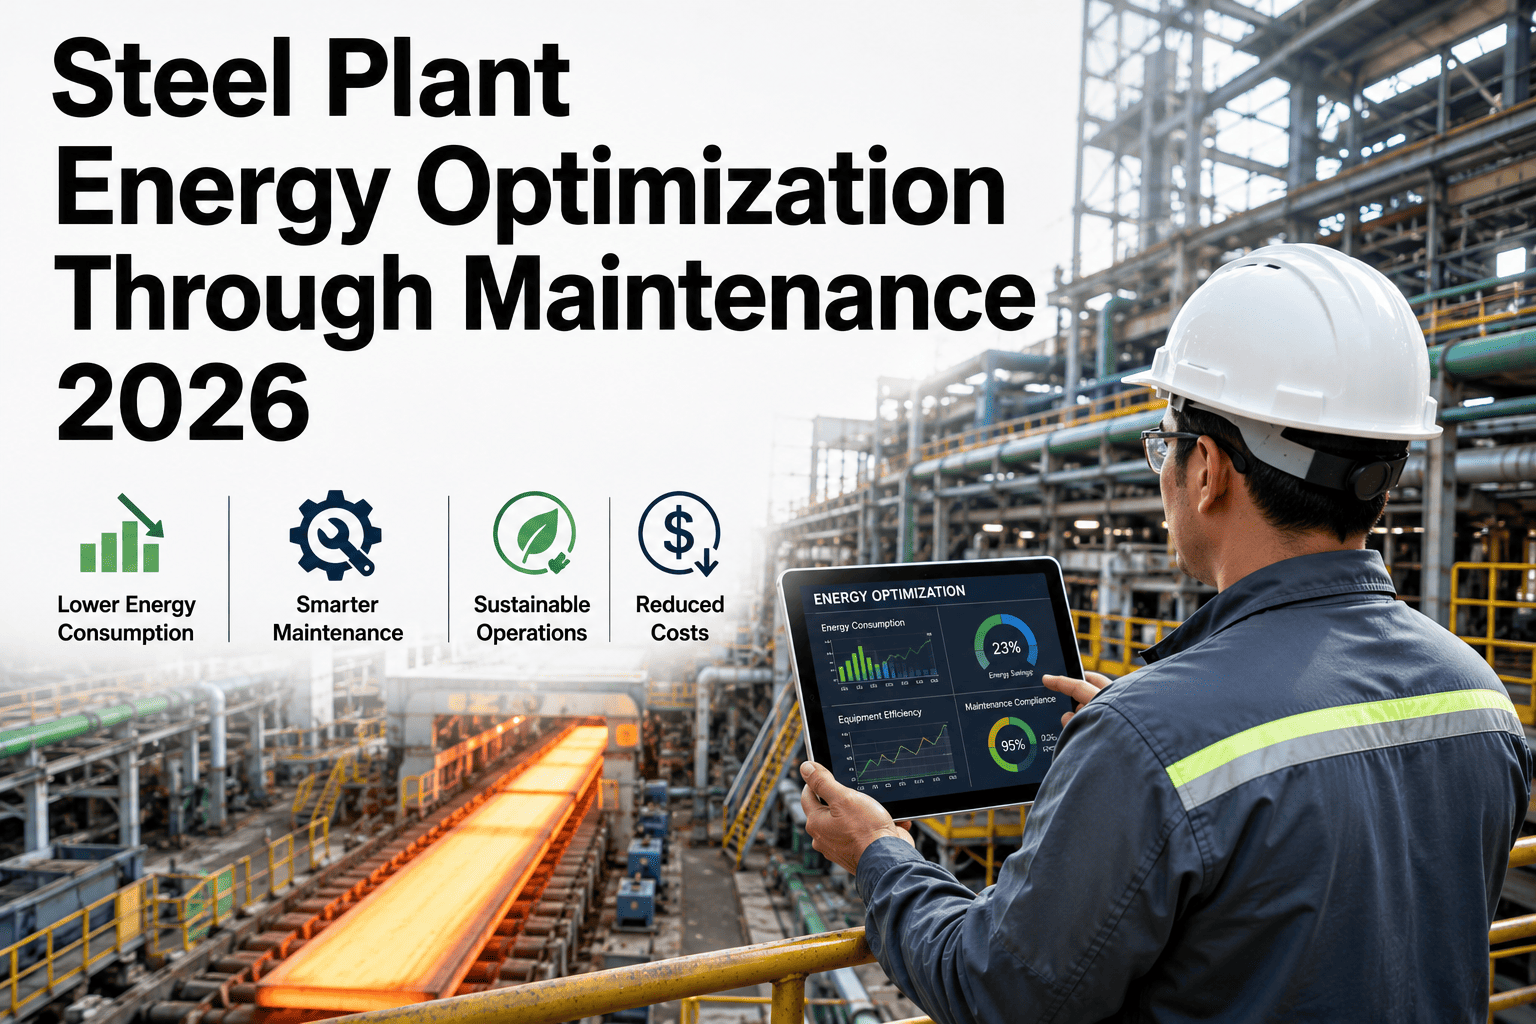
Steel Plant Energy Optimization Through Maintenance
Maintenance controls 15-30% of your total energy spend — blast furnace cooling, reheat combustion, motor efficiency, and compressed air all shift with every work order you do or skip.
Where Steel Plants Quietly Overspend on Energy
Energy waste in a steel plant almost never looks like a single failure. It looks like a burner running slightly out of tune for three months, a compressor operating a few PSI too high, or a bearing that adds a small current draw nobody notices on a shift report. Individually these are small. Multiplied across a full asset base running around the clock, they become the difference between a plant that hits its energy targets and one that quietly bleeds margin every single day.
5 Places Energy Disappears Across the Plant
Not every asset class carries the same energy risk. Some losses build over weeks through gradual drift, others appear the moment a component wears past tolerance. Knowing which system to watch — and what maintenance signal to track — is what turns a generic energy program into one that actually moves the utility bill.
Maintenance Indicators That Predict Energy Waste
Every one of these signals shows up in maintenance data well before it shows up as a spike on the electricity or fuel bill. Catching them at the work-order stage is what separates a plant reacting to costs from one preventing them.
| Maintenance Signal | What It Indicates | Typical Energy Impact | Detection Method |
|---|---|---|---|
| Elevated flue gas O2 reading | Reheat furnace burning excess air | 10-15% extra fuel burn | Continuous gas analyzer readings |
| Compressor specific power creep | Fouled intercoolers or worn seals | 15-25% above rated efficiency | kW per 100 CFM trend tracking |
| Rising coke rate at blast furnace | Refractory or cooling system degradation | ~$180K per year per 1% at 1 MTPA | Coke rate KPI monitoring |
| Drive current rising on rolling stands | Misaligned rolls or worn bearings | 3-9% higher specific energy per ton | Drive current baseline comparison |
| Audible or ultrasonic air leak | Failed fittings, hoses, or drain traps | $8,000-$14,000 per leak yearly | Quarterly ultrasonic leak survey |
| ASU approach temperature rising | Cold box heat exchanger fouling | 4-7% higher ASU power draw | Approach temperature trend logging |
The 4-Layer Energy-Linked Maintenance Framework
Energy optimization does not work as a side project bolted onto maintenance. It works when every PM task, every meter reading, and every efficiency program feeds into the same system — so the connection between a work order and a kilowatt-hour is visible, not assumed.
Every Unlinked Work Order Is an Energy Number You Cannot See
Oxmaint ties PM tasks, submeter readings, and combustion data into one system so energy loss shows up as a flagged work order, not a surprise on next month's bill.
Spreadsheet Energy Tracking vs. Maintenance-Linked Optimization
How Oxmaint Turns Maintenance Data Into Energy Savings
Oxmaint connects preventive maintenance, submetering, and combustion data into a single view — so energy performance is something your maintenance team manages every day, not an annual audit finding.
Every furnace, motor, and compressor PM task includes energy-relevant checkpoints — combustion readings, current draw, refractory condition — captured automatically during routine inspections.
Track Energy Performance Indicators for every Significant Energy Use, normalized against production so real efficiency changes are visible instead of masked by output swings.
Log flue gas readings and burner maintenance history side by side so drift toward excess air is caught before it turns into a 10-15% fuel penalty.
Trend kW per 100 CFM against baseline for every compressor, flagging degradation and leak-driven waste before it shows up as a wider utility bill.
Compare drive current and refractory wear against fleet baselines to isolate whether rising specific energy is a mechanical issue or a genuine process change.
Maintain the documented EnPIs, baselines, and review history needed for certification without a month of manual data aggregation before every audit.
What Energy-Linked Maintenance Delivers
Frequently Asked Questions
How much of a steel plant's energy cost does maintenance actually control?
Maintenance quality directly influences an estimated 15-30% of total energy spend through combustion tuning, motor condition, and compressed air integrity. Start a free trial to see where your plant sits against that range.
Which assets should we prioritize first for energy-linked maintenance?
Reheat furnaces and blast furnace cooling systems typically offer the largest dollar impact per fix, followed by rolling mill drive motors and compressed air systems. Book a demo to map priorities for your asset mix.
Does energy-linked maintenance require new capital equipment?
No. Most of the savings come from tuning, leak repair, and monitoring existing assets rather than purchasing new hardware, making this largely maintenance-addressable. Start a free trial to configure checkpoints on your current equipment.
How does this support ISO 50001 certification?
Energy-tagged PM data and submetering create the documented baselines and EnPIs that ISO 50001 requires, removing the manual data aggregation that usually delays certification. Book a demo to see the audit trail in action.
How soon do plants see measurable energy savings?
Combustion tuning and compressed air leak repair typically show measurable savings within weeks, with most programs reaching full payback around 90 days. Start a free trial to begin tracking your baseline today.
Stop Losing Energy to Maintenance Gaps You Cannot See
Oxmaint links every PM task, submeter reading, and combustion checkpoint into one system — turning energy optimization into a daily maintenance habit instead of an annual audit scramble.