Steel plants run equipment for decades, but the drives, controllers and electronic cards inside them are often discontinued within a fraction of that time. A part that was a catalogue item at commissioning can become a hunt through brokers and surplus dealers when a card fails in the middle of a campaign. Obsolete spare parts management is the discipline of finding these risks early and choosing a planned response, rather than reacting to a breakdown with no part and no supplier. This guide covers identification, risk scoring, response strategies and records for critical steel plant equipment. To keep obsolescence status beside each asset and spare, you can track parts and equipment together in Oxmaint.
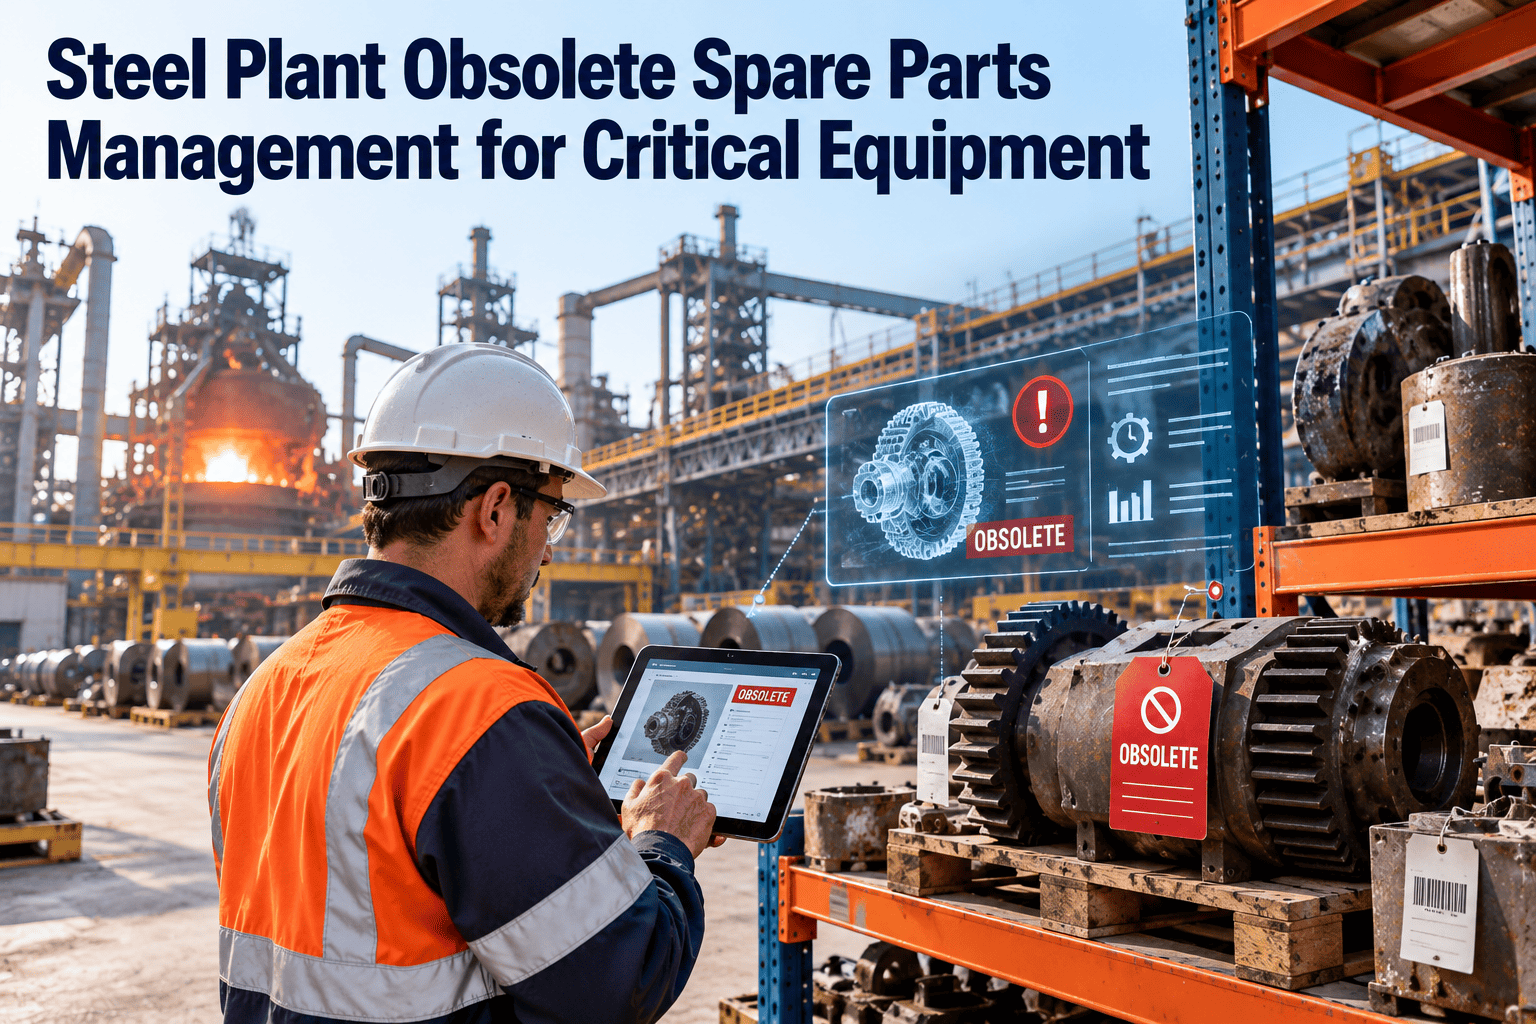
Steel Plant Obsolete Spare Parts Management for Critical Equipment
Map where obsolescence sits in your plant, rank it by consequence and pick a response that fits each part, from last-time buy to planned retrofit.
Why obsolescence is a steel plant problem
Long equipment life
Mill stands, casters and furnaces are built to run for decades, which far outlasts the support period of most electronic components.
Piecemeal upgrades
Controls are replaced in stages, leaving old and new generations side by side with parts that do not interchange.
High cost of waiting
A single obsolete card on a critical line can hold production while a replacement is sourced or the logic is reworked.
Weak records
Many plants cannot say how many units of a given drive or controller are installed, so risk stays invisible.
Which parts become obsolete first
| Part group | Typical obsolescence driver | Risk to the plant |
|---|---|---|
| PLC and controller modules | Product line retired by the manufacturer | Loss of replacement cards and programming support |
| Variable speed drives and DC drives | Generation change and withdrawn repair service | Main drive failures with no direct replacement |
| Operator panels and HMIs | Operating system and hardware support ends | Local control lost after a panel failure |
| Instruments and sensors | Model discontinued or protocol replaced | Measurement loss and control instability |
| Motors and gearboxes | Manufacturer closed or frame size changed | Long lead times and custom adapters |
| Hydraulic and pneumatic valves | Series withdrawn or supplier acquired | Non-standard replacements and retesting |
| Bearings and seals in old designs | Custom sizes no longer produced | Reliance on special orders or remanufacture |
Obsolescence differs by manufacturer and product line, so confirm status with each supplier and record the date you checked.
Rank obsolescence risk: consequence against supply
Watch
Hold stock and monitor notices.Act now
Buy, qualify an alternate or plan a retrofit.Urgent
Project-level response with a funded date.Routine
Normal stocking and review.Plan
Decide a response at the next outage.Plan soon
Choose a substitute or refurbishment path.Response strategies and when each fits
Last-time buy
Purchase enough units to cover the expected life of the equipment before supply ends. It suits small, stable parts, but ties up cash and needs a sound demand estimate.
Repair or refurbish
Use a qualified repair shop to restore failed units. It keeps old hardware running, though turnaround and parts supply need checking.
Approved equivalent
Fit a form, fit and function replacement from another supplier. It needs engineering approval and testing before it counts as a spare.
Surplus and broker supply
Buy from specialist suppliers of used or new-old-stock parts. Verify authenticity, condition and warranty, since quality varies widely.
Reverse engineer or remanufacture
Recreate a mechanical part from samples and drawings. It can solve long-lead items but needs material and tolerance checks.
Planned retrofit
Upgrade the drive, controller or panel during an outage. It removes the risk, but needs budget, engineering time and commissioning.
A decision path for each at-risk part
Confirm status
Ask the supplier for lifecycle stage and record the date.Count exposure
List installed units, spares on hand and equipment dependent on the part.Score consequence
Rate production, safety and environmental impact if it fails.Choose a response
Select buy, repair, substitute, source or retrofit with reasons.Fund and schedule
Attach a budget and a target outage or date.Review
Recheck status on a set cycle and after any supplier notice.Know which spares are at risk before they fail
Oxmaint links parts to assets, installed counts and work history, so obsolescence risk is visible where maintenance decisions are made.
What to record for every obsolete or at-risk part
Identity
- Part number and manufacturer
- Equipment and tag it serves
- Installed quantity across the plant
- Approved alternatives and conditions
Status
- Lifecycle stage and date checked
- Supplier notice reference
- Repair option and turnaround
- Last known price and lead time
Decision
- Chosen response and reason
- Owner and target date
- Budget reference
- Next review date
Stock
- Spares on hand and location
- Tested or untested condition
- Shelf life and storage needs
- Reserved for which asset
Buying obsolete parts safely
Risks with surplus supply
- Counterfeit or relabelled components
- Used units with hidden wear
- Wrong firmware or hardware revision
- Unclear return and warranty terms
Controls that reduce the risk
- Buy from suppliers with traceable sources and test reports
- Inspect and bench-test on receipt before stocking
- Record revision and firmware against the part
- Agree returns and warranty before ordering
Treat parts from surplus channels as unproven until tested. Stock them with a clear label so no one mistakes a bench-tested spare for a factory-new unit.
Building obsolescence into maintenance planning
| Planning moment | Obsolescence action | Benefit |
|---|---|---|
| Annual maintenance plan | Review the at-risk register and fund the top items | Risk is budgeted, not discovered |
| Shutdown planning | Schedule retrofits and substitutions into outage scope | Upgrades use planned downtime |
| Failure review | Check whether the failed part is already at risk | Repeat exposure is caught early |
| Project design | Check lifecycle stage of every new component specified | New obsolescence is avoided at source |
| Supplier meetings | Ask for end-of-life notices and roadmap changes | Longer warning before supply ends |
How Oxmaint helps manage obsolescence risk
Asset management
Record installed equipment, models and revisions so you can count exposure to any one part.
Inventory
Track spares, locations and minimums, and mark items as insurance stock for at-risk equipment.
Work orders
Create planned retrofit and substitution jobs with parts, labour and documents attached.
Reporting
Review failures by part and asset to spot repeat exposure and prioritize replacement.
Early warning sources worth monitoring
Manufacturer notices
End-of-life and last-order announcements are the clearest signal. Assign someone to receive and log them.
Supplier conversations
Regular account meetings often reveal quiet changes, such as longer repair queues or limited stock.
Rising lead times
A part that used to arrive in weeks and now takes months is often heading toward withdrawal.
Failed order attempts
Record any case where a part could not be bought new, since it flags a supply problem early.
Repair shop feedback
Repairers know when component supply is drying up and can warn about it.
Failure history
Repeat failures on aging controls point to parts that deserve a lifecycle check.
Stock or retrofit: factors that decide
| Factor | Points toward stocking spares | Points toward retrofit |
|---|---|---|
| Installed quantity | Few units, easy to cover with a small stock | Many units, so spares would be expensive and still finite |
| Remaining equipment life | Short, with a replacement already planned | Long, so supply risk will outlast any stock |
| Repair availability | A qualified shop can restore failed units | No repair route and failed units are scrapped |
| Consequence of failure | Contained, with a bypass or standby | Vital, with long outage and safety exposure |
| Support and knowledge | Engineers still know the system well | Few people understand the old platform |
| Outage windows | Rare, so large changes are hard to schedule | Regular, so retrofit can be planned in |
No single factor decides. Score each one and discuss the total with operations, engineering and finance.
Software and firmware obsolescence
Often overlooked
- PLC programs stored on a single laptop or a retired engineer's account
- Programming software that needs an old operating system
- Firmware revisions that differ between spare and installed units
- Drive parameter sets that were never exported
- Licences tied to hardware that is no longer made
Protective steps
- Keep verified backups of programs and parameters in controlled storage
- Preserve a working engineering workstation or virtual copy
- Record firmware and hardware revision against each spare
- Test restoring a backup on a spare unit before a failure forces it
- Link these records to the equipment in the maintenance system
Building the case for a retrofit
Describe the exposure
Equipment affected, installed units, spares on hand, supply status.Show the failure history
Past failures, downtime and repair difficulty from work order records.Estimate consequence
Production, safety and environmental effect if the part fails with no supply.Compare options
Stock, repair, substitute and retrofit with cost and risk side by side.Propose a window
Match the work to a planned outage and list parts, labour and testing.A case built from the plant's own work order history is far more persuasive than a general argument about aging electronics. Clean records make the case for you.
Mistakes that leave critical equipment exposed
Counting spares but not installed units
Knowing you hold two cards means little if you do not know forty are running.
Assuming supplier status stays true
Lifecycle status changes. Record the check date and re-verify on a cycle.
Stocking untested used parts
An untested spare gives false comfort. Bench-test before it counts as cover.
Leaving retrofit to a breakdown
Emergency replacement under pressure costs more and risks errors in commissioning.
Ignoring non-electronic parts
Custom bearings, gears and castings also lose supply and need the same attention.
An annual obsolescence review in six questions
- Which critical assets contain parts that are mature, limited or obsolete?
- For each, how many units are installed and how many spares are tested and on hand?
- Which parts have no repair route and no approved substitute?
- Which retrofits are funded and scheduled, and which are still only ideas?
- Have program backups and parameter sets been verified in the last year?
- What new risk came from projects or changes completed this year?
Obsolescence in mechanical parts
Electronics get the attention, but heavy mechanical parts also lose supply. Custom bearing sizes, large gears, couplings and castings may no longer be produced, or may need long production slots and special material checks.
Bearings and housings
Record the exact designation, fit and housing details, then check for current equivalents before a failure forces a rush.
Gears and pinions
Keep drawings, material specifications and heat treatment details so a remake is possible.
Couplings and spindles
Capture dimensions and balance data. Long lead items need an insurance spare or a remake plan.
Seals and gaskets
Confirm profile and material for each application, since small differences affect life.
Example path for one at-risk drive card
Supplier announces withdrawal
The notice is logged against the part and every asset that uses it.Count exposure
Installed units, spares and failure history are pulled from records.Choose a response
The team compares last-time buy, repair and a planned drive upgrade.Schedule the work
A retrofit work order is planned into the next outage with parts and testing.The example is illustrative and generic. Real decisions depend on your equipment, supplier terms and outage calendar.
Who does what in an obsolescence program
| Role | Responsibility | Output |
|---|---|---|
| Reliability engineer | Scores consequence and recommends a response | Risk ranking and options |
| Controls or electrical engineer | Checks substitutes, backups and firmware | Technical approval for alternates |
| Planner | Builds retrofit jobs and links them to outages | Scheduled work orders |
| Storekeeper | Holds and labels insurance and tested spares | Accurate stock and test status |
| Procurement | Manages suppliers, last-time buys and notices | Verified sources and terms |
| Finance partner | Reviews budget and cost of delay | Funded plan |
Measures that show the program is working
Critical assets with a status check
Share of critical equipment whose parts have a recorded lifecycle status and check date.
At-risk items with a decision
Share of obsolete or limited parts that have a chosen response and an owner.
Funded retrofits
Number of retrofit items with a budget and an outage slot.
Failures with no spare
Count of failures where an obsolete part was unavailable, expected to fall.
Frequently asked questions
What is obsolete spare parts management?
It is identifying parts at risk of discontinuation and choosing a planned response, so critical equipment is not left without a supply path.
Is a last-time buy always the best option?
No. It ties up cash and depends on a good demand estimate. Compare it with repair, substitution and planned retrofit.
How do we know which equipment is exposed?
Link parts to equipment and installed counts. You can get started and build that register from your asset list.
Are used or surplus parts safe for critical equipment?
They can be, with traceable sourcing and bench testing. You can book a demo to see how test status is recorded.
When should a plant retrofit instead of stocking spares?
When supply is gone, spares are scarce and the equipment is vital. Plan the retrofit for an outage and fund it in advance.
Plan for the part that will not be there
Map the exposure, rank it by consequence and choose a response before the failure. Oxmaint keeps parts, assets and decisions in one record.