A steel plant already produces the signals that predict most maintenance work: a drive fault on a mill stand, pressure drift on a hydraulic unit, a pump that trips on motor current. Too often those signals stop at a control room screen, and maintenance hears about them after the failure. OPC UA gives plants a standard, secure way to carry that data into the maintenance system. This guide covers what to connect, which signals deserve a work order and how to keep the link secure. You can start a free Oxmaint account to prepare the asset register first.
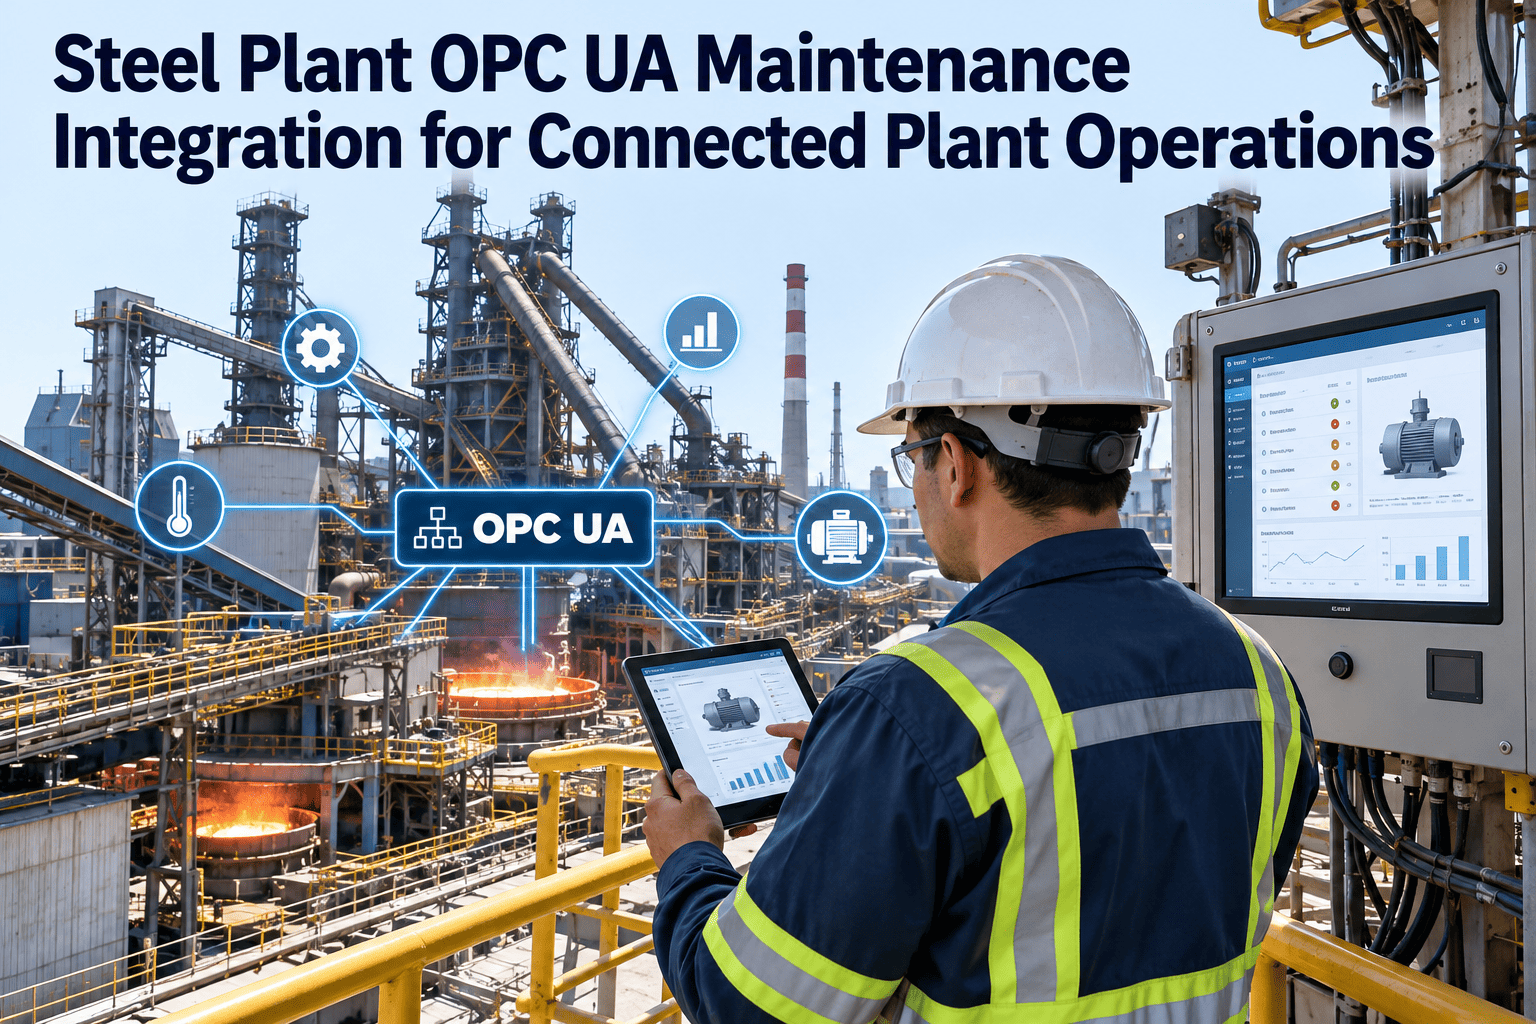
Steel Plant OPC UA Maintenance Integration for Connected Plant Operations
Connect PLCs, SCADA, historians and your maintenance system through one open standard, so a signal on the mill floor becomes an assigned, evidenced work order instead of a line in a shift log.
Where Steel Plant Maintenance Signals Get Lost
The gap is rarely a lack of data. It is a lack of a path from the automation layer to the person who can act on it.
What OPC UA Brings to the Maintenance Layer
OPC UA is an open, platform-independent standard, published internationally as IEC 62541. Its value for maintenance is that one client can read data from many vendors without a custom driver per controller.
| Capability | What it exposes | Maintenance use |
|---|---|---|
| Data Access | Current values of tags with quality status, timestamp and engineering units | Read run-hour accumulators, cycle counters and condition variables for usage-based and condition-based PM |
| Alarms and Conditions | Alarm and event objects with severity, state, acknowledgement and time | Create corrective work orders from real alarm events rather than from screenshots and phone calls |
| Historical Access | Time-series values and events stored by a historian | Attach the trend before a fault to the work order so the technician starts with evidence |
| Information Model | A structured address space with typed objects, folders and references | Map a node to the asset it belongs to, instead of working from flat tag names |
| Security Model | Application certificates, signing, encryption and user authentication | Let the maintenance system read plant data without opening an unprotected path into the control network |
| Publish and Subscribe | Subscriptions with monitored items, and a PubSub option for broker-style delivery | Receive changes as they happen instead of polling every tag on a timer |
From Tag to Work Order: The Six-Step Path
An integration succeeds when each step has an owner and a rule. Skipping the middle steps is why many projects produce either silence or a flood of unusable work orders.
Map Your First Ten Signals to Real Assets
Start with one process area, one asset list and ten signals. Build the asset register and work order templates in Oxmaint, then connect the data once the mapping is agreed.
Which Signals Deserve a Work Order
Not every alarm is a job. Sort signals by two questions: how confident are you that it means a real fault, and what happens if nobody acts.
Securing the Connection Between OT and Maintenance
Plant security teams are right to be cautious. OPC UA was designed with security built in, and the maintenance integration should use all of it.
- Choose a current security policy such as Basic256Sha256 or newer. Older policies such as Basic128Rsa15 and Basic256 are regarded as outdated.
- Exchange and approve application certificates deliberately, and keep a trust list of which clients may connect.
- Use a dedicated read-only account for the maintenance client, with access limited to the nodes it needs.
- Place the collector in a demilitarized zone between the control network and the business network, with firewall rules limited to the server endpoint.
- Treat certificate expiry as a maintenance task on the integration itself, with a preventive work order raised well before the date.
Mapping the Plant Hierarchy to the Asset Register
OPC UA node names follow the automation engineer's logic. Maintenance needs the same signal under the asset it belongs to. The table below is an illustrative mapping, not a template for your site.
| Node path (illustrative) | Asset | Signal type | Maintenance response |
|---|---|---|---|
| Mill/Stand3/MainDrive/FaultActive | Stand 3 main drive | Fault bit | Corrective work order with high priority |
| HydraulicUnit2/Pressure | Hydraulic power unit 2 | Analog value with limits | Inspection work order after dwell time |
| Caster/Segment12/CycleCount | Caster segment 12 actuator | Counter | Usage-based preventive maintenance |
| DescalingPump1/RunHours | Descaling pump 1 | Run-hour accumulator | PM at the meter interval |
| Compressor3/DischargeTemp | Air compressor 3 | Analog trend | Condition-based inspection when drift persists |
A Rollout Timeline That Protects Production
The timeline depends on plant age, network design and how many controllers need gateways. The sequence below stays the same.
KPIs That Prove the Integration Is Working
Measure the integration like any other maintenance process. Set your own baselines before go-live so the trend is honest.
| KPI | How to calculate it | What it tells you |
|---|---|---|
| Alarm-to-work-order conversion | Qualified alarms that produced a work order divided by qualified alarms | Whether real faults are reaching maintenance |
| Time to work order | Alarm timestamp to work order creation time | How much detection delay the integration removed |
| False trigger rate | Work orders closed with no fault found divided by work orders raised | Whether rules and dwell times need tuning |
| Evidence coverage | Work orders with a trend or alarm record attached divided by all integrated work orders | Whether technicians start with data |
| Critical asset coverage | Critical assets with at least one mapped signal divided by all critical assets | How far the integration has actually reached |
| Meter-based PM share | PMs triggered by counters or run hours divided by all PMs on integrated assets | How much calendar maintenance has become usage-based |
Where Oxmaint Fits in the Connected Plant
Oxmaint is the maintenance system of record that receives the qualified event and manages the response through the integration approach agreed for your site.
Pre-Integration Checklist
Work through these checks before you ask anyone to open a firewall port.
- Critical assets are ranked and have unique IDs in the register
- Each target controller is confirmed as native OPC UA, gateway or driver
- A plant-side owner is named for every OPC UA server
- Selected nodes each answer a defined maintenance question
- Priority and response window are set for every mapped signal
- Security mode, policy and certificate process are agreed with plant IT
- A read-only account and access scope are documented
- Dwell time and planned-stop suppression rules are written down
- Work order templates exist for each signal type
- Success KPIs have a baseline before go-live
Choosing a Connection Path for Each Controller
A steel plant rarely has one automation vendor or one generation of equipment. Decide the path asset by asset, and record the choice in the mapping table.
| Path | Where it fits | Strength | Watch-out |
|---|---|---|---|
| Native OPC UA server on the controller | Newer PLCs and drives that ship with a server | Direct, structured access without extra software | Enabling it may need a firmware or licence check, and extra load on the controller |
| SCADA or DCS OPC UA server | Areas where the supervisory system already aggregates tags | One endpoint for many controllers, with alarms included | Tag names follow the SCADA design, and may not match the asset register |
| Historian interface | Trends, summaries and event history | Good for attaching evidence to work orders | Check which tags are stored and at what resolution |
| Gateway for legacy protocols | Older PLCs speaking serial, Modbus or vendor protocols | Avoids replacing working controllers | Adds a device to maintain, patch and document |
| Level 2 or MES database view | Production systems that expose data through tables | Brings heat, coil and campaign context | Access must be read-only and agreed with the system owner |
| Broker-based publishing | Many sites or edge devices sending events | Scales across plants and tolerates intermittent links | Needs clear topic naming and message ownership |
Where OPC UA Projects Stall
A Commissioning Test Plan Before Go-Live
- Browse the address space and confirm every mapped node exists, with the expected data type and unit.
- Force a safe test condition on one asset and confirm the event reaches the maintenance system with the right timestamp.
- Interrupt the network link, restore it and confirm that no events are duplicated or silently lost.
- Expire a test certificate on purpose and confirm that someone is alerted, instead of the connection failing without notice.
- Check that a planned stop suppresses the corrective trigger it is supposed to suppress.
- Confirm that the maintenance account can read the agreed nodes and nothing else.
- Repeat the whole test after any controller program change that touches mapped tags.
Frequently Asked Questions
Give Every Critical Signal a Maintenance Owner
Bring plant data and maintenance records into one workflow, so alarms, trends and counters turn into planned work with evidence attached.