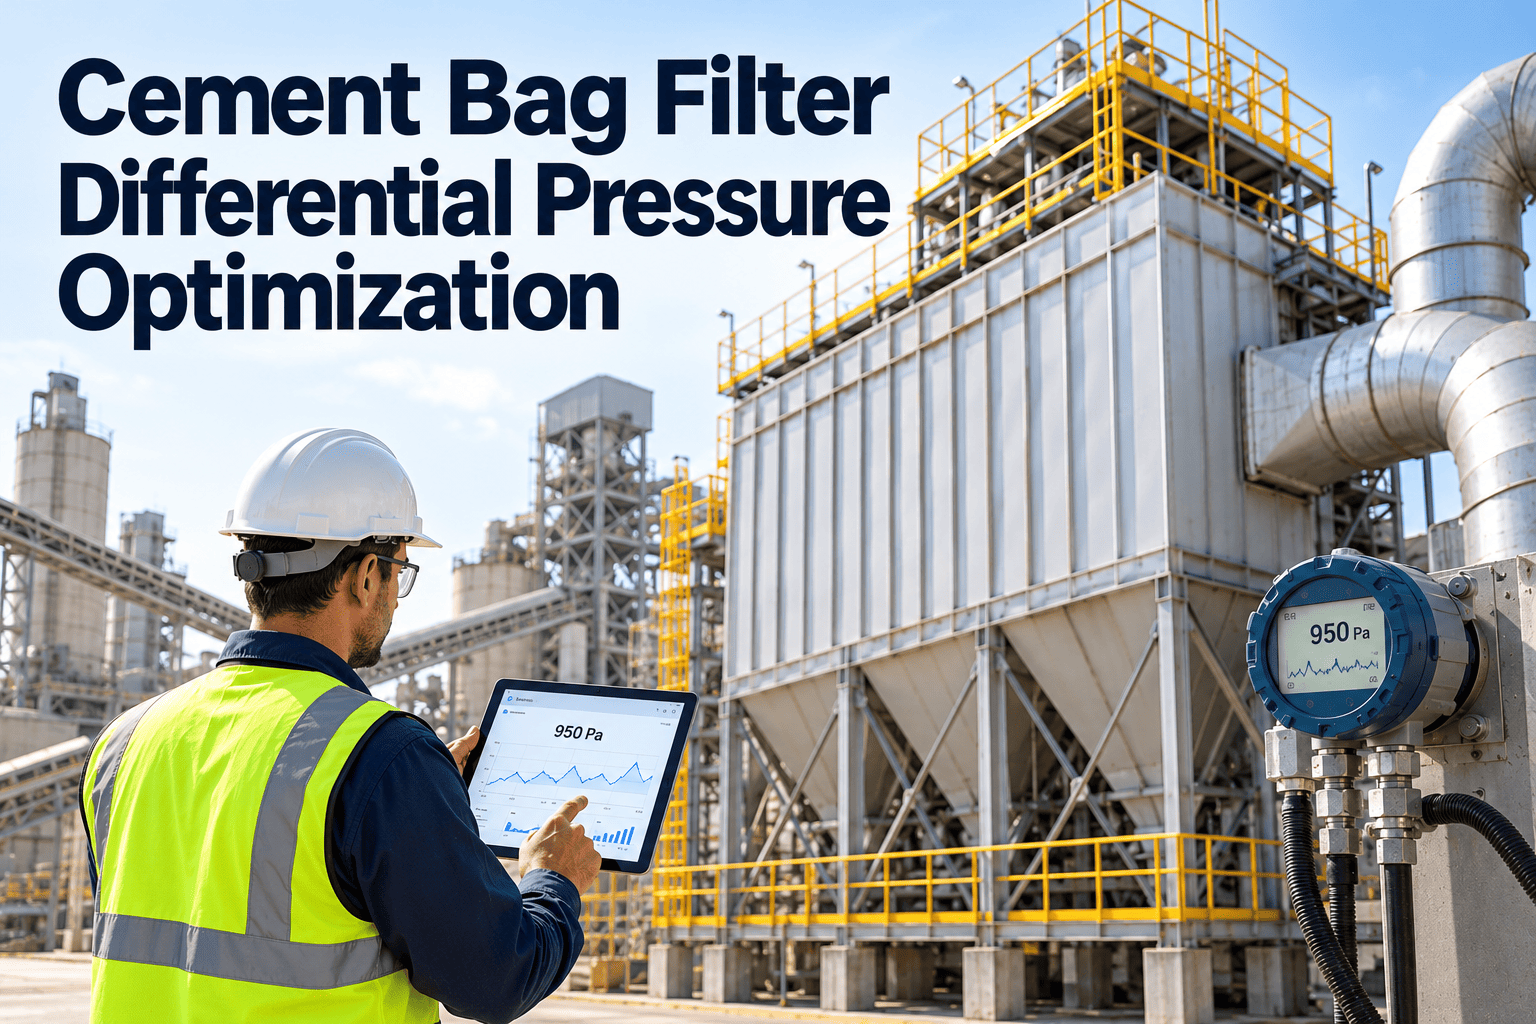
Bag filters clean the dust-laden gas from kilns, raw mills, coolers, cement mills, and transfer points, and differential pressure is their most important health signal. When it climbs, fans work harder, airflow drops, and energy use rises. When it falls suddenly, bags may be torn and dust may be escaping. Many plants watch the number but have no routine for acting on it. This guide shows how to read it, tune cleaning, and organize the work with Oxmaint maintenance management software.
Cement Bag Filter Differential Pressure Optimization
Keep dust collectors in the efficient window: low enough to save fan energy, high enough to prove the bags are intact.
Why differential pressure matters for energy and emissions
Differential pressure is the resistance the gas meets crossing the bags and the dust cake on them. Every extra unit of resistance must be supplied by the fan.
When pressure drop is too high
- Fan power rises to hold airflow
- Airflow can fall below what the process needs
- Kiln or mill draft may become unstable
- Bags wear faster under stress
- Compressed air use increases with cleaning
When pressure drop is too low
- Torn or missing bags let dust through
- Seals, doors, or tube sheet leaks bypass the filter
- Stack dust readings may rise
- Over-cleaning can strip the protective cake
- Compliance risk grows
Energy and emissions pull in opposite directions, so optimization means finding the stable middle, not simply driving the number down.
Reading the trend: what the shape of the curve says
A single value tells little. The pattern over days and weeks points to the cause.
| Trend pattern | Likely causes | First checks |
|---|---|---|
| Slow steady rise over weeks | Bag blinding, fine or sticky dust, gradual loss of cleaning effect | Cleaning settings, compressed air quality, bag condition |
| Sudden step increase | Cleaning system failure, valve or controller fault, process upset, moisture event | Controller status, valve operation, inlet temperature |
| Sudden drop | Bag failure, loose bags, leaking seals or doors | Stack dust monitor, visual check, compartment isolation |
| Rises after every shutdown or start-up | Condensation, low temperature operation, poor start-up procedure | Preheating, temperature logs, bypass practice |
| One compartment differs from others | Local valve, diaphragm, blow tube, or bag issue | Compartment pulse count and valve test |
| Noisy, swinging readings | Blocked or leaking sensing lines, transmitter fault | Impulse lines, transmitter calibration |
How pulse-jet cleaning sets the pressure
Most cement bag filters clean by releasing a short burst of compressed air down each row of bags. The burst shakes loose part of the dust cake, and the cycle repeats row by row.
- Dust builds. Gas passes through and a cake forms on the outside of the bags, raising pressure drop.
- Controller triggers. A timer or a pressure setpoint starts the cleaning sequence.
- Valve opens briefly. A diaphragm valve releases air through the blow tube into the bag row.
- Cake releases. The pulse flexes the bag, and dust falls to the hopper.
- Cake rebuilds. A thin layer returns, which is needed for good filtration.
- Hopper empties. Rotary valves or conveyors remove the dust so it does not rise back into the bags.
Timed versus demand-based cleaning
| Approach | Advantage | Risk |
|---|---|---|
| Timed cleaning | Simple and predictable | Cleans too often at low load, too little at high load |
| Demand-based on differential pressure | Cleans when needed and can save air and bag wear | Depends on a reliable pressure signal and sensible limits |
Whichever method is used, record setpoints and changes. A cleaning change made without a record becomes a mystery the next time pressure moves.
Turn pressure trends into planned filter work
Schedule inspections, log findings, and track every filter from one maintenance system.
Root causes of high differential pressure
Root causes of low or falling differential pressure
Low pressure is not always good news. Treat an unexplained fall as a possible emissions problem until proven otherwise.
Look for
- Holes, tears, or abrasion near the top or bottom of bags
- Bags not seated or sealed on the tube sheet
- Damaged or corroded cages cutting the fabric
- Leaks at doors, hatches, and compartment dampers
- Over-cleaning that removes the filter cake
Confirm with
- Stack dust or opacity monitor trends
- Visual dust at the clean-gas outlet or stack
- Compartment isolation tests
- Leak checks during planned stops
- Bag inspection and replacement records
A diagnostic path from alarm to action
Preventive maintenance plan for bag filters
Most pressure problems start as small neglected tasks. A clear schedule keeps them from building up.
| Frequency | Task | Purpose |
|---|---|---|
| Every shift | Check differential pressure, compressed air pressure, and hopper discharge | Catch early drift and stalled discharge |
| Weekly | Drain air receivers and filters, listen for valve leaks, check dryer function | Keep air dry and pulses strong |
| Monthly | Test solenoids and diaphragm valves, review pulse counts by compartment | Find weak or failed cleaning valves |
| Quarterly | Inspect rotary valves, screws, seals, and access doors | Prevent dust build-up and false air |
| At planned stops | Inspect bags, cages, blow tubes, and tube sheet; replace damaged items | Restore filtration and cleaning performance |
| Annually | Calibrate transmitters, review setpoints, and check bag life against records | Keep readings and settings reliable |
Optimization levers, in the order to try them
Filter duty differs across the cement plant
A kiln and raw mill filter faces very different gas and dust than a packing plant filter. Set pressure expectations and maintenance tasks by duty, not by one plant-wide rule.
| Filter location | Typical challenge | Maintenance emphasis |
|---|---|---|
| Kiln and raw mill | High gas temperature, moisture swings, and fine alkali-bearing dust | Temperature control, start-up heating, bag material, and sealing |
| Clinker cooler | Hot, abrasive clinker dust and varying gas flow | Bag wear, inlet protection, and cleaning intensity |
| Cement mill | Very fine product dust and variable load | Blinding, air quality, and cleaning tuning |
| Coal and alternative fuel systems | Combustible dust and strict safety needs | Safety devices, inspections, and housekeeping per site rules |
| Silos, transfer points, and packing | Many small filters, often unattended | Routine rounds, discharge reliability, and spare management |
Smaller filters are easy to overlook. A simple inspection route with a pass or fail pressure check keeps them visible.
Compressed air: the hidden driver of cleaning quality
Cleaning energy comes from the air supply. A filter with perfect valves still cleans poorly if the air is wet, low, or unstable.
Check regularly
- Header pressure at the filter, not only at the compressor
- Receiver drains and automatic drain function
- Dryer performance and dew point alarms
- Filters and regulators on the supply line
- Audible leaks at fittings and valves
Signs of an air problem
- Weak pulse sound or slow pressure recovery
- Water or oil at drain points
- Pressure rising while pulses appear normal
- Compressor running longer than before
- Repeated diaphragm failures
Start-up and shutdown practices that protect bags
Many bag failures begin at the edges of operation, when gas is cold, wet, or changing quickly. Written procedures reduce the damage.
- Preheat before dusty gas. Bring the filter above the dew point before process gas with moisture reaches the bags.
- Pre-coat where required. Follow supplier advice for protecting new bags during first operation.
- Watch temperature limits. Avoid exceeding fabric ratings during upsets and bypass events.
- Clean before shutdown. Run an off-line cleaning cycle if the design allows it, to limit moist residue.
- Empty hoppers. Discharge dust so it does not absorb moisture and bridge during the stop.
- Record the event. Log temperatures, duration, and any problems to support later diagnosis.
Fan energy: turning pressure into a cost conversation
Fan power depends on flow and the pressure the fan must overcome. Lower resistance in the filter reduces the work required, so stable low-end operation within the target window can save energy.
Bag replacement decisions
Changing bags too early wastes money, and changing them too late costs energy and risks emissions. Use evidence from several sources.
- Trend evidence. Pressure that no longer recovers after cleaning suggests permanent blinding.
- Visual evidence. Wear, holes, or hardened dust seen during inspection of sample bags.
- Laboratory evidence. Supplier or lab tests on strength and permeability where available.
- Age and cycles. Operating hours and number of cleaning pulses since installation.
- Failure pattern. Repeated failures in one compartment point to a local cause, not overall age.
Keep installation dates and compartment locations in the asset record. That history is what lets you judge whether a bag type is performing.
Where Oxmaint helps with filter reliability
The software does not tune the filter. It makes sure the inspection, repair, and learning around the filter actually happen.
Compliance and record keeping
Dust emission limits and monitoring rules vary by country and permit, so follow the requirements that apply to your site. Maintenance records strengthen your position in any review.
- Keep dated records of bag replacements, with location and reason
- Record every cleaning system repair and setpoint change
- Link stack monitor excursions to the related inspections and work orders
- Store calibration records for pressure and dust monitoring instruments
- Document start-up and shutdown practices that protect the bags
Good records also help during bag warranty and supplier discussions, since actual operating conditions can be shown.
KPIs for filter performance
| KPI | What it shows | Use |
|---|---|---|
| Average and peak differential pressure | Typical load and worst events | Compare filters and periods |
| Time outside target window | How often the filter ran too high or too low | Prioritize attention |
| Fan energy per tonne processed | Energy cost of filtration | Quantify savings from tuning |
| Compressed air use for cleaning | Air consumed by pulses | Detect over-cleaning and leaks |
| Bag life | Operating time or tonnes before replacement | Plan stock and compare fabrics |
| Valve failure count | Cleaning system reliability | Target weak components |
| Stack dust excursions | Emissions performance | Link to bag and seal condition |
Bag filter pressure questions
What differential pressure is normal for a cement bag filter?
It depends on design, bags, and load. Use the manufacturer's values and your own stable baseline.
Should we lower the pressure setpoint to save energy?
Only carefully. Over-cleaning shortens bag life and removes the cake. Book a demo to see how changes can be tracked.
Why does pressure rise after every start-up?
Cold gas can drop below the dew point and wet the dust. Review preheating and start-up steps.
Can low pressure mean a problem?
Yes. A sudden fall may mean torn bags or leaks, so check stack readings and inspect the compartments.
How do we track bag life properly?
Record each bag change against the asset and compartment. You can sign up and start a history today.
Run every dust collector in its best window
Give your team one system for inspections, repairs, bag history, and compliance records.