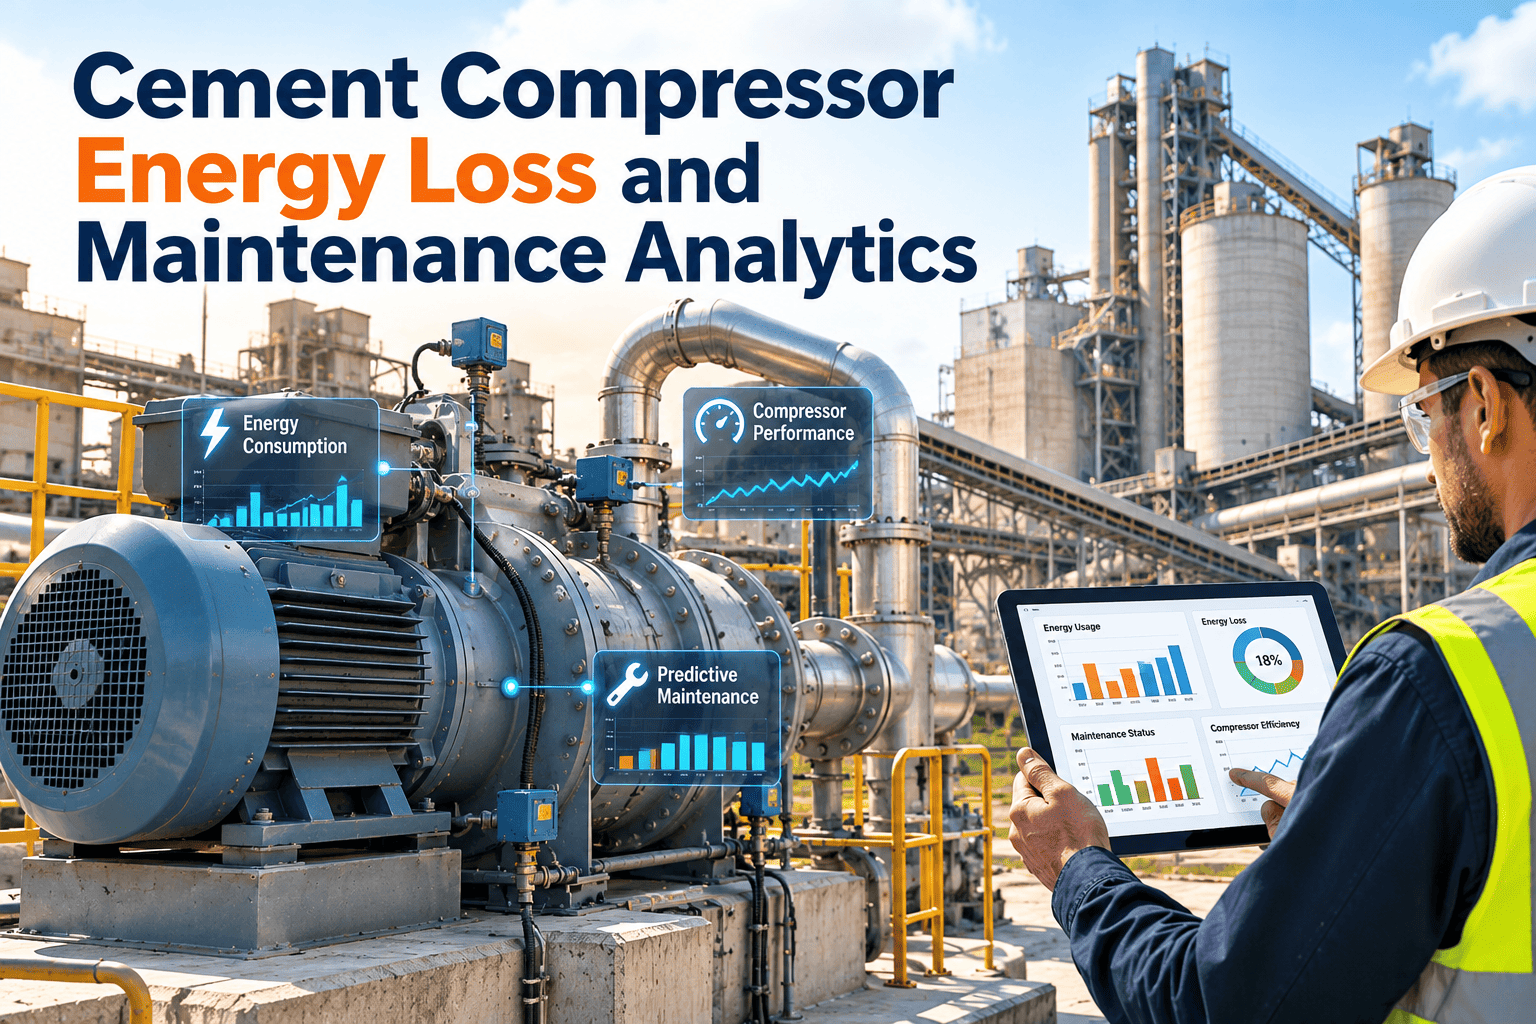
Compressed air is one of the least visible energy users in a cement plant and one of the most expensive per unit of useful work. It cleans baghouse filters, drives pneumatic conveying and air slides, supplies instrument air, and runs packing plant equipment. Leaks, high pressure settings, fouled coolers, and clogged filters quietly raise power use month after month. This guide shows how to find and measure compressor energy loss, which maintenance tasks recover it, and how maintenance management software keeps leak repairs and compressor service on schedule.
Cement Compressor Energy Loss and Maintenance Analytics
Find where compressed air energy is wasted in a cement plant, and use maintenance data and analytics to recover it and keep it recovered.
Where Compressed Air Is Used in a Cement Plant
Dust, heat, and vibration make cement plants harsh for compressors, dryers, filters, and piping, which accelerates every loss described below.
The Main Sources of Energy Loss
| Loss source | What happens | Maintenance or analytics signal |
|---|---|---|
| Leaks | Compressed air escapes through joints, hoses, fittings, valves, and worn couplings | Rising load time, falling pressure at no-production periods, ultrasonic survey findings |
| Artificial demand | Pressure set higher than needed, so unregulated uses consume more | Discharge pressure above requirement, higher power for the same output |
| Filter and dryer pressure drop | Clogged filters force the compressor to work harder | Differential pressure across filters and dryers |
| Inter- and after-cooler fouling | Dust and scale reduce heat transfer, raising air temperature | Rising approach temperature and discharge temperature |
| Inlet air condition | Hot or dusty inlet air reduces efficiency | Inlet temperature and inlet filter differential pressure |
| Control inefficiency | Poor sequencing makes several machines run partly loaded | Low load factors, frequent loading and unloading cycles |
| Condensate drain failures | Stuck drains vent air or let water into the system | Constant air loss at drains, moisture downstream |
Metrics That Make Energy Loss Visible
Meter air flow and electrical power at compressor level if possible. Without them, savings from repairs cannot be proven.
Keep Leak Repairs and Compressor Service on Schedule
Log every compressed air leak, schedule filter and cooler service, and track compressor history with Oxmaint.
Leak Management as a Maintenance Workflow
Leak surveys find leaks, but repairs happen only when each leak becomes a tracked task. Treat the process as a cycle, not a one-off audit.
Maintenance Analytics for Compressors
Compressor data is usually available from controllers, meters, and SCADA. Trend a few indicators per machine and look for gradual drift.
| Indicator | What a change may mean | Typical action |
|---|---|---|
| Specific power rising | Leaks, fouling, control problems, or internal wear | Compare with leak survey and cooler data, then inspect |
| Discharge temperature rising | Cooler fouling, oil or cooling problem, airflow restriction | Clean coolers, check oil and ventilation |
| Filter differential pressure rising | Clogged air or oil separator filters | Replace by condition instead of fixed time alone |
| Vibration or bearing temperature rising | Bearing or drive-end problems | Inspect, lubricate, plan bearing work |
| More frequent starts and stops | Control or sizing issue, demand swings | Review control settings and storage capacity |
| Condensate drain activity abnormal | Drain stuck open or blocked | Service drain and check downstream moisture |
Combine data with context
- Compare readings across similar compressors in the same room.
- Adjust for ambient temperature and plant load before judging a trend.
- Link every anomaly to inspection and repair outcomes, so thresholds improve.
- Review cumulative running hours alongside service dates.
- Keep a log of settings changes, since an energy shift may come from a controller adjustment rather than a mechanical fault.
- Flag compressors whose specific power is worse than the others in the same room for early inspection.
Preventive Maintenance Calendar for Compressed Air
| Interval | Compressors | Dryers and filters | Distribution system |
|---|---|---|---|
| Daily or each shift | Check pressure, temperature, alarms, unusual noise | Check drain operation and dryer status | Walk for audible leaks |
| Weekly | Check oil level and cooling airflow | Check filter differential pressure | Check hoses and quick couplings in work areas |
| Monthly | Clean coolers and ventilation paths | Inspect and test automatic drains | Spot-check ultrasonic readings in high-use zones |
| Quarterly | Check belts, couplings, and mounting | Replace filter elements by condition | Review leak tags and open repairs |
| Annually or by hours | Oil and separator service, inspect valves and bearings | Service dryers and calibrate sensors | Full ultrasonic leak survey and pressure profile review |
Adjust intervals for dust levels. Plants with heavy dust load need shorter cooler and filter cycles than clean-air sites.
Before and After: A Managed Compressed Air System
- Leaks tolerated until noise is obvious
- Pressure raised to cover unexplained drops
- Filters changed on a fixed date regardless of condition
- Coolers cleaned only after high temperature trips
- No record linking repairs to energy results
- Leaks surveyed, tagged, and repaired on a schedule
- Pressure set from measured requirements
- Filters replaced by differential pressure
- Cooler cleaning scheduled by trend
- Energy and repair results recorded together
How Oxmaint Supports Compressor and Air System Maintenance
Oxmaint is maintenance management software. It organizes the maintenance side of compressed air management, while meters and analytics provide the energy measurements.
- Asset records for compressors, dryers, receivers, filters, and key distribution assets, with service history.
- Preventive maintenance schedules by hours, calendar date, or condition reading.
- Inspection checklists for pressure, temperature, drain operation, and leak walkdowns.
- Work orders for every leak tag and compressor repair, with parts and labor recorded.
- Inventory for filter elements, separators, belts, and drain valves.
- Reports on repeat failures, overdue tasks, and maintenance cost by compressor.
Prioritizing Compressor Actions by Effect
Baghouse Cleaning Air: A Large Demand Worth Tuning
Pulse-jet baghouses fire solenoid valves on a timer or on differential pressure. If the settings are conservative, they use more air than the filters need.
- Review cleaning pressure and pulse interval against actual filter differential pressure.
- Clean on demand, not only on a timer, where the system supports it.
- Check diaphragm valves and solenoids, since a leaking valve wastes air continuously.
- Inspect bags and cages, because damaged filters raise differential pressure and cleaning frequency.
- Record any setting change in the work order history so results can be compared with energy data.
Changes must keep emissions compliance and dust control intact. Verify with the environmental team before adjusting cleaning cycles.
Pressure Setpoints and Artificial Demand
Raising system pressure to overcome pressure drop increases the flow through every leak and every unregulated use. Lowering it is only safe when the real requirement is known.
- One critical user once needed more pressure
- Pressure drop across dirty filters never fixed
- Poor piping that starves far points
- No record of actual minimum pressure per user
- Measure the minimum pressure each major user needs
- Fix filters, dryers, and piping restrictions first
- Lower setpoints in small steps and monitor
- Document the final setpoint and who approved it
Compressor Room Environment and Heat
| Condition | Effect | Maintenance response |
|---|---|---|
| Hot, poorly ventilated room | Higher inlet temperature, lower efficiency, more trips | Clear ventilation paths, check fans and ducts |
| Dust in the room | Fouled coolers and filters, faster wear | Clean on a schedule and improve filtration |
| Oil leaks and condensate puddles | Safety risk and environmental issues | Repair leaks and check condensate handling |
| Poor access to machines | Service tasks are skipped or delayed | Clear access and label service points |
Heat from compressors can sometimes be reused for space or process heating. Evaluate it only after basic leak and maintenance losses are controlled.
Measuring Savings From Maintenance Actions
Energy projects lose support when savings cannot be shown. Use a simple measurement approach from the start.
- Record baseline power, air flow, and pressure before any repair campaign.
- Note the date and scope of each action in the work order.
- Compare power and flow after the action under similar production conditions.
- Adjust for production level, ambient temperature, and number of compressors running.
- Report the result in energy and cost, and keep it with the maintenance record.
Even a basic before-and-after comparison, with the conditions documented, is more convincing than an estimate.
Safety and Compliance in Compressed Air Maintenance
- Depressurize and lock out systems before opening components, and verify zero pressure.
- Inspect pressure vessels, safety valves, and gauges according to local regulations and insurer requirements.
- Keep records of inspections and certificates, and attach them to the asset.
- Prohibit using compressed air to clean clothing or skin, and control blow-down practices.
- Manage condensate and oil waste according to environmental rules.
- Check hose whip restraints and couplings, since failed connections can injure people.
- Train maintenance and production staff on the hazards of stored pressure, and refresh the training regularly.
- Include compressed air systems in management of change reviews whenever new equipment or air users are added.
Storing inspection records against each vessel and valve simplifies audits and avoids missed statutory checks.
Trends in Cement Compressed Air Management
- Metering at area level: plants add flow meters to see which areas and processes use the most air.
- Ultrasonic imaging tools: newer detectors can locate leaks quickly, even in noisy plants.
- Variable speed and central controllers: better control reduces unloaded running and pressure swings.
- Energy management standards: structured energy programs include compressed air as a significant energy use.
- Condition-based service: sensor data replaces some fixed-interval filter and cooler tasks, which cuts unnecessary changes while catching fouling earlier.
- Integrated reporting: energy, maintenance, and production data are increasingly reviewed together in one monthly performance meeting.
Running Your First Leak Survey
- Choose a quiet period, such as a planned stop, when background noise is low.
- Cover one area at a time and record the location of every leak found.
- Estimate the size category of each leak, and mark the highest-loss leaks as first priority.
- Tag each leak physically and create a matching work order.
- Plan repairs by area to reduce travel time and the need for repeated isolation.
- Re-survey after repairs and compare air consumption during stoppage with the baseline.
Most leaks come from small fittings, hoses, couplings, and valves, so keep common spares ready to fix them on the spot.
KPIs for Compressed Air Reliability and Energy
| KPI | Purpose |
|---|---|
| Specific power by compressor | Tracks efficiency drift over time |
| No-production air consumption | Estimates leak load |
| Open leak tags and average age | Shows repair backlog |
| Filter and cooler cleaning compliance | Confirms preventive work is done |
| Unplanned compressor downtime | Measures reliability |
| Maintenance cost per compressor | Supports repair or replace decisions |
Compressor Energy and Maintenance Questions
Stop Paying for Air That Never Does Work
Make leak repairs, filter changes, and compressor service visible and scheduled. Use Oxmaint to keep every compressed air task on track.