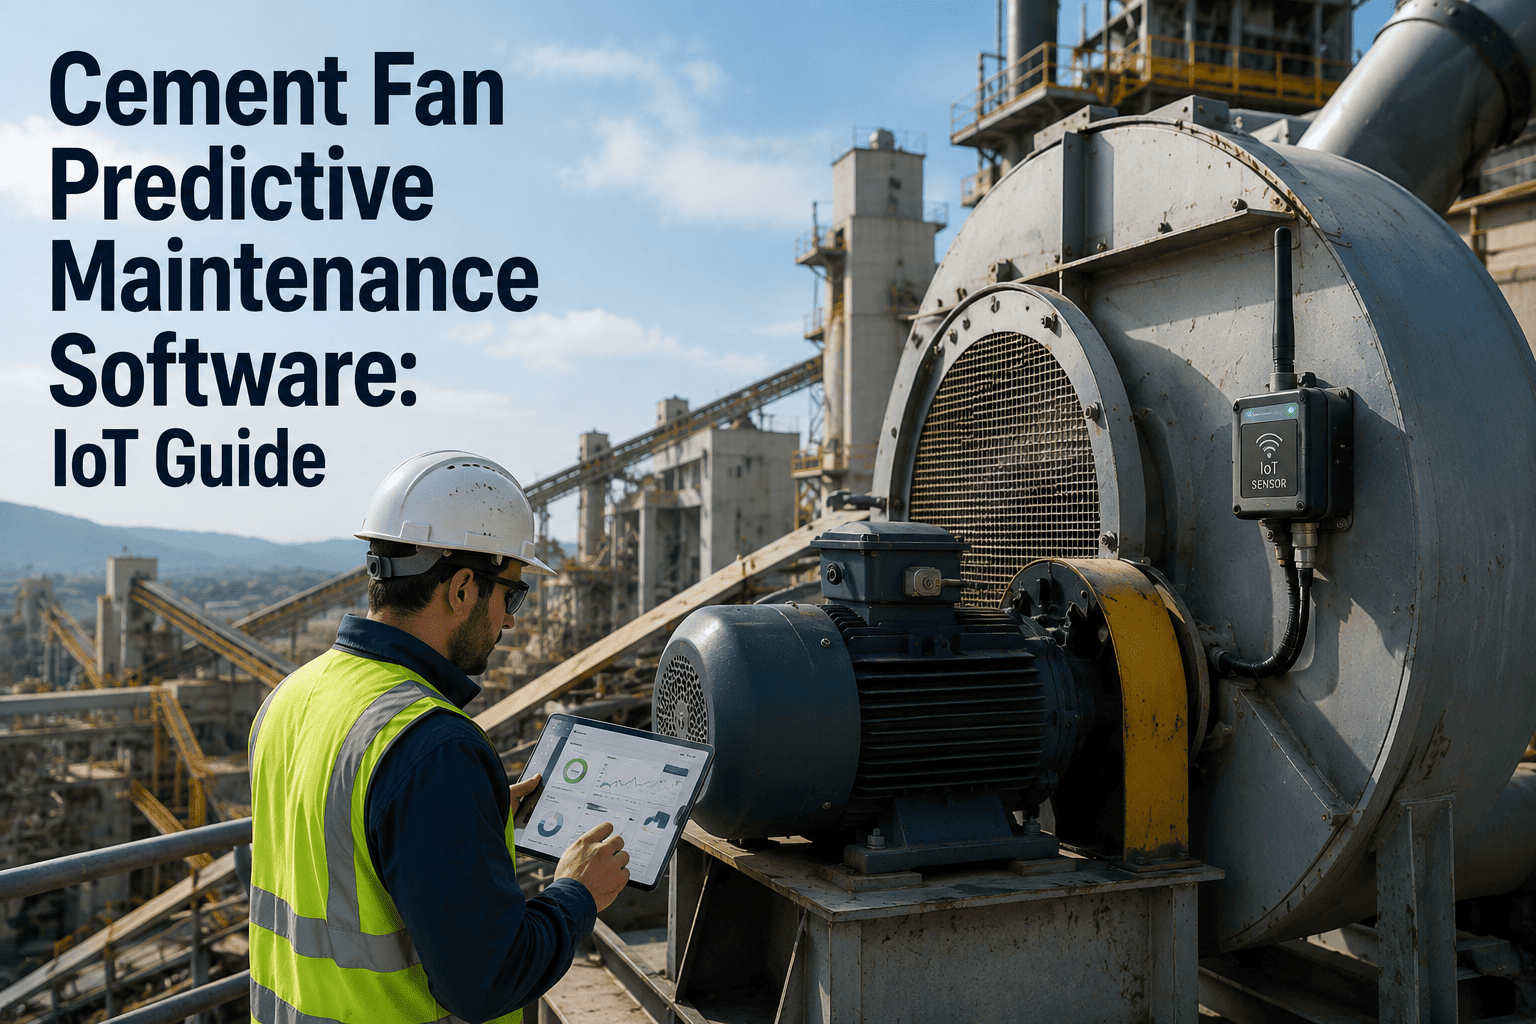
Cement plants lose more unplanned production hours to fan failures than to almost any other class of rotating equipment on site. ID fans, PA fans, cooler fans, and dust collector fans run continuously under heavy dust loading, high temperatures, and constant shock-loading, and those conditions wear bearings and blades long before a control room alarm ever fires. Most plants still rely on scheduled inspections or a technician walking the floor once a week with a handheld vibration meter, so an early-stage bearing defect can progress for days before anyone notices it. Predictive maintenance software paired with continuous IoT sensors closes that gap, turning a fan's vibration, temperature, and current signature into 4 to 8 weeks of advance warning instead of a shutdown notification. This guide breaks down how cement fan predictive maintenance actually works, which failure modes it catches first, and how a connected CMMS turns raw sensor data into a scheduled work order rather than an emergency callout — or you can book a 30-minute session with our team to see it against your own fan fleet.
Predictive Fan Maintenance
Cement Fan Predictive Maintenance Software: The IoT Guide
Cooler fans, ID fans, PA fans, and dust collector fans give off warning signs weeks before they trip. Here is how CMMS and IoT sensors catch them in time.
4-8 wks
Typical early warning window
38-44%
Of fan trips traced to bearing failure
90%+
Of developing faults visible in vibration data
Why Cement Fans Fail More Often Than Any Other Rotating Asset
Cooler fans pull hot clinker air, ID fans handle abrasive kiln exhaust, PA fans push preheated air through raw mill circuits, and dust collector fans run against a constant load of fine cement dust. Every one of them is exposed to conditions that accelerate wear far beyond what a standard industrial fan experiences.
Bearing Contamination
Dust Ingress Through Worn Seals
Fine cement dust works past degraded shaft seals and mixes into bearing grease, turning it into an abrasive paste. This single cause is behind the largest share of fan bearing failures across cement plants.
Blade Imbalance
Uneven Material Build-Up
Sticky clinker dust and fly ash deposit unevenly across fan blades, shifting the center of gravity away from the rotational axis. Even a small asymmetric deposit generates forces strong enough to damage bearings over a few weeks.
Thermal Misalignment
Shaft Movement
Repeated heating and cooling cycles on cooler and ID fans cause thermal growth in shafts and housings, gradually shifting alignment and generating vibration at twice the running speed.
Abrasive Erosion
Impeller and Housing Wear
Kiln exhaust and raw mill air streams carry abrasive particulate that thins impeller blades and casing walls over time, changing airflow efficiency long before the fan shows an obvious fault.
Which Fans Need Predictive Monitoring First
Not every fan in a cement plant carries the same risk. This breakdown ranks the four fan families by failure impact and shows what a predictive program should watch on each one.
| Fan Type |
Typical Failure Mode |
Downtime Impact |
Primary Sensor Signal |
| ID Fan |
Bearing spalling, blade imbalance from ash build-up |
Halts kiln exhaust — full line stop |
Vibration spectrum, bearing temperature |
| Cooler Fan |
Thermal shaft misalignment, seal degradation |
Reduces clinker cooling capacity |
Vibration phase, motor current |
| PA Fan |
Dust ingress into bearings, impeller erosion |
Slows raw mill throughput |
Vibration amplitude, oil condition |
| Dust Collector Fan |
Bag-house dust loading, motor overheating |
Triggers environmental compliance risk |
Motor current, differential pressure |
ID fans and cooler fans carry the highest downtime cost because both sit directly in the pyroprocessing line — a trip on either one stops clinker production, while a PA fan or dust collector issue is usually a slower, throughput-limiting event.
Not sure which of your fans is closest to failure? OxMaint's predictive maintenance module ranks every monitored fan by risk score, so your team always knows which work order to schedule next.
How Cement Fan Predictive Maintenance Actually Works
Predictive maintenance is not a single sensor or a single alarm. It is a workflow that takes raw signal data and turns it into a scheduled repair before the fan ever trips. Here is how that workflow runs inside OxMaint.
1
Sensors capture continuous baseline data
Vibration, bearing temperature, motor current, and airflow sensors record readings around the clock instead of during a weekly walk-down. The system establishes a healthy baseline for each fan during its first weeks of normal operation.
2
Algorithms flag deviation from baseline
When vibration amplitude at running speed rises, or bearing temperature trends upward against load, the platform flags the deviation and classifies the likely fault — imbalance, misalignment, or bearing defect — based on the frequency pattern.
3
CMMS auto-generates a ranked work order
Instead of a raw alert sitting in a dashboard, OxMaint creates a work order with the suspected fault, recommended inspection steps, and a priority ranking based on how close the fan is to its failure threshold.
4
Technician confirms and schedules the fix
A technician reviews the flagged fan during a normal round, confirms the finding, and the repair gets slotted into the next planned stop instead of forcing an emergency shutdown mid-shift.
5
Post-repair baseline resets automatically
Once the fan is repaired, OxMaint resets the baseline to reflect the new condition of the equipment, so the same fault does not trigger a false alert again next month.
The IoT Sensor Stack Behind Every Prediction
A predictive maintenance program is only as good as the data feeding it. These are the sensor types that give the clearest early signal on cement plant fans.
Signal Type
Vibration Sensors
Accelerometers mounted at the drive-end and non-drive-end bearing housings capture amplitude and frequency data. A rise at running speed signals imbalance; a rise at twice running speed signals misalignment; sub-synchronous energy signals bearing cage wear.
Signal Type
Bearing Temperature Probes
Continuous temperature tracking against the fan's normal operating curve catches lubrication breakdown and early-stage bearing distress that vibration alone can miss during slow-developing faults.
Signal Type
Motor Current Signature
Subtle changes in current draw reveal rotor bar faults, stator winding degradation, and mechanical load changes on the fan shaft — often weeks before the issue is visible on a vibration spectrum.
Signal Type
Differential Pressure Sensors
On dust collector fans, a rising pressure drop across the bag-house signals filter loading or airflow restriction that will eventually overload the fan motor if left unaddressed.
What a Predictive Fan Program Should Deliver
These are the numbers plant managers track once a predictive maintenance program is running on the fan fleet. Set targets for each of these from the first month of deployment.
0
Unplanned ID fan or cooler fan trips
The target for line-critical fans is zero unplanned trips once continuous monitoring and alert-to-work-order automation are fully in place.
6-14 wk
Detection window for bearing defects
Early-stage bearing degradation is typically visible in vibration data 6 to 14 weeks before a defect would otherwise cause a shutdown.
>90%
Planned maintenance completion rate
A healthy predictive program pushes 90 percent or more of fan work orders into planned stops rather than reactive, unscheduled repairs.
100%
Sensor and calibration uptime
Every monitored fan should have continuous sensor coverage with no calibration gaps, since a blind spot on a critical fan defeats the purpose of the program.
Frequently Asked Questions
How early can predictive software detect an ID fan bearing fault?
Continuous vibration monitoring typically flags early-stage bearing spalling 6 to 14 weeks before it would cause a trip, giving maintenance teams time to schedule the repair during a planned stop.
Book a session to see detection timelines for your own fans.
What sensors does a cement fan predictive program actually need?
Vibration accelerometers and bearing temperature probes cover most fault types, while motor current sensors add coverage for electrical and rotor issues. Dust collector fans also benefit from differential pressure sensors.
See supported sensor integrations in OxMaint.
Can predictive maintenance replace scheduled fan inspections completely?
No. Predictive monitoring catches developing faults between inspections, but physical checks for seal condition, bolt torque, and visible blade wear still belong in the maintenance calendar alongside sensor data.
Which cement plant fan fails most often?
ID fans and PA fans see the highest failure rates because they run continuously against dust-loaded, high-temperature air streams, and bearing failure is the leading cause across both fan types.
How does OxMaint turn a sensor alert into a work order?
When a sensor reading crosses its threshold, OxMaint classifies the likely fault, ranks it by urgency, and auto-generates a work order with recommended inspection steps for the assigned technician.
Sign up free to try it on your fan fleet.
Give Your Fans the Warning System They Deserve
OxMaint combines IoT vibration and temperature sensors with an automated CMMS workflow so your ID fans, PA fans, cooler fans, and dust collector fans get flagged weeks before they fail — not the day they trip.