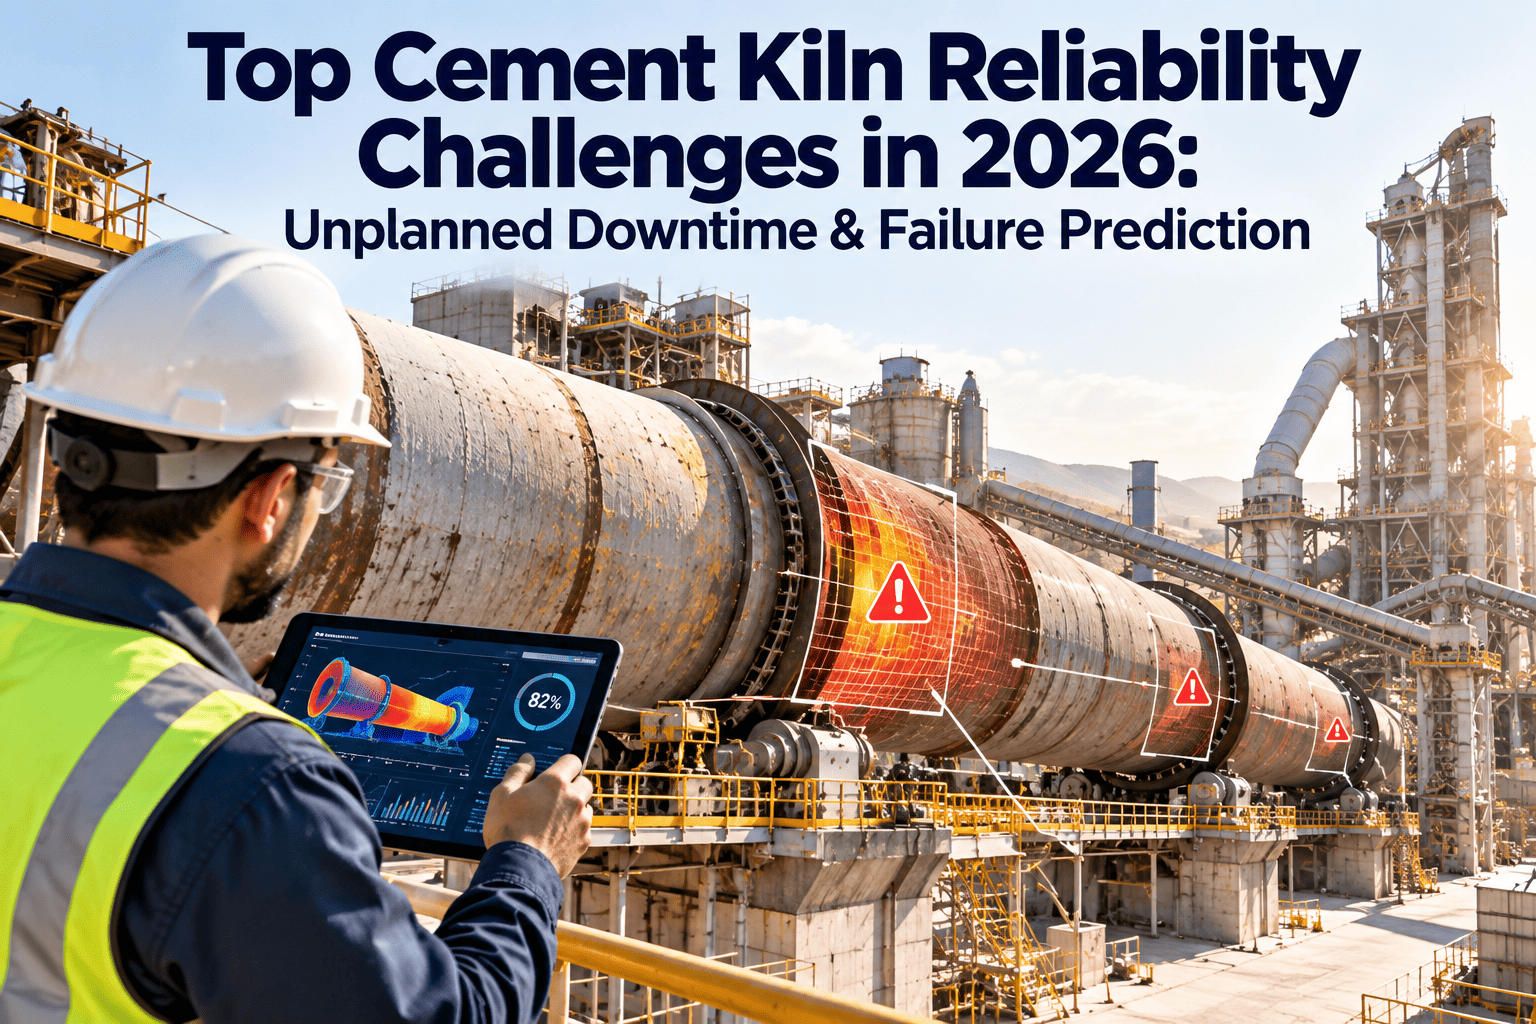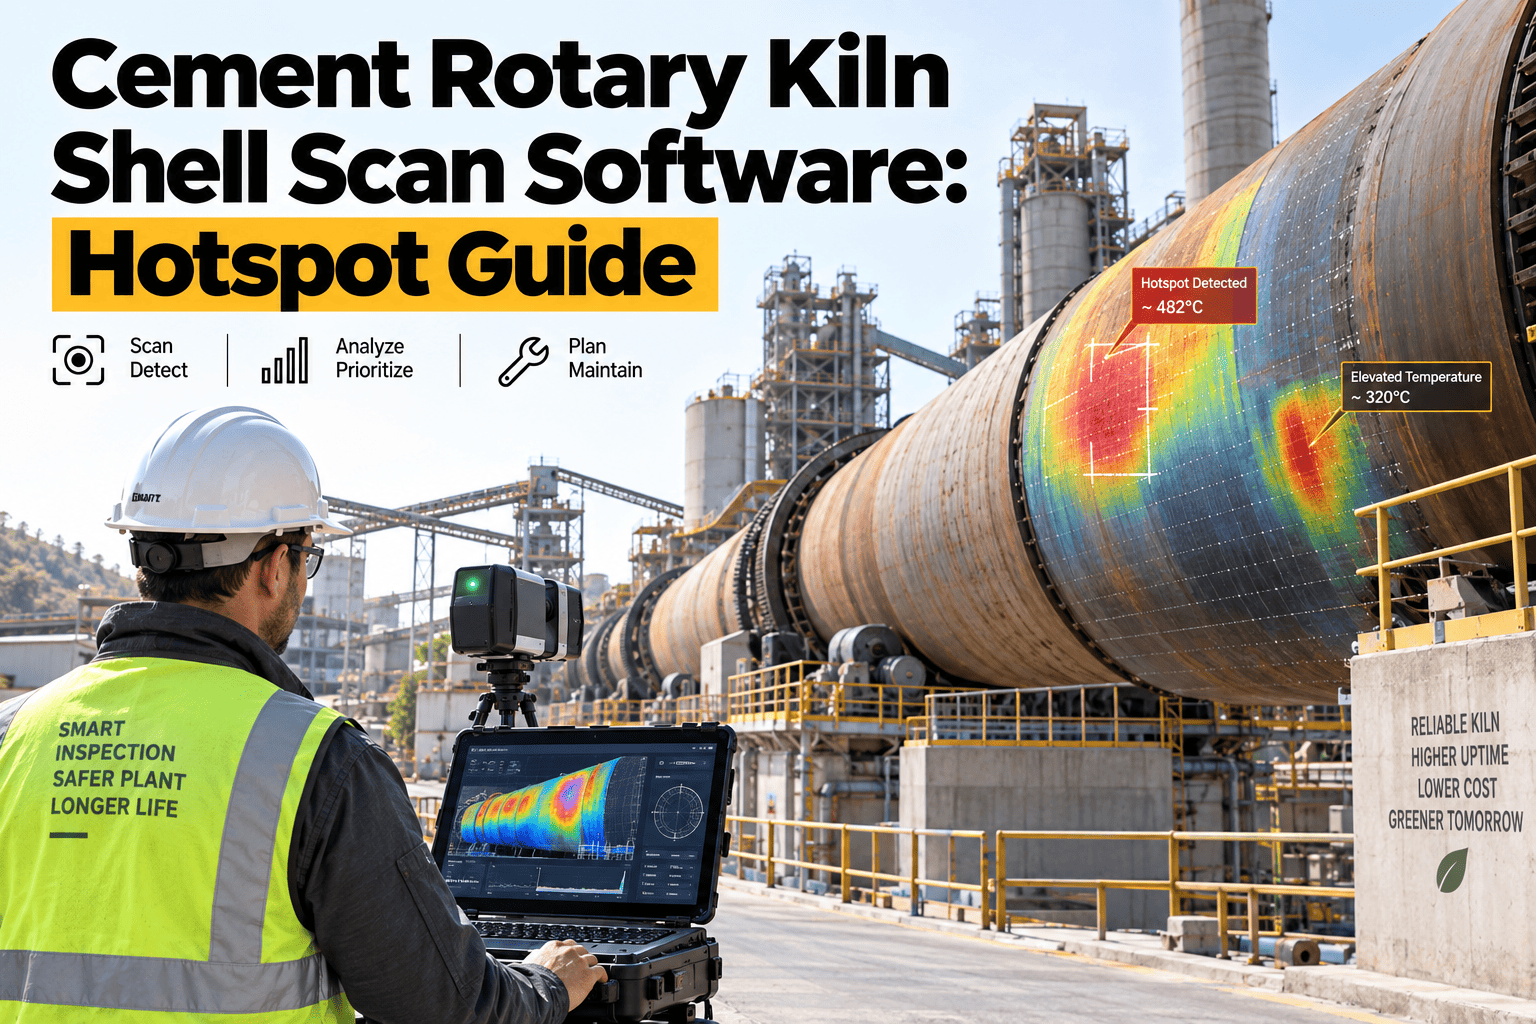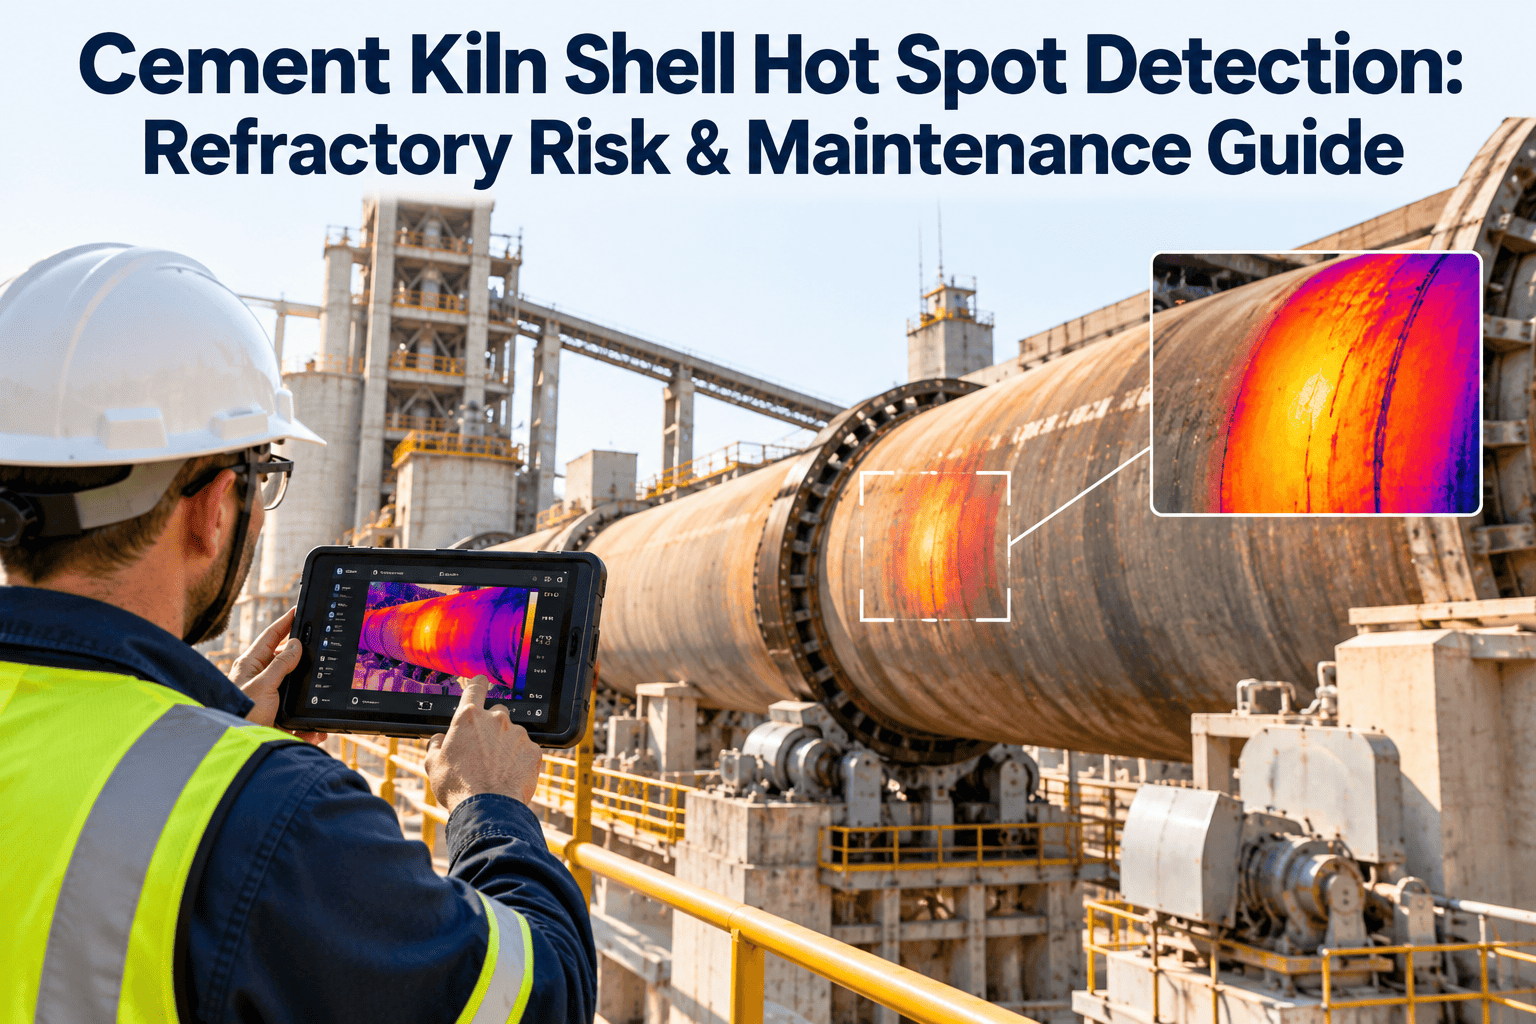
A cement kiln shell is steel plate doing a job it was never designed to do on its own — holding its shape at 1,450°C of internal process heat with nothing but a 200–250mm refractory lining standing between the flame and the metal. When that lining thins, cracks, or spalls away in one localized patch, the shell underneath starts absorbing heat directly, and a hot spot is born. Left undetected, a hot spot does not stay a maintenance note; it becomes a forced kiln stop, a multi-week reline, and a production hole that can run into seven figures. This guide walks through how hot spots actually form, why they are so often caught too late, and what a structured detection and maintenance workflow looks like when it is built around a CMMS rather than a clipboard. If your kiln reliability program is still leaning on once-a-shift handheld readings, Oxmaint's scanning and work order workflow is worth a look before your next campaign.
Kiln Reliability · Refractory Risk
Cement Kiln Shell Hot Spot Detection & Refractory Risk
How thinning refractory turns into a shell hot spot, why manual patrol readings miss the early window, and how a scan-to-work-order maintenance workflow keeps a developing hot spot out of red-kiln territory.
Why the Shell Is the Last Warning, Not the First
By the time a shell hot spot is visible to the naked eye, the refractory brick behind it has usually already failed. The shell is the last line of defense, not the first sign of trouble — which is exactly why plants that rely on visual patrol inspection alone tend to discover damage only after it has become an emergency rather than a planned repair.
How a Hot Spot Actually Develops
Refractory wear is rarely sudden. It progresses through a fairly predictable sequence driven by thermal cycling, clinker abrasion, alkali attack, and coating loss — and each stage narrows the window for an affordable fix.
Detection Methods, Compared
Plants generally rely on some combination of handheld pyrometer patrols, periodic infrared scanning, and continuous thermal monitoring. Each has a different blind spot, and understanding those gaps matters more than picking a single "best" method.
| Method | Typical Interval | Main Strength | Main Blind Spot |
|---|---|---|---|
| Handheld pyrometer patrol | Once per shift or less | Low cost, no new hardware | Misses gradual drift between readings; operator-dependent |
| Fixed-point infrared scanner | Weekly circumferential scan | Structured baseline across full circumference | Days pass between scans; a fast-developing zone can be missed |
| Continuous thermal imaging | Every rotation, ongoing | Trend and rate-of-change visibility | Requires camera calibration and dust/moisture-tolerant optics |
| Manual visual/color inspection | Ad hoc, daylight only | Zero equipment cost | Only catches damage that is already advanced (glow, discoloration) |
Root Causes Behind Most Refractory Failures
Hot spots rarely appear at random. A handful of recurring conditions account for most of the damage a reline crew finds when they finally open up a section of shell.
- Thermal cycling from frequent stop-startsRepeated heating and cooling stresses brick joints faster than continuous operation, especially near burner-pipe and kiln-inlet zones.
- Alkali, sulfate, and chloride attackVolatile compounds condense in cooler zones and chemically erode brick from the inside, a mechanism that accelerates with certain alternative fuel and raw mix chemistries.
- Mechanical abrasion from clinker flowCoarse or unstable clinker nodules scour brick faces in the burning and transition zones over time.
- Coating instabilityA stable clinker coating is itself a protective layer; when flame shape, kiln speed, or feed chemistry destabilizes it, the underlying brick is exposed directly to process heat.
- Shell ovality and misalignmentTyre and roller wear that lets the shell flex out of round opens joints in the brick ring, giving heat a path to the steel.
Turn Scan Data Into a Scheduled Work Order, Not a Post-It Note
A hot spot flagged on a Tuesday scan is only useful if it reaches a planner before Friday. Oxmaint connects kiln shell readings, thresholds, and refractory history to a single work order pipeline so nothing sits unassigned.
Building a Weekly Shell Scanning Routine
Consistency matters more than sophistication. A plant running a disciplined weekly scan with clear thresholds will typically outperform one with expensive sensors and no follow-through process. The routine below is a practical baseline most kilns can adopt regardless of current instrumentation.
- Define baseline zones. Break the shell into fixed circumferential and axial segments so every scan compares the same points over time, not a rough visual sweep.
- Scan on a fixed cadence. Weekly is a reasonable minimum for most kilns; zones with a known wear history may justify a tighter interval.
- Set differential thresholds, not just absolute ones. A 40–50°C jump above a zone's own baseline is often a stronger early signal than a single absolute temperature reading.
- Route flagged readings into a work order automatically. Manual handoff between the person taking the reading and the person who schedules the repair is where most delays happen.
- Log every reading against asset history. A single scan tells you today's condition; a logged trend tells you how fast a zone is deteriorating and how much time you actually have.
What a Ready Repair Package Looks Like
Catching a hot spot early only pays off if the repair itself is ready to execute during the next available stop. A prepared refractory work order typically has brick type and quantity specified, crew and duration estimated, and the outage window coordinated with the kiln stop — so the fix happens on a planned schedule instead of an emergency one.
- Damage found during a walk-through, after it is already visible
- Brick and crew sourced under time pressure
- Kiln stopped without a planned window
- Repair scope discovered on site, not before
- Zone flagged from trend data days or weeks ahead
- Brick, tools, and crew staged before the stop
- Repair aligned to an existing planned outage
- Scope and duration estimated in advance
How Oxmaint Supports Shell and Refractory Reliability
Oxmaint gives kiln reliability teams a single place to log shell readings, track refractory campaign life, and turn a threshold breach into a scheduled work order without the reading sitting in someone's notebook.
- Zone-based reading logRecord shell temperatures against fixed circumferential zones so every scan is comparable to the last one, not a fresh guess.
- Threshold-triggered work ordersSet differential and absolute temperature thresholds that automatically generate a work order the moment a reading crosses them.
- Refractory campaign historyTrack brick type, install date, and repair history per zone so a planner can see whether a hot spot is a fresh issue or a known weak point.
- Mobile inspection captureTechnicians log readings from a handheld device during rounds, with photos and notes attached directly to the asset record.
- Outage-aligned schedulingCoordinate refractory repair windows against the same kiln stop calendar used for other planned maintenance, so access is negotiated once.
- Reporting and trend dashboardsReview shell temperature trends by zone over weeks or months to separate normal wear from an accelerating problem.
Frequently Asked Questions
What shell temperature indicates a refractory problem?
Normal burning-zone shell temperature is commonly in the 200–280°C range depending on kiln design and lining thickness. A reading that climbs well above a zone's own established baseline, or shows a sharp differential against neighboring zones, is a stronger early signal than any single absolute number.
How often should kiln shell scanning happen?
A weekly full-circumference scan is a reasonable baseline for most kilns, with more frequent checks on zones that have a known wear history. Book a demo to see how zone-based scheduling works inside a CMMS.
Why does manual patrol inspection miss developing hot spots?
A single reading per shift cannot capture a gradual temperature drift between checks, and visual inspection alone typically only catches damage once it is already advanced enough to show color change or glow.
What causes shell hot spots besides refractory age?
Thermal cycling, alkali and chloride attack, coating instability, clinker abrasion, and shell ovality from tyre or roller wear are the most common contributing factors alongside simple brick age.
Can hot spot repairs be scheduled instead of handled as emergencies?
Yes, if the zone is flagged early enough from trend data. A repair identified days or weeks ahead can be scoped, staged, and aligned to an existing planned stop instead of forcing an unplanned shutdown. Sign up for Oxmaint to connect scanning data to scheduled work orders.
Scan · Trend · Schedule
Catch the Drift Before It Becomes a Red Shell
A hot spot caught at stage one is a line item on next month's planned stop. A hot spot caught at stage four is a multi-week reline. Oxmaint gives your kiln reliability team the zone tracking, thresholds, and work order routing to make sure every scan actually leads somewhere.