Most cement plants know how many hours the kiln stopped, but far fewer can say what those hours cost or why they happened in a way that holds up in a budget meeting. Without a consistent cost method and loss codes, downtime becomes a list of stories instead of data. This guide gives maintenance and operations teams a practical way to calculate downtime cost, code every loss, and rank the problems worth fixing, supported by a cement plant CMMS that keeps the records in one place.
Cement Plant Downtime Cost Calculator and Loss Coding
Put a defensible number on every stoppage, then classify it with a loss code so repeat causes stand out and maintenance budgets follow evidence.
Why Downtime Cost Stays Unclear
- Production, maintenance, and finance each record stoppages in their own way.
- Operators log a stop as "mechanical" or "process" with no detail about the cause.
- Short stops of a few minutes are rarely recorded, yet they add up over a month.
- Kiln stoppages carry restart costs, such as extra fuel and process instability, that never appear on a repair work order.
- Whether lost output was truly lost or recovered later is rarely agreed.
What an unclear number costs the plant
- Maintenance requests for spares and upgrades lose to projects with clearer payback.
- Chronic small losses stay hidden behind a few dramatic breakdowns.
- Different sites cannot compare performance because they count differently.
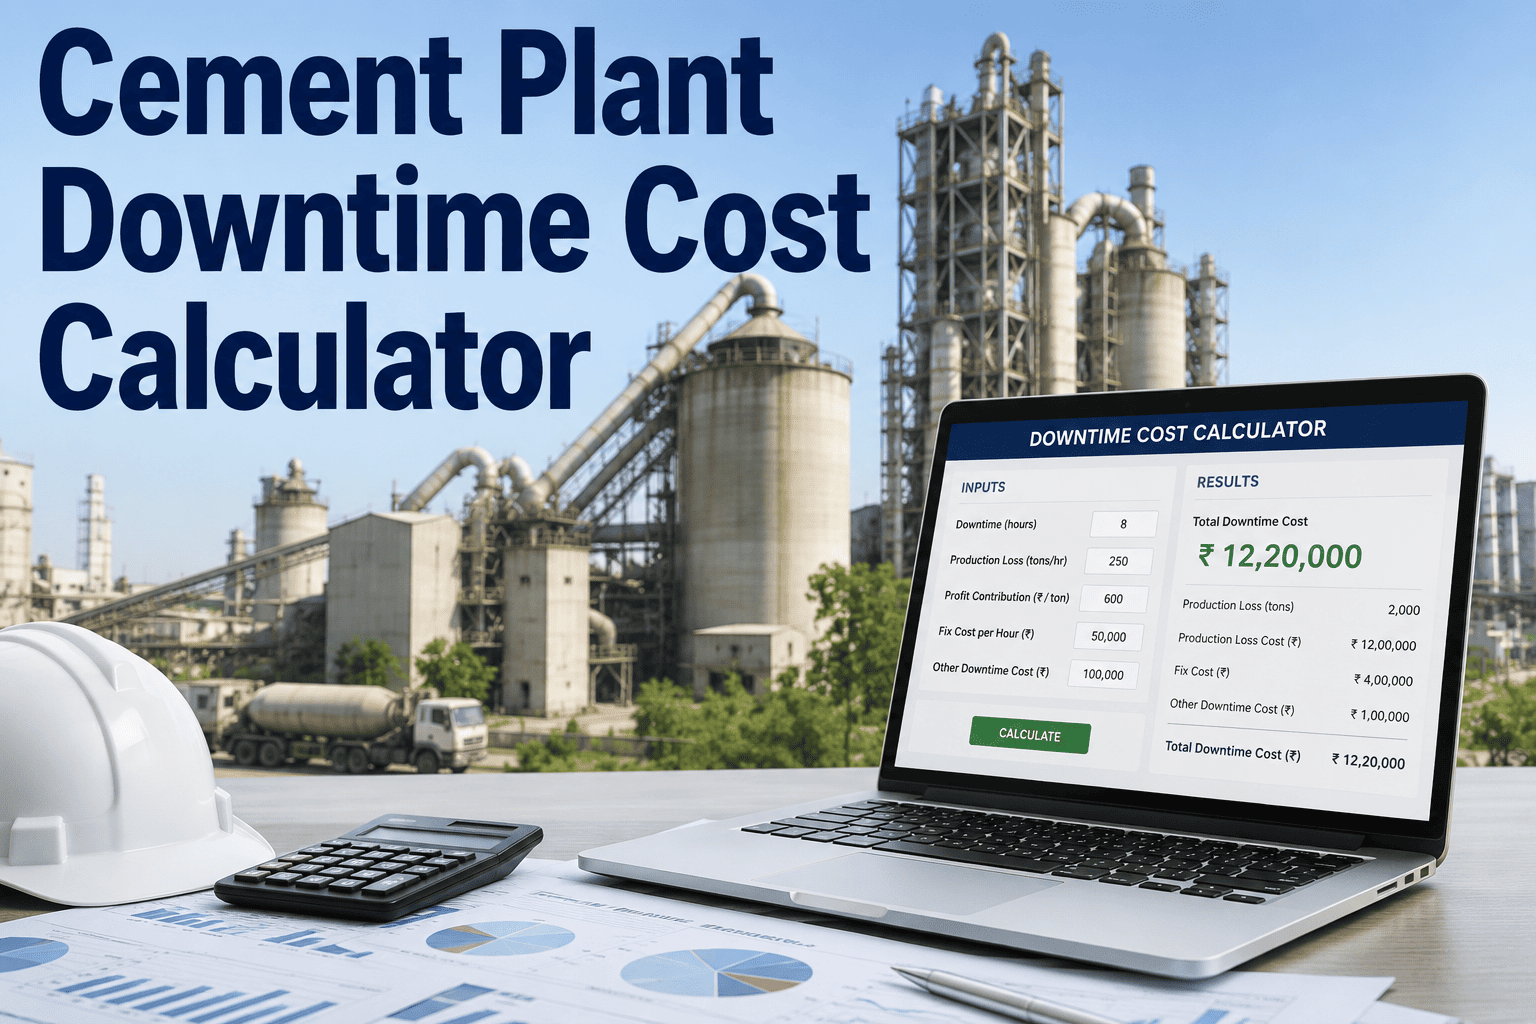
Step 1: Build the Downtime Cost Worksheet
Use one worksheet structure for every stoppage. Agree on each input with finance before the first use.
| Cost Element | How to Calculate | Who Provides It |
|---|---|---|
| Lost production value | Stop hours x rated hourly output x agreed value per tonne | Production and finance |
| Maintenance labor | Hours on the work order x labor rate, including contractors | Maintenance |
| Parts and materials | Issued spares and consumables from the work order | Stores |
| Restart and recovery | Extra fuel, power, and quality loss during return to steady running | Process engineering |
| Secondary effects | Idle labor, missed dispatch, penalties, or outsourced supply | Operations and sales |
| Recovery credit | Output later recovered from stock or extra running, subtracted | Production planning |
Agree the value per tonne carefully
- Use contribution margin when the plant is sold out, and lost sales are real.
- Use a lower value when stock buffers absorb the stop.
- Document the choice so results stay comparable over time.
Worked Example With Illustrative Numbers
The figures below are invented for demonstration and do not represent any real plant. Replace them with your own rates.
Step 2: Design a Loss Coding Tree
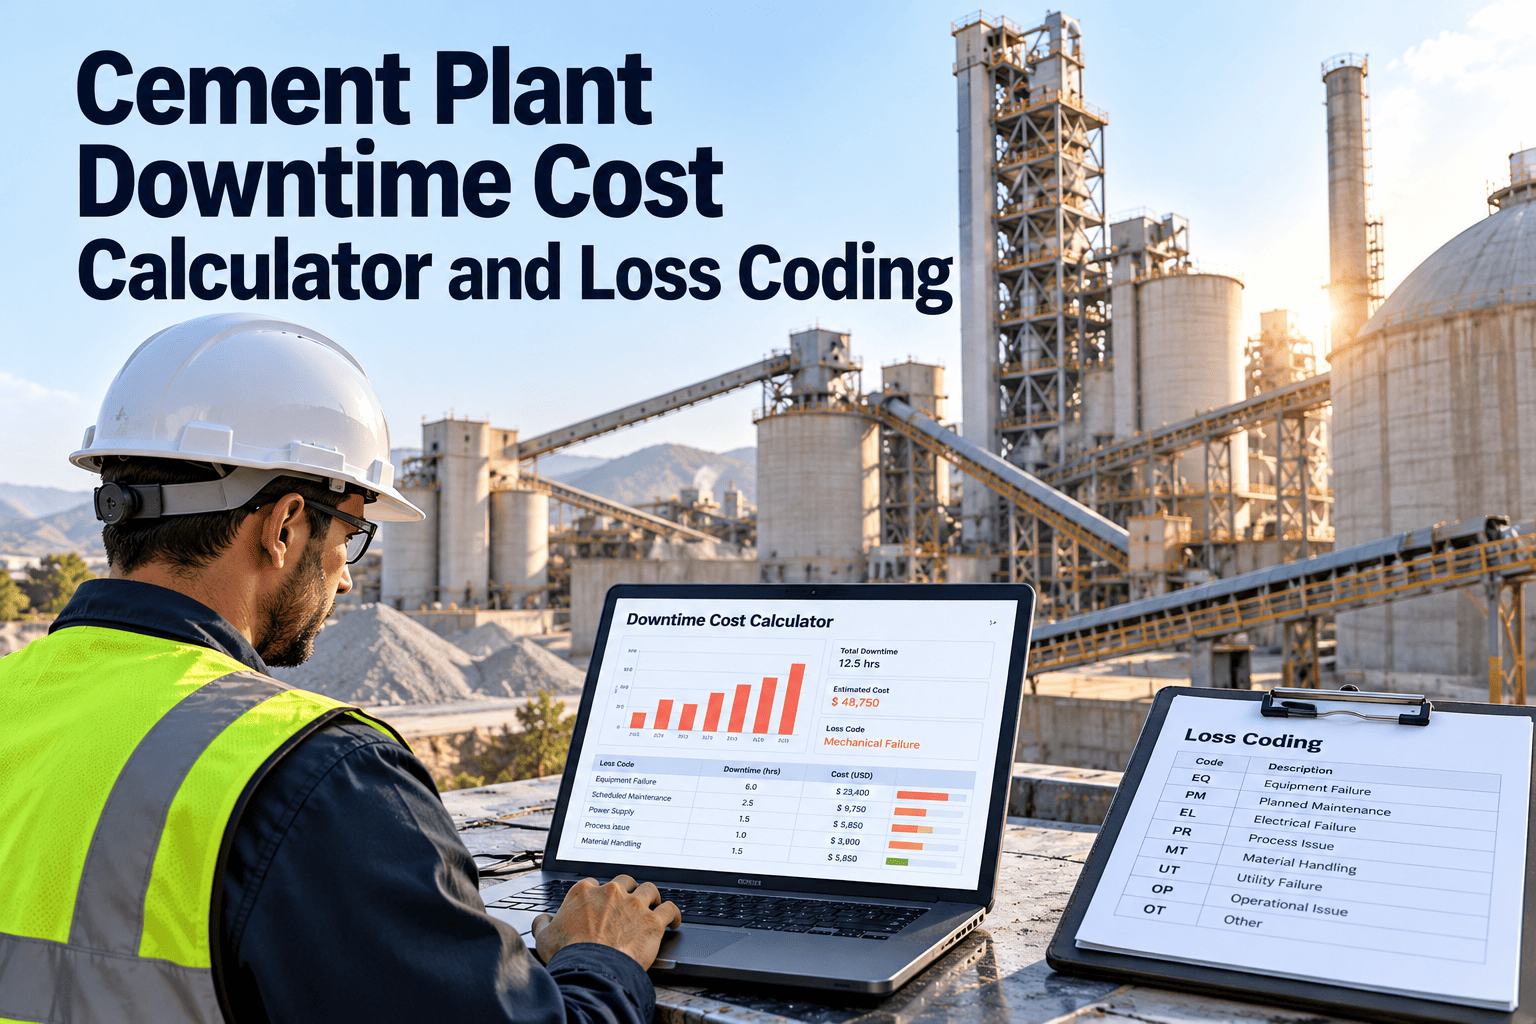
A loss code answers one question: why did output stop or slow? Keep the tree shallow so operators actually use it.
- Scheduled shutdown
- Refractory work
- Planned changeover
- Mechanical
- Electrical
- Instrumentation
- Wear part failure
- Kiln instability
- Coating or buildup
- Quality hold
- Power interruption
- Raw material shortage
- Market or dispatch
Rules that keep coding trustworthy
- One stop, one primary code. Secondary notes go in the description.
- Codes describe the cause, not the symptom. "Motor tripped" is a symptom; "bearing failure" is a cause.
- Every code has a written definition and an owner.
- Avoid an "other" bucket that grows beyond a small share of total time.
Step 3: Capture Stops Where They Happen
Know What Every Stoppage Really Costs
Link stops, loss codes, work orders, and spare parts in one record, so downtime cost is calculated from data instead of estimates.
Step 4: Rank Losses to Decide Where to Act
Once codes and costs are attached, sort by total cost and by frequency. The two lists often differ.
Before and After: Downtime Reporting
- Monthly summary shows total hours only
- Repair costs and lost output are reported separately
- Causes are argued, not proven
- Budget requests rely on opinion
- Every event has a code, duration, and cost
- Top loss causes ranked by value
- Repeat failures visible by asset
- Investment cases backed by event history
KPIs to Report From Coded Downtime
Where Oxmaint Supports the Method
Oxmaint maintenance management software keeps the maintenance side of the calculation reliable, including labor, parts, and history.
| Method Step | Software Capability |
|---|---|
| Identify the failed asset | Asset management with a structured hierarchy |
| Record the repair | Work orders with labor hours, parts, and failure codes |
| Capture field findings | Mobile workflows for technicians and operators |
| Prevent repeat losses | Preventive maintenance and inspection scheduling |
| Know spare availability | Inventory tracking for critical parts |
| Report and rank causes | Dashboards and reports on downtime, backlog, and repeat failures |
Implementation Checklist
- Agree value per tonne and recovery rules with finance
- Publish a short loss code list with definitions
- Train operators and shift leaders on code selection
- Link stop events to work orders in one system
- Review the top ten loss causes monthly
- Audit a sample of codes for accuracy each quarter
Frequently Asked Questions
Turn Downtime Hours into Decisions
Standardize loss codes, capture cost at the event, and give maintenance leaders evidence to prioritize the fixes that matter most.