An electrostatic precipitator is often the last barrier between kiln or raw mill gas and the stack. When fields trip, rappers stop, hoppers plug or gas conditions drift, dust emissions rise and the plant can face compliance pressure and production limits. Good ESP reliability depends on electrical, mechanical and process checks being done together and recorded consistently. This checklist covers each area, and shows how teams can manage the work in Oxmaint.
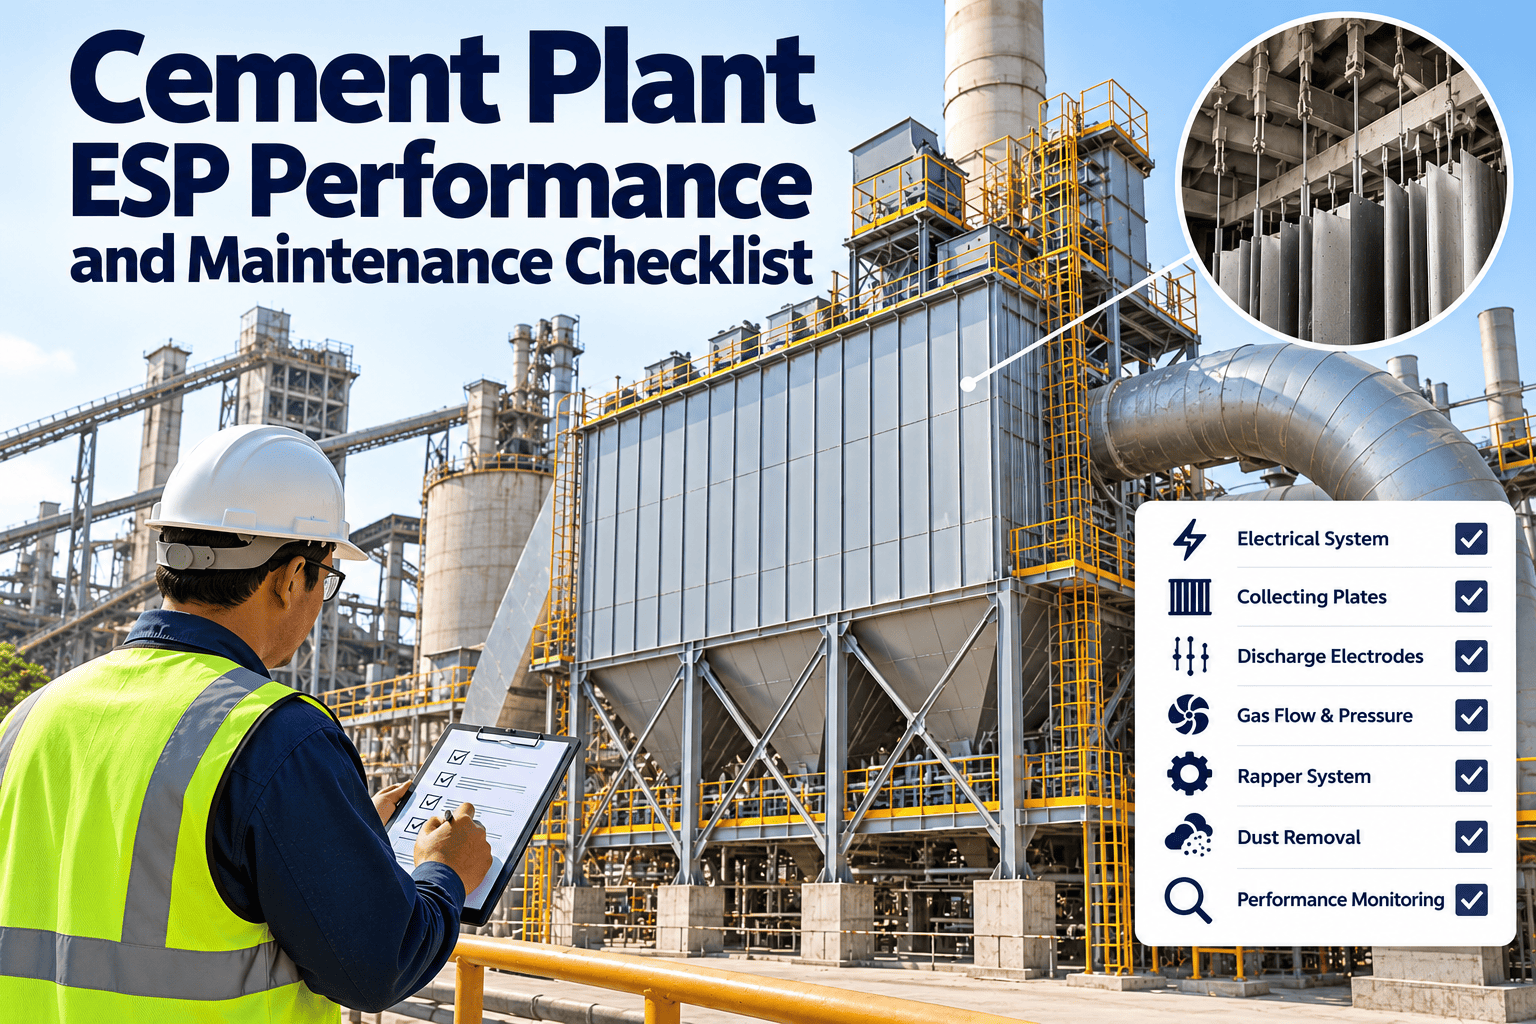
Cement Plant ESP Performance and Maintenance Checklist
Protect emission compliance by checking transformer-rectifier sets, electrodes, rappers, hoppers, insulators and gas conditions on a fixed routine, with clear limits for escalation.
Inspection Record Header
Complete this block before starting the checklist, and tick each item as it is verified in the field.
Why ESP Performance Slips in Cement Plants
Cement ESPs handle gas that changes with kiln mode, raw mill on or off, fuel mix and moisture. That variability exposes small maintenance gaps quickly.
Symptom to Cause: Tracing a Rising Emission Trend
When opacity or dust readings rise, check in a defined order so the team does not guess. Start with electrical status, then mechanical, then process.
- Field out of service or tripped
- Low secondary voltage with high spark rate
- Controller or TR set fault
- Broken or loose discharge wire
- Rappers not operating or poorly timed
- Hopper full or discharge device stopped
- Plate or electrode misalignment
- Insulator contaminated or cracked
- Gas temperature or moisture out of range
- High inlet dust load after an upset
- Air in-leakage and gas flow distortion
- CO trip or mode change at the kiln or mill
Electrical Checklist: Fields, TR Sets and Controllers
| Check | What good looks like | Warning sign | Action |
|---|---|---|---|
| Field voltage and current | Stable values consistent with past readings for the same operating mode | Voltage falls, current rises or readings oscillate | Inspect electrodes, hopper level and rapping, review resistivity |
| Spark rate | Controlled spark rate that suits the field and gas condition | Frequent or sudden sparking | Check clearances, debris, insulator tracking and wire breakage |
| TR set oil and cabinet | Oil level normal, no leaks, cabinet clean and cool | Temperature alarm, oil seepage, burnt smell | Check cooling, connections and oil condition |
| Controller alarms and logs | Alarms are acknowledged, with fault history reviewed | Repeated alarms on a field | Raise a work order and test the control loop |
| High-voltage insulators and bushings | Clean, dry and uncracked, with heaters working where fitted | Tracking, cracks or condensation | Clean or replace, check heater and purge air |
| Earthing and interlocks | Earth links and safety interlocks intact and tested | Missing link or bypassed interlock | Restore immediately under permit |
Make ESP Checks Visible to Operations and Environment Teams
Build ESP routes in Oxmaint, record field readings and hopper checks by asset, and link every abnormal reading to a work order.
Mechanical Checklist by Area
- Collecting plate rappers operate in sequence, with correct intensity and timing.
- Discharge electrode rappers or vibrators are working on every field.
- Hammers, shafts, bearings and drive motors show no excessive wear or seizure.
- Rapping settings are recorded and changed only with an authorised reason.
- Plate spacing and alignment are checked during outage with a defined method.
- Broken discharge wires are removed and counted against each field.
- Frames, hangers and plate suspension show no corrosion or cracking.
- Dust build-up on plates and wires is recorded and photographed.
- Hopper levels are normal, and level detectors are tested.
- Screw conveyors, drag chains and rotary valves run without blockage.
- Heaters and vibrators operate where they are fitted.
- Access doors seal properly, with no air in-leakage or dust leakage.
- Casing and roof show no corrosion, holes or insulation damage.
- Expansion joints and dampers are sealed and moving freely.
- Gas distribution screens and baffles are clean and secure.
- Inlet and outlet temperature and pressure readings are within the expected range.
Process Interface: Where Operations and Maintenance Overlap
Maintenance cannot fix an ESP that is being fed unsuitable gas. Share these checks with the process team and record decisions in the same system.
- Gas conditioning water spray, nozzles and control valves are operating, with no blocked or leaking nozzles.
- Gas temperature at the inlet and outlet is logged for each operating mode, such as raw mill on and raw mill off.
- CO analyser calibration and trip logic are verified on the schedule set by your safety procedure.
- Start-up and shutdown sequences follow the plant procedure for energising and de-energising fields.
- Stack opacity or dust monitor readings are compared with field behaviour to spot lag or drift.
- Fuel changes, such as alternative fuel use, are noted when emissions or sparking patterns change.
Inspection Rhythm: Daily, Weekly, Monthly and Outage
- Field voltage, current and spark trends
- Controller alarms and trip log
- Hopper discharge status
- Stack opacity or dust reading
- Rapper operation walk-through
- Insulator compartment heater and purge checks
- Air in-leakage inspection at doors and joints
- Conditioning tower or nozzle check
- TR set cabinet and oil checks
- Hopper vibrator and heater test
- Drive and gearbox lubrication
- Calibration check of local instruments
- Internal inspection of plates, wires and frames
- Alignment and clearance measurement
- Hopper cleaning and corrosion survey
- Insulator cleaning, replacement and electrical tests
Compliance Records and Emission Excursion Response
Emission limits and monitoring rules vary by country, permit and plant. Confirm your local requirements, and keep the maintenance records that show how you controlled the equipment.
Records that support an audit
- ESP inspection checklists with dates, inspector and findings by field.
- Work orders showing corrective actions and completion dates.
- Calibration records for CO analysers and emission monitors where maintenance owns them.
- Outage inspection reports with photos of plates, wires and hoppers.
Spreadsheet Rounds Versus a Connected ESP Workflow
- Field readings are on a separate DCS screen from maintenance records.
- Rapper failures are fixed but not counted by field.
- Outage findings are summarised once and rarely reviewed.
- Environment and maintenance teams use different data.
- Each field and rapper group is an asset with its own history.
- Abnormal readings create work orders with priority and owner.
- Outage findings become planned tasks for the next stop.
- Dashboards show repeat defects and overdue inspections.
How Oxmaint supports ESP maintenance
- Asset management for ESP fields, TR sets, rappers, hoppers, conditioning equipment and instruments.
- Preventive maintenance for lubrication, calibration, rapper checks and heater tests.
- Mobile inspections with photos for hoppers, insulators and in-leakage points.
- Corrective work orders, spare parts tracking and reports for environmental audits.
- Condition-based and trend-driven tasks when readings are captured in the system.
Outage Inspection Scope: What to Do Inside the Casing
The internal inspection is the best chance to see electrode and plate condition. Plan access, scaffolding, cooling time and permits well before the kiln stops.
Common ESP defects and their usual maintenance causes
- Broken discharge wires, often linked to excessive sparking, corrosion, fatigue or mechanical damage during rapping.
- Plate distortion and misalignment, linked to temperature excursions, poor support condition or heavy dust build-up.
- Insulator tracking, usually from dust and moisture on the insulator surface, or from heater and purge-air failures.
- Hopper build-up, linked to cold spots, poor heating, leaking doors or inadequate discharge capacity.
- Weak rapping, caused by worn hammers, loose fasteners, drive faults or incorrect settings.
- Falling collection efficiency in one field, which may point to controller issues, short circuits or wire breakage.
Start-Up and Shutdown Considerations
Many ESP problems begin during transitions. Follow your site procedure, and add maintenance checks that confirm equipment is ready for each state change.
- Insulator heaters and purge air have been running for the period set by the procedure.
- Rappers, hopper discharge devices and heaters are operating.
- All permits are closed, access doors are sealed, and interlocks are restored.
- CO and gas analysers are available, calibrated and in service.
- Operators watch voltage, current and spark rate on each field.
- Gas temperature and conditioning flow are adjusted per the process plan.
- Any field that trips is logged with the time, mode and alarm text.
- Repeat trips are reviewed with maintenance for a cause, not just reset.
- Hoppers are emptied or managed according to procedure, to avoid cold set dust.
- Fields are checked for water ingress or condensation before energising.
- Findings from the outage are entered, including parts replaced and open defects.
- Rapping and conditioning settings are verified against the approved values.
- Event time, duration and operating mode are recorded.
- Field status and readings before and during the event are reviewed.
- Root cause is classified as electrical, mechanical, process or instrument.
- Corrective actions are assigned and followed until closed.
Spare parts worth stocking for ESP maintenance
- Discharge wires or electrodes, and fixings that match the installed design.
- Rapper hammers, shafts, bearings and drive motors or gearboxes.
- Support insulators, bushings and heater elements for insulator compartments.
- Rotary valve and screw conveyor wear parts for hopper discharge.
- Controller cards, TR set components and key instruments, such as level switches and temperature sensors.
Reading Field Trends Without Over-Reacting
Field readings change with kiln mode and dust properties, so a single abnormal value is not always a defect. Compare each field with its own history in the same operating mode.
- Record voltage, current and spark rate at the same points in each shift, and note the mill status, kiln feed and fuel type.
- Look for a slow downward trend in secondary voltage at constant conditions, which can indicate dirty electrodes, weak rapping or insulator leakage.
- Treat a sudden step change as a possible short circuit, broken wire or controller fault, and inspect that field first.
- Compare adjacent fields. If the inlet field is normal but later fields degrade, check gas distribution, hopper levels and rapping sequence.
- Review the relationship between stack opacity and field status, to learn how many fields can be lost before your plant approaches its limits.
Settings control and change records
- Keep an approved list of controller, rapping and conditioning setpoints for each operating mode.
- Record who changed a setting, when, and why, and review the effect on emissions and sparking after the change.
- Restore settings after maintenance tests, and have a second person confirm that values match the approved list.
KPIs That Show ESP Reliability
ESP Maintenance FAQs
Keep Every ESP Field Working and Every Record Ready
Bring electrical, mechanical and process checks into one maintenance workflow, so emission risks are found and fixed before they become excursions.