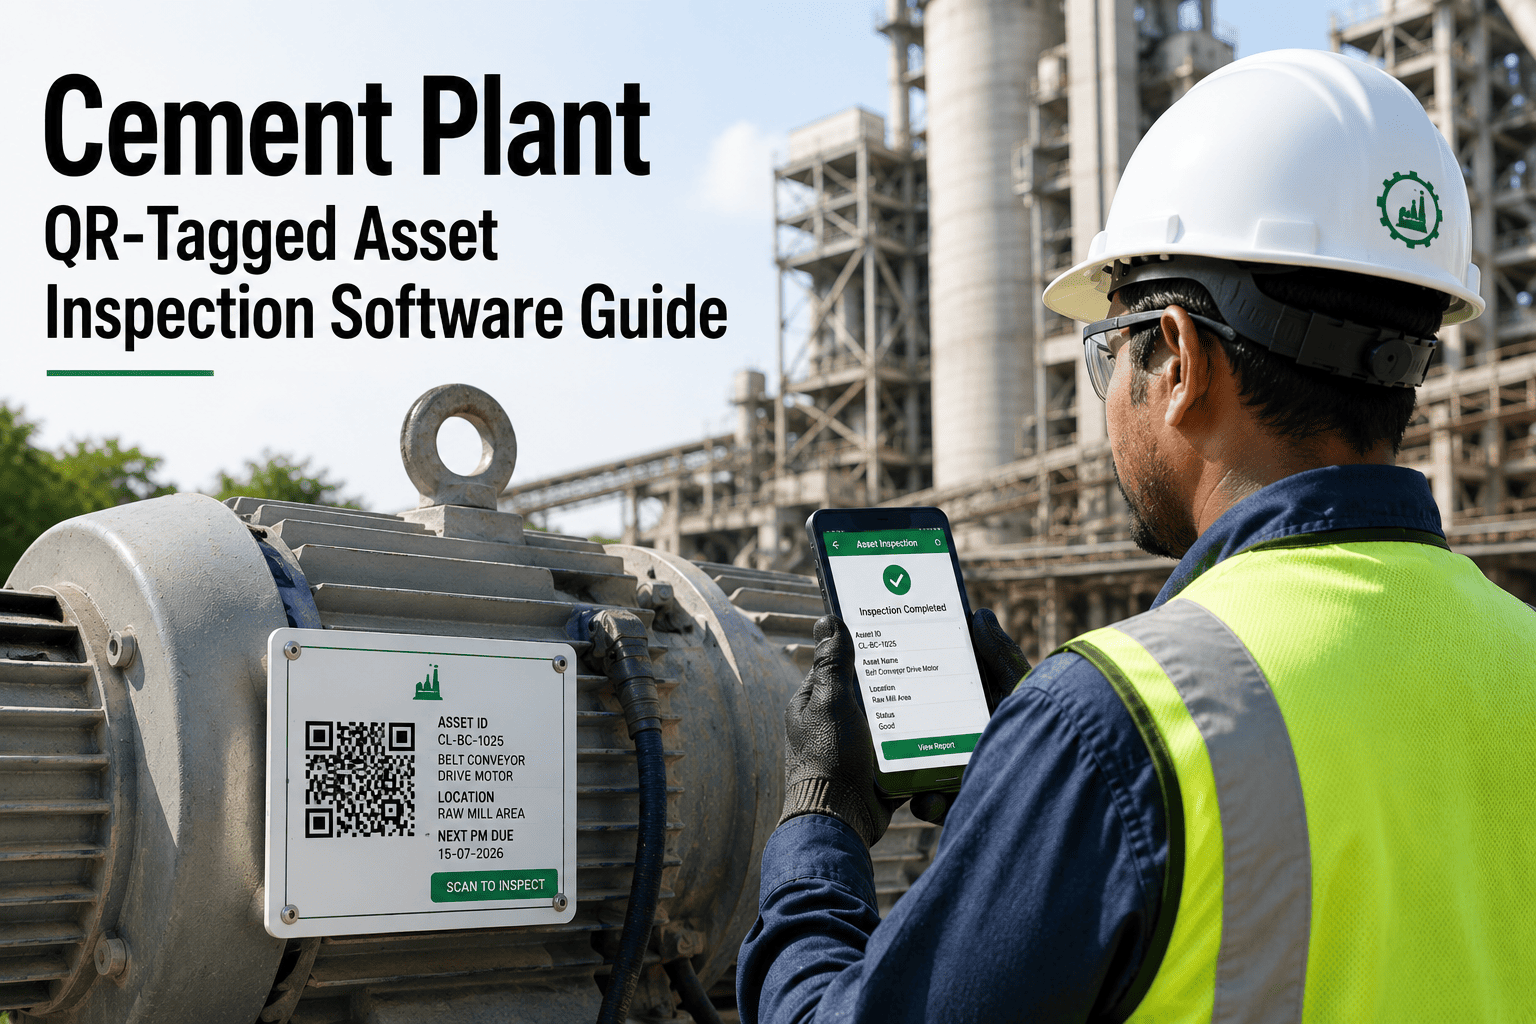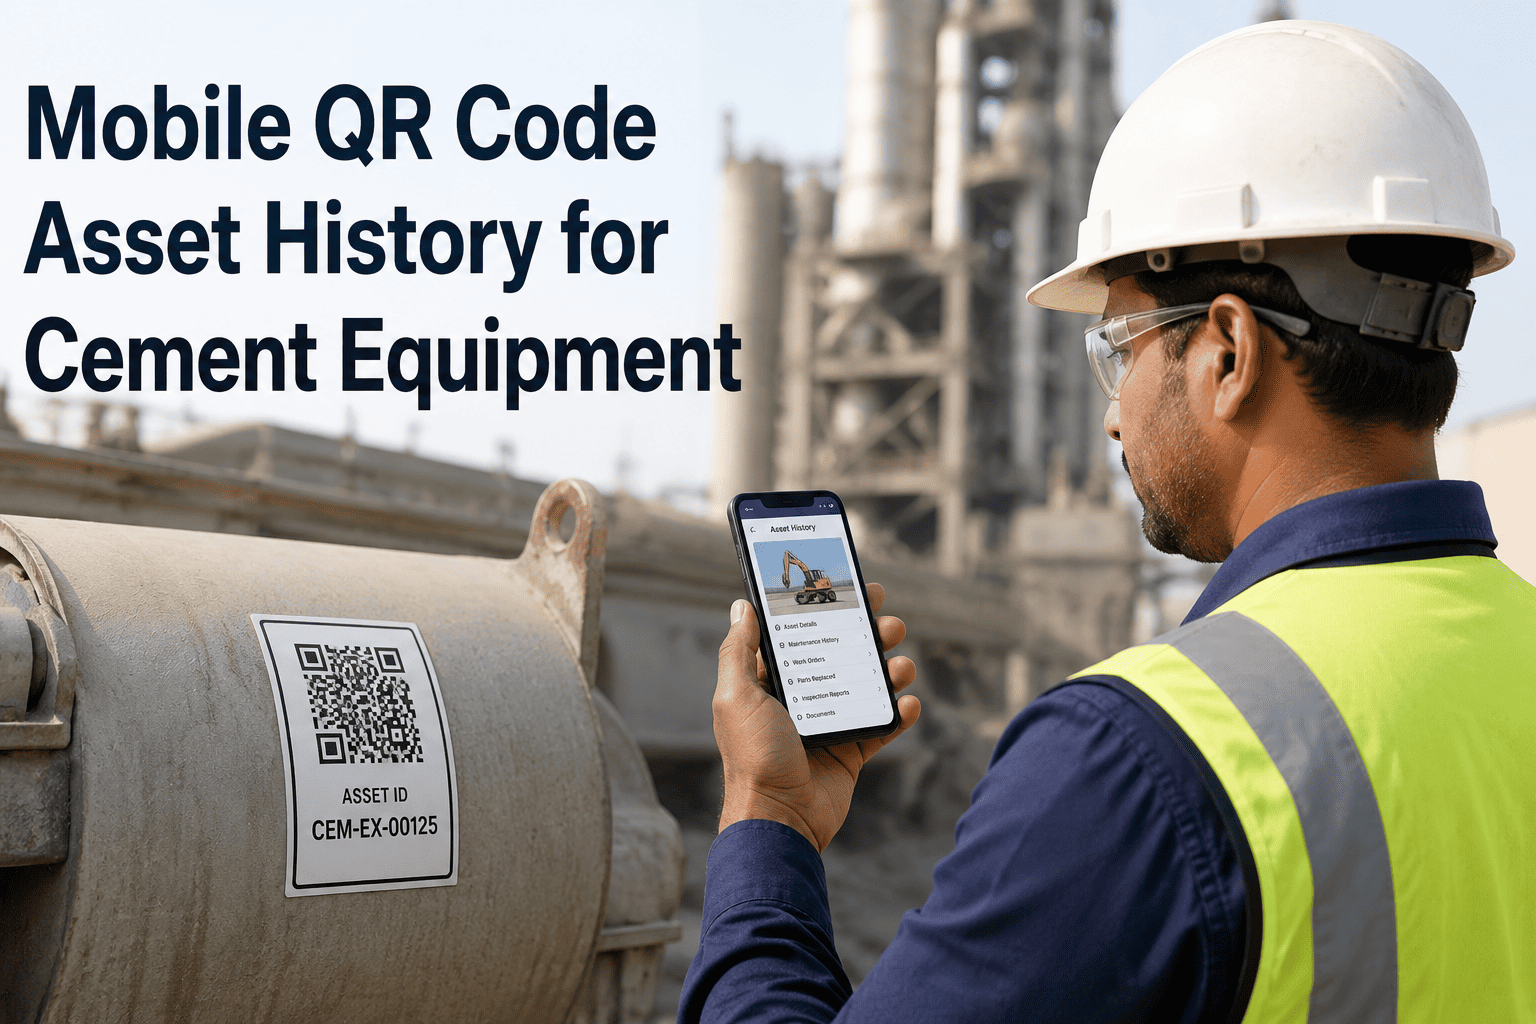
Cement plants spread inspection routes across crushers, mills, kilns, coolers, fans and packing lines, often in dusty, hot and noisy areas where paper forms get dirty, lost or filled in later. A mobile inspection checklist library gives every route a standard set of questions on a phone or tablet, with photos, readings and automatic follow-up. This page lists the checklists a cement plant typically needs, how to design them, and how cement plant CMMS software turns each finding into maintenance action.
Cement Plant Mobile Inspection Checklist Library
Build a structured library of mobile checklists for every area of the plant, so conditions, risks, actions, owners and follow-up evidence are captured at the equipment, not remembered afterwards.
Paper Rounds Versus a Mobile Checklist Library
The Checklist Library by Plant Area
Treat the following as a library index. Each area has several checklists with different frequencies, owners and escalation rules, and every plant should adjust points to its own equipment and risk assessment.
Quarry and crushing
- Crusher rotor, hammer and liner wear
- Bearing temperature and lubrication
- Feeder, chute and conveyor condition
- Dust suppression and guard integrity
Raw mill and cement mill
- Gearbox oil level, temperature and leaks
- Hydraulic pressure and accumulator readings
- Roller, table or ball charge condition notes
- Separator drive, seals and air leakage
Preheater and kiln
- Shell hot spots and refractory observations
- Support roller and thrust roller condition
- Kiln drive, girth gear and lubrication
- Seals, build-up and blaster status
Clinker cooler
- Grate plate condition and undergrate spillage
- Cooler fan vibration and airflow
- Hydraulic drive pressure and leaks
- Clinker breaker and conveyor condition
Fans, filters and environment
- ID fan bearing temperature and vibration
- Bag filter differential pressure and pulse valves
- Stack monitoring alarms and sampling points
- Dust leakage at ducts and transfer points
Packing and dispatch
- Packer spouts, load cells and rotor condition
- Bag placer and conveyor safety devices
- Silo discharge, loading arm and weighbridge
- Housekeeping and emergency stop tests
Electrical and automation
- MCC room cleanliness and cooling
- Panel temperature checks and loose connections
- Drive faults and protection relay alarms
- Cable trays, earthing and labelling
Safety and utilities
- Compressed air system leaks and receivers
- Fire protection and extinguisher status
- Walkway, handrail and lighting condition
- Lockout/tagout and permit readiness
Standardise Every Route Across Shifts
Give inspectors the same questions on every round, and give supervisors a live view of what was done and what was found.
Design Rules for Checklists People Will Actually Complete
A long list of vague questions encourages tick-and-flick behaviour. These rules keep checklists useful in a harsh plant environment.
Replace "Is the bearing OK?" with a temperature reading, an abnormal noise yes/no, and a lubrication check.
Display the acceptable range next to each numeric field so inspectors know when a value is abnormal.
Split large areas into logical routes so each can be completed without rushing.
Failed points need a photo and a note, which helps planners prepare the right parts and tools.
Kiln floors, tunnels and basements can lose signal, so confirm offline capture and later synchronisation.
An unassigned finding rarely gets fixed, so each failure should route to a responsible person.
Severity Rules That Drive Follow-Up
Agree the response for each severity level in advance so inspectors do not have to improvise. The timeframes below are examples to adapt.
| Finding level | Example in a cement plant | Required action | Owner |
|---|---|---|---|
| Critical | Rapidly rising bearing temperature on a kiln support roller or main fan | Notify the control room immediately, assess for shutdown and raise an urgent work order | Area engineer and shift supervisor |
| High | Hydraulic leak at a cooler drive, missing guard on a rotating shaft | Fix or make safe within the shift, then verify | Maintenance supervisor |
| Medium | Worn conveyor idlers, minor dust leakage at a transfer chute | Plan into the weekly schedule | Planner |
| Low | Faded signage, minor housekeeping issue | Add to routine backlog and review monthly | Area owner |
From Checklist Answer to Maintenance Record
A library only creates value when its outputs feed the rest of the maintenance system. Here is how each type of result should be used.
Pass results
- Stored as time-stamped evidence of completed rounds
- Used to build condition history per asset
- Reviewed for compliance and audit requests
Fail results
- Converted to corrective work orders with photos
- Prioritised by severity and equipment criticality
- Linked to spares and procedures needed for repair
Reading trends
- Temperature and pressure values charted over time
- Repeat defects flagged for root cause analysis
- Findings used to adjust preventive maintenance tasks
KPIs for the Inspection Programme
| KPI | Calculation | Use |
|---|---|---|
| Route completion rate | Completed routes divided by scheduled routes | Confirms inspections are happening |
| Defects found per round | Failed points divided by completed checklists | Shows whether checks are meaningful |
| Time to action | Hours from failed point to work order assignment | Measures follow-up discipline |
| Inspection-to-failure ratio | Breakdowns on assets with recent inspections | Tests checklist quality |
| Open findings by area | Unresolved items grouped by plant area | Highlights backlog hotspots |
How Oxmaint Supports Mobile Inspections
Oxmaint helps maintenance teams keep inspections, assets and work orders in one connected workflow.
Inspection tools
- Configurable checklists for each asset type
- Mobile capture of photos, readings and notes
- Scheduled routes with overdue visibility
Maintenance workflow
- Work orders generated from failed points
- Preventive maintenance linked to inspection results
- Reports and dashboards for supervisors
Asset context
- Equipment history and documents in one place
- Spare parts linked to the asset
- Compliance records ready for audits
Sample Checklist: Kiln Shift Round
This example shows the level of detail that works on a mobile device. Adapt each point to your kiln design and operating limits.
Kiln shift round
Sample Checklist: Clinker Cooler and Fans
Cooler grate and drive
- Hydraulic pressure within the defined range
- Hose and fitting leaks, with photos if found
- Undergrate spillage level and cleaning status
- Abnormal noise or grate movement observed
Cooler fans
- Bearing temperature and vibration readings
- Coupling guard and base bolt condition
- Damper movement and position feedback
- Motor current and abnormal heating
Clinker handling
- Breaker hammer and housing condition
- Conveyor tracking and idler condition
- Pan or drag chain tension and wear signs
- Housekeeping and dust leakage at transfer points
Who Does What on an Inspection Round
Complete routes, record readings and report defects with photos, using the same templates on every shift.
Review findings each shift, confirm severity, and assign work to the right trade.
Group findings into plannable work, order parts and slot jobs into stops or low-load periods.
Study repeat defects and trends, then revise checklists and preventive maintenance tasks.
Use inspection records for dust, guarding, permit and emission-related checks and audits.
Track route completion, backlog and downtime reasons to decide where to invest.
Rolling Out the Library Without Overwhelming Crews
Phasing the rollout helps inspectors build confidence and gives engineers time to refine each template.
Why Mobile Inspection Programmes Stall
- Too many points per checklist. Long forms lead to rushed answers, so keep each route realistic for the time available.
- No visible response to findings. When reports vanish, inspectors stop writing them. Show the status of each finding to the person who raised it.
- Weak asset tagging. If labels are damaged by heat or dust, scanning fails and crews revert to paper. Choose durable tags and replace them during shutdowns.
- Training done once. New hires and contractors need a short, practical onboarding on the device and the templates.
- Library never reviewed. Equipment changes, so revisit templates after modifications and major failures.
Sample Checklist: Raw Mill, Fans and Packing
Libraries become more useful when templates are reusable across similar equipment. These three examples can be cloned for each mill, fan or packer.
| Equipment | Typical checks | Evidence captured |
|---|---|---|
| Vertical roller mill | Gearbox oil temperature, hydraulic pressure, vibration, leaks at roller arms, reject system condition | Readings, leak photos and operator notes |
| Bag filter and ID fan | Differential pressure, pulse valve function, bearing temperature, ducting leaks, damper position | Numeric values and visible dust photos |
| Packing machine | Spout wear, load cell drift, bag placer function, emergency stop test, guarding | Pass/fail results and test timestamp |
Using Inspection Data to Improve Maintenance Plans
After several months of structured rounds, patterns appear that are impossible to see on paper. Use them to improve preventive and condition-based maintenance.
Tighten intervals
- Assets with repeated findings between PM visits
- Lubrication points that regularly show dryness
- Wear parts replaced earlier than planned
Relax or remove tasks
- Checks that never find a defect over a long period
- Duplicated tasks across operations and maintenance
- Low-risk equipment inspected too often
Escalate for engineering
- Recurring failures despite repairs
- Design weaknesses causing dust or leaks
- Candidates for sensors and online monitoring
Making Mobile Inspections Work in Dusty, Hot Plant Conditions
Cement plants are hard on devices and labels. Planning for the environment avoids the most frequent reasons crews return to paper.
Choose devices with protective cases and screens that can be used with gloves and in bright outdoor light.
Use heat and dust resistant labels, positioned where they can be reached safely and cleaned easily.
Define who charges and issues devices at shift start so rounds are never delayed.
Set clear rules on where devices may be used, especially near rotating equipment and in restricted zones.
Training checklist for new users
- How to scan a tag, open a checklist and save progress
- How to take clear photos that show the defect and its location
- When to escalate by phone instead of waiting for a work order
- How offline entries synchronise once signal returns
- Who to contact when a template appears wrong or incomplete
Records to Keep as Follow-Up Evidence
Strong inspection programmes preserve evidence that supports internal reviews, insurers and regulators. Confirm the exact retention rules that apply in your region.
Frequently Asked Questions
What is a mobile inspection checklist library?
It is a set of standard digital checklists organised by plant area and equipment type, used on phones or tablets during routine rounds. Each template defines the questions, limits, evidence required and escalation rules, so every inspector records conditions the same way and results are stored against the asset.
How many checklists does a cement plant need?
It depends on equipment count and risk, but most plants start with one checklist per major area, such as kiln, cooler, raw mill, fans and packing. After a pilot, templates are usually refined and cloned by equipment type, so the library grows in a controlled way instead of starting with hundreds of forms.
Can inspectors work without network coverage?
Many cement plant areas have weak signal, so check that offline capture and synchronisation are supported before rollout. Inspectors should be able to scan a tag, complete the checklist and attach photos without coverage, with results uploading later. Book a demo to review this with your team.
How do inspections reduce unplanned downtime?
Inspections catch early signs such as leaks, heat, vibration, wear and dust leakage, then convert them into planned work before a failure stops the line. Trends in readings and repeat defects also help engineers adjust preventive maintenance intervals and decide where condition monitoring would add value.
What is a sensible way to begin?
Pilot one critical area such as the kiln or cooler, refine the questions with the inspectors who use them, then extend to other areas in phases. Tag equipment, define severity rules and name owners from the start. You can sign up to build your first checklist.
Bring Every Inspection Round Into One Library
Standardise checklists, capture evidence on mobile and turn findings into tracked maintenance work across your cement plant.