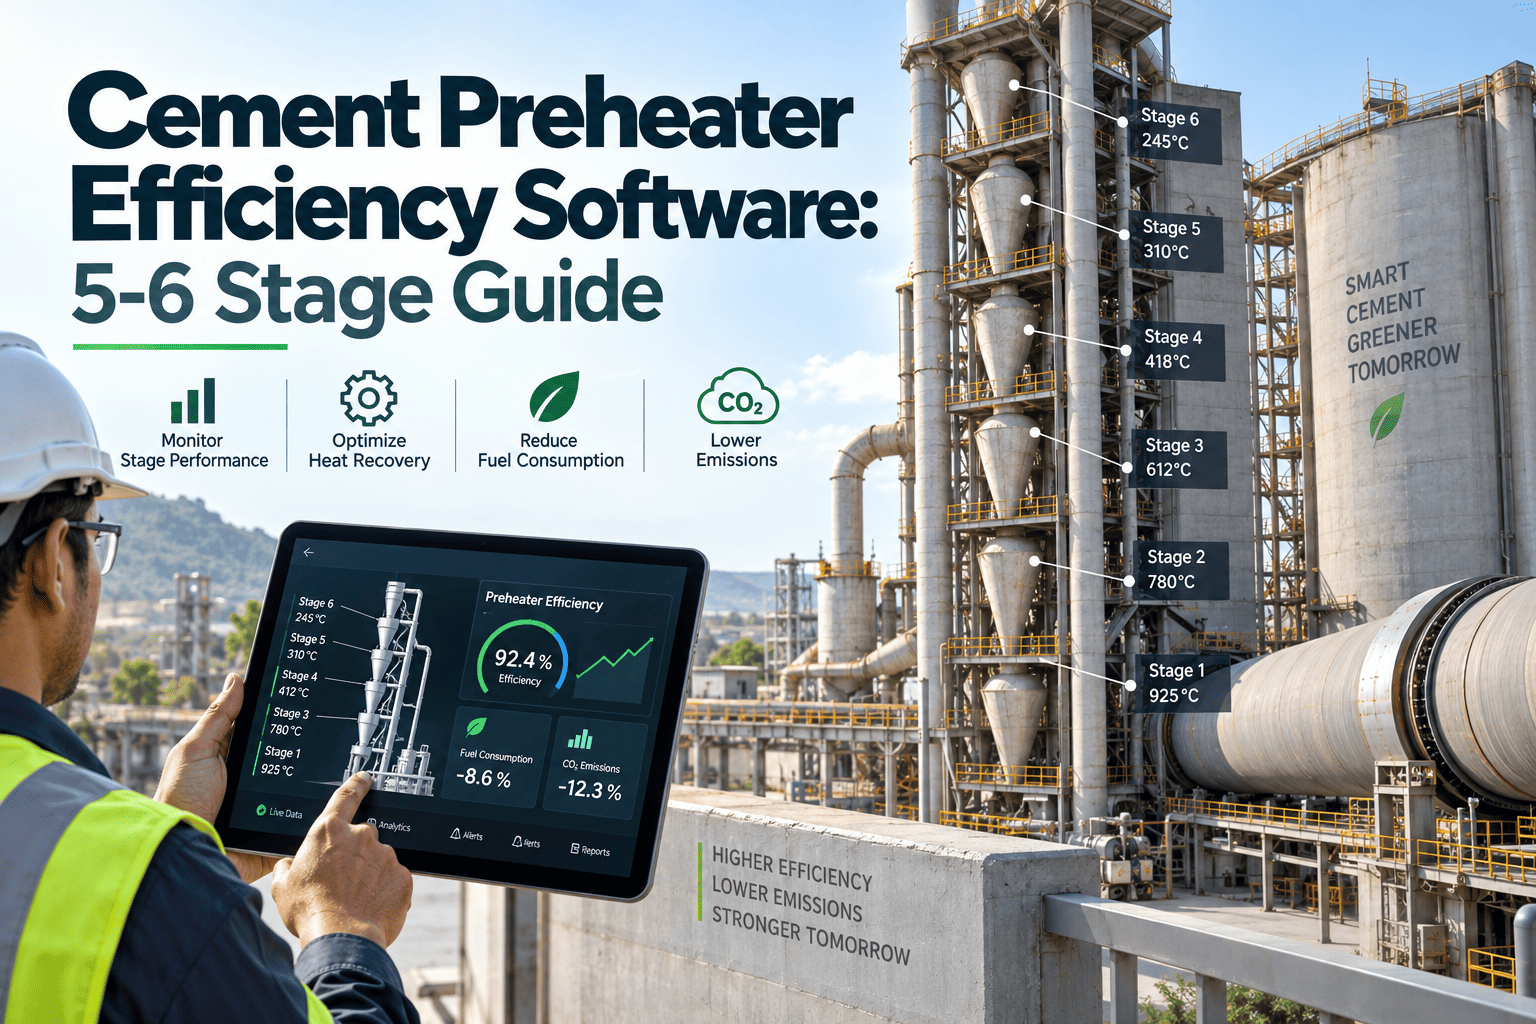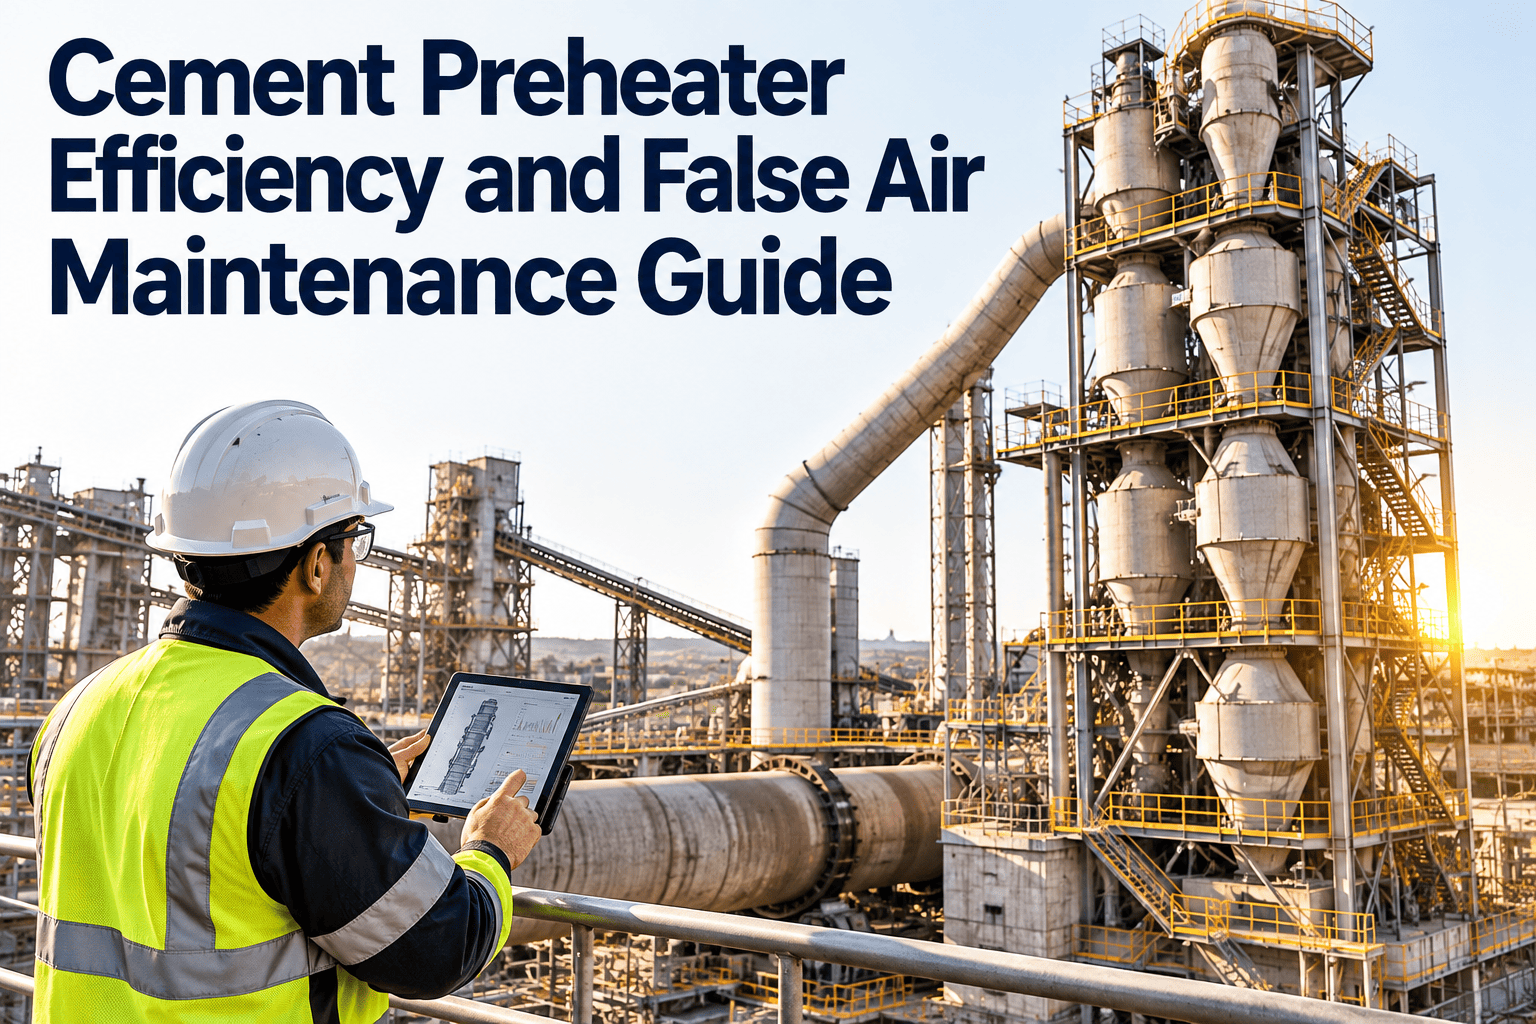
A five-stage preheater tower is the thermal heart of a dry-process cement kiln, exchanging heat between hot kiln exhaust gas and incoming raw meal before the material ever reaches the calciner. When every cyclone, dip tube, and expansion joint holds its seal, the tower runs close to its design specific heat consumption. The moment cold ambient air is pulled in through a worn door gasket or a cracked joint, that efficiency starts leaking away quietly, shift after shift, long before anyone notices a change in fuel invoices.
Stop Paying for Heat Your Preheater Tower Is Quietly Losing
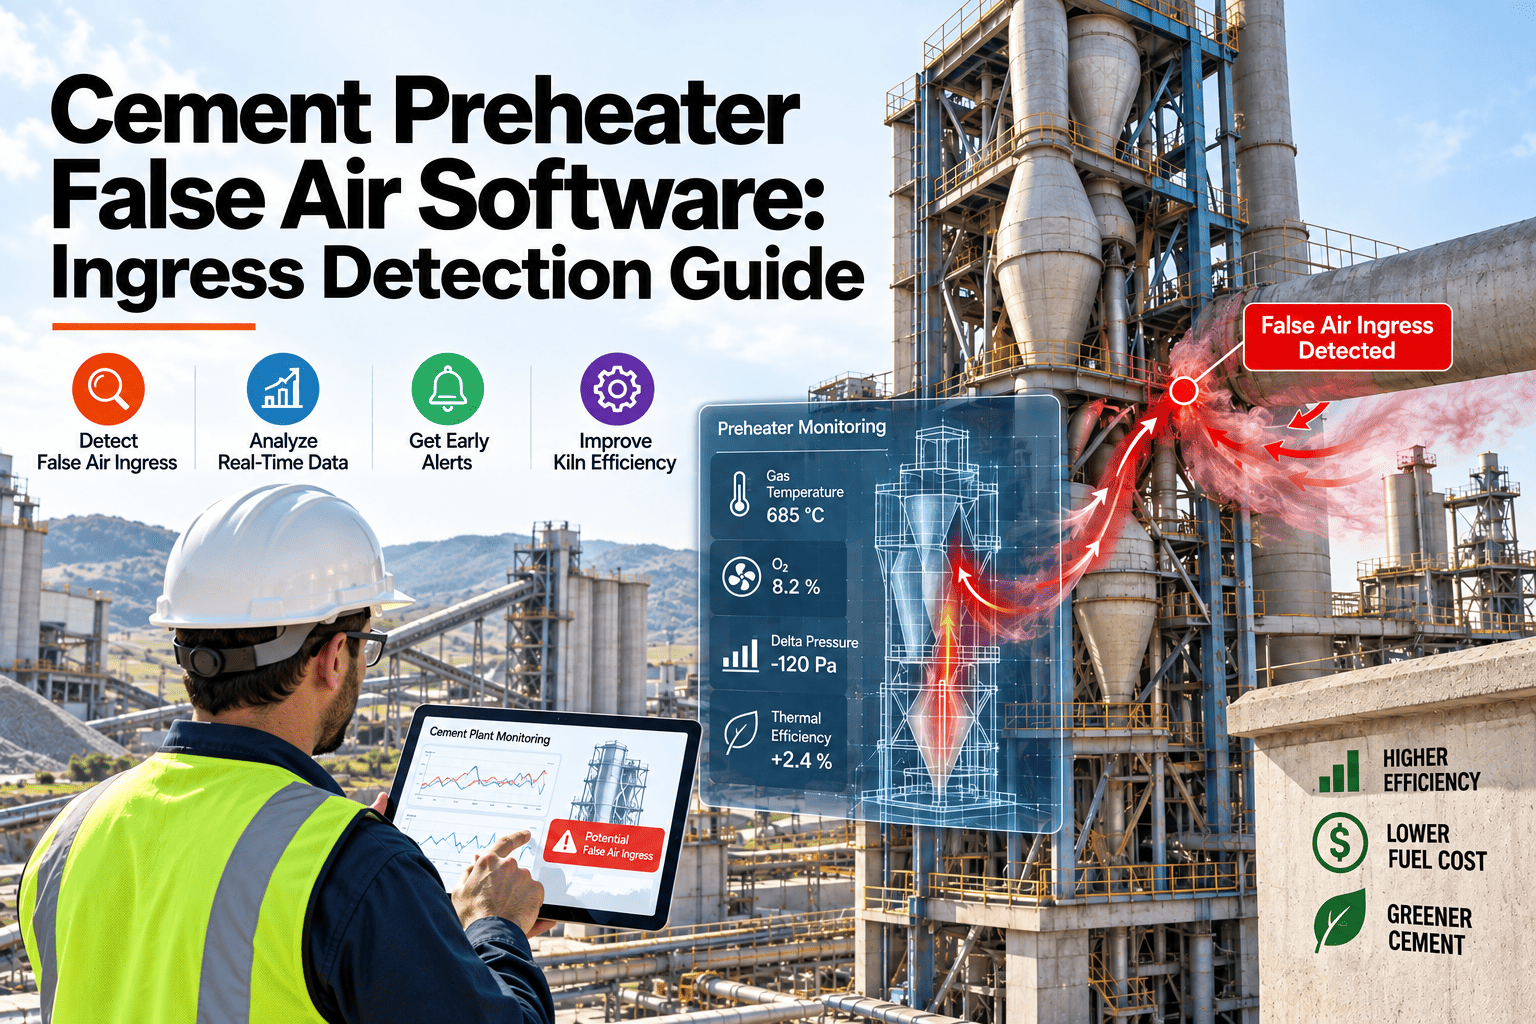
False air infiltration is the largest controllable source of fuel waste in a cement kiln line, yet most plants still treat preheater tightness as a once-a-year outage task instead of a tracked operational metric. OxMaint turns O2 mapping, seal inspections, and door gasket replacement into a scheduled, auditable maintenance program.
How Heat Moves Through a Dry-Process Preheater Tower
Raw meal enters the top cyclone near ambient temperature and falls stage by stage against a rising countercurrent of hot kiln gas, gaining roughly 700 to 900°C of preheat before it reaches the calciner and kiln inlet. Every stage depends on the gas stream carrying only the oxygen and combustion products it is supposed to carry.
Plant teams researching preheater optimization often start with a maintenance platform built to track tightness at every stage rather than relying on a single annual survey.
Why False Air Is So Easy to Ignore and So Expensive to Carry
False air does not trip an alarm or stop production. It hides inside a slightly higher O2 reading, a fan running a little harder than it should, and a fuel bill that creeps upward over a campaign without an obvious single cause.
A wider gas stream also dilutes oxygen at the burner, forcing combustion adjustments that push CO and NOx in the wrong direction, so the losses extend beyond fuel cost into emissions performance and refractory life.
Turn a Once-a-Year Survey Into a Tracked Program
OxMaint schedules O2 mapping rounds, seal and gasket inspections, and expansion joint checks against your preheater asset register, so leaks are found, assigned, repaired, and verified in one continuous record instead of a spreadsheet nobody updates.
Where False Air Actually Gets In
Cold air follows the pressure gradient created by the ID fan into every gap the string offers. A targeted survey route is far more effective than a general walk-through.
| Leak Point | Typical Contribution | Primary Inspection Method |
|---|---|---|
| Kiln inlet seal | Largest single source; grows with shell ovality | Monthly visual gap check plus differential pressure trend |
| Kiln outlet seal | Up to 8% of total ingress in worn seals | Quarterly wear measurement against baseline |
| Cyclone inspection doors and poke holes | Dominant source on most 4 and 5 stage towers | Gasket condition check every planned shutdown |
| Meal pipe joints and expansion bellows | Rises sharply once fabric bellows exceed 18–24 months | Weekly thermal imaging for hot spots |
| Cyclone flap valves | Recirculates gas between stages once wear exceeds design clearance | Function test during scheduled stops |
| Tertiary air duct dampers | Concentrated near the calciner inlet, hardest to reach | Annual access-platform inspection |
Three Warning Signs Your Tower Tightness Program Is Failing
These indicators consistently show up before a plant's specific heat consumption drifts noticeably higher, and each one is catchable weeks ahead of the fuel bill confirming it.
Measured during steady 90–105% production with feed stable within 2%, exit O2 above 3.5% signals measurable ingress. Above 4.5–6% without a tracked sealing program is common and costly.
A fan working harder to maintain the same draft, with no change in feed or fuel rate, almost always points to a growing leak path somewhere along the tower or kiln seals.
A thermal scan that repeatedly flags the same expansion joint or riser duct location, shutdown after shutdown, means the repair scope during the last outage was insufficient.
Building a Preheater Tightness Program That Sticks
Closing the gap between finding a leak and confirming it stays sealed is mostly a process problem, not a detection problem. A structured sequence keeps every finding accountable.
- Baseline exit O2, CO2, and temperature during one hour of stable operation, logged against feed and fuel rate.
- Map O2 stage by stage from the top cyclone down using dedicated sampling ports.
- Route every identified leak as a work order tied to the specific asset and seal component.
- Re-gasket inspection doors and verify frame flatness during every planned shutdown.
- Re-measure O2 after repair to confirm the leak is actually closed, not just addressed on paper.
- Trend fan power and specific heat consumption monthly to catch new leaks between shutdowns.
How OxMaint Supports Preheater Tightness Management
OxMaint gives reliability and process teams one shared system for tracking every seal, gasket, and joint across the preheater string, so tightness becomes a measured discipline rather than a memory exercise.
Preventive Maintenance Scheduling
Automated recurring work orders for door gasket replacement, flap valve function tests, and expansion joint checks, scheduled against each cyclone stage asset.
Mobile Inspection Workflows
Technicians log O2 readings, thermal photos, and gap measurements from the platform during shutdowns, tagged to the exact stage and component.
Corrective Work Order Automation
Any reading outside the tightness threshold automatically generates a corrective work order and assigns it before the shift ends.
Reporting and Trend Dashboards
Fan power, exit O2, and specific heat consumption trends sit alongside inspection history so a rising fuel curve can be traced back to its source.
The Connection Between Preheater Tightness and Refractory Life
False air does more than waste fuel. Diluted, cooler gas near the calciner and kiln riser disturbs the temperature profile the refractory lining was designed around, and repeated thermal cycling from an unstable flame accelerates brick spalling at the hot face.
Plants that track tightness alongside refractory inspections typically find the two datasets tell the same story from different angles: a chronic hot spot on a riser duct joint often correlates with a refractory zone wearing faster than its neighbors, and closing the air leak frequently slows the wear rate on the adjacent lining as a secondary benefit.
Combustion stability matters just as much on the emissions side. A burner starved of controlled combustion air by a diluted, oxygen-rich gas stream tends to run hotter locally to compensate, which pushes NOx formation upward even while overall fuel efficiency is falling — a case where a single root cause shows up as two separate compliance and cost problems on two different reports.
Give Your Preheater Tower a Measured Tightness Program
Stop waiting for the annual audit to find out how much heat the tower lost this campaign. OxMaint keeps every seal, gasket, and joint on a schedule with a documented history.
What a Full Preheater Audit Should Cover
An annual audit is a starting point, not a substitute for ongoing tracking, but it should be thorough enough to set an accurate baseline for the months between shutdowns.
- Stage-by-stage O2 and CO2 mapping from the top cyclone to the kiln inlet, recorded against feed rate and load.
- Physical measurement of kiln inlet and outlet seal gaps against OEM tolerance, not a visual pass or fail.
- Thermal imaging of every accessible expansion joint and riser duct section during stable operation.
- Function testing of cyclone flap valves under simulated backward flow to confirm they seat correctly.
- Cross-referencing fan power trends against the prior audit to catch drift that occurred between inspections.
Documenting each finding against the specific asset, rather than as a general note in a shutdown report, is what makes the next audit faster and the trend line meaningful instead of just a snapshot.
Preheater False Air: Frequently Asked Questions
What is a normal exit O2 reading for a well-sealed preheater tower?
How often should cyclone inspection doors be re-gasketed?
Can false air be reduced without a full kiln stop?
How does OxMaint track false air findings across shutdowns?
What is the fastest way to see how OxMaint fits a specific plant?
Make Preheater Tightness a Measured Discipline, Not a Once-a-Year Guess
Every percentage point of false air is fuel you already paid for and never used. OxMaint keeps O2 mapping, seal inspections, and gasket replacement on a schedule your whole team can see.