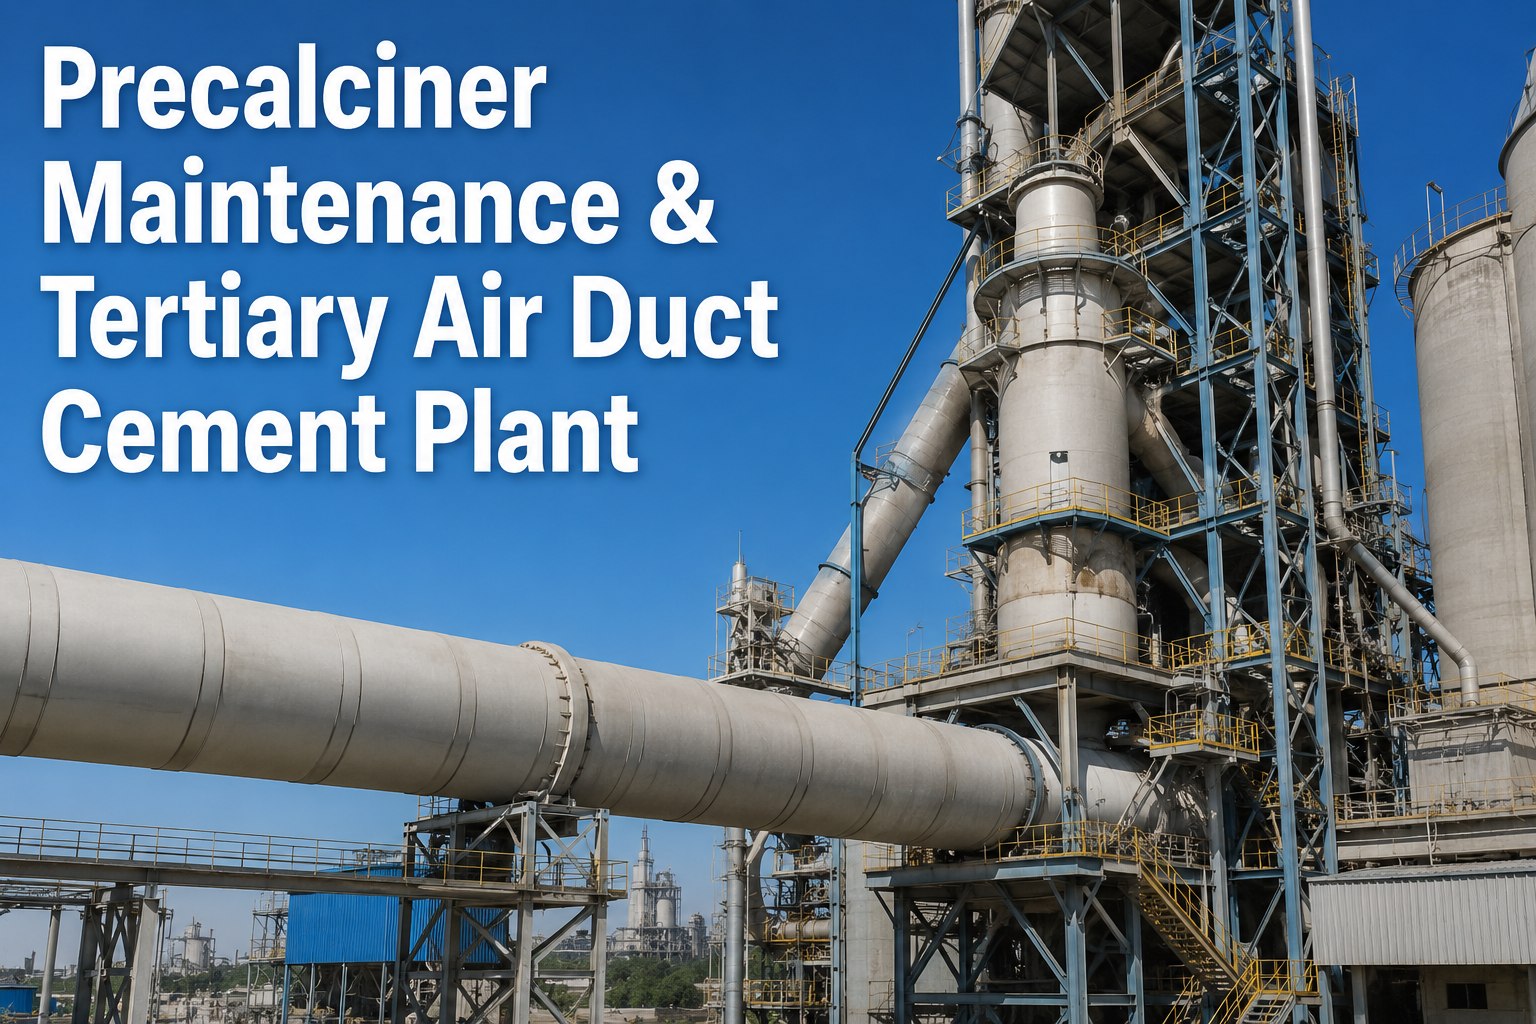
The precalciner and tertiary air duct (TAD) together handle roughly 60% of total fuel combustion on a modern cement kiln line, which makes them the single largest lever for thermal efficiency and clinker capacity. A well-run precalciner maintenance program protects calcination rates above 90%, holds specific heat consumption within 860–880 kcal/kg clinker, and prevents the unplanned outages that cost a typical 5,000 tpd plant $180,000–$420,000 per day in lost output. This guide walks plant and reliability managers through burner pipe PM, refractory inspection intervals, TAD damper service, false-air control, and the CMMS workflows that keep heat balance and precalciner performance aligned. Start with the inspection checklist below, or Start Free Trial to deploy a structured precalciner maintenance plan in days, not months.
Is your precalciner quietly burning 8% more fuel than it should?
Most cement plants lose 3–8% in calciner thermal efficiency between scheduled outages — not from catastrophic failure, but from false-air ingress, burner pipe drift, and refractory thinning that goes unmeasured for 11 months. The right maintenance plan closes that gap and protects the 60% of fuel combustion the precalciner and TAD are responsible for.
The 7-zone precalciner and TAD inspection checklist
Every shutdown and planned outage should follow the same seven-zone sequence. Together these zones cover the full combustion path from kiln riser to stage-4 cyclone and account for more than 90% of precalciner reliability losses observed across cement industry audits.
Calciner refractory lining
- Measure remaining thickness at 12 datum points; flag any zone below 60 mm.
- Inspect coating ring build-up at the cone; remove if asymmetrical >150 mm.
- Document hot-face spalling and alkali-alumina reactions.
Burner pipe assembly
- Check nozzle tip wear; replace if tip-to-nozzle gap exceeds 4 mm.
- Verify coal/coarse particle swirl plate alignment to ±2°.
- Pressure-test primary air channels for cross-leakage.
Tertiary air duct
- Thermo-scan TAD elbows for red-spots above 320°C skin temp.
- Inspect expansion joints; replace gaskets every 24 months.
- Measure dust accumulation; clean if cross-section reduced >15%.
TAD damper & actuator
- Calibrate damper position feedback to DCS within ±1.5%.
- Inspect blade-edge wear; replace at 5 mm loss.
- Lubricate trunnion bearings per OEM torque schedule.
SNCR / NOx system
- Verify ammonia or urea injection lance flow balance to ±5%.
- Check atomizing air pressure and lance tip erosion.
- Log NSR ratio trends against NOx stack readings.
Riser & meal feed
- Inspect meal splash box wear plates; replace at 40% thickness.
- Confirm feed chute rotation and distribution uniformity.
- Check kiln riser choke ring for build-up above 200 mm.
Cyclone & dip tube
- Measure stage-4 cyclone efficiency; investigate below 90%.
- Inspect dip tube immersion depth and erosion pattern.
- Clear material build-up in the lower cone and flap valve.
Where precalciner reliability actually breaks down
Audit data from 40+ kiln lines shows a consistent distribution of unplanned precalciner and TAD downtime causes. The table below ranks them by frequency and shows the typical lead-time you have before a finding becomes an outage.
| Failure mode | Share of downtime | Typical lead-time to outage | Detection method |
|---|---|---|---|
| Refractory thinning / hot-spot | 27% | 8–16 weeks | IR thermography, shell scan |
| Burner pipe tip erosion | 18% | 6–10 weeks | Flame-shape deviation, CO spike |
| TAD false-air ingress | 16% | 10–20 weeks | O2 delta, mass-balance audit |
| Damper blade binding | 11% | 4–8 weeks | Positioner feedback error |
| Coating ring collapse | 9% | 2–6 weeks | Draft instability, meal spike |
| SNCR lance blockage | 7% | 2–4 weeks | NOx trend, NH3 slip alarm |
| Expansion-joint failure | 6% | 1–3 weeks | Visible leakage, air draft loss |
A 12-month precalciner and TAD maintenance timeline
The cadence below is calibrated for a 5,000 tpd line running 330 days/year. Shorter intervals apply to alternative-fuel or high-alkali operations where coating and build-up are more volatile.
Operational round & DCS review
Verify calciner exit temperature (880–920°C), TAD oxygen (2–3.5%), damper position, and NOx trend. Log any flame-shape change or CO excursion above 0.1%.
Burner pipe external inspection
Inspect primary-air fan curves, coal-feed consistency, and burner pipe movement. Check for refractory fall-out at the burner throat and document with photos.
False-air and damper audit
Run a mass-balance false-air test on the preheater and TAD. Calibrate damper position feedback and SNCR lances. Target total false-air below 8% of preheater gas flow.
IR thermography & coatings
Full-shell IR scan of calciner, riser, and TAD. Review coating-ring management plan and adjust meal-feed distribution. Inspect expansion-joint gaskets.
Burner pipe internal & SNCR service
Pull the burner pipe for nozzle-tip inspection, swirl-plate alignment, and channel pressure test. Service SNCR lances and atomizing-air nozzles. Replace worn tips.
Major outage & refractory campaign
Full 7-zone inspection. Ultrasonic thickness measurement at all datum points. Replace refractory below 60 mm, re-line TAD elbows as needed, and recalibrate the entire combustion control loop.
What false air and refractory drift really cost your plant
The economics of precalciner maintenance are unusually clean: every percentage point of false-air or refractory thinning you tolerate translates directly into specific heat consumption and lost clinker output. The formula and worked example below show the math.
Excess energy from false-air ingress
Where Efalse = wasted energy (kcal/h), Vfa = false-air volume (Nm³/h), Texit = preheater exit temperature (°C), Tamb = ambient temperature (°C). A 10% false-air rise typically adds 6–9 kcal/kg clinker.
A 5,000 tpd plant with 14% false air
- Baseline fuel 860 kcal/kg × 5,000 t = 4,300 Gcal/day
- Excess from 14% FA +9 kcal/kg = 45 Gcal/day
- Fuel cost @ $1.10/therm ≈ $2,080/day lost
- Annualized (330 days) ≈ $686,400 avoidable
- Refractory campaign cost $120K–$180K every 14 months
- Net payback of PM upgrade 5–7 months
How a precalciner CMMS keeps heat balance aligned
A purpose-built CMMS turns the inspection checklist and timeline above into a closed-loop system: every finding generates a work order, every work order links to an asset record, and every asset record feeds the heat-balance dashboard your process engineers already use.
Asset hierarchy & criticality
Model the calciner, burner pipe, TAD, damper, SNCR system, and cyclones as a structured hierarchy with criticality ratings. PM triggers flow automatically based on runtime, fuel type, and thermal loading.
Condition-based triggers
Integrate DCS tags — calciner exit temperature, TAD O2, NOx, damper feedback — so inspection work orders fire automatically when a threshold is breached, not just on a calendar date.
Mobile inspection rounds
Technicians complete the 7-zone checklist on a tablet at the asset, with photo capture, thickness readings, and voice notes that auto-attach to the work order and asset history.
Heat-balance dashboard
Track specific heat consumption, false-air %, calcination rate, and refractory thickness trends side-by-side. Spot drift before it becomes a 9 kcal/kg penalty.
Stop losing 9 kcal/kg to drift you can measure today
Deploy a structured precalciner and TAD maintenance plan with OxMaint — inspection checklists, condition-based PM triggers, and a heat-balance dashboard in one platform.
Precalciner and TAD maintenance — the questions plant managers ask most
How often should I inspect the calciner refractory?
Run an external IR shell scan monthly and a full internal ultrasonic thickness measurement at every major outage — typically every 12–14 months on a standard kiln line. If you burn alternative fuels or run high-alkali raw mix, shorten the internal inspection to every 8–10 months, because alkali-alumina reactions accelerate refractory wear by 20–35%.
What is the acceptable false-air level in the preheater and TAD?
Industry benchmark is below 8% of total preheater gas flow. Above 10% you are paying measurable fuel penalties (roughly 6–9 kcal/kg per 10% rise), and above 14% you should schedule a gasket and expansion-joint replacement at the next outage. A monthly mass-balance test takes under an hour and pays for itself within the first detected leak. Start Free Trial to automate the false-air audit inside your CMMS.
When should the calciner burner pipe be pulled for service?
Pull and inspect the burner pipe every 6 months on a coal-fired line and every 4 months if you co-fire alternative fuels. Replace nozzle tips when the tip-to-nozzle gap exceeds 4 mm or when you see flame-shape deviation, CO spikes above 0.1%, or a 5°C rise in calciner exit temperature at constant fuel input.
How do I know the TAD damper needs service?
The three leading indicators are positioner feedback error above ±2%, blade-edge wear above 5 mm, and binding or stalling during DCS-driven movements. If your damper cannot hold TAD oxygen within the 2–3.5% band at constant kiln draft, schedule blade inspection and actuator calibration within 30 days.
Can a CMMS actually improve precalciner thermal efficiency?
Yes — by closing the loop between inspection findings, work orders, and DCS trend data. Plants that deploy condition-based PM triggers on calciner exit temperature, TAD O2, and refractory thickness typically recover 3–5% in specific heat consumption within the first 6 months, because drift is caught at the weekly rather than the annual cadence. Book a Demo to see the precalciner module configured for your line.
Protect the 60% of combustion your kiln line depends on
Join the cement plants using OxMaint to keep precalciner performance, heat balance, and TAD reliability aligned — every shift, every outage, every year.
Free 14-day trial · No credit card required