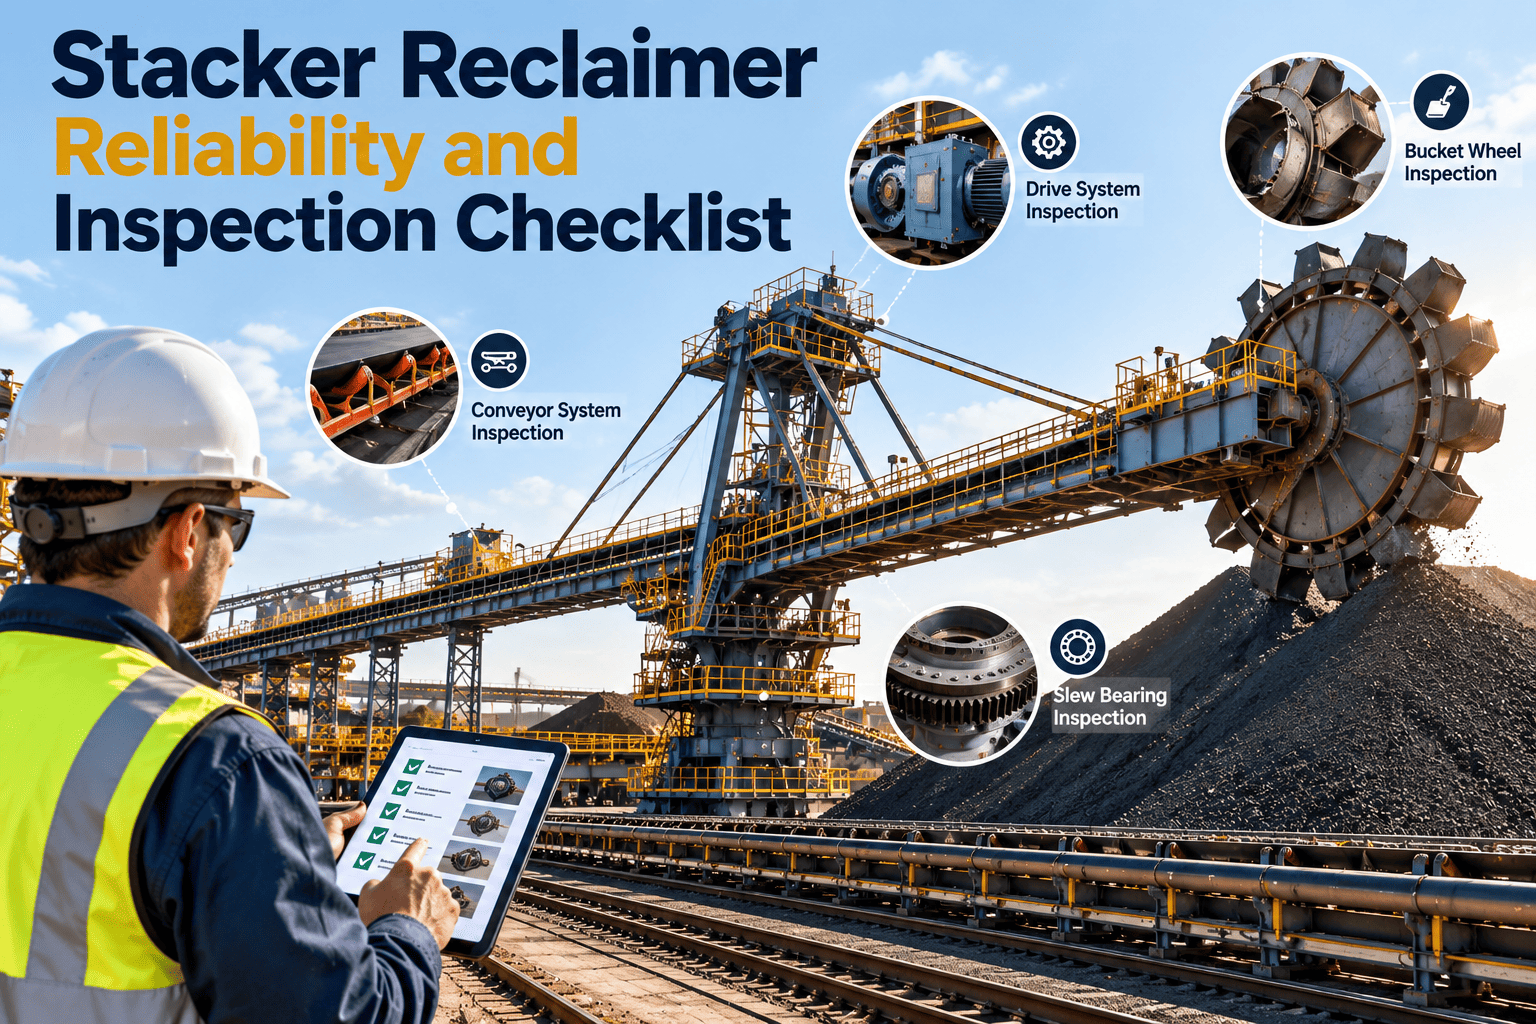
Stacker reclaimers are the quiet backbone of raw material preparation in a cement plant. They build and recover blending beds of limestone, additives and sometimes coal, so the raw mill sees a consistent feed. When a slewing drive, boom conveyor or rail wheel fails, the plant loses blending quality and then production. This checklist gives maintenance teams a practical way to inspect, trend and act on stacker and reclaimer condition, with records managed in Oxmaint.
Stacker Reclaimer Reliability and Inspection Checklist
Inspect the boom, slew, travel, bucket wheel or scraper, and bed conveyor as one reliability system. Use clear condition limits and escalation steps to protect blending bed availability.
Inspection Record Header
Complete this block before starting the checklist, and tick each item as it is verified in the field.
What Makes Stacker Reclaimers Hard to Keep Reliable
These machines are large, slow-moving and exposed. They work outdoors or in open sheds, in dust, rain and heat, and a defect can stay hidden until a rail or bearing fails under load.
Inspection to Action: The Reliability Loop
Stacking Mode and Reclaiming Mode: Two Checklists
A combined machine behaves differently depending on its duty. Inspect each mode with its own focus, and record which mode was active when a defect was found.
- Boom belt tracks centrally and loads evenly at the discharge point.
- Luffing system moves smoothly, with no jerking or oil leakage on hydraulic cylinders.
- Boom position sensors and height limits report correctly.
- Discharge chute is clear, and no material is building up on the boom tip.
- Dust suppression or enclosure at the discharge point is working.
- Pile height and shape match the stacking plan, with no overload condition.
- Tripper car or feed conveyor transfers are free of spillage.
- Bucket wheel or scraper turns without abnormal noise, and drive current is stable.
- Buckets, lips and wear liners are intact, with no cracks or missing teeth.
- Scraper chain or harrow tension is within the OEM range.
- Reclaim conveyor carries material without spillage or blockages.
- Slewing speed and cut depth are within set limits.
- Overload, torque and level protection devices function when tested.
- Bed face is stable and has no hang-ups or collapse risk.
Component Checklist by Machine Section
- Bearing bolts are present, with no loose, stretched or missing fasteners and no rust trails.
- Grease is present at the seal and raceway points, and the relubrication log is current.
- Drive gearbox oil level, colour and temperature are normal, and breathers are clear.
- Pinion and ring gear contact pattern is even, and wear is within allowed limits.
- Abnormal noise or vibration during slew is reported and trended.
- Welds and gussets are free from visible cracks, paint splitting or corrosion bleed.
- Pins and bushings show no excess clearance, and retaining devices are secure.
- Wire ropes show no broken wires, flattening, kinks, corrosion or poor spooling on drums.
- Hydraulic cylinders, hoses and fittings show no leaks, scoring or damaged guards.
- Counterweight and ballast fixings are secure.
- Wheels have no flange cracking, flat spots or one-sided wear that suggests misalignment.
- Rail clips, fishplates and joints are tight, and gauge has been surveyed on schedule.
- Rail ends, buffers and end stops are in good condition and clear of debris.
- Travel drives, brakes and couplings are checked for wear, noise and leakage.
- Cable reel or festoon system winds correctly without abrasion or tension spikes.
- Buckets and cutting edges are measured, and replacement timing is based on actual wear.
- Bucket wheel bearings and drive show normal temperature, oil condition and vibration.
- Boom conveyor idlers, pulleys, lagging and cleaners are inspected on the conveyor checklist cycle.
- Belt scale or weighing device is verified against a reference at set intervals.
- Transfer chutes are checked for wear and blockages.
- Limit switches, anti-collision sensors and emergency stops are function tested.
- Cabinet seals, filters and cooling are intact, with dust kept out of panels.
- Motor and cable terminations show no heat discolouration, checked by thermography where possible.
- Warning alarms, lights and communication links work as designed.
- Wind or weather protection logic, where fitted, is tested.
Put the Checklist on Every Operator's Phone
Create stacker and reclaimer inspection routes in Oxmaint, assign work orders from failed checks, and keep one history per machine section.
Failure Priority Matrix for Stacker Reclaimer Defects
Not every finding is equal. Rank defects by how likely they are to progress and how much damage they would cause if left.
Condition Indicators and Escalation Criteria
| Indicator | What to check | Maintenance response | Escalate if |
|---|---|---|---|
| Rising gearbox temperature | Oil level, cooling, load, breather, trend against past runs | Sample oil, correct cause, plan inspection | Temperature keeps rising or oil is contaminated |
| Metal particles in oil | Magnetic plug, lab sample, noise and vibration | Plan gearbox opening, check gear contact | Particle count rises quickly |
| Rope wear | Broken wires, diameter loss, corrosion, drum spooling | Plan rope change with parts ordered | Wire breaks exceed OEM or standard limits |
| Wheel flange wear | Rail gauge, wheel profile, lubrication, load distribution | Survey rail, correct alignment, replace wheel | Flange climbs rail or derailment signs appear |
| Bucket wear | Cutting edge height, cracks, tooth loss, cut depth | Weld repair or replace buckets in a window | Cracks extend into bucket wheel structure |
| Boom belt mistracking | Idlers, build-up, loading point, tail alignment | Align and clean, inspect structure | Belt contacts the boom frame |
| Cable reel faults | Spooling, slip rings, cable jacket damage, tension | Repair path, replace damaged section | Insulation damage or intermittent power loss |
Reactive Operation vs Condition-Aware Maintenance
- Defects are reported only after a trip.
- Wear parts are ordered when the machine stops.
- Rail and bearing issues are found at annual survey.
- Knowledge sits with a few experienced technicians.
- Operators log findings during every stacking or reclaiming cycle.
- Wear measurements drive part orders and shutdown scope.
- Temperature, vibration and oil trends signal drift early.
- Inspection steps and limits are written into shared templates.
How Oxmaint fits stacker reclaimer maintenance
- Asset hierarchy for each machine, with sub-assets for slew drive, boom, travel, bucket wheel and electrical.
- Preventive maintenance schedules for lubrication, rope checks, rail surveys and drive inspections.
- Mobile inspections with photo capture, so a cracked weld or leaking cylinder is documented at the point of finding.
- Work orders and spare parts tracking for buckets, ropes, wheels and gearbox seals.
- Dashboards and reports that show overdue inspections, repeat defects and downtime by machine.
Annual and Shutdown Inspection Scope
Some checks need isolation, access equipment and time. Plan these into major shutdowns, and track their completion in the same system as routine inspections.
Lubrication and Contamination Control Routine
Limestone dust is one of the fastest ways to shorten bearing and gearbox life. A lubrication route that is specific to each point will outperform a general greasing round.
- List every grease point and oil sump on the machine as a task with lubricant type, quantity and interval.
- Clean fittings before greasing, and record when old grease is seen purging from a seal, since this shows whether the seal is still working.
- Sample gearbox oil at set intervals, and keep results beside the asset so trends in wear metals, water and viscosity are visible.
- Check breathers and desiccant on drives that operate in humid or dusty conditions.
- Inspect centralised lubrication lines, pumps and distributor blocks for blockages, leaks and empty reservoirs.
- Record top-up volumes, because a sump that needs frequent topping up has a leak that should be repaired.
Weather and pile readiness checks
- Before the rainy or windy season, verify drainage around rails and pile edges, and check that wind alarms and storm parking procedures work.
- After heavy rain, inspect rails for washout, settlement or debris, and look for wet material that has bridged in chutes.
- In hot weather, watch gearbox and motor temperatures more closely and confirm that cooling fans and filters are clear.
- Where coal or petcoke is stacked, add temperature checks of the pile for self-heating, and keep records beside the stacker asset.
Shift Handover Notes That Prevent Repeat Problems
A good handover turns small observations into planned work. Ask each shift to record the same few items on every machine.
Spare parts worth holding for stacker reclaimers
- Bucket teeth, lips and wear liners that match the installed wheel or scraper design.
- Travel wheels or bearings for the most heavily loaded wheel positions, where lead times are long.
- Slew drive and travel gearbox seals, coupling elements and brake pads.
- Wire rope sets, sheave bearings and critical sensor assemblies such as position and limit devices.
- Cable reel brushes or slip ring components and spare protective relays.
Track minimum stock levels for these items in the maintenance system, so a worn component is known to be on the shelf before the shutdown starts.
Why Blending Bed Consistency Depends on Machine Condition
A stacker reclaimer does more than move material. Its stacking pattern and reclaim cut shape the chemical consistency of kiln feed, so mechanical drift shows up in process results.
- A worn or misaligned bucket wheel or scraper changes the cut profile, which can reduce the number of layers blended in each reclaim pass.
- Slew or travel speed variation, caused by drive wear or control faults, changes the layer thickness on the pile.
- An inaccurate belt scale distorts the stacked tonnage record and the reclaim rate, so the bed plan and the real pile drift apart.
- Frequent trips interrupt stacking or reclaiming, creating uneven layers that the raw mill and process team have to compensate for.
Information worth sharing with the process team
- Planned outage dates for each machine, so material can be buffered in the other bed before work starts.
- Known mechanical limits, such as reduced reclaim rate or restricted slew range, along with expected repair dates.
- Calibration status of weighing and position devices, with the date of the last verification.
KPIs for Blending Bed Machine Reliability
- Availability by machineRun time against scheduled time for stacker and reclaimer duties separately.
- Mean time between failuresTracked by section, so drive, boom and conveyor issues are not hidden in one number.
- Planned maintenance complianceCompleted preventive tasks against those due, including lubrication and rail checks.
- Wear part lifeBucket, rope and wheel life compared with expected life to refine replacement intervals.
- Open defect ageHow long inspection findings stay open before a work order is closed.
Stacker Reclaimer FAQs
Protect Blending Bed Availability With Better Inspection Data
Give your team one place to inspect, trend and repair stacker and reclaimer assets. Start with one machine, then extend the routine across material handling.