A fleet shop can have enough technicians on the clock and still run behind. The reason is often mismatch: a brake job lands on someone who is not certified for it, a diagnostic sits waiting for the one person who can read the fault codes, or a lift is free while the right technician is on another job. Scheduling by skill and availability fixes that by matching each work order to a qualified person at a realistic time. This guide walks through how to do it, and where Oxmaint scheduling and work order features can support the process.
Fleet Technician Scheduling by Skill and Availability
Match the right technician, the right bay, and the right parts to every job, so qualified labor is never waiting and unqualified labor is never guessing.
Headcount scheduling hides the real constraint
Counting technicians per shift tells you how many hands are available, not whether the right hands are available for the work waiting. Four constraints cause most schedule failures.
Symptoms you may recognize
- Specialists are pulled into routine PM work while complex repairs wait.
- Jobs are reassigned midway because the first technician lacked the skill or the time.
- Comebacks rise on work done by less experienced staff without support.
- Vehicles sit in bays waiting for parts or a free technician.
Build a skills matrix that dispatchers will actually use
List the competencies your fleet needs, then record each technician's level and the evidence behind it. Keep levels simple so they can be maintained.
| Skill area | Examples in a fleet shop | Possible evidence | Scheduling use |
|---|---|---|---|
| Brakes and suspension | Air brake service, wheel-end work, steering and alignment | ASE medium and heavy truck tests for brakes and suspension, plus internal sign-off | Safety-critical jobs assigned only to qualified staff |
| Engine and aftertreatment | Diesel diagnostics, regeneration faults, injector and turbo issues | ASE diesel engine test, manufacturer training | Complex diagnostics routed to certified technicians |
| Electrical and electronics | Wiring faults, module work, lighting systems, telematics installs | ASE electrical test, in-house practical assessment | Intermittent faults handled by experienced staff |
| Preventive maintenance inspections | Scheduled PM services and annual inspections | Inspector qualification records, ASE preventive maintenance test | Regulated inspections signed by qualified inspectors only |
| Climate and refrigeration | Cab air conditioning, reefer units | Refrigerant handling certification where required, OEM training | Specialized work held for certified personnel |
| High-voltage and EV systems | Battery, charger, and inverter service | Manufacturer or industry high-voltage training | Restricted to trained and authorized staff |
| Road test and driving | Moving vehicles in and out of the yard, road tests | Valid license with the required class and endorsements | Assign only those cleared to drive the vehicle type |
A weekly view that reflects reality, not wishes
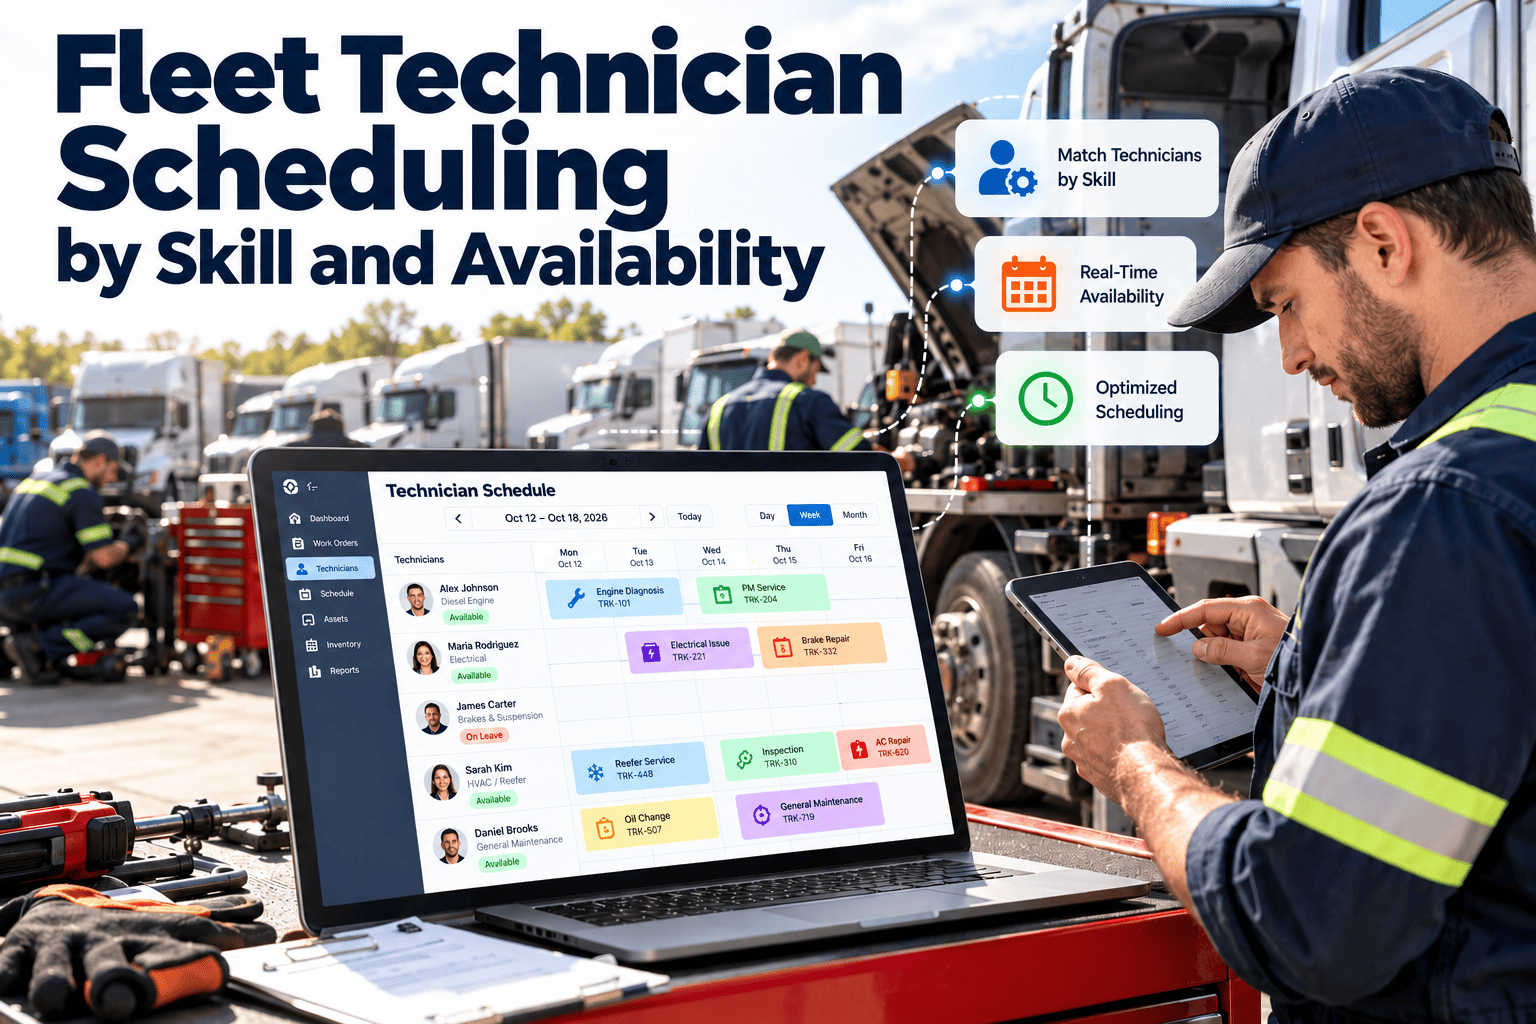
The board below is illustrative. It shows how work can be organized by lane, with each lane tied to the skills and equipment it needs.
A priority ladder that settles conflicts quickly
When two jobs compete for the same technician, a written ladder removes the argument. Adjust the order to your operation.
Put the right technician on the right job before the shift starts
See how work orders, due dates, and technician assignments can be organized in one maintenance system.
How to assign a job in seven checks
Whether a planner does this by hand or a system suggests it, the logic is the same.
Do not schedule a job that cannot start
A technician assigned to a job with no parts or no vehicle is lost labor. Add simple gates before a job enters the schedule.
What improves when scheduling uses skill and availability
Metrics that show whether scheduling is working
| Metric | What it shows | Watch for |
|---|---|---|
| Wrench time | Share of paid hours spent on actual repair work | Time lost waiting for parts, bays, or instructions |
| Schedule adherence | Jobs started and finished as planned | Frequent reassignments mid-job |
| PM on-time completion | Services done within their interval window | PM pushed aside by breakdown work |
| First-time fix rate | Repairs resolved without a return visit | Skill mismatch or poor diagnostics |
| Comeback rate | Repeat repairs on the same issue | Concentration on particular jobs or technicians |
| Backlog age | How long open work orders have been waiting | Low-priority items that quietly become risks |
A practical three-stage rollout
Reduce single-point dependence on one expert
If only one technician can handle a job type, the schedule is as fragile as that person's calendar. Cross-training turns bottlenecks into depth.
Better time estimates make better schedules
A schedule built on optimistic durations collapses by midday. Ground your estimates in the shop's own history.
- Record actual labor hours on every closed work order, by task type and vehicle class.
- Use manufacturer labor guides as a reference, then adjust for your fleet's age and condition.
- Add a margin for diagnostics on jobs where the cause is not yet known.
- Review estimates against actuals monthly and correct the tasks that miss most often.
- Separate the time a job takes from the time it waits, so planners see both.
Keep work moving across shifts and absences
Jobs often span more than one shift, and absences are a normal part of any week. Plan for both before they happen.
When a job should leave the shop
Keeping every job in-house is not always efficient. Use clear criteria to decide when outside help makes sense.
| Situation | Typical choice | Record to keep |
|---|---|---|
| Skill or tool the shop does not have | Sublet to a specialist or dealer | Vendor, invoice, and warranty terms on the work order |
| Capacity peak with routine work waiting | Sublet lower-risk jobs to protect in-house safety work | Return date and completion sign-off |
| Warranty or program work | Use the authorized provider | Authorization reference and claim notes |
| Repeat in-house failures on one task | Review training or sublet until competence improves | Comeback history and corrective action |
Scheduling errors that quietly cost shop capacity
A daily routine that keeps the weekly plan honest
The weekly board sets intent, but the day decides what actually happens. A short, consistent routine keeps the two aligned.
Scheduling that respects the people doing the work
Skilled technicians are hard to hire and hard to replace. A schedule that overloads the best people burns them out, while one that never challenges others stalls their growth.
- Spread complex and unpleasant jobs across qualified staff rather than always defaulting to the same person.
- Track overtime by technician and look for patterns that signal a structural capacity gap.
- Give developing technicians planned exposure to harder work with support nearby.
- Share the schedule early, so staff can plan their time and flag conflicts before they cause delays.
- Use completion and comeback data to coach, not to punish, and to recognize strong work.
Treat bays and special tools as schedulable resources
A shop with six technicians and two lifts can only run two lift jobs at once. Add the scarce resources to the plan, not just the people.
- List the equipment that limits throughput, such as alignment racks, pits, tire machines, and diagnostic tools.
- Book those resources against each work order, so conflicts appear before the shift begins.
- Group jobs that need the same equipment into one block to reduce setup and idle time.
- Track calibration and maintenance dates for shop tools so they are available when needed.
How Oxmaint supports skill and availability scheduling
Oxmaint organizes the work, the assets, and the people involved so planners can see what is due and who can do it.
- Work orders with priority, due dates, assigned technician, status, and notes.
- Preventive maintenance schedules that generate recurring work ahead of time.
- Asset records and history so technicians see prior repairs before starting.
- Inventory visibility to check parts before committing a job.
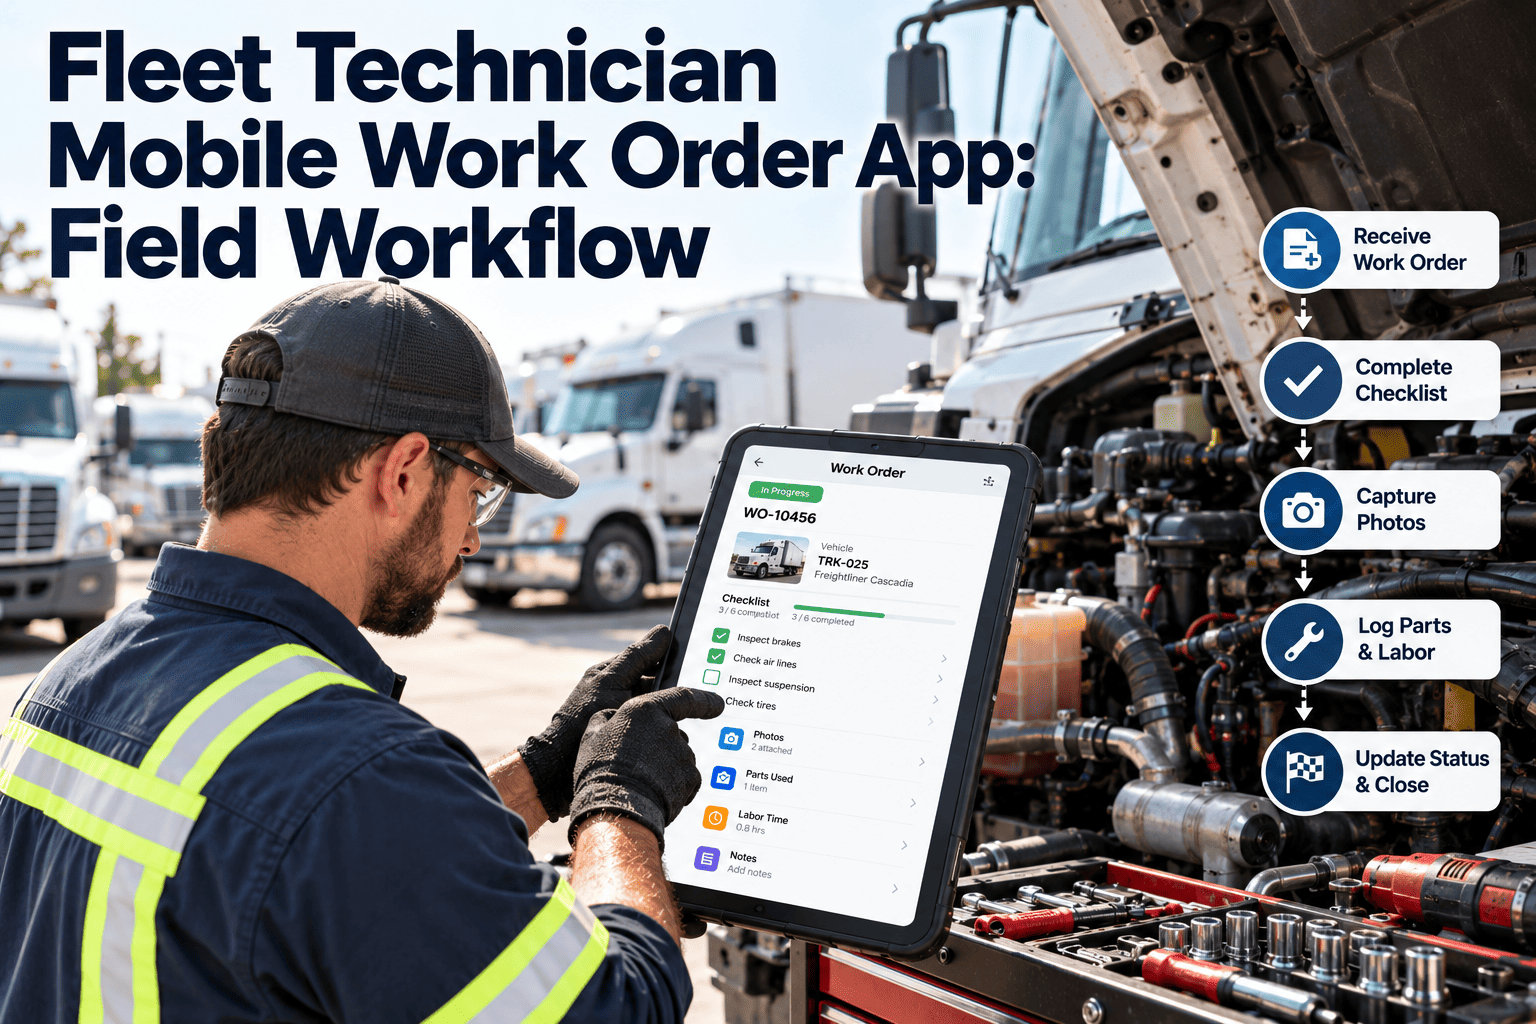
- Mobile access so technicians update progress, parts, and findings at the vehicle.
- Reports on backlog, completion, and workload that guide staffing and training decisions.
Frequently asked questions
Turn technician time into completed work, not waiting time
Plan jobs around skill, availability, parts, and bay capacity, and keep every assignment visible in one maintenance workflow.