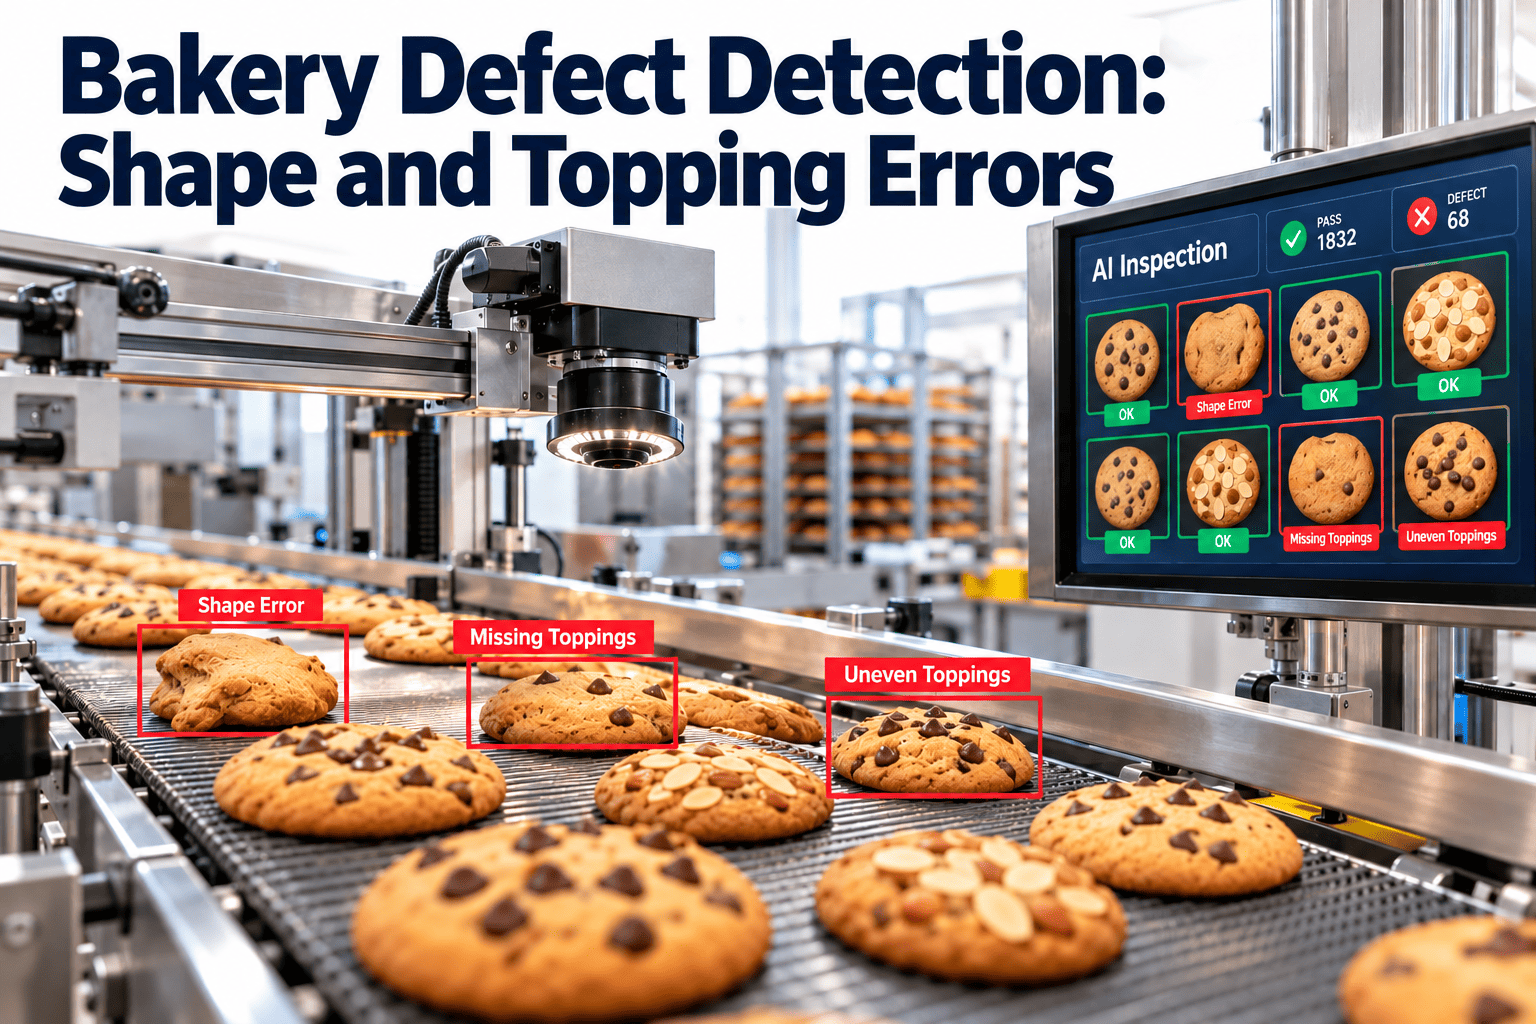
A loaf that leaves the oven slightly oval, a pizza base with bare patches, a bun a few millimetres short of specification: each looks minor on its own. Together they drive rework, giveaway, customer complaints and rejected loads. Bakery defect detection for shape and topping errors catches these faults while product is still moving on the belt and ties each fault to the line and machine behind it. Teams that feed those findings into a maintenance management platform turn rejects into work orders instead of recurring surprises.
Bakery Defect Detection: Shape and Topping Errors
Detect deformed shapes, missing toppings and size variation automatically, record the trend by line, and fix the machine cause before the next shift repeats it.
Shape and topping errors cost money in four quiet ways
Most bakeries already know their scrap number. Fewer know what appearance defects cost once giveaway, complaints and manual sorting are added.
Rework and scrap
Deformed or undersize product fails the specification and is scrapped, downgraded or reworked. One bad hour can affect thousands of units.
Giveaway
Oversize pieces and heavy topping use extra dough and ingredients per unit. The loss rarely shows up as a single event.
Customer rejection
Retail and foodservice buyers specify appearance. Bare patches and uneven shape trigger complaints, chargebacks and listing risk.
Line interruptions
Operators who spot faults by eye stop the line or sort by hand, which pulls skilled people away from production.
Trace every visual defect back to a stage on the line
A shape or topping error seen at the packing end usually started several machines earlier. Mapping defects to stages shows where to look first.
Dividing and sheeting
Weight and thickness drift here becomes size variation later. Check blades, roller gaps and hopper feed.
Moulding and forming
Worn belts, uneven roller gaps and misaligned guides create oval, folded or open-seam pieces.
Proofing
Uneven temperature or humidity across the proofer slumps some pieces and over-proofs others.
Topping application
Clogged depositor nozzles, sticky seeder gates and weak sprayers cause missing, clumped or off-centre topping.
Baking
Zone imbalance, damper faults or conveyor speed drift change spread, colour and surface cracking.
Cooling and transfer
Rough transfers and tracking errors bump, merge or crush product before it reaches packaging.
Common shape and topping defects and the equipment behind them
Use this table to turn a reject code into a first inspection target.
| Defect | What the camera sees | Likely cause | Check first |
|---|---|---|---|
| Oval or distorted shape | Aspect ratio outside the template | Uneven roller gap, worn belt, proofer slump | Moulder, belts, proofer zones |
| Undersize or oversize | Length, width or area off target | Divider weight drift, sheeting thickness | Divider, sheeter, hopper feed |
| Missing topping | Low coverage in one or more zones | Empty hopper, blocked nozzle, stuck gate | Depositor, seeder, shredder feed |
| Uneven or clumped topping | High coverage variance between zones | Vibration, wrong viscosity, worn dosing parts | Dosing unit, hopper agitator |
| Off-centre topping | Topping centroid shifted from product centre | Belt tracking, timing between sensor and depositor | Belt tracking, photo-eye timing |
| Cracked or torn surface | Contour breaks, colour contrast lines | Dry proofing, oven humidity, sheeting stress | Proofer humidity, oven steam |
| Merged or touching pieces | Two outlines detected as one | Spacing error, belt speed mismatch | Pattern settings, transfer points |
Three inspection layers on one camera view
Machine vision systems compare each product image against a reference. Lighting, camera position and a reject mechanism complete the setup.
Size inspection
- Length, width and diameter
- Projected area
- Height, where 3D sensing is used
- Count per tray or per pitch
Shape inspection
- Roundness or aspect ratio
- Contour match to a template
- Symmetry and edge breaks
- Touching or merged outlines
Topping inspection
- Coverage percentage
- Distribution across zones
- Piece count, such as slices
- Colour and presence checks
Detection quality depends on contrast between product and topping. Test any system on your real product, at line speed, before setting reject limits.
Zone-based coverage checks catch what an average hides
Average coverage can look fine while one edge is bare. Splitting the product into zones exposes the pattern.
Reading the pattern
- Illustrative example: zones 3, 6 and 9 run low on one edge
- A one-sided pattern points to belt tracking or nozzle position
- Random bare zones point to hopper flow or blocked dosing
- Low coverage everywhere points to supply or setting changes
Set a three-band tolerance ladder, not a single cut-off
A single pass or fail limit hides drift. Three bands give maintenance time to act before product is rejected.
Accept
Within the target band. Log the measurement and keep running.
Alert
Trending toward the limit. Raise a work order for inspection at the next planned stop.
Reject
Outside the limit. Divert product, flag the line and open a corrective work order.
- Base limits on customer specifications and internal quality standards, not on what the camera can detect
- Set separate limits for each product code, since a flatbread and a bun behave differently
- Require a rework or hold decision for rejected product so it is never mixed back silently
- Review limits after any recipe, tooling or line speed change
Record defects as trends so repeat faults stand out
One reject is an event. The same reject at the same hour every day is a maintenance finding.
| Measure | How to read it | Maintenance response |
|---|---|---|
| Reject rate by defect type and line | Shows which fault dominates on which line | Prioritise the dominant cause for inspection |
| Reject rate by shift and product | Separates people, recipe and machine effects | Compare against changeover and cleaning events |
| Size capability (Cpk) on length or diameter | Falling capability signals drift before rejects rise | Check dividers, sheeters and moulders |
| Average coverage and spread | Wide spread means inconsistent dosing | Service depositors and seeders |
| Time between repeats of the same defect | Short gaps mean the fix did not hold | Review root cause, parts and method |
| Vision system calibration status | Overdue checks undermine every number above | Schedule lens cleaning and reference checks |
Turn every reject into a traceable maintenance action
Log defects by line, link them to the asset behind them and track the fix to closure in one workflow.
From detection to repair in five steps
Detection only pays off when the finding reaches the technician who can fix the cause.
Detect
The vision system flags size, shape or coverage outside limits.
Classify
The defect is coded by type, line, product and time.
Trigger
A corrective work order is raised against the suspect asset.
Fix
The technician repairs, adjusts or replaces and records parts used.
Verify
Quality confirms the defect rate falls before the order closes.
Oxmaint does not replace vision hardware. It manages the maintenance side: assets, work orders, schedules, inspections, spares and reporting.
Preventive tasks that protect shape and topping quality
Most visual defects trace to a small set of wear and cleanliness issues. Schedule them as preventive tasks with checklists.
Depositors and seeders
- Clean and inspect nozzles and gates each changeover
- Check dosing parts for wear
- Verify hopper agitators and level sensors
- Confirm timing with product detection sensors
Dividers, sheeters and moulders
- Inspect blades and roller surfaces
- Measure roller gaps against setpoints
- Check belts for wear and tracking
- Lubricate to the manufacturer schedule
Proofers and ovens
- Verify temperature and humidity sensors
- Check zone balance and dampers
- Inspect steam systems and burners
- Confirm conveyor speed against setpoint
Vision and reject systems
- Clean lenses and lighting covers
- Run reference piece checks
- Test the reject device each shift
- Back up recipes and limits
Where bakery inspection technology is heading
Inspection hardware is improving quickly, but the maintenance demands grow with it. Each upgrade adds sensors, software and calibration work that someone has to own.
Learning-based vision
Newer systems learn what acceptable product looks like from sample images, which helps with natural variation in baked goods. They still need clean optics, stable lighting and regular review of rejected samples.
3D and height sensing
Height and volume checks catch under-proofed or collapsed product that looks acceptable from above. These sensors need protection from flour dust, steam and vibration.
Line-level data
Inspection results are increasingly stored by line, product and time. That history is only valuable if it can be compared with maintenance activity on the same assets.
Condition-based triggers
Rising alert counts can trigger an inspection before rejects occur. Teams define the trigger, such as repeated low coverage on one edge, and the work order follows.
Mistakes that quietly undermine defect detection
Many installations disappoint because of maintenance and process gaps, not because the camera is wrong.
Flour dust, oil mist and steam film on lenses reduce contrast and create false rejects. Put lens cleaning on a shift-based checklist.
Reject limits copied from another line cause either constant stoppages or missed defects. Tie limits to customer specifications.
When operators change settings without logging them, nobody can link a trend to its cause. Require an entry for every change.
A detection system is only useful if the pusher or air jet removes the right piece. Test the diverter at each start-up.
Many topping errors start after a product change, when settings and cleaning are rushed. Include a post-changeover check in the schedule.
Keep the evidence customers and auditors ask for
Appearance defects are mainly a quality issue, but buyers and certification auditors still expect documented control of monitoring equipment.
- Calibration and reference check records for vision systems and reject devices
- Preventive maintenance completion records for depositors, seeders, ovens and conveyors
- Corrective work orders showing cause, action and verification for repeat defects
- Hold and rework decisions for rejected product, with date, line and product code
- Spare part usage for nozzles, belts and sensors tied to the asset
Where a monitoring device supports a food safety control, calibration and verification records carry extra weight. Confirm requirements with your quality team and certification scheme.
A simple per-shift routine that keeps detection reliable
Small, repeatable checks at the right moments prevent most false rejects and missed defects.
Verify the system
Wipe lenses, run a reference piece, confirm the correct product recipe is loaded and test the reject device.
Confirm settings
Check depositor position, roller gaps and topping weight, then review the first coverage and size readings.
Review the trend
Look at alert counts by defect type. A rising alert trend is the cue to inspect before rejects begin.
Log and hand over
Record defects, adjustments and open work orders so the next shift starts with the full picture.
What changes when defect data feeds maintenance
The difference shows up in how quickly causes are found and how often they return.
Without a connected workflow
- Rejects are counted but not traced to an asset
- Operators adjust settings without a record
- The same nozzle or belt fault returns weekly
- Calibration checks depend on memory
- Audit evidence sits in paper logs
With defects linked to work orders
- Each defect type points to a suspect asset
- Adjustments and repairs are logged with the order
- Repeat faults trigger root cause review
- Calibration is scheduled and tracked
- History is searchable by line and date
A practical four-stage rollout for one line
Start with the line that has the highest reject cost, prove the loop, then replicate.
Register assets
List every machine on the line with location, model and critical spares.
Define defect codes
Agree one code list across quality, production and maintenance.
Build schedules
Create preventive tasks and mobile checklists for the high-risk assets.
Review weekly
Compare defect trends with work orders and adjust limits and tasks.
Bakery defect detection questions
What defects can automated bakery inspection detect?
Typical systems check size, shape, colour and topping presence or coverage. Results depend on contrast and lighting, so validate on your own product.
How do I reduce missing toppings?
Schedule nozzle, gate and hopper checks at every changeover and log coverage trends. You can set up those tasks in Oxmaint as recurring work orders.
Does Oxmaint perform image inspection?
No. Oxmaint manages the maintenance workflow around your inspection system, including assets, work orders, schedules and reporting.
How often should vision systems be calibrated?
Follow the manufacturer guidance and add a reference piece check each shift. A recurring task keeps it from being missed.
Can I see how this fits my lines?
Yes. Book a short demo and walk through your assets and defect codes with the team.
Fix the machine behind the defect, not just the product
Connect shape, size and topping findings to preventive and corrective maintenance for every bakery line.