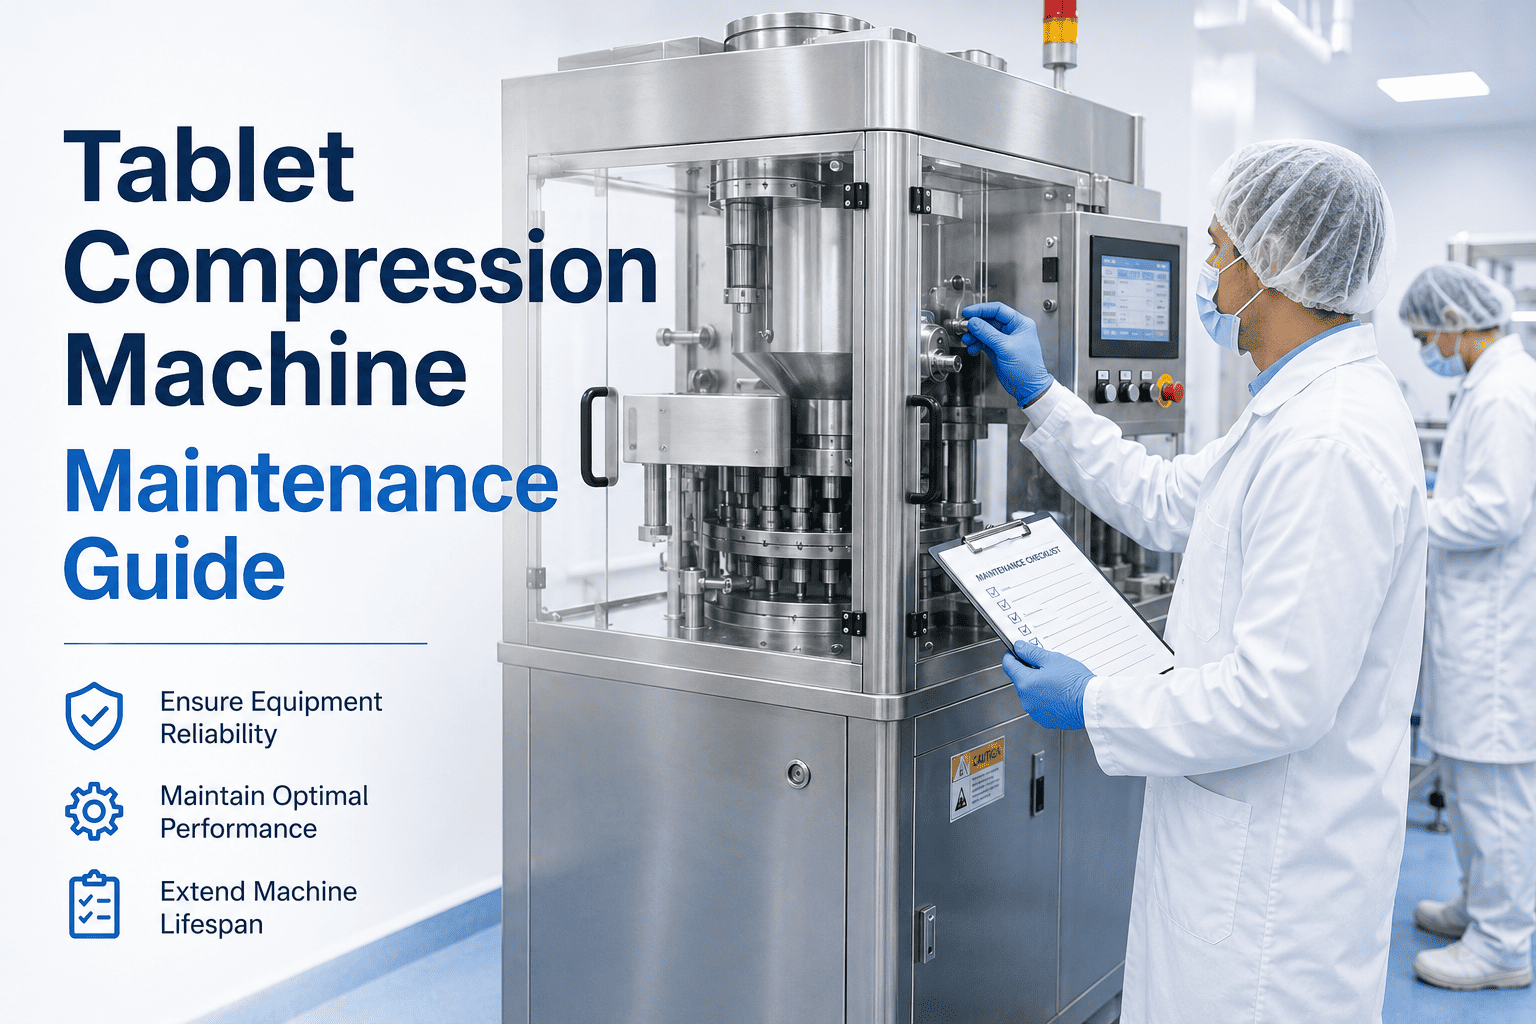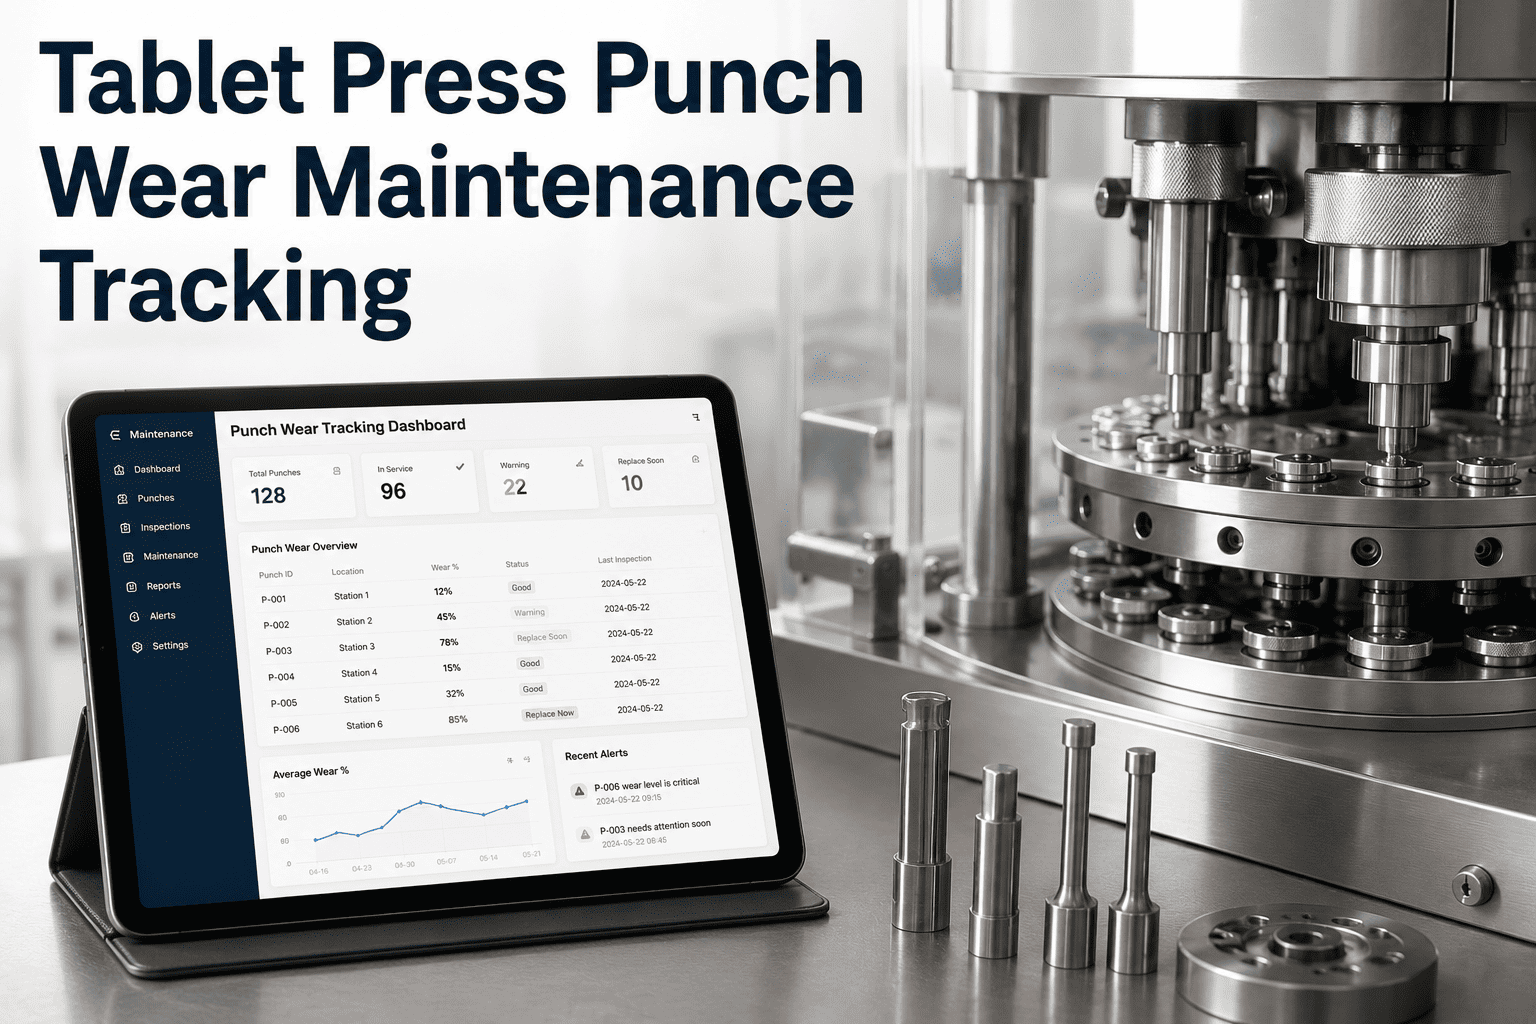
A single worn punch hiding inside a 40-station turret can quietly produce out-of-spec tablets for hours before anyone notices a pattern. Punch wear tracking software closes that gap by logging compression cycles against every punch ID, flagging force drift and turret vibration in real time, and turning a silent wear curve into a scheduled tooling swap. Instead of discovering the problem in a failed weight-variation test, your team sees it three shifts earlier — while the batch is still good. Below is how wear actually develops, what it costs when it is missed, and how a connected CMMS workflow catches it first.
The Punch Wear Curve Nobody Is Watching
Punch heads take 20,000 to 50,000 compression cycles every hour. Long before a punch visibly fails, it is already shifting tablet weight, hardness, and dissolution — and most plants have no system tracking the cycle count that predicts it.
Four Warning Signals Before a Punch Fails
Wear does not announce itself with a broken part. It shows up as drift, first in data, then in the tablets themselves.
Compression Force Drift
Force readings per station begin spreading away from the batch average as the punch tip geometry changes shape.
Turret Vibration Rise
Bearing and cam-track wear introduce vibration frequencies that climb steadily for two to three weeks before failure.
Weight Variation Creep
Worn punch tips and die-bore clearance let fill volume drift, pushing individual tablets toward the ±0.5 percent limit.
Sticking and Picking
Heat from punch friction and surface wear causes granulation to adhere to the punch face, marking tablet after tablet.
What One Missed Punch Inspection Actually Costs
A batch is not rejected because a punch broke. It is rejected because nobody connected a small force anomaly to a tooling problem until quality testing caught it downstream — by then the whole lot is on hold.
- QualityFull batch discard when weight variation exceeds the ±0.5% specification
- ComplianceUnsigned or missing PM records under 21 CFR 211.68 trigger 483 observations
- ProductionUnplanned mid-run stoppage when sticking forces an emergency changeover
- Root CauseIntermittent defects misread as random variation instead of one worn station
See Punch Wear Tracking Running on a Live Press
Walk through how OxMaint logs cycle counts per punch ID, flags force and vibration drift, and auto-generates the GMP-ready PM record before a batch is ever at risk.
Manual Tooling Checks vs Tracked Punch Lifecycle
Most plants still rely on visual inspection at changeover. Here is the practical difference a cycle-tracked system makes.
| Maintenance Approach | Manual Visual Check | Cycle-Tracked CMMS |
|---|---|---|
| Wear detection point | After visible damage or defect | 2-3 weeks before failure via vibration trend |
| Punch identification | By station number only | Serialized ID with full usage history |
| Force drift visibility | Not tracked between QA samples | Logged per station, per cycle |
| Audit record | Paper log, easy to miss a signature | Timestamped, attributable, 21 CFR Part 11 ready |
| Replacement timing | Reactive, after a quality event | Scheduled at planned changeover window |
How the Tracking Workflow Actually Runs
Three checkpoints turn raw press data into a maintenance decision before quality ever sees a deviation.
Cycle Counter Per Punch
Every punch gets a serialized ID. Compression cycles accumulate against that ID, not just the station, so wear-out is predictable per tool, per supplier, per formulation.
Drift Threshold Alert
When force variance or vibration amplitude crosses a set threshold, a work order is generated automatically and routed to the maintenance queue with the station ID attached.
Logged PM Record
The replacement, inspection notes, and operator signature are captured digitally — ready for a 21 CFR Part 11 audit without anyone re-typing a paper log.
Tooling failures rarely come from one bad punch — they come from nobody tracking the cycle count against the wear curve. The moment a facility serializes its tooling and watches force drift per station, batch-related tooling rejects drop sharply within the first quarter.
Frequently Asked Questions
Stop Finding Out About Punch Wear From a Failed Batch
Give every punch a tracked lifecycle, every drift signal a threshold, and every PM a digital signature. Start on one press or roll it out across the line.