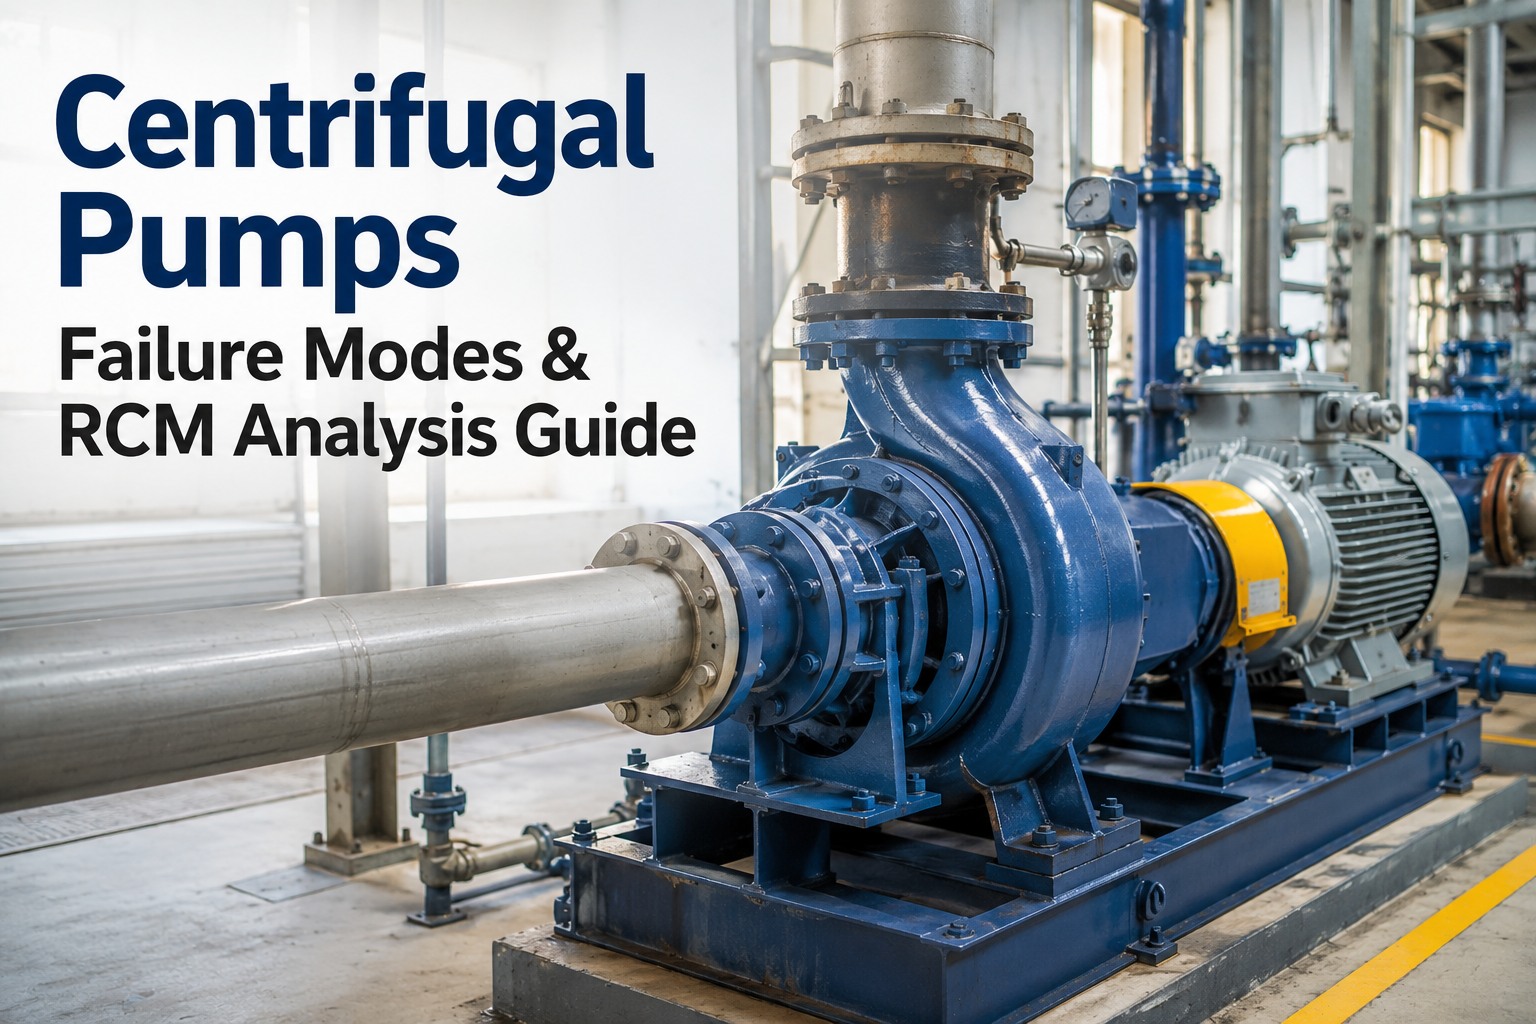
Ask a plant why its centrifugal pumps keep failing and most will point at the mechanical seal — it accounts for roughly 69% of pump breakdowns, after all. But that number is a trap. The seal is usually the victim, not the culprit: misalignment, bearing wear, cavitation, and dry-running destroy seals as a secondary effect, so replacing the seal without tracing the root cause just resets the clock on the next failure. That's exactly the gap FMEA and RCM close. Instead of reacting to the symptom, a structured failure-mode analysis maps how a pump actually fails, what each mode really stems from, how to detect it early, and which maintenance task addresses it — so effort lands on root causes, not repeat repairs. This guide walks the full analysis for centrifugal pumps: the dominant failure modes and their true root causes, the detection signatures that catch each one early, the RCM task strategies, criticality ranking, and the condition-monitoring overlay that keeps the whole thing live. Book a live RCM demo against your own pump fleet.
The Seal Gets Blamed. The Root Cause Gets Missed.
69% of pump failures show at the seal — but misalignment, cavitation, and bearings are usually why.
69%
Of pump breakdowns surface at the mechanical seal — often as a symptom
NPSH
Insufficient suction head is the root cause of cavitation — keep 10% margin
2–3 mils
Of shaft misalignment can cut bearing L10 life by 50% or more
±20%
Of BEP — the flow band pumps should run within to avoid damage
The Dominant Failure Modes · And Their Real Root Causes
FMEA is the analytical engine of RCM — it answers how a pump fails and what each failure actually stems from. For centrifugal pumps, a handful of modes account for most downtime, and they cascade into one another. The critical insight: the visible failure is often not the root cause.
~69%
Mechanical Seal Failure
Symptom more than cause. Face wear, O-ring degradation, and leakage — but usually driven by misalignment, bearing wear, dry-running, chemical attack, or cavitation. Trace it back or it recurs.
Root
Cavitation (NPSH Deficiency)
Gravel-like noise, broadband vibration. Vapor bubbles form when suction pressure drops below vapor pressure, then collapse and pit the impeller. Root cause: insufficient NPSH — clogged strainers, excess suction lift, hot fluid.
Root
Bearing Failure
The hidden driver. Misalignment is the leading contributor — even 2–3 mils of offset can halve L10 life through radial loading. Failing bearings then transfer vibration straight into the seal.
10–25%
Impeller Damage & Imbalance
Erosion, pitting, fouling, broken vanes. Shows as 1x running-speed vibration for imbalance and vane-pass-frequency energy for hydraulic issues — accelerates both bearing and seal wear.
Detection Signatures · Catching Each Mode Early
The value of the FMEA is in the detectability column — knowing the early signature of each mode is what moves a pump from run-to-failure to condition-based. Each failure writes a distinct fingerprint across vibration, performance, and the senses.
Failure Mode
Early Signature
Best Detection
Cavitation
Gravel/crackling noise, broadband 1–10 kHz vibration, unstable discharge pressure
Vibration + NPSH check
Bearing failure
Bearing defect frequencies, rising temperature, later audible noise
Vibration analysis + thermography
Seal failure
Visible drip/leak, contamination, seal-chamber temperature rise
Leak inspection + temperature
Impeller imbalance
1x running-speed vibration, vane-pass-frequency energy, head drop
Vibration FFT + performance
Misalignment
1x/2x radial vibration, coupling wear, elevated bearing load
Vibration + laser alignment
Wear-ring / internal wear
Falling flow and head, rising power draw, internal recirculation
Performance trending
See RCM Live on Your Pump Fleet in 30 Minutes
Working session with our reliability team — bring your pump list. We'll rank them by criticality, map failure modes to their true root causes and detection tactics, and show how OxMaint auto-generates PM and condition-based work orders from vibration and performance triggers.
The Four RCM Task Strategies · Where Each Mode Lands
Once the FMEA maps the modes, RCM routes each to one of four maintenance strategies by failure pattern and consequence. Matching the mode to the right strategy is the whole point — it's why RCM beats a flat calendar that can't tell a cavitation problem from a bearing one.
On-Condition
Predictive / Condition-Based
For modes with a detectable P-F interval. Vibration trending, performance monitoring, and temperature catch bearing, cavitation, and impeller faults early — the primary strategy for critical pumps.
Scheduled Restoration
Time / Usage-Based
Restore or replace at a fixed interval before wear-out — seal-kit replacement, wear-ring renewal, bearing regrease and change on a known service life.
Failure-Finding
Hidden-Function Check
Periodic tests for functions you can't see fail — standby pumps, minimum-flow recirculation lines, low-suction trips — so a hidden failure doesn't surface only on demand.
Run-to-Failure
Deliberate Acceptance
A conscious choice for low-consequence pumps where prevention costs more than the failure — a small non-critical transfer pump with a spare on the shelf, not a process-critical unit.
Criticality Ranking · Not Every Pump Earns the Same Analysis
RCM analysis takes time, so it's spent where consequences justify it. The same pump model is a run-to-failure asset on a non-critical sump and a fully-analyzed critical asset on a process-critical duty. Rank first, then invest the analysis depth accordingly.
CRITICAL
Process-Critical & No-Spare Pumps
Single-point-of-failure pumps on the main process, hazardous or high-head duties. Failure stops production or creates a safety event — full FMEA plus continuous condition monitoring.
IMPORTANT
Pumps With Redundancy
Duty/standby pairs or units with a tolerable short outage. Targeted FMEA on the dominant modes, condition-based tasks on bearings and seals, scheduled restoration on wear parts.
NON-CRITICAL
Utility & Low-Duty Pumps
Sump, transfer, and low-consequence pumps where a short outage is a non-event. Simple inspection or a deliberate run-to-failure decision — no analysis overhead required.
The Condition-Monitoring Overlay · Keeping It Live
An FMEA is only valuable if something is actually watching the signatures it identified. The mode that ranked "detectable by vibration" only helps if a sensor is trending that vibration. This is where a live CMMS overlay turns a static analysis into an operating discipline.
Sensors Watch the Signatures
Vibration, temperature, suction/discharge pressure, and flow sensors track exactly the parameters the FMEA flagged — bearing frequencies, cavitation broadband, NPSH margin, performance drift.
Thresholds Fire Work Orders
When a reading breaches its limit, the system auto-generates a work order tied to the specific predicted failure mode — with the right seal, bearing, or wear ring and procedure staged.
Findings Feed Back
When technicians close the work order, the measured root cause returns to the failure history — keeping the FMEA live and improving it, so recurring seal failures finally get traced to source.
How OxMaint Runs RCM for Centrifugal Pumps
OxMaint embeds RCM directly into execution — failure-mode libraries in the asset record, criticality scoring that drives task selection, condition-monitoring triggers, auto-generated work orders at RCM-defined intervals, and cloud reliability reporting that replaces spreadsheet RCM, from one dashboard on desktop or mobile.
FMEA
Live Failure-Mode Libraries
Pump failure modes and their root causes loaded into each asset record, linked to work-order templates and condition triggers — not stranded in a spreadsheet.
Criticality
Consequence-Driven Scoring
Rank and color-code every pump by process criticality and redundancy, so PM strategy follows risk instead of a flat calendar.
Condition
Vibration & Performance Triggers
IoT, SCADA, and vibration data convert cavitation, bearing, and performance alerts into prioritized work orders automatically — the P-F window put to use.
Work Orders
Auto-Generated by Interval
PM and condition-based tasks fire at RCM-defined intervals with seals, bearings, and wear parts staged — mobile-first, with offline mode and QR asset tags.
Feedback
Root-Cause History
Closed-work-order findings feed the failure record, so the seal that keeps failing finally gets traced to the misalignment or cavitation behind it.
Overlay
SAP & Maximo Support
Sit over existing SAP PM or IBM Maximo as the reliability layer, with cloud KPI reporting — one view across a single plant or a global network.
Stop Replacing Seals. Start Fixing Root Causes.
Replace spreadsheet RCM with a live program that ranks criticality, maps every failure mode to its true root cause, and turns vibration and performance data into work orders before the pump fails. See OxMaint on your own assets. Free forever plan available.
Frequently Asked Questions
What are the most common centrifugal pump failure modes?
The dominant modes are mechanical seal failure (which surfaces in roughly 69% of breakdowns but is usually a symptom of another problem), cavitation from insufficient NPSH, bearing failure (most often driven by misalignment), and impeller damage or imbalance from erosion, pitting, and fouling. Wear-ring and internal wear round out the list. The critical point for analysis is that these cascade and mask each other — a seal leak is frequently the visible end of a chain that started with misalignment or cavitation. That's why an FMEA traces each mode to its root cause rather than stopping at the component that visibly failed.
Book a demo to map yours.
Why is mechanical seal failure so often a symptom, not the cause?
Because the seal is the most delicate part of the pump and absorbs the consequences of nearly every other problem. Misalignment increases radial loading and shaft deflection that wears the seal faces; bearing wear lets the shaft move and destroys the seal; dry-running overheats it; cavitation and vibration hammer it; chemical incompatibility degrades its elastomers. So when a seal fails, replacing it without diagnosing why simply resets the clock — the same underlying misalignment or NPSH deficiency will kill the new seal too. Effective reliability work traces seal failures back to their root cause, which is exactly what FMEA and a root-cause-capturing CMMS are built to do.
What is cavitation and how do you detect it early?
Cavitation occurs when local suction pressure drops below the fluid's vapor pressure, forming vapor bubbles that collapse violently near the impeller — generating shockwaves that pit the impeller, cause intense vibration, and erode efficiency. Its hallmark is a gravel-like or crackling noise at the suction, unstable discharge pressure, and broadband high-frequency vibration energy (commonly in the 1–10 kHz range) distinct from the 1x running-speed peak of mechanical imbalance. The root cause is almost always insufficient NPSH — clogged strainers, excessive suction lift, or hot fluid raising vapor pressure. Maintaining an adequate NPSH margin (around 10% above required) and running near the best efficiency point are the primary preventives.
How does misalignment affect pump reliability?
Misalignment between the pump and driver shaft is one of the leading root causes of premature bearing and seal failure. Even 2–3 mils of offset misalignment can reduce bearing L10 life by 50% or more through increased radial loading, and the resulting shaft movement and vibration transfer directly into the mechanical seal. It typically shows up as elevated 1x and 2x running-speed vibration in the radial direction, plus coupling wear. Precision laser alignment at installation and after any maintenance, along with proper piping support to eliminate pipe strain and a check for soft foot, are among the highest-return reliability practices for centrifugal pumps.
Sign up free to track alignment PMs.
How does OxMaint support pump FMEA and RCM?
OxMaint embeds RCM into execution: failure-mode libraries with root causes live in each pump's asset record linked to work-order templates and condition triggers, criticality scoring drives PM strategy selection, and IoT, SCADA, and vibration data auto-convert threshold breaches into prioritized work orders tied to the predicted mode. Tasks fire at RCM-defined intervals with seals, bearings, and wear parts staged; technicians close them mobile-first with offline mode and QR asset tags; and findings feed a root-cause history that keeps the analysis current — so recurring seal failures finally get traced to source. It overlays SAP PM and IBM Maximo and delivers cloud reliability KPI reporting. A free forever plan is available to trial the full workflow.