Packaging line OEE losses don't come from a single source — they hide across three distinct buckets: stop losses from unplanned downtime, speed losses from running below target rate, and quality losses from rejects and rework. Most packaging teams measure OEE as a single number and miss the diagnostic information that tells them which bucket is shrinking output and which one keeps returning during runs and changeovers. Sign Up Free to segment your packaging line's OEE losses by stop, speed, and quality and build a targeted recovery plan. OxMaint connects OEE loss data to maintenance work orders, inspection triggers, and asset health records — turning loss segmentation from a weekly report into a real-time action system. Book a Demo to see how OEE loss segmentation maps across your specific packaging line configuration and shift structure.
OEE Analytics · Packaging Lines · 2026
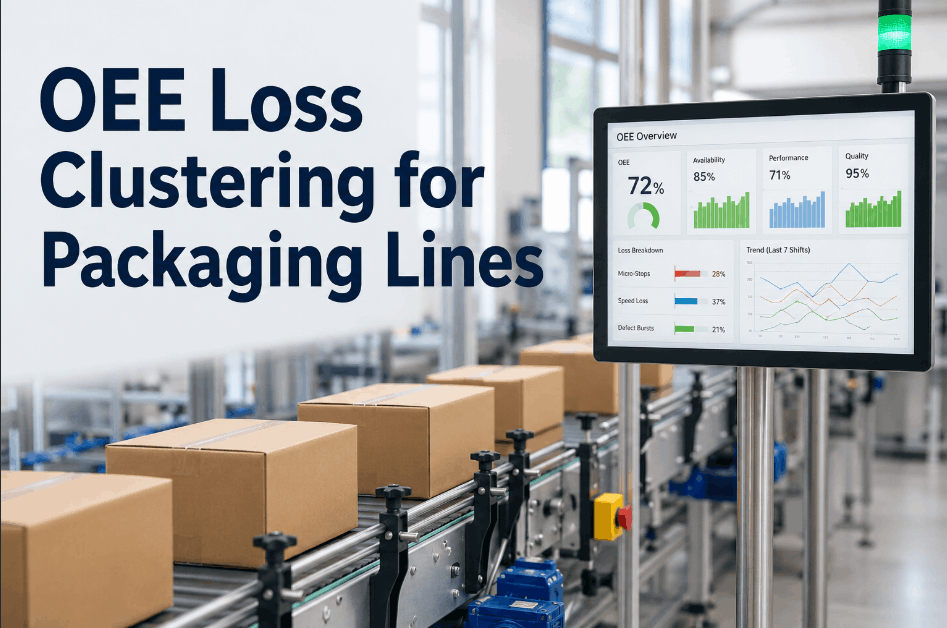
OEE Loss Segmentation for Packaging Lines
Break OEE into stop, speed, and quality losses — so packaging teams can see which bucket shrinks output and which one keeps returning during runs and changeovers.
72%Of packaging OEE loss comes from stop and speed buckets, not quality
−29%Micro-stop frequency in lines with real-time stop loss segmentation
18%Average throughput recovery after targeted speed loss intervention
94%Loss attribution accuracy with OxMaint OEE loss tree analytics
The Three OEE Loss Buckets — What Each One Tells You
OEE loss segmentation means more than splitting a percentage into three columns. Each bucket has a distinct root cause profile, a different maintenance intervention, and a different production recovery path. Understanding which bucket is dominating on any given line tells the maintenance team exactly what to fix — not just that something is wrong. Sign Up Free to configure OEE loss tree analytics for your packaging line in OxMaint.
Stop Losses
Availability Bucket
Unplanned Downtime
Equipment failures, breakdowns, and emergency stops. The most visible loss type — machines that aren't running can't produce. Root cause: reactive maintenance, deferred PM, and component wear.
Planned Downtime Overrun
Changeovers and maintenance windows that run longer than planned. Often invisible in OEE reporting because they are classified as planned — but time over plan is production lost.
Micro Stops
Repeated sub-5-minute stoppages that don't trigger a downtime record. Individually minor, collectively significant — micro stops on packaging lines can account for 8–15% of total stop loss.
Speed Losses
Performance Bucket
Target Gap
Line running below its nameplate or engineered speed. Often attributed to operator caution, material variation, or equipment wear that hasn't triggered a stoppage yet. The hidden throughput drain.
Changeover Drag
Time lost between format changes, material switches, and line reconfiguration. Changeover drag appears in the performance bucket when the line is running slowly during setup rather than fully stopped.
Speed Degradation
Progressive rate reduction across a run as components wear, lubrication depletes, or material feed becomes inconsistent. Detectable only by comparing actual vs. target speed across run segments.
Quality Losses
Quality Bucket
Yield Drop
Units produced that fail inspection and cannot be reworked. On packaging lines, yield drop is most common at line startup, after changeovers, and when material batch characteristics shift mid-run.
Rework Load
Units that require additional processing before they meet specification. Rework consumes downstream capacity and distorts throughput reporting if not tracked as a quality loss separately.
Process Instability
Quality losses that occur during normal run conditions rather than startup or changeover — indicating a process parameter drift that requires inspection and corrective maintenance action.
OEE Loss Segmentation — Without vs. With OxMaint
The gap between a packaging team reading a weekly OEE number and one with real-time loss segmentation per bucket is the difference between knowing something is wrong and knowing exactly where to send the maintenance crew. The comparison below shows what changes when OEE loss data is connected to a CMMS. Book a Demo to see how OxMaint's OEE loss segmentation integrates with your existing line data sources.
OEE Segmentation Maturity — Where Does Your Packaging Line Score?
OEE loss segmentation capability ranges from no structured measurement to real-time loss tree analytics integrated with preventive maintenance and inspection workflows. The maturity framework below lets packaging managers identify the specific measurement gap that is leaving throughput recovery on the table. Book a Demo to assess your line's current OEE segmentation capability with an OxMaint solutions engineer.
Packaging Line OEE Segmentation Maturity
Score 5 = real-time loss tree with CMMS integration · Score 1 = OEE not measured
5
Real-Time Loss Tree · CMMS-Integrated · Auto-Trigger
Stop, speed, and quality losses measured per run segment, attributed per asset, and linked to maintenance work orders automatically. Loss tree updated in real time per shift.
Profile: Every OEE event generates a maintenance action. Throughput recovery is systematic rather than reactive. Loss patterns visible before they compound across shifts.
4
Loss Bucket Tracking · Daily Reporting Active
Stop, speed, and quality buckets measured and reported daily. CMMS linkage partial — some loss events trigger work orders, others require manual escalation.
Action: Complete CMMS integration and add micro stop detection. Full loss tree automation is a configuration task in OxMaint — no additional hardware.
3
OEE Reported · Buckets Not Segmented
OEE calculated and reported as a single number. Stop, speed, and quality losses not separated. Root cause analysis done manually after the fact.
Gap: Single OEE number hides which bucket is dominating. Loss segmentation is the missing step — without it, corrective effort is distributed rather than targeted.
2
Downtime Logged · OEE Not Calculated
Unplanned downtime recorded manually. Speed and quality losses undocumented. OEE not calculated — throughput performance measured only by units out vs. plan.
Risk: Speed and quality losses invisible. Target gap and yield drop are compounding without attribution — throughput below potential with no recovery path defined.
1
No OEE Measurement
Production output tracked against plan but no availability, performance, or quality rate measured. Loss attribution informal and undocumented.
Risk: All three loss buckets accumulating without visibility. OEE baseline unknown — improvement effort has no starting point and no measurement of impact.
Stop Managing OEE as a Single Number.
OxMaint segments stop, speed, and quality losses per shift, per asset, and per run phase — giving packaging teams the loss tree clarity to target recovery where it actually matters.
How OxMaint Builds the Loss Tree — From Line Event to Work Order
OxMaint connects packaging line event data to OEE loss segmentation and maintenance work orders in a single workflow — so every stop, every speed deviation, and every quality loss generates both a measurement and an action. Predictive maintenance algorithms analyze loss patterns across runs to surface assets with degrading OEE contribution before they generate a shutdown event. Sign Up Free to connect your packaging line's loss data to OxMaint's loss tree engine. Book a Demo to see how OEE segmentation integrates with your existing downtime logging and production reporting systems.
Stop Loss Engine
Event → Work Order
Every stop event logged and attributed
Unplanned downtime, changeover overrun, and micro stops all captured with duration, asset, and run context. Recurring stop patterns trigger preventive maintenance review automatically.
Speed Loss Monitor
Target Gap → Inspection
Actual vs. target rate compared in real time
Speed degradation detected against engineered rate per run segment. When degradation exceeds the configured threshold, an asset inspection work order is created in the CMMS automatically.
Quality Loss Tracker
Reject → Root Cause
Quality events attributed by run phase
Yield drop and rework events tagged by run phase — startup, mid-run, or changeover. Process instability patterns trigger corrective work orders linked to the relevant asset in the CMMS.
OEE Loss Tree
Shift Dashboard
Stop, speed, quality buckets per shift
Live loss tree updated per shift — each bucket shows contributing events, affected assets, and open work orders. Maintenance team and production team share a single view of OEE loss and recovery status.
"
We had a packaging line running at 71% OEE and everyone assumed it was a downtime problem. OxMaint's loss segmentation showed us it was 60% speed loss — our filler was running 12% below target rate across every shift. We ran one targeted inspection and found a worn feed screw. After replacement, OEE went to 84% in two weeks. We'd been looking at the wrong bucket for six months.
Packaging Operations Manager — FMCG, 5 packaging lines, Auckland, New Zealand
Frequently Asked Questions
What are the three OEE loss buckets for packaging lines?
Stop losses (availability): unplanned downtime, changeover overrun, and micro stops. Speed losses (performance): target gap, changeover drag, and speed degradation across a run. Quality losses: yield drop, rework load, and process instability events.
What are micro stops and why do they matter in packaging?
Micro stops are repeated sub-5-minute stoppages that don't trigger a formal downtime record. On packaging lines they typically account for 8–15% of total stop loss — significant enough to affect shift output but invisible without sub-minute event logging.
How does OxMaint connect OEE losses to maintenance work orders?
OxMaint attributes each loss event to a specific asset and loss type. When a stop, speed deviation, or quality loss meets the configured threshold, the system automatically creates a work order in the CMMS and assigns it to the relevant maintenance team.
Can OEE loss segmentation be tracked across multiple packaging lines?
Yes — OxMaint tracks stop, speed, and quality losses independently per line and aggregates them into a multi-line OEE dashboard. Loss bucket dominance can be compared across lines to prioritize maintenance investment.
How quickly can OEE loss segmentation be configured in OxMaint?
Most packaging teams configure loss bucket definitions, target speed baselines, and automatic work order triggers within a single day. No hardware changes are required — OxMaint works with existing line data and downtime logging systems.
Turn Every OEE Loss Into a Targeted Maintenance Action.
OxMaint segments stop, speed, and quality losses per shift and links every event to the right work order — giving packaging teams the clarity to recover throughput systematically.