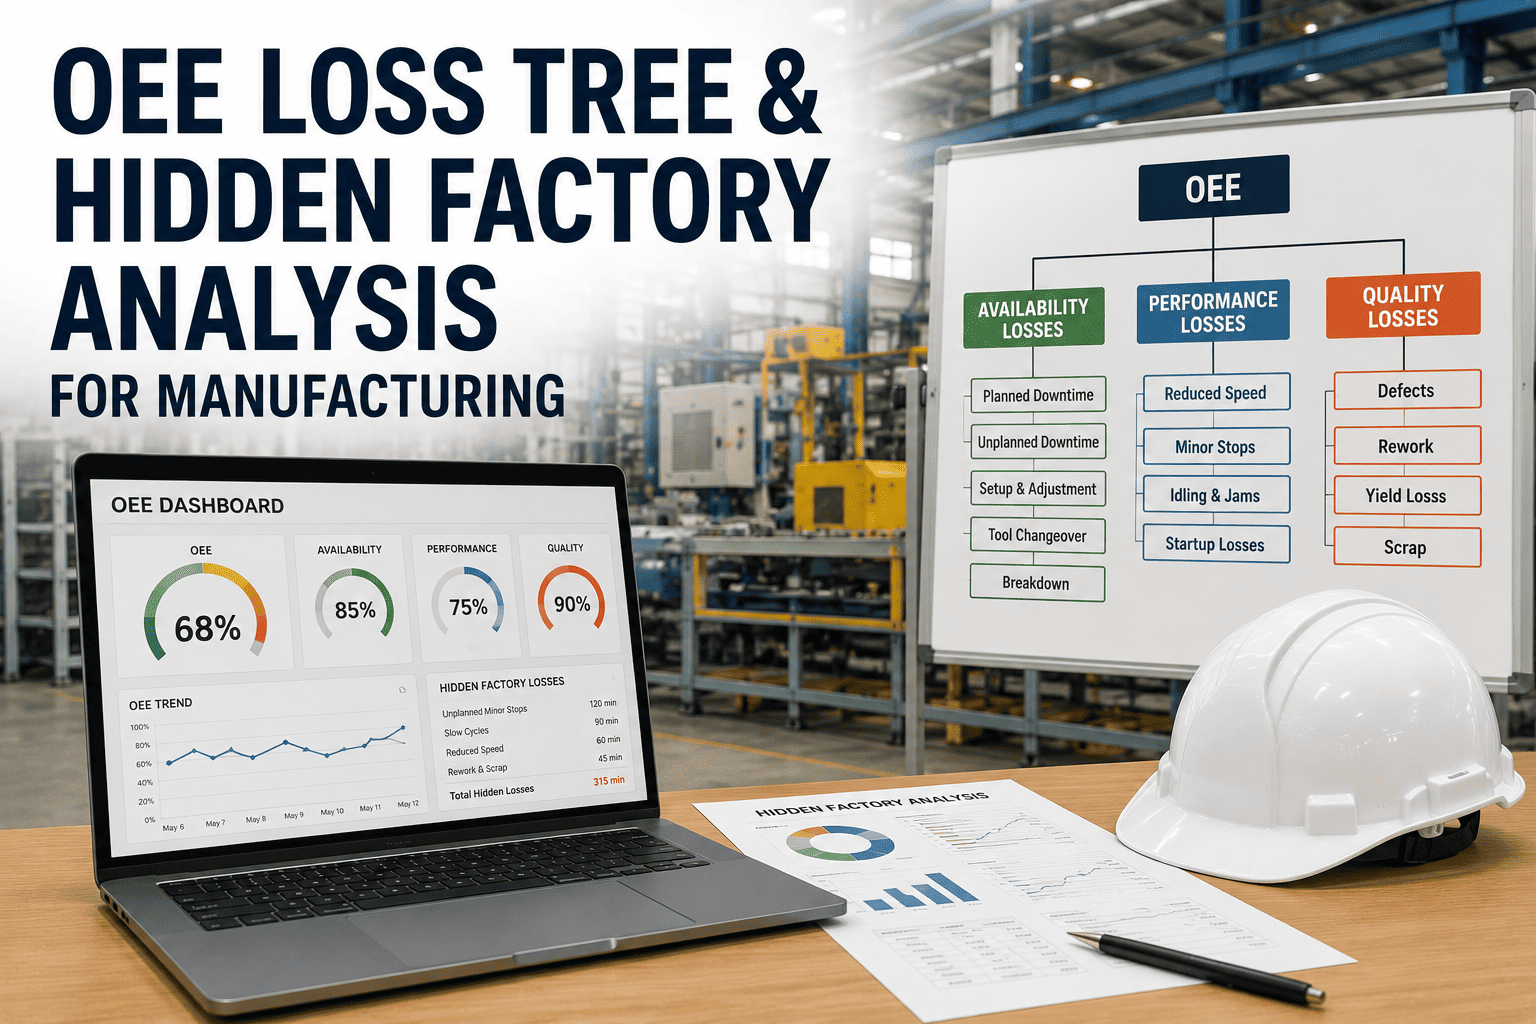
Most manufacturers lose 20–40% of installed capacity to invisible waste — micro-stops under two minutes, speed losses of 3–8%, and quality write-offs that never reach a downtime report. An OEE loss tree makes that hidden factory visible by structuring every loss against Availability, Performance and Quality, then attributing each one to a cause, asset and shift. Built correctly, it turns a vague "we should be running better" into a ranked list of the top three losses worth fixing first. Start Free Trial to build your first tree inside Oxmaint and recover meaningful capacity without capex.
OEE Loss Tree & Hidden Factory
What if 30% of your plant's capacity is hiding in plain sight?
The hidden factory rarely shows up on a downtime log. It lives in 90-second micro-stops, 5% slow-cycling, and scrap that never gets tagged as a loss event. A structured OEE loss tree exposes it — line by line, cause by cause — and ranks exactly where to act first.
Step-by-step build
How to construct an OEE loss tree in five phases
A loss tree is not a dashboard — it is a hierarchical decomposition of every minute, cycle and unit your plant failed to convert to good product. Each phase below narrows the loss from category down to a CMMS-actable work order.
Define the boundary and time window
Pick one line or asset family and a 30–90 day window of timestamped production data. Anything narrower hides shift patterns; anything wider dilutes recent fixes. Lock the scheduled production time as the denominator so every downstream loss is a percentage of the same base.
Capture every stop above and below 5 minutes
Pull planned and unplanned stops from the MES and CMMS, then layer in PLC cycle-state data for stops under 5 minutes. The sub-5-minute bucket is where most hidden factories live — individual events are tiny, but thousands of them compound into double-digit availability loss.
Isolate speed loss from cycle-count loss
Compare actual run rate to the validated ideal cycle time for each SKU. Split the gap into two buckets: slow-cycling (equipment running below setpoint) and minor stops below the PLC's stop threshold (under 3–5 seconds). Most plants find 4–9% of capacity here that no downtime report ever flagged.
Attribute scrap and rework to the loss event
Tie every rejected unit to the shift, asset and preceding loss event when possible. A scrap spike that follows a 6-minute jam is a symptom of that jam, not an independent quality issue — mis-attribution sends engineers chasing the wrong root cause.
Rank losses by recovered-OTIF value, not raw minutes
Convert each loss bucket into the units it cost you, then multiply by contribution margin per unit. A 2% speed loss on a high-margin SKU is often worth more than an 8% availability loss on a break-even one. Fix the top three by value and you typically recover 60–70% of the hidden factory without capex.
Where losses hide
The four loss categories behind the hidden factory
TPM and ISO 22400 group production losses into families. Below is how each one typically contributes to hidden capacity — use these ranges as a sanity check against your own tree before you start fixing anything.
Breakdowns, jams and changeovers above 5 minutes — the part most plants already track, but rarely attribute to a root cause.
Sub-5-minute events invisible to CMMS — sensor faults, brief clearances, operator assists. Often the single largest hidden bucket.
Equipment running 3–8% below setpoint. Rarely alarmed, rarely investigated, compounding across every shift.
Scrap and rework written off as cost-of-doing-business instead of traced to the upstream loss event that caused it.
The math
OEE loss tree formula and worked example
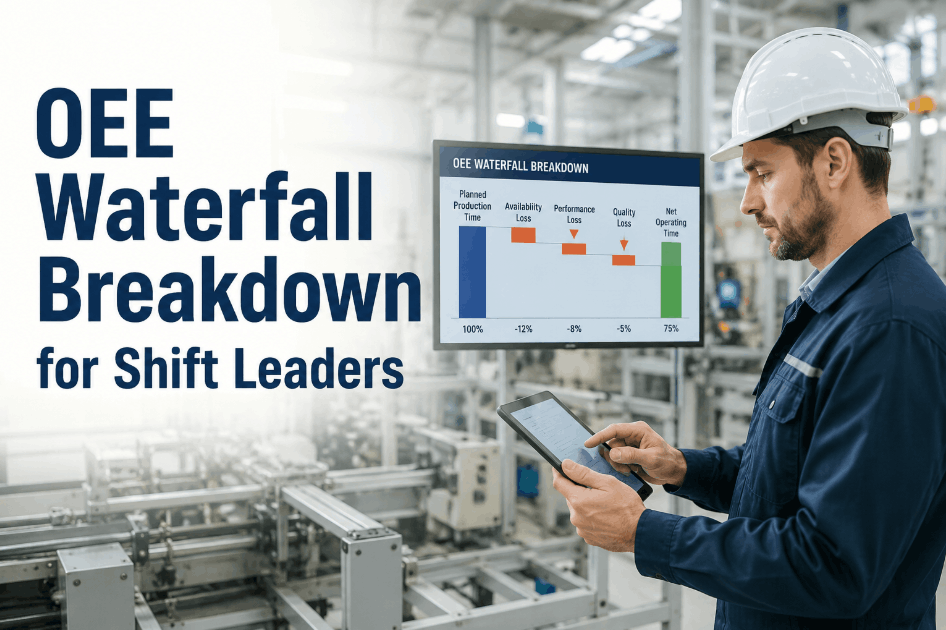
The loss tree is built bottom-up: every leaf loss rolls into one of three OEE multipliers. When you quantify each leaf, the gap between your current OEE and 100% stops being a mystery and becomes a ranked to-do list.
A world-class line runs 85% OEE; this line sits at 74.6% — a 10.4-point gap worth roughly 14% of nominal capacity. Drilling the loss tree shows the top three contributors are a recurring 90-second film-spool splice (4.1% of A), a filler running 4% below rated speed (3.2% of P), and a labeler scrap cluster at shift change (2.7% of Q). Fixing just those three recovers about 9 points of OEE with zero capex.
Cost of inaction
What the hidden factory costs a typical plant
The numbers below come from a 180-asset packaging plant spending $42,000 per year on reactive maintenance and overtime to hit the same output a tighter loss tree would deliver on straight time.
| Loss bucket | Annual minutes lost | Units foregone | Contribution margin / unit | Annual value lost |
|---|---|---|---|---|
| Unplanned downtime (>5 min) | 34,600 | 120,000 | $1.85 | $222,000 |
| Micro-stops (<5 min) | 41,200 | 148,000 | $1.85 | $273,800 |
| Speed loss (4% below setpoint) | 28,800 | 102,800 | $1.85 | $190,180 |
| Quality scrap & rework | — | 62,400 | $1.85 | $115,440 |
| Total hidden factory | 104,600 | 433,200 | — | $801,420 |
On $14.2M annual revenue, that is 5.6% of top-line being absorbed as invisible waste. The top three losses — micro-stops, speed loss and the largest downtime cause — account for $686,000 of the total. Targeting them first typically pays back a CMMS-and-sensor investment in under four months.
From insight to action
Turning loss-tree findings into CMMS work orders
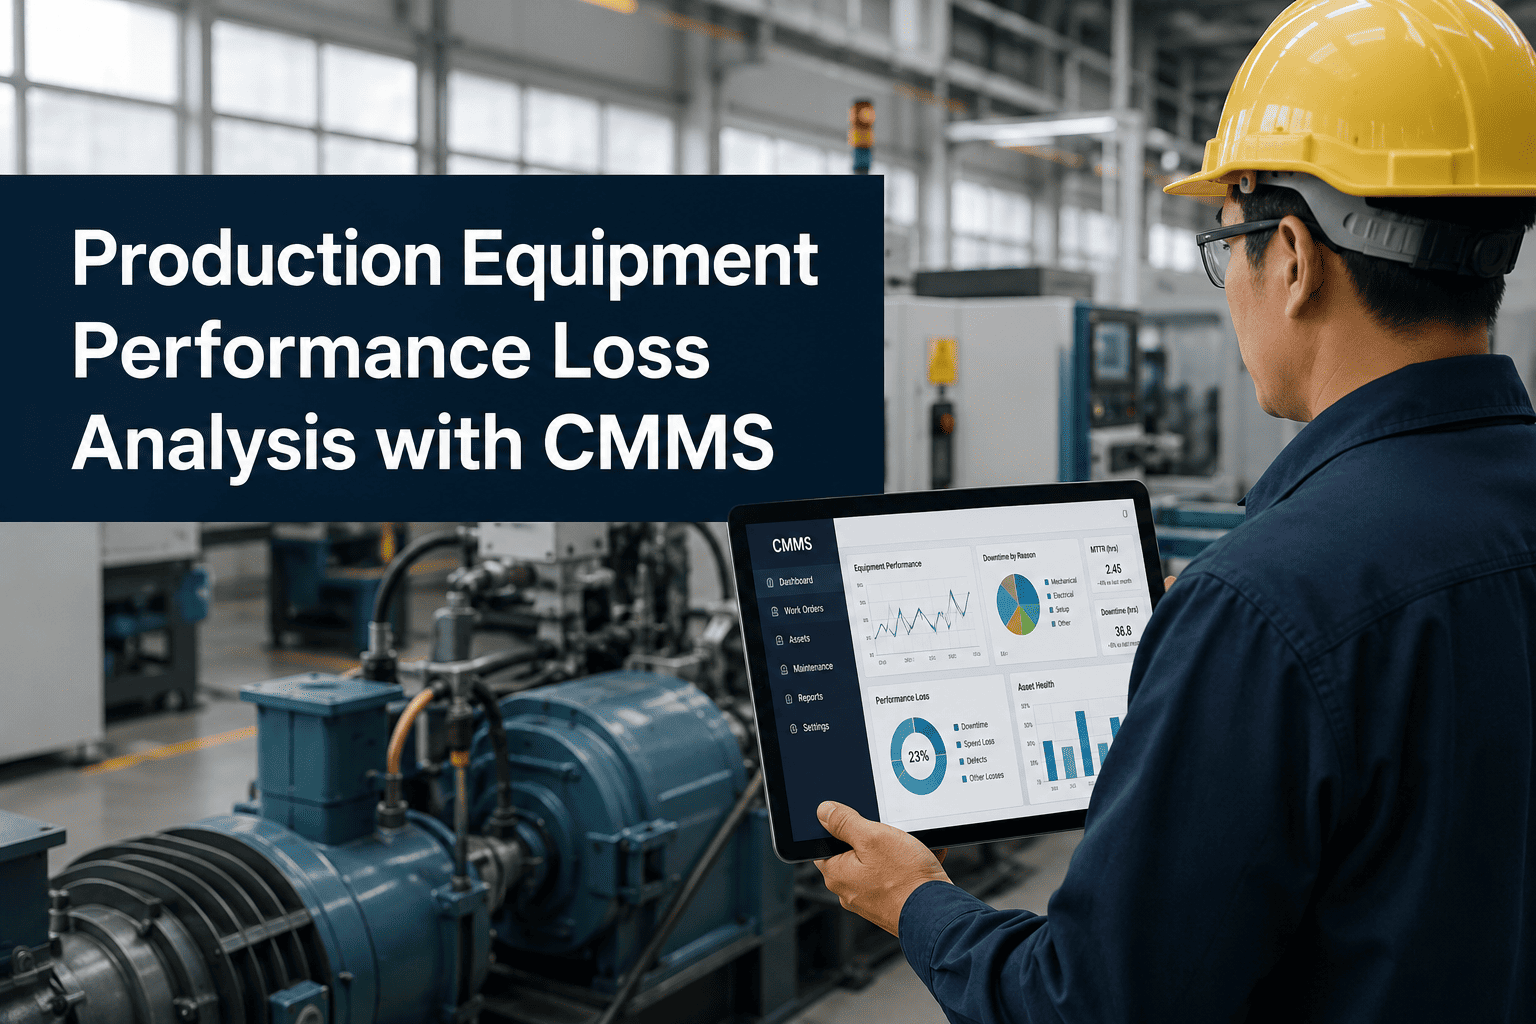
A loss tree only creates value when each top loss is converted into a tagged, tracked work order. Below is the standard mapping from loss category to the CMMS action that closes the loop.
Recurring micro-stop on filler head 3
Open a PM with a 7-day trigger to inspect seal pressure and actuator stroke. Attach PLC trend export as the defect evidence so the technician knows exactly what to look for — not just "check filler."
Capper running 4% below rated speed
Generate a corrective work order linked to the loss-tree speed-loss bucket. Engineering reviews torque setpoint against SKU spec; if setpoint is correct, the issue is mechanical wear and moves to the rebuild schedule.
Labeler scrap cluster at shift change
Tag the preceding handover event as the root cause. Create a checklist-driven standard work for changeover and a quality inspection trigger at the first 15 minutes of every shift to catch the defect before it compounds.
Stop guessing where your capacity went.
Oxmaint turns PLC, MES and CMMS data into a live OEE loss tree — ranked by recovered-margin value and ready to convert into work orders.
FAQ
OEE loss tree & hidden factory — questions we hear most
What exactly is the "hidden factory" in OEE terms?
It is the 20–40% of nominal capacity lost to events that never appear on a downtime report — sub-5-minute micro-stops, minor speed losses, and quality write-offs absorbed as normal. In an OEE loss tree these sit inside the Performance and Quality multipliers, not Availability, which is why traditional downtime tracking misses them entirely.
How is an OEE loss tree different from a standard downtime report?
A downtime report lists stops over a threshold (usually 5–10 minutes) and stops there. A loss tree decomposes all three OEE dimensions — Availability, Performance and Quality — down to leaf-level causes and ranks them by recovered-margin value. You can Start Free Trial and see the difference on your own data within a day.
Do we need new sensors or PLC integration to build one?
Not necessarily. A credible first pass uses existing MES production counts and CMMS downtime logs to capture Availability and Quality. To expose the hidden factory fully — micro-stops and speed loss — you need PLC cycle-state data, which most modern lines already expose through an OPC-UA or MQTT gateway.
How often should we refresh the loss tree?
Monthly is the practical cadence for most plants — long enough to smooth shift-to-shift noise, short enough to verify that recent fixes actually moved the needle. High-mix lines may need a rolling 30-day window per SKU so product changeovers do not distort the averages.
What OEE number should we target first?
World-class is 85%, but chasing the headline number is the wrong move. Target the top three losses by recovered-margin value first — they typically hold 60–70% of the hidden factory and unlock 8–10 OEE points with zero capex. If you want a structured walkthrough, Book a Demo and we will map them on your lines.
Recover the capacity you already paid for.
Build your first OEE loss tree in Oxmaint — see the hidden factory, rank the top three losses, and turn them into work orders in a single afternoon.
Free 14-day trial · No credit card