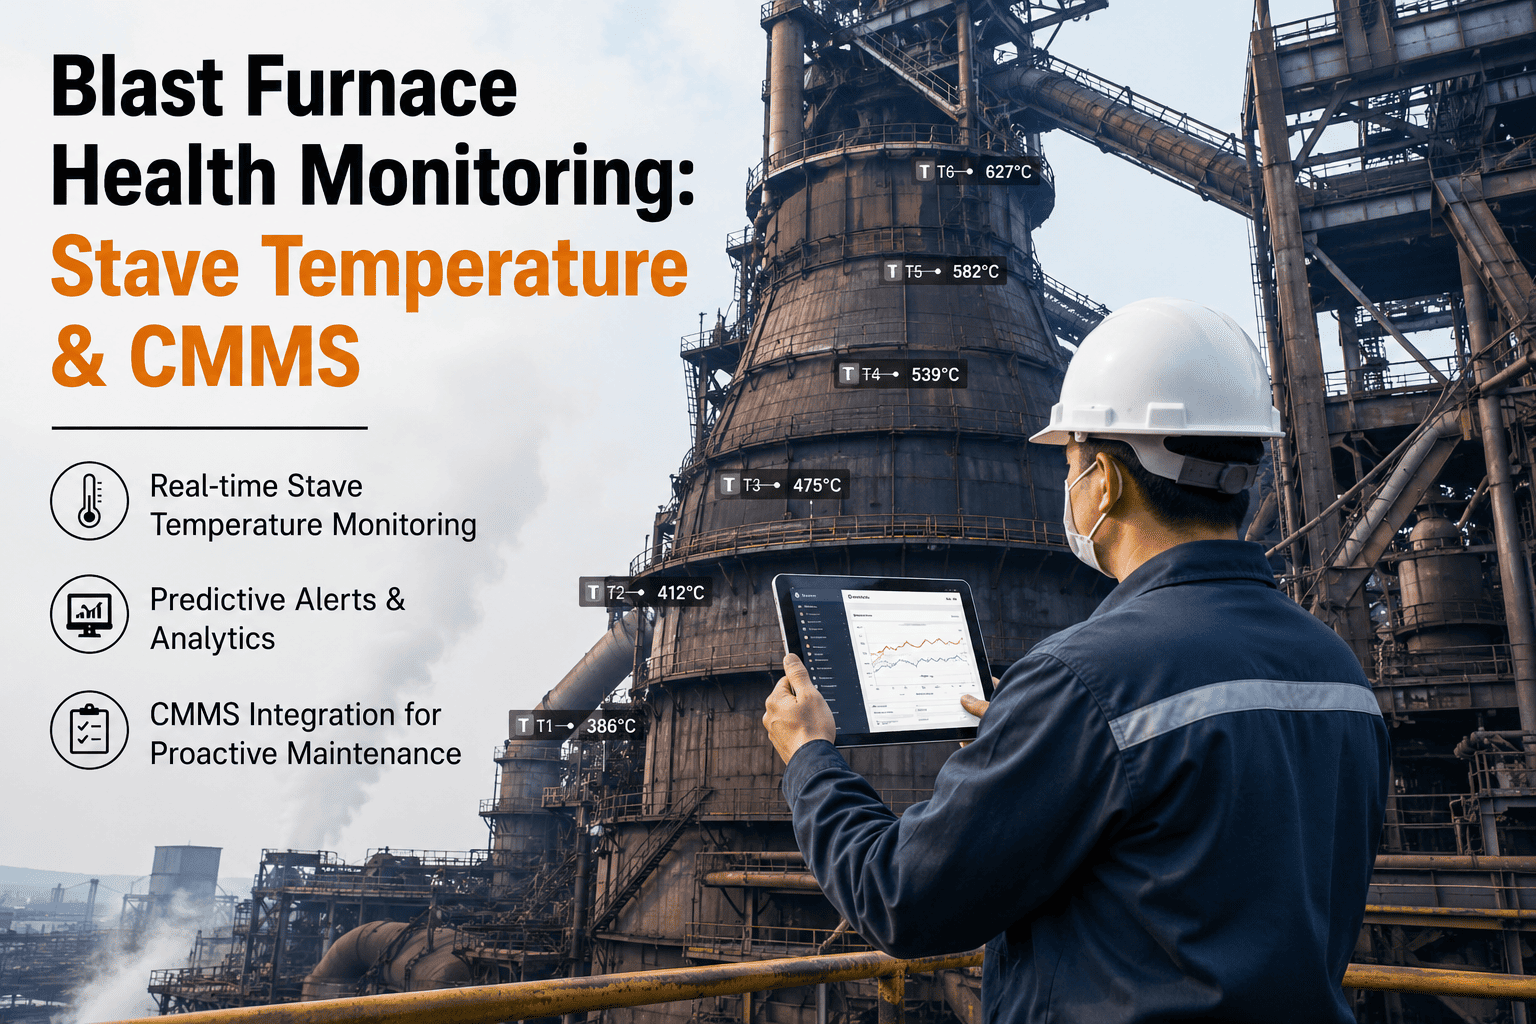
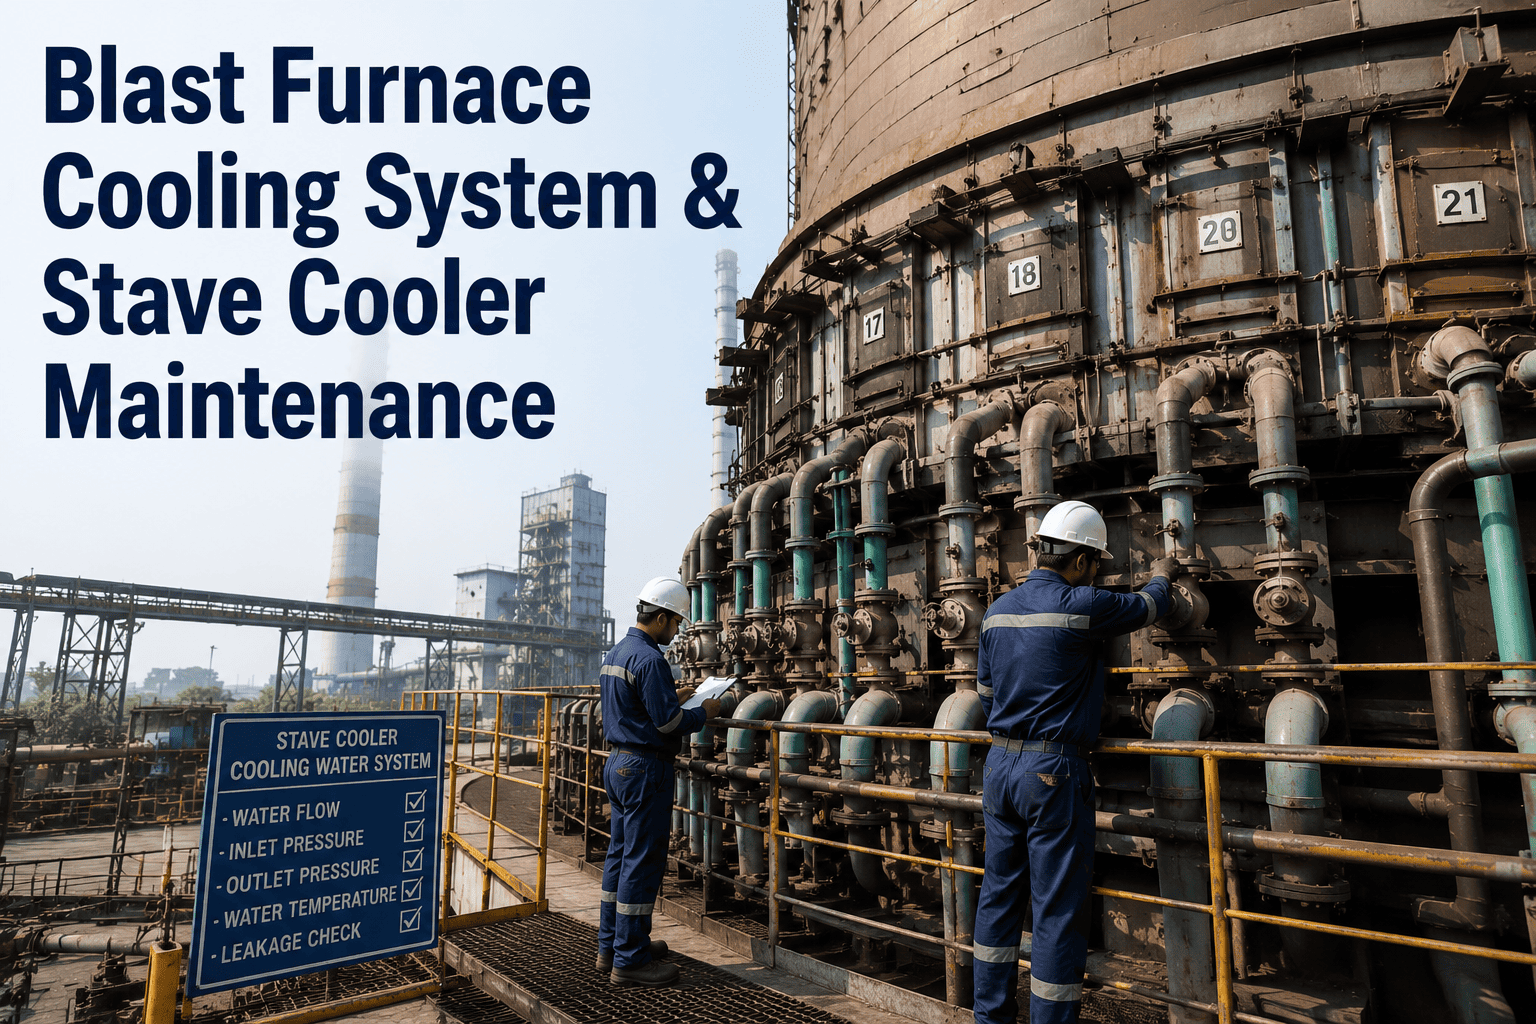
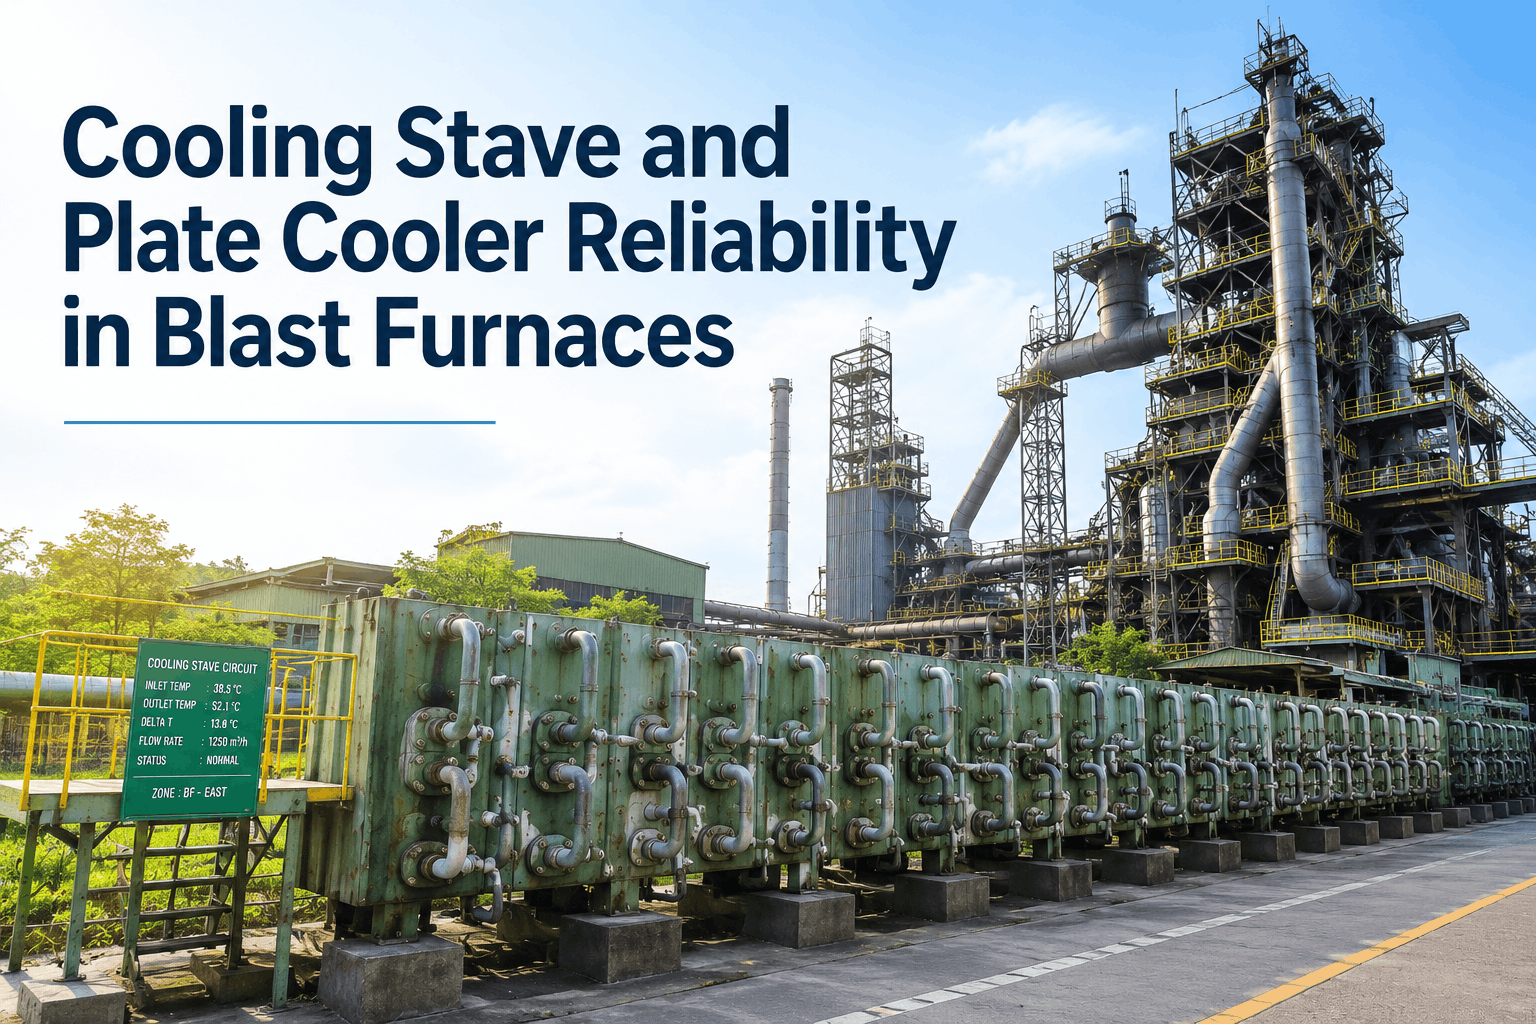
The cooling system is the lifeline of every blast furnace—a network of hundreds of staves, thousands of water channels, and tens of thousands of liters of cooling water flowing continuously to prevent the 2,000°C+ internal temperatures from destroying the furnace shell. When cooling fails, the consequences are catastrophic: water leaks into molten iron create explosive hydrogen and oxygen, shell burnthrough releases hundreds of tons of liquid metal, and unplanned shutdowns cost millions in lost production and repairs. Real-time stave protection isn't optional—it's essential for safe, profitable blast furnace operation.
Modern blast furnaces employ sophisticated cooling system monitoring with 500+ flowmeters, hundreds of thermocouples, and advanced analytics to detect problems before they become emergencies. One major steel plant implemented a leak detection system using over 530 electromagnetic flowmeters to monitor supply-return differentials across every cooling circuit, enabling detection of leaks as small as a few drips per minute. When the coolant is only centimeters away from molten material at temperatures exceeding 2,000°C, this level of monitoring precision is the difference between controlled operation and disaster.
Why Cooling System Monitoring is Critical
Blast furnace cooling systems operate at the extreme edge of engineering—keeping water-filled channels just centimeters away from molten iron at over 1,500°C. The consequences of cooling system failure extend far beyond equipment damage.
Explosion Risk
Water contacting molten iron creates explosive steam expansion and generates hydrogen/oxygen gases. Water leaks into the high-temperature furnace atmosphere (2,000°C+) can cause devastating explosions that threaten personnel safety and destroy equipment.
Shell Burnthrough
Without effective cooling, the furnace shell is exposed to extreme thermal stress. Hearth burnthrough accidents release hundreds of tons of molten iron, causing substantial economic losses, extensive equipment damage, and potential casualties.
Shortened Campaign
Cooling system inefficiency accelerates refractory wear and stave degradation. Premature copper stave failure due to the "banana effect" (bending) or abrasion exposes water channels, forcing early and costly furnace relining.
Stave Types and Cooling Characteristics
Different furnace zones require different stave types based on thermal load, wear mechanism, and operational requirements. Understanding these differences is essential for effective monitoring strategy design.
Copper Staves
Copper's excellent thermal conductivity (390 W/m·K) enables rapid heat dissipation and promotes protective skull formation on the hot face. First introduced in Germany in 1993, copper staves have revolutionized blast furnace cooling.
Cast Iron Staves
Traditional stave material with proven reliability since the mid-1900s. Lower thermal conductivity requires brick lining for insulation but provides excellent wear resistance against burden abrasion.
Steel Staves
Steel staves feature a monolithic construction where the cooling coil melts and becomes one piece with the stave body during casting—eliminating gaps that reduce thermal conductivity.
Copper Plate Coolers
Compact copper coolers (500-1000mm long, 400-800mm wide, ~75mm thick) installed in high heat load zones. Widely used in European large furnaces for targeted cooling in critical areas.
Implement Real-Time Cooling System Monitoring
Protect your blast furnace investment with comprehensive stave monitoring, leak detection, and predictive maintenance analytics.
Cooling System Monitoring Technologies
Comprehensive cooling system monitoring integrates multiple technologies to provide complete visibility into stave condition, cooling efficiency, and early warning of developing problems.
Flow Differential Monitoring
Electromagnetic flowmeters on supply and return lines detect water loss indicating leaks. Advanced systems use 500+ flowmeters to monitor individual cooling circuits, detecting leaks as small as a few drips per minute.
Temperature Differential (ΔT)
Inlet/outlet temperature difference indicates heat transfer rate and cooling efficiency. Rising ΔT may indicate reduced flow, scaling, or increased thermal load from refractory wear.
Heat Flux Calculation
Combines flow rate and temperature differential to calculate heat removal per stave segment. Heat flux trending reveals refractory wear progression and skull formation/dissolution cycles.
Embedded Thermocouples
Thermocouples in refractory lining (449+ per hearth typical) provide temperature distribution for erosion modeling. Data feeds inverse heat conduction models to calculate remaining lining thickness.
Pressure Leak Detection
Monitors cooling circuit pressure to detect leaks that may not show in flow differential. Pressure-based systems can detect tiny leaks providing very early warning of developing failures.
Ultrasonic Thickness Measurement
Non-destructive testing of copper stave residual thickness using specialized fixtures to overcome accessibility challenges. Critical for monitoring wear progression in operating furnaces.
Water Leak Detection Methods
Water leaks into the furnace create immediate safety hazards and accelerate refractory damage. Multiple complementary detection methods ensure comprehensive coverage.
| Detection Method | How It Works | Sensitivity | Response Time |
|---|---|---|---|
| Flow Differential | Supply-return flow comparison per circuit | Drips/minute | Immediate |
| Pressure Monitoring | Circuit pressure drop detection | Very small leaks | Seconds |
| Gas Bubble Detection | Monitors for furnace gas in return water | Medium | Minutes |
| Hydrogen Monitoring | Detects H₂ from water-iron reaction in top gas | Small-medium leaks | Minutes |
| Moisture Condensation | Samples top gas for excess moisture | Medium leaks | Minutes-hours |
| Radiotracer Injection | Tritiated water traced through system | Identifies leak location | Hours |
Stave Wear Failure Modes
Understanding stave failure mechanisms enables targeted monitoring strategies and protective measures to extend cooling system life.
"Banana Effect" Bending
Mechanism: Thermal cycling causes copper staves to bend outward at corners, stressing cooling pipe connections.
Consequence: Pipe joint failure, water leaks, premature stave replacement required.
Detection: Temperature anomalies at stave edges, increased heat flux variability, visual inspection during stops.
Prevention: Anti-bending stave designs, optimized cooling water flow, controlled thermal cycling.
Abrasive Wear
Mechanism: Burden material abrasion when protective skull is lost. Soft copper is particularly vulnerable.
Consequence: Progressive thinning exposes water channels, leading to catastrophic failure.
Detection: Ultrasonic thickness measurement, increasing heat flux, temperature profile changes.
Prevention: Hexagonal insert protection, maintain stable skull formation, optimize burden distribution.
Thermal Overload
Mechanism: Heat load exceeds stave cooling capacity, causing material softening and deformation.
Consequence: Stave deformation, reduced cooling efficiency, accelerated wear progression.
Detection: Elevated outlet temperatures, heat flux exceeding limits, surface temperature monitoring.
Prevention: Adequate cooling water flow (2.4+ m/s), proper zone sizing, operational controls.
Scaling/Fouling
Mechanism: Mineral deposits reduce water channel cross-section and insulate pipe walls.
Consequence: Reduced cooling capacity, localized hot spots, increased pump energy consumption.
Detection: Reduced flow at constant pressure, increasing ΔT, elevated stave temperatures.
Prevention: Water treatment (1400-1600 μS/cm conductivity), periodic descaling, closed-loop systems.
Monitoring System Architecture
An effective blast furnace cooling monitoring system integrates sensors, data acquisition, analytics, and operator interfaces into a unified platform.
Key Performance Parameters
Closed-Loop Cooling System Benefits
Modern blast furnaces use closed-loop cooling systems with chemically treated water to maximize reliability and minimize operational costs.
15-20 Year Operation
Well-designed closed-loop systems enable furnace operation without major cooling system overhauls for 15-20 years, even under intensified operation with pulverized coal injection.
5x Water Reduction
Closed-loop systems reduce water consumption by up to 5 times compared to open systems, minimizing operating costs and environmental impact.
Reduced Scaling
Chemically purified water (1400-1600 μS/cm conductivity) prevents mineral scaling that degrades cooling efficiency and restricts flow.
Multiple Backup Modes
Modern systems provide fallback modes: hot water operation if heat exchangers fail, evaporative cooling during power loss, and standby process water for emergencies.
A major Ukrainian steel producer implemented comprehensive leak detection across two reconstructed blast furnaces, creating the most efficient furnaces in the country.
Application: Cooling lines of blast furnace cooler, tuyere zone, hearth and bottom—measuring supply-return differential per circuit.
Communication: 4-20mA HART to automatic control system with alarm on differential exceeding limits.
Result: Real-time leak detection prevents hydrogen/oxygen generation from coolant contact with molten materials, ensuring process safety.
Protect Your Blast Furnace Cooling System
Implement comprehensive real-time monitoring with leak detection, heat flux analysis, and predictive maintenance to maximize campaign life and ensure safe operation.