Blast furnace cooling system reliability decides how long a campaign lasts and how safely it runs. Staves, tuyeres, cooling plates and shaft panels sit between the burden and the shell, and they only survive because water carries heat away every second. When flow drops, a circuit scales up or a tuyere cooler leaks, the damage moves from a minor alarm to refractory loss, a water leak into the hearth or a forced blast reduction. This guide covers failure modes, detection windows, pump resilience and water quality for steel plant teams. It also shows how Oxmaint steel plant CMMS turns cooling data and inspections into planned work.
Blast Furnace Cooling System Reliability for Steel Plant Reliability
Water flow, temperature, pressure, staves, tuyere coolers and pumps all work as one protective system. Track them together and act on small deviations before a cooling failure shortens your campaign.
Why cooling failures hurt more than most blast furnace faults
A blast furnace cannot simply be switched off and restarted. Hot blast near 1,100 degrees C reaches the tuyeres, and the shell protects the process from heat that would destroy bare refractory. Cooling failures are therefore both a production risk and a safety risk.
Risk matrix for cooling system failure modes
Rank each failure mode by how likely it is to go unnoticed and how severe it is if it develops. The position on the grid drives how often you inspect and how fast you respond.
Detection windows: how early can each method see a leak?
No single signal catches every cooling fault. Faster methods react to large leaks, while slower methods find small ones. Layer them so each covers the gaps of the other.
Stave, plate and shaft cooling: what actually fails
Cooling elements fail from heat load, thermal cycling, scale and mechanical stress. Each mechanism leaves a different signature in the data.
| Failure mechanism | What drives it | Early signal | Maintenance response |
|---|---|---|---|
| Stave deformation | Heat load beyond cooling capacity, thermal cycling | Rising stave temperature, pipe joint stress | Review heat flux, plan inspection, adjust operation |
| Hot face wear | Abrasion and chemical attack from burden and slag | Falling remaining thickness estimate | Schedule gunning or repair in the next window |
| Cooling channel scaling | Poor water quality, low velocity | Higher delta-T at constant flow | Adjust water treatment, flush or clean circuits |
| Pipe joint leakage | Deformation, corrosion, fatigue | Makeup water rise, pressure loss | Isolate circuit, plan repair, check neighbors |
| Complete blockage | Debris or heavy scale | Zero flow with no alarm if not monitored | Immediate action and flow indicator checks |
Neighboring staves share heat load. A leak or blockage on one circuit raises stress on the ones beside it, so inspect the group, not only the alarmed circuit.
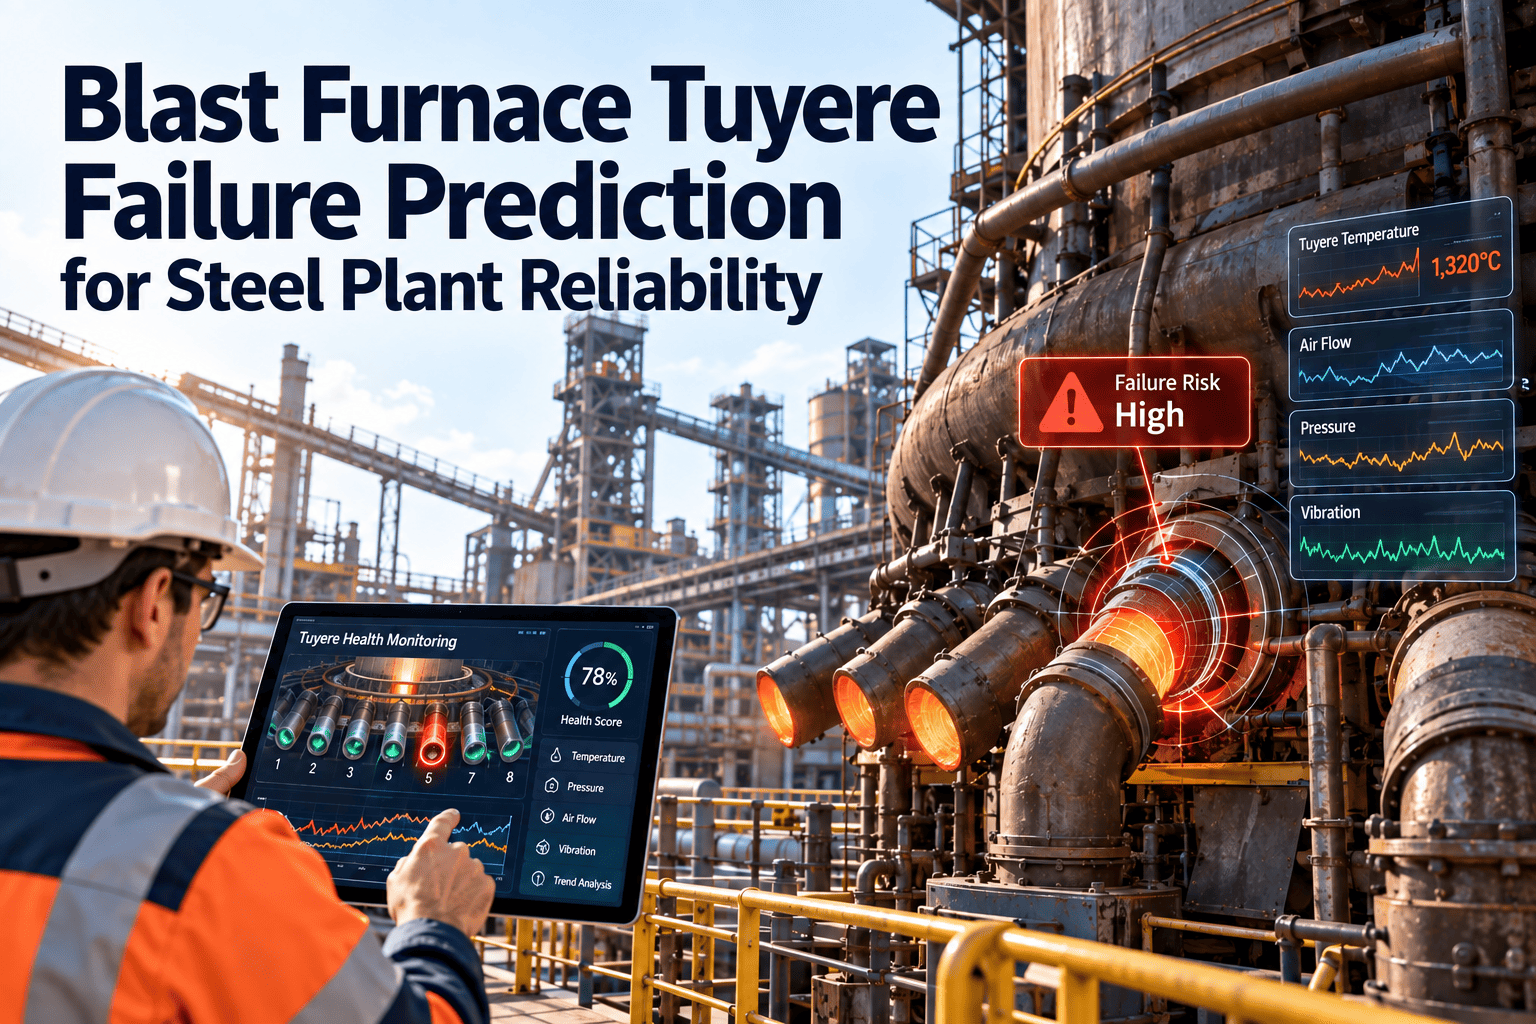
Tuyere cooling: the highest consequence component
Tuyeres face the blast and the raceway at once, so their coolers carry some of the heaviest thermal duty in the furnace. Many designs use separate nose and body circuits so a nose failure can be isolated while the body stays cooled.
Pumps, power and emergency cooling
Cooling reliability depends on the water supply as much as on the furnace. A pump failure with no clean transfer to standby can be as damaging as a leak.
- Test duty-to-standby changeover on a schedule and record the response time.
- Check pump vibration, bearing temperature, seals and motor current as part of condition-based routines.
- Verify emergency supply, such as an elevated water tank or backup pump, and confirm it is full and its valves work.
- Remember that some emergency tanks only help until they empty, and emergency water can carry solids into circuits afterward.
- Review power supply arrangements, including backup power for critical cooling pumps.
Water quality is a maintenance task
Scale, corrosion and biological growth restrict flow and reduce heat transfer, often without any visible change in the equipment. Water treatment belongs in the same maintenance plan as pumps and valves.
What to test
- pH and conductivity
- Hardness, chlorides and suspended solids
- Inhibitor and biocide levels
- Makeup water volume as a leak indicator
What to maintain
- Strainers and filters on each header
- Blowdown and dosing equipment
- Heat exchangers and cooling tower fill
- Sample points and lab records
Use the limits in your water treatment specification. Published pH ranges differ by system design, so do not copy limits from another furnace.
Give your cooling circuits a maintenance record that follows every pump and stave
Plan inspections, log readings and raise corrective work from one steel plant maintenance system.
Time-based, condition-based and predictive cooling maintenance
Most furnaces use a mix. The goal is to move critical items from fixed calendars to decisions based on evidence.
| Approach | Best used for | Weak point | Example task |
|---|---|---|---|
| Time-based PM | Valves, strainers, instruments, lubrication | Ignores actual condition | Quarterly strainer cleaning |
| Condition-based | Pumps, heat exchangers, circuit delta-T | Needs reliable readings | Clean exchanger when approach temperature rises |
| Predictive trend review | Stave heat load, thickness estimates | Needs history and discipline | Plan repair when trend crosses a review level |
| Corrective response | Confirmed leaks and breakdowns | Late by definition | Replace failed tuyere cooler |
Operator and maintenance round checklist
Digital rounds make sure the same points are checked every shift and that findings reach planners.
Every shift
- Main header pressure and temperature
- Flow indicators per tuyere position
- Return temperature by stave zone
- Visible leaks, steam or wet areas
Weekly
- Standby pump start test
- Strainer and filter differential pressure
- Water treatment dosing check
- Infrared scan of shell hot spots
Planned outage
- Calibrate flow and temperature instruments
- Inspect tuyere coolers and blowpipe seals
- Test valves and isolation points
- Update stave condition records
KPIs for cooling system reliability
Choose measures that show both the health of the system and the quality of your response.
How Oxmaint supports blast furnace cooling maintenance
Oxmaint provides the work management layer around your instrumentation and operator knowledge.
- Asset management: model pumps, headers, circuits, staves and tuyere positions with their history.
- Preventive maintenance and scheduling: recurring pump tests, strainer cleaning and instrument calibration.
- Inspections on mobile: digital rounds with readings, photos and pass or fail results.
- Corrective maintenance: findings from rounds create work orders with priority and ownership.
- Inventory: keep tuyere coolers, seals and valves tied to planned jobs.
- Reporting and dashboards: overdue critical tasks, repeat failures and response times.
Cooling reliability FAQs
What is the first sign of a stave cooling problem?
Often a rise in return temperature or refractory readings at constant flow, or unexplained makeup water use. Trends show it before alarms do.
How often should tuyere coolers be inspected?
Every shift visually, with periodic infrared checks. Set your frequency in Oxmaint from your furnace procedure.
Why track makeup water?
A rising makeup volume in a closed circuit can signal a leak long before pressure alarms. It costs nothing extra to trend.
Can a CMMS monitor cooling sensors directly?
Your control system and historian handle live signals. A CMMS records readings and triggers work. A demo shows the workflow.
What should we record after a cooling failure?
Location, detection method, time to response, cause and repair. Link it to the asset so repeat failures become visible.
Protect the campaign by catching cooling faults early
Bring pumps, circuits, staves and tuyeres into one maintenance plan, and keep a clear record of every inspection and repair.