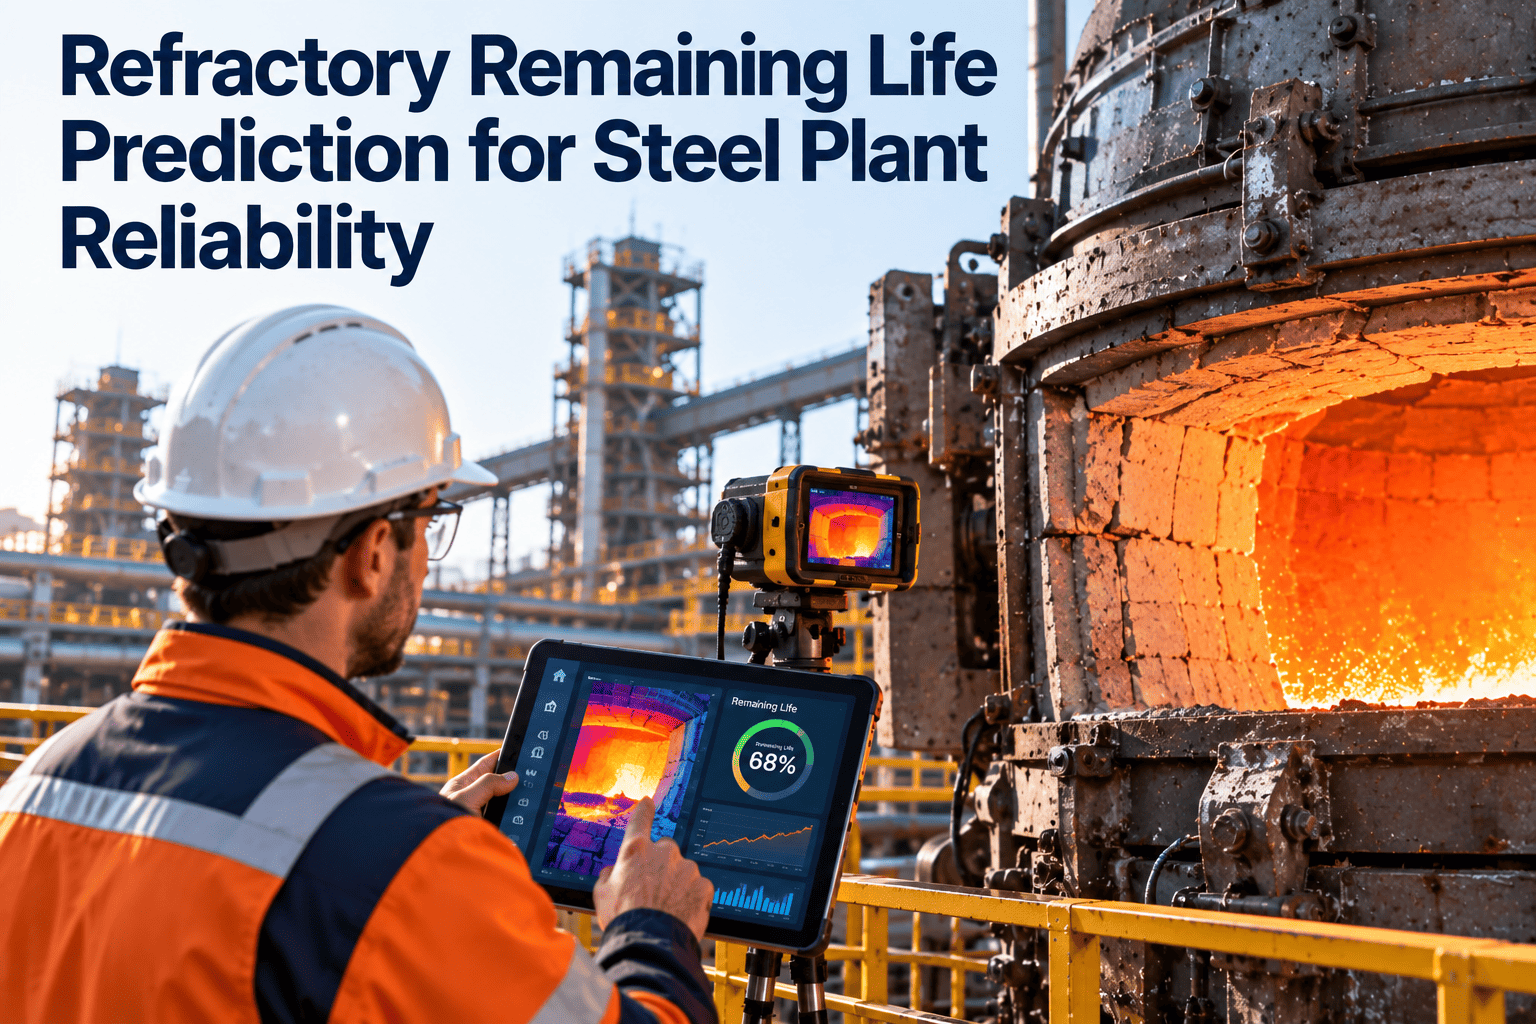
Knowing how a refractory lining is wearing is only half the job — the harder question is knowing how many heats it has left before it crosses a safety threshold, and being confident enough in that number to schedule the reline as planned maintenance instead of reacting to an emergency. Remaining life prediction answers that question by combining three data streams that most plants already collect separately: thermal trend data from shell or zone temperature scans, heat history for the vessel and each of its wear zones, and periodic condition measurements such as thickness or laser profile scans. Put together and extrapolated forward, those three inputs turn a static "how thick is it right now" reading into a forward-looking "how many heats until it needs attention" projection — the difference between knowing a lining's current condition and knowing when that condition will require action. This guide walks through how that prediction actually gets built, what confidence a plant should demand before trusting it, and how a CMMS such as OxMaint turns the projection into a scheduled work order instead of a spreadsheet nobody revisits.
Refractory Remaining Life Prediction Across BOF, EAF, Ladle, and Tundish Linings
Combine thermal trends, heat history, and zone condition data into a remaining-life estimate you can safely plan a reline around.
Two Ways to Get a Refractory Reline Schedule Wrong
A fixed calendar-based reline schedule fails in one of two directions, and both are expensive. Remaining life prediction exists to sit between them.
What Feeds a Remaining Life Estimate
Shell or zone surface temperature readings, taken on a fixed cadence, reveal thinning refractory long before it reaches a critical thickness — a rising temperature trend at one zone means less insulating lining stands between the heat and the shell.
The number of heats processed since the last reline or repair at each zone is the denominator every wear-rate calculation runs against — without an accurate heat count per zone, a thickness trend cannot be converted into heats-remaining.
Direct thickness measurement — by laser scan, ultrasonic gauge, or physical probe — anchors the prediction to a real data point rather than letting it drift on thermal inference alone.
From Wear Curve to Confidence Interval
The simplest version of a prediction is a linear extrapolation: measure the wear rate over the last several inspection intervals, and project forward to the point where remaining thickness reaches the minimum safe limit. A more reliable version adjusts that line for how consistent the wear rate has actually been.
A wide scatter in successive thickness readings should widen the predicted end-of-life range rather than being smoothed away — the prediction is only as trustworthy as the variance it is built on, and presenting a false sense of precision by collapsing that scatter into a single confident date does the planning team no favors when the reline actually comes due.
What a Plant Should Do at Each Confidence Level
| Confidence in Projection | What It Means | Recommended Action |
|---|---|---|
| Low | Fewer than three consistent measurement points on this zone | Continue standard-cadence scanning, do not schedule a reline from this data alone |
| Moderate | Consistent wear rate across several intervals, some scatter | Increase scan frequency as the zone approaches its projected end-of-life window |
| High | Tight, consistent wear rate across many intervals | Schedule the reline inside the predicted safe margin, tied to a planned outage |
Turn Thickness Trends Into a Scheduled Reline Date
OxMaint combines thermal scans, heat counts, and thickness measurements per zone into a trended remaining-life projection, then generates the reline work order automatically ahead of the predicted safe margin.
Remaining Life Prediction Is Not an EAF-Only Concept
| Vessel | Typical Campaign Scale | Fastest-Wearing Zone | Primary Prediction Input |
|---|---|---|---|
| BOF Vessel | Thousands of heats | Trunnion and charge pad | Laser profile scan trend |
| EAF Shell | Hundreds of heats | Slag line / sidewall | Thermal scan plus gunning history |
| Steel Ladle | Dozens to low hundreds of heats per campaign | Slag line | Visual plus periodic gauge measurement |
| Tundish | Single sequence to low double digits of heats | Working lining, weir and dam | Visual inspection per sequence |
Each vessel type needs its own zone map and its own wear-rate baseline — a prediction model calibrated on EAF slag line behavior does not transfer directly to a ladle slag zone, even though the underlying method is identical. The methodology travels across vessel types even when the specific wear rates, campaign lengths, and measurement techniques do not, which is what makes a single CMMS-based prediction framework practical to roll out plant-wide rather than building a separate one-off tool for each vessel.
Converting a Prediction Into a Planned Outage
- Set a minimum safe thickness threshold per zone before relying on any prediction, based on OEM or engineering guidance
- Require at least three consistent measurement points before treating a wear-rate trend as reliable enough to schedule against
- Widen the predicted end-of-life window whenever measurement scatter increases, rather than defaulting to the tightest historical estimate
- Increase scan frequency automatically as a zone enters its predicted final 10–15% of remaining life
- Generate the reline work order with enough lead time for material procurement and outage scheduling, not at the moment the threshold is reached
- Log the actual end-of-life heat count and measured thickness at reline, and feed it back into the model to refine the next campaign's prediction
Where Remaining Life Predictions Go Wrong
A prediction model is only as good as the discipline behind the data feeding it, and several recurring mistakes undermine otherwise sound methodology across steel plants building their first remaining life program.
The most common is treating a single measurement as a trend. One thickness reading tells you where a zone is right now, not how fast it is getting there — a prediction built from a single data point is really just a guess dressed up as a projection, and it should never be the basis for a scheduling decision on its own. A second frequent mistake is averaging wear rate across an entire vessel rather than by zone, which smooths away exactly the localized acceleration that a targeted repair program depends on catching early.
A third pitfall is failing to account for a process change when interpreting a shift in wear rate. If slag chemistry, tap temperature, or charging practice changes mid-campaign, the wear-rate curve calculated from heats before that change no longer describes the heats after it, and a prediction that keeps extrapolating the old rate will either overstate or understate the true remaining life. Any known process change should reset the calibration window for that zone's prediction rather than being folded silently into a longer trend line.
A fourth pitfall, more organizational than technical, is generating a prediction that nobody acts on until the number becomes alarming. A remaining-life projection that sits in a report without a defined lead-time trigger for procurement and outage scheduling delivers none of the planning benefit the prediction was built to provide — the value of the number comes entirely from the action it triggers, not from its accuracy in isolation.
From Isolated Readings to a Living Prediction Model
Most steel plants already have every raw ingredient a remaining life prediction needs — thermal scans logged somewhere, heat counts tracked in the production system, and thickness measurements recorded on inspection sheets. What is usually missing is the connective layer that pulls those three sources into a single per-zone record and recalculates the projection every time a new data point arrives, rather than requiring someone to manually reconstruct the trend at the next planning meeting.
Building that connective layer inside a CMMS rather than a standalone spreadsheet has a specific advantage: the same system that stores the prediction is the system that generates the work order once a lead-time threshold is crossed, so the prediction and the action it triggers never drift apart. It also means the model improves on its own over time — every reline logs its actual end-of-life heat count and measured thickness back into the same record, giving the next campaign's prediction a slightly better calibrated starting point than the one before it.
Frequently Asked Questions
How many measurements are needed before a prediction is trustworthy?
Can thermal data alone predict remaining life without thickness measurement?
Does OxMaint generate the reline work order automatically?
Does this replace the zone-level wear tracking used for EAF campaigns?
How does a plant handle a sudden spike in wear rate?
A Remaining Life Projection Serves More Than One Audience
A remaining life prediction is not just a maintenance planning tool — it is one of the few reliability figures that production planning, procurement, and finance all need at the same time, for different reasons, and reconciling those needs is part of why the projection has to be built with a defined confidence level rather than presented as a single hard date.
Production planning needs the projected reline window early enough to schedule around it without disrupting downstream order commitments — a projection that only firms up days before the threshold is reached gives no room to build that accommodation into the production calendar. Procurement needs enough lead time to secure refractory material and any contracted installation labor, particularly for vessels using specialty brick or castable mixes with longer order lead times than standard gunning material. Finance, particularly at plants tracking cost per ton of steel produced, uses the same projection to time capital or maintenance budget allocation across quarters rather than being surprised by an unplanned reline landing in the wrong budget period.
Presenting one projection with a defined confidence band, rather than three separately calculated numbers for three departments, keeps everyone working from the same underlying data — and it is precisely the kind of cross-functional visibility that a CMMS-based prediction, updated automatically as new measurements arrive, is positioned to provide in a way a maintenance-only spreadsheet never was.
From Fixed Campaigns to Condition-Driven Relines
Steelmaking has run on fixed-interval refractory campaigns for most of its history, largely because reliable in-service measurement technology — laser profiling, embedded thermocouple arrays, ultrasonic thickness gauges — was either unavailable or too expensive to deploy broadly across every vessel in a plant. Fixed campaigns were a reasonable response to that constraint: set a conservative interval based on worst-case wear assumptions, and accept the waste of relining before some zones were truly due as the cost of avoiding an unplanned failure.
That constraint has loosened considerably. Thermal imaging equipment, laser scanning tools, and the CMMS platforms needed to store and trend the resulting data are now well within reach of mid-size steel plants, not just the largest integrated producers. The barrier to condition-driven refractory management today is less about instrumentation cost and more about the discipline of consistent measurement and logging — which is exactly the gap that a structured remaining life prediction workflow, built into daily maintenance routines rather than treated as a separate analytics project, is designed to close.
Know the Reline Date Before the Lining Forces It On You
OxMaint turns thermal trends, heat history, and zone condition data into a remaining-life projection you can schedule an outage around — across BOF, EAF, ladle, and tundish linings alike.