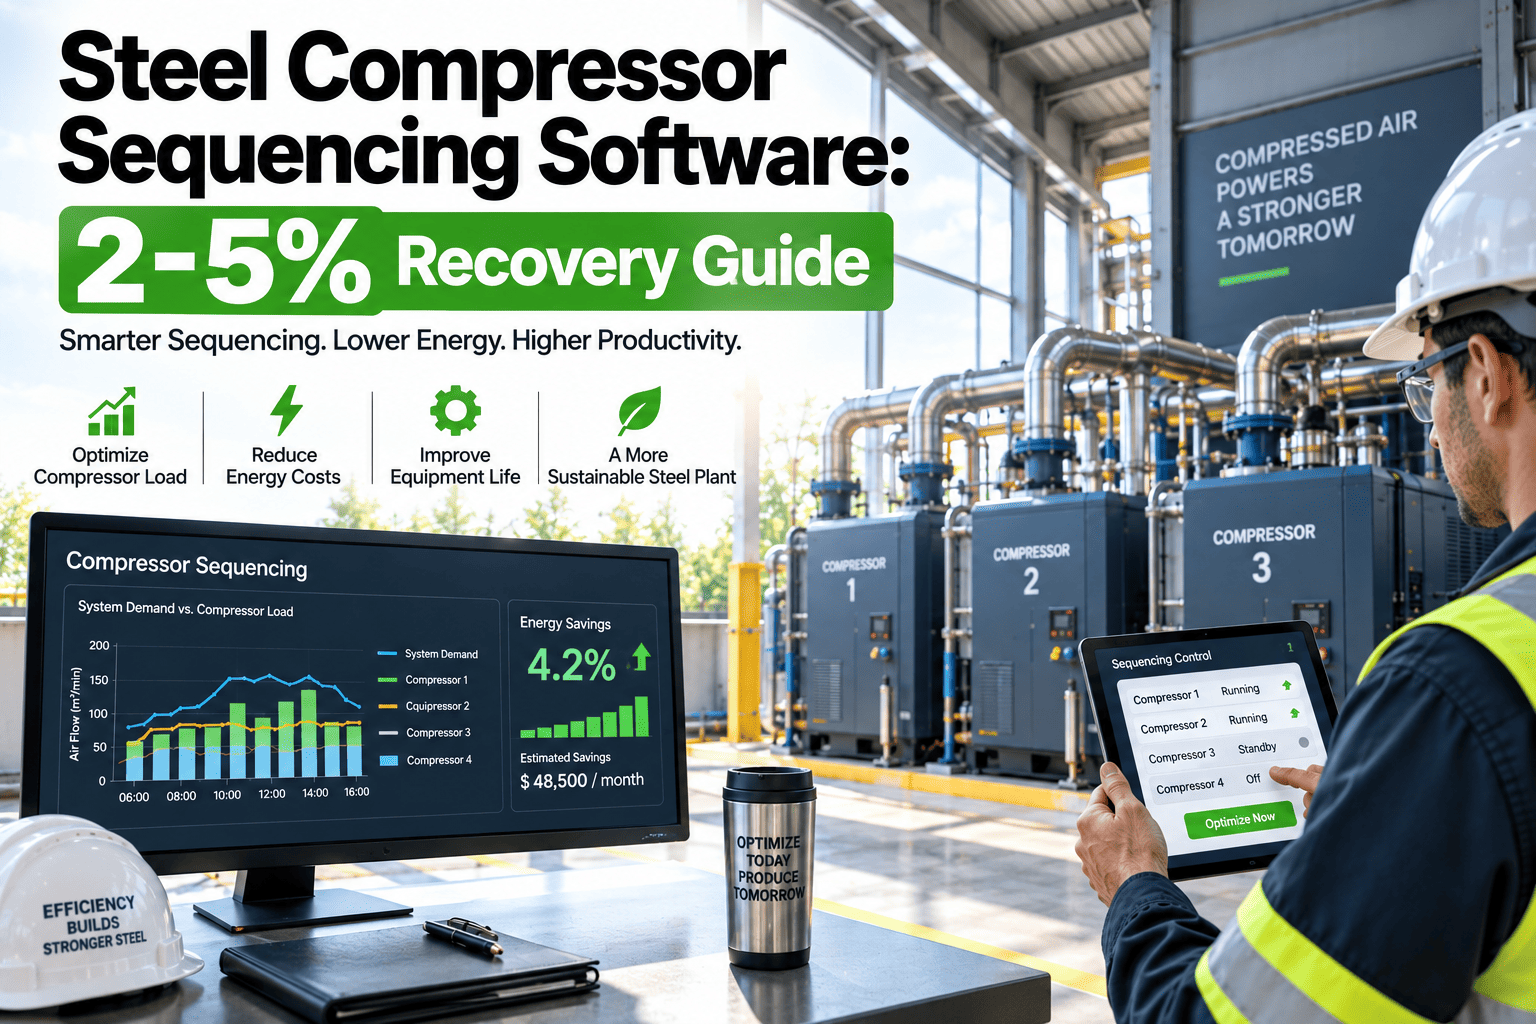
A blast furnace air separation unit, a caster spray system, and a pickle line rinse header all pull from the same compressed air header, and none of them care which compressor happens to be running when they do. Most steel plants solve this with local pressure switches bolted to each machine, which keep the plant running but leave two to five percent of total electrical spend sitting on the table in the form of compressors fighting each other, unloaded units spinning at partial power, and trim capacity that never gets called in cleanly. Sequencing is the discipline of coordinating load, unload, and standby state across every machine on the header so the plant runs the fewest compressors necessary at the tightest pressure band the process allows.
Why Sequencing Is Its Own Discipline, Separate From Leak Repair
Leak repair and pressure reduction get most of the attention in compressed air programs because the savings are easy to visualize — a hissing fitting is an obvious target. Sequencing is quieter. It does not show up as a hiss or a hot spot; it shows up as a specific power trend that creeps upward even after every leak has been tagged and fixed. Two identical plants can run the same leak-free header at the same average pressure and still differ by several percent in electricity per standard cubic foot delivered, purely because one plant's compressors take turns loading and unloading in a coordinated pattern while the other plant's compressors are guessing independently, based on whatever their local pressure switch reads at that instant.
The Three States Every Compressor Moves Through
The failure mode that costs plants the most is not any single state — it is time spent in the unloaded state. A compressor that unloads and reloads repeatedly because a local pressure switch is set too close to a neighboring unit's switch point burns power without moving air, and it does so continuously, shift after shift, invisibly.
Root Causes of Poor Sequencing on a Steel Plant Header
Sequencing Strategies Compared
| Strategy | How It Coordinates | Best Fit | Common Failure Point |
|---|---|---|---|
| Cascading pressure bands | Each compressor assigned a distinct, non-overlapping load/unload pressure window | 2-4 fixed-speed compressors on one header | Bands drift together over time and start overlapping |
| Network master controller | One controller reads header pressure and commands every compressor's state directly | 4+ compressors, mixed types, multiple pressure zones | Controller logic not updated when a compressor is added or retired |
| Base-and-trim with VFD | Fixed-speed units hold steady base load; one VFD unit absorbs swings | Plants with a highly variable minute-to-minute demand profile | Trim unit undersized for the actual swing range, so base units still cycle |
| Local pressure switches only | Each compressor reacts independently to its own local reading | Single-compressor systems or true emergency backup only | Guaranteed hunting and overlap once a second compressor is added |
What a Correctly Sequenced Header Looks Like
On a well-sequenced header, base-load compressors run fully loaded for hours at a time without cycling, one trim unit tracks the swing, and every other machine sits in true standby with its motor stopped. Total electricity per thousand cubic feet delivered stays flat across shifts because the same logic governs every hour of the day rather than whatever the last operator happened to set. Getting there requires two things most plants lack: a documented sequencing scheme tied to actual demand data, and a way to notice immediately when a compressor's actual runtime pattern drifts from that scheme. Start a free trial to put both in place, or book a demo to walk through your current header configuration.
Unsequenced vs. Sequenced Header
Estimating What Sequencing Waste Is Actually Costing You
Most plants can estimate their sequencing waste with numbers they already have, without a new instrumentation project. The starting point is specific power: kilowatts drawn per hundred cubic feet of air delivered, calculated per compressor from existing amp readings and flow estimates. A compressor's specific power should stay flat, within a narrow band, across every hour it spends fully loaded. If a machine's specific power reading climbs during periods when its runtime log shows repeated load-unload cycling rather than steady loaded operation, that gap between the two numbers is a reasonable proxy for how much of its draw is being wasted on cycling rather than delivering usable air.
A Note on Sequencing Across Multiple Pressure Zones
Integrated steel plants rarely run a single compressed air header. Blast furnace instrument air, EAF fume system air, and general shop air frequently sit on separate zones with different pressure requirements, and sequencing decisions in one zone can shift load onto a shared set of compressors feeding another. Treating each zone's sequencing scheme in isolation misses these interactions. A compressor sequenced as "trim" for the shop air zone but also feeding instrument air during a header tie-in event needs its state logic to account for both roles, or the trim assignment for one zone quietly becomes an unplanned base-load assignment for the other.
How Oxmaint Supports Compressor Sequencing
Sequencing and the Maintenance Calendar
Sequencing performance and preventive maintenance are more connected than most plants treat them. An intake filter that has gone past its service interval raises the pressure drop a compressor has to work against, which changes the amp draw at a given output and quietly shifts the specific power baseline that sequencing logic assumes is stable. A worn unloading valve does something similar from the opposite direction, allowing a compressor to leak air internally while nominally in standby, so a machine the sequencing scheme believes is drawing zero power is actually consuming a small but continuous amount. Because of this link, PM records and sequencing performance data are more useful reviewed together than separately. A specific power trend that starts climbing gradually across several weeks, with no corresponding change in sequencing setpoints, is often the first visible sign of a mechanical issue that a monthly inspection round would not catch until it had progressed considerably further. Treating the two data sets as one review, rather than maintenance in one spreadsheet and sequencing performance in another, shortens the time between a mechanical issue starting and someone noticing it.
Getting Started Without a Full Header Overhaul
Plants hesitant to take on a full sequencing redesign project can start narrower and still capture meaningful savings. Logging current load, unload, and standby states for two to four weeks, without changing any setpoints yet, produces a baseline that often reveals the worst offenders on its own — a specific compressor cycling every few minutes, or a standby machine that has quietly been left running for months. Addressing those obvious cases first, before attempting a plant-wide sequencing redesign, tends to capture a meaningful share of the available 2-5% recovery with the least operational risk, and it builds the runtime history needed to design a more complete sequencing scheme with confidence rather than guesswork.