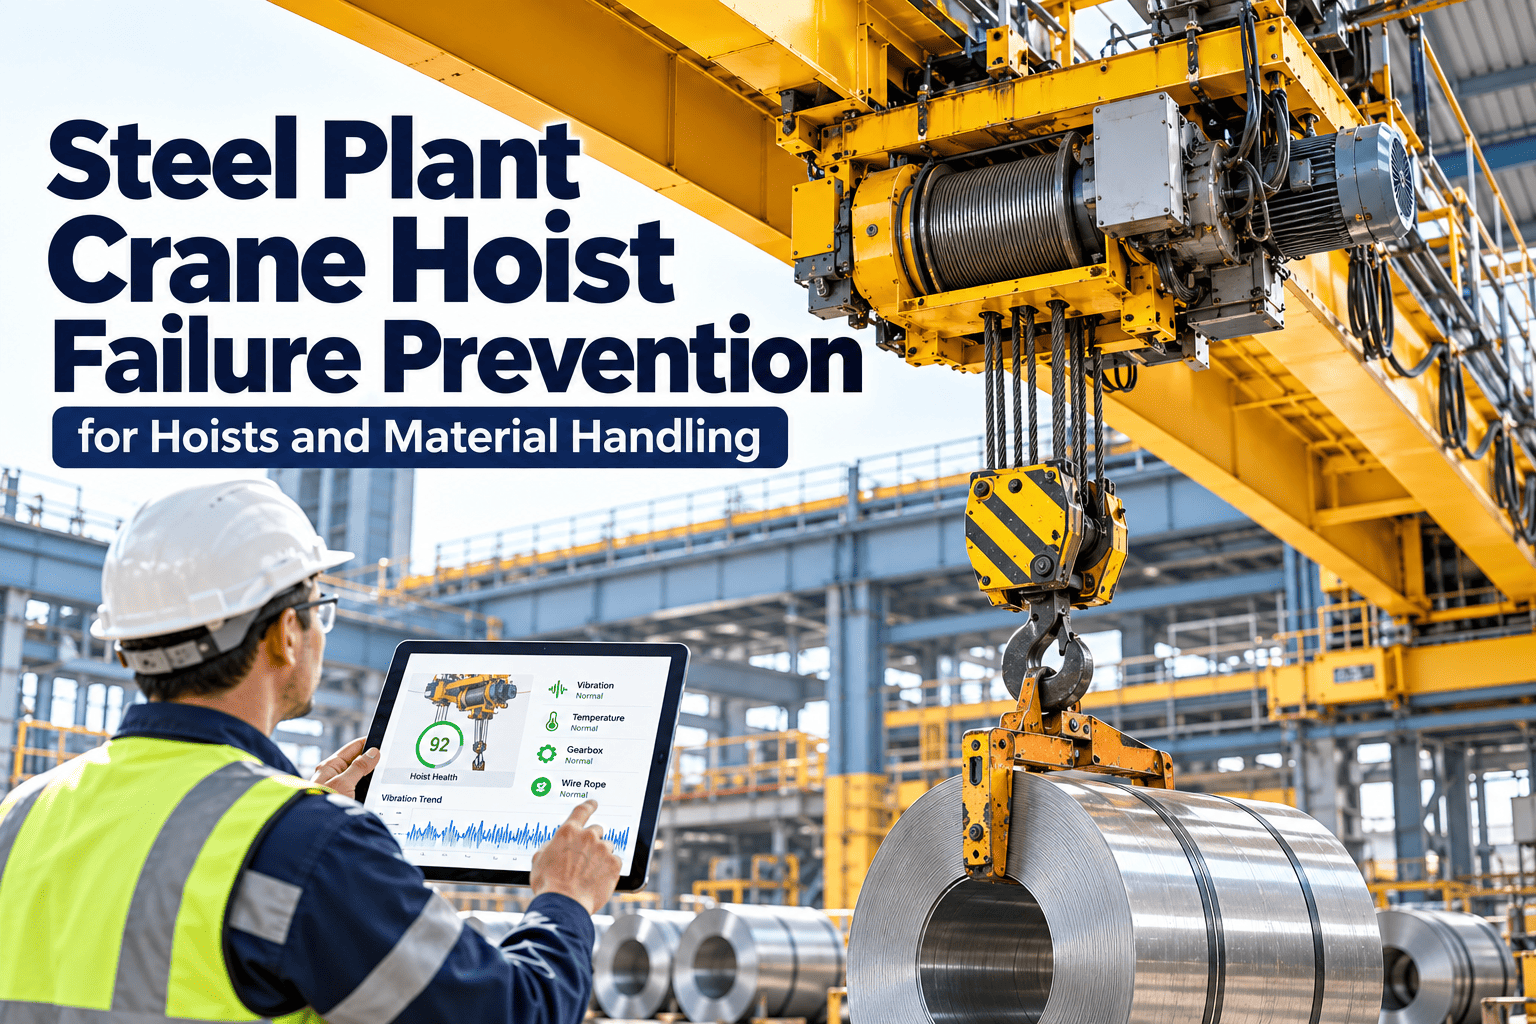
In a steel plant, overhead cranes carry ladles of molten metal, slabs, coils, scrap and rolls over people and production lines. A hoist failure is rarely a minor repair. It can mean a dropped load, a stopped caster or a serious injury. Most hoist failures give warning through wire rope wear, brake slip, heat, noise or missed inspection findings, but only if someone records and acts on them. This guide covers the main failure modes, inspection routines and condition tracking, and how Oxmaint maintenance management software keeps crane records complete.
Heat, duty cycle and consequence raise the stakes
A crane in a warehouse and a crane over a melt shop may share a design family, but their duty is not comparable. Steel plant cranes face conditions that wear every part of the load path faster.
Operating conditions
- Radiant heat near furnaces, ladle bays and casters
- Scale, dust and splash that contaminate rope lubricant and brakes
- Near-continuous duty in charging, teeming and casting cycles
- Shock loads from scrap handling and magnet or grab operation
Consequence of failure
- Risk to people working under or beside the load path
- Molten metal exposure when a ladle crane fails
- Stopped production when a bay loses its only crane
- Damage to the load, the crane and the building structure
Common hoist failure modes and the warning signs
Use the table as the basis for inspection checklists and failure codes. Each mode has early signs that a trained inspector or a condition sensor can catch.
| Component | Failure mode | Early warning signs | Typical response |
|---|---|---|---|
| Wire rope | Fatigue, abrasion, corrosion, kinking, birdcaging, core damage | Broken wires, reduced diameter, flattened or corroded sections, poor lubrication | Measure and record, remove from service when rejection criteria are met |
| Hook | Throat opening increase, cracks, twist, latch damage | Opening wider than the allowed percentage, visible cracks, bent latch | Measure against a baseline, replace when limits are exceeded |
| Hoist brake | Lining wear, glazing, contamination, gap out of range | Load drift, slow stopping, heat marks, oil or dust on lining | Test holding, adjust or replace linings, check for contamination |
| Gearbox | Gear tooth wear, bearing damage, oil degradation | Rising noise or vibration, metal in oil, high case temperature | Oil analysis, vibration check, planned repair |
| Motor and controls | Overheating, insulation breakdown, contactor or drive faults | Rising current or temperature, nuisance trips, burnt contacts | Thermal and electrical checks, planned component replacement |
| Limit switches and overload devices | Out of adjustment, damaged, bypassed | Failure to stop travel, unexplained overtravel, wiring damage | Functional test before use, repair and record any defect |
| Wheels, rails and runway | Flange wear, misalignment, rail damage | Skewing, noise, uneven wear patterns | Measure wear, align, plan rail and wheel work |
| Structure | Cracks, loose fasteners, heat distortion, corrosion | Visible cracks near welds, loose bolts, paint cracking | Structural inspection, repair under approved procedure |
The two tracks that deserve their own program
Rope and brakes sit directly in the load path. Treat them as tracked assets with measurements, not as items on a general checklist.
- Record installation date, rope type, diameter and length for every hoist.
- Log broken wire counts by location at each inspection, not only pass or fail.
- Measure diameter at set points and compare with the baseline.
- Note corrosion, flattening, kinks and lubrication condition.
- Apply the rejection criteria in the applicable standard, such as ASME B30.2, and the manufacturer instructions.
- Keep retired rope records to learn real service life by crane and duty.
- Record lining thickness or gap readings at each inspection.
- Run a holding test under a safe test load and log any drift.
- Note hot running, glazing, oil contamination and unusual noise.
- Track adjustments and replacements against each hoist.
- Escalate any report of slip or delayed stopping immediately.
- Compare brake wear between cranes with similar duty.
Inspection limits and intervals come from OSHA 29 CFR 1910.179, ASME B30.2 and B30.17, the manufacturer and your own risk assessment. Always apply the current text of the standards that govern your crane.
A layered inspection program, from every shift to every year
OSHA 1910.179 separates frequent inspections from periodic ones, and plants usually add their own layers for critical cranes. Build the layers into scheduled tasks so none depend on memory.
Operator checks
Visual look at hook, rope, hoist brake function, limit devices, controls and warning devices before lifting. Defects are reported and tagged out where required.Frequent inspections
Competent person checks operating mechanisms, rope condition, hooks, brakes and reeving. Findings and measurements are recorded.Detailed inspections
Thorough examination of structure, fasteners, gearing, brakes, wheels, rails, electrical gear and safety devices, with dated sign-off.Sensor and trend checks
Current, temperature, vibration and duty counts reviewed for drift, prompting inspection before the next scheduled tier.Special inspections
Triggered by overloads, collisions, repairs, modifications or long outages, with a documented return-to-service decision.Measure hooks instead of judging them by eye
A hook that looks fine can still be stretched beyond its limit. Recording measurements makes gradual deformation visible over time.
What to record
- Throat opening measured against the baseline taken when the hook was new
- Twist relative to the plane of the hook
- Visible cracks, nicks, gouges and wear at the saddle
- Latch condition and spring action where a latch is fitted
- Hook serial number and capacity marking legibility
Why it prevents failures
- Gradual opening shows overloading or heat exposure before the hook gives way
- Baselines make decisions consistent between inspectors and shifts
- Serial-linked records show when a hook was replaced and why
- Trends across cranes reveal where abuse or overload is occurring
Extra care where molten metal is in the load
Cranes handling hot metal need stricter practices than general-purpose cranes. Many plants add redundancy, tighter intervals and specific design features to the standard program.
- Hoist redundancy: confirm that braking and drive systems meet the design requirements for hot metal service and test them as specified.
- Heat protection: inspect shielding, cable insulation and lubricant condition where radiant heat is present.
- Rope condition: inspect more often and keep detailed measurement records, because heat accelerates lubricant loss and wire wear.
- Controls and limits: test overload, upper limit and emergency stop functions at defined intervals.
- Return to service: require documented sign-off after any repair affecting the hoist before the crane lifts hot metal again.
Your crane manufacturer, insurer, safety authority and corporate engineering standards may set stricter requirements than the general references used here. Follow the most demanding applicable requirement.
Many failures start with how the crane is used
Good maintenance cannot fully offset rough operation. Feedback from records can help operators and supervisors see the cost of poor habits.
| Practice | Damage it causes | Preventive measure |
|---|---|---|
| Side pulling and angled lifts | Rope wear on drum and sheaves, hook and structural stress | Operator training, supervision and tracking of rope wear patterns |
| Shock loading and snatch lifts | Gearbox, brake and rope fatigue | Smooth controls, drive tuning and load monitoring |
| Hitting limit switches routinely | Switch damage and loss of safety function | Coach operators and record limit device defects at once |
| Skipping pre-use checks | Defects found late or after an incident | Digital pre-use checklists with required sign-off |
| Overloading or unknown load weight | Structural fatigue, brake and rope damage | Load indication, clear weight information and overload protection |
| Delayed defect reporting | Small faults grow into failures | Simple reporting by mobile device with fast acknowledgement |
Plan spares around the failures that would stop a bay
When a bay depends on one crane, the wait for a part can be longer than the repair. Spare strategy should follow criticality and lead time.
- Brake linings, discs and adjustment parts for critical hoists
- Pre-fitted wire rope sets for ladle and charging cranes where practical
- Limit switches, contactors and control cards
- Hook blocks or hooks matched to critical hoists
- Gearbox rebuild or exchange arrangements with defined lead times
- Motor rewind and replacement agreements
- Wheel and rail components with long manufacturing times
- Emergency support contacts for specialist crane service
Inspection program weaknesses to look for in your plant
- Inspection forms that record pass or fail without measurements.
- Findings noted on paper but never converted into work orders.
- No link between a defect and the exact component, so history cannot be trended.
- Rope and brake replacements not recorded, hiding real service life.
- Inspection tasks missed during busy outages and not rescheduled.
- Crane records spread across spreadsheets, folders and individual notebooks.
Fixing these gaps does not require new cranes or sensors. It requires a consistent inspection workflow and a place where every record lives.
Put Every Crane Inspection on a Schedule You Can Prove
Digital checklists, timestamped sign-offs and automatic work orders for findings keep crane safety records complete and easy to produce.
Not every crane carries the same risk
Rank cranes by consequence and duty, then match inspection depth and spares to the ranking.
| Crane class | Typical duty | Consequence of failure | Suggested program depth |
|---|---|---|---|
| Ladle and teeming cranes | Molten metal, continuous cycles | Highest: safety and production | Strictest intervals, redundant checks, condition monitoring, critical spares on site |
| Charging and scrap cranes | Heavy shock loads, magnets or grabs | High: safety and furnace supply | Frequent inspections, rope and brake tracking, electrical monitoring |
| Slab, coil and roll handling cranes | Repetitive heavy lifts | High: production and load damage | Scheduled detailed inspections, brake and hook measurements |
| Maintenance and bay cranes | Intermittent lifts of spares and tools | Medium: delays and moderate risk | Standard inspection program with duty hour tracking |
| Light-duty hoists and monorails | Occasional use | Lower, but not zero | Routine inspection schedule and recorded findings |
Adding data to the inspector's eyes
Inspection finds visible condition at set times. Monitoring adds a continuous view of what the machine is doing between visits.
Monitoring supports inspection. It does not replace statutory inspections or qualified judgment, and its alerts should create inspection tasks, not skip them.
What happens when an inspection finds a defect
Record the finding
Component, location, measurement and a photo are captured on a mobile checklist at the crane.Decide on use
A competent person decides whether the crane stays in service, is restricted or is tagged out.Raise the work order
A corrective work order is created against the exact component with priority and due date.Plan parts and window
Rope, brake parts or hooks are reserved and the repair is fitted into an available window.Repair and test
Work is completed, functional tests are run and results are recorded.Return to service
An authorized person signs off, and the history is updated for future trend review.What Oxmaint adds to a crane maintenance program
| Crane maintenance need | Oxmaint capability |
|---|---|
| Model each crane with hoist, trolley, bridge and brake components | Asset register with parent and child hierarchy |
| Run shift, frequent and periodic inspections on time | Scheduled inspections and preventive maintenance with reminders |
| Capture measurements, photos and signatures in the field | Mobile checklists and work orders |
| Act on defects with clear ownership | Corrective work orders with priority and assignment |
| Keep critical rope, brake and hook spares ready | Inventory with reorder levels linked to assets |
| Show auditors dated, signed records | Compliance records and reports by crane and inspection type |
| Spot cranes with repeating problems | Dashboards on backlog, overdue inspections and repeat failures |
KPIs for crane reliability and inspection discipline
Crane and hoist failure prevention questions
What causes most hoist failures in steel plants?
Rope wear, brake degradation and gearbox or electrical faults are common, made worse by heat, contamination and heavy duty cycles.Which standards apply to overhead crane inspections?
In the US, OSHA 29 CFR 1910.179 and ASME B30.2 and B30.17 are the main references. Always confirm requirements for your jurisdiction.Can sensors replace manual inspections?
No. Sensors add early warning between inspections, while required inspections and competent judgment remain essential.How do we prove inspections were done?
Use dated, signed digital checklists linked to each crane. You can book a demo to see crane inspection records.Where should we start?
Register your highest-risk cranes first, then create inspection schedules in Oxmaint and track every finding to closure.Keep Every Lift Under Control
Bring crane inspections, defect tracking, spares and compliance records into one maintenance system built for steel plant duty.