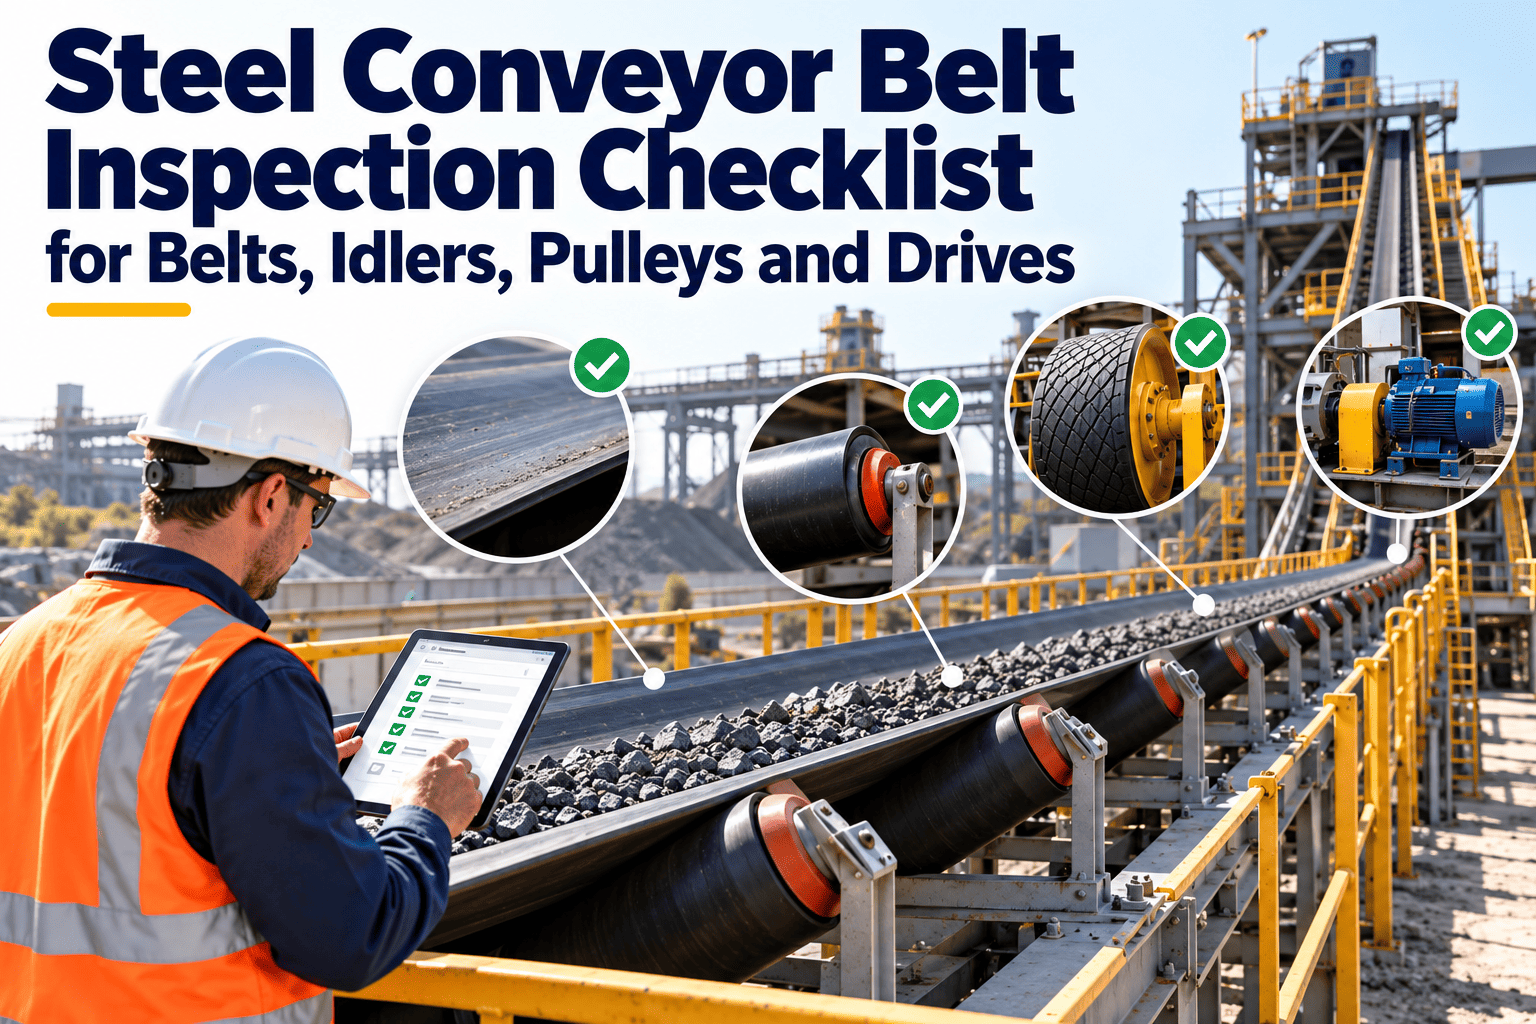
A conveyor pulley rarely fails without warning. The bearing runs a little warmer for weeks, the shaft picks up a trace of misalignment, lagging wears smooth, and a belt starts tracking to one side. In a steel plant, where conveyors move ore, coke, sinter, limestone and scrap-handling fines around the clock, that slow drift ends in a seized pulley and a stopped feed line. This guide explains how to prevent conveyor pulley failure with disciplined inspection, and how a steel plant CMMS keeps every finding tied to a work order.
Conveyor Pulley Failure Prevention for Steel Plant Material Handling
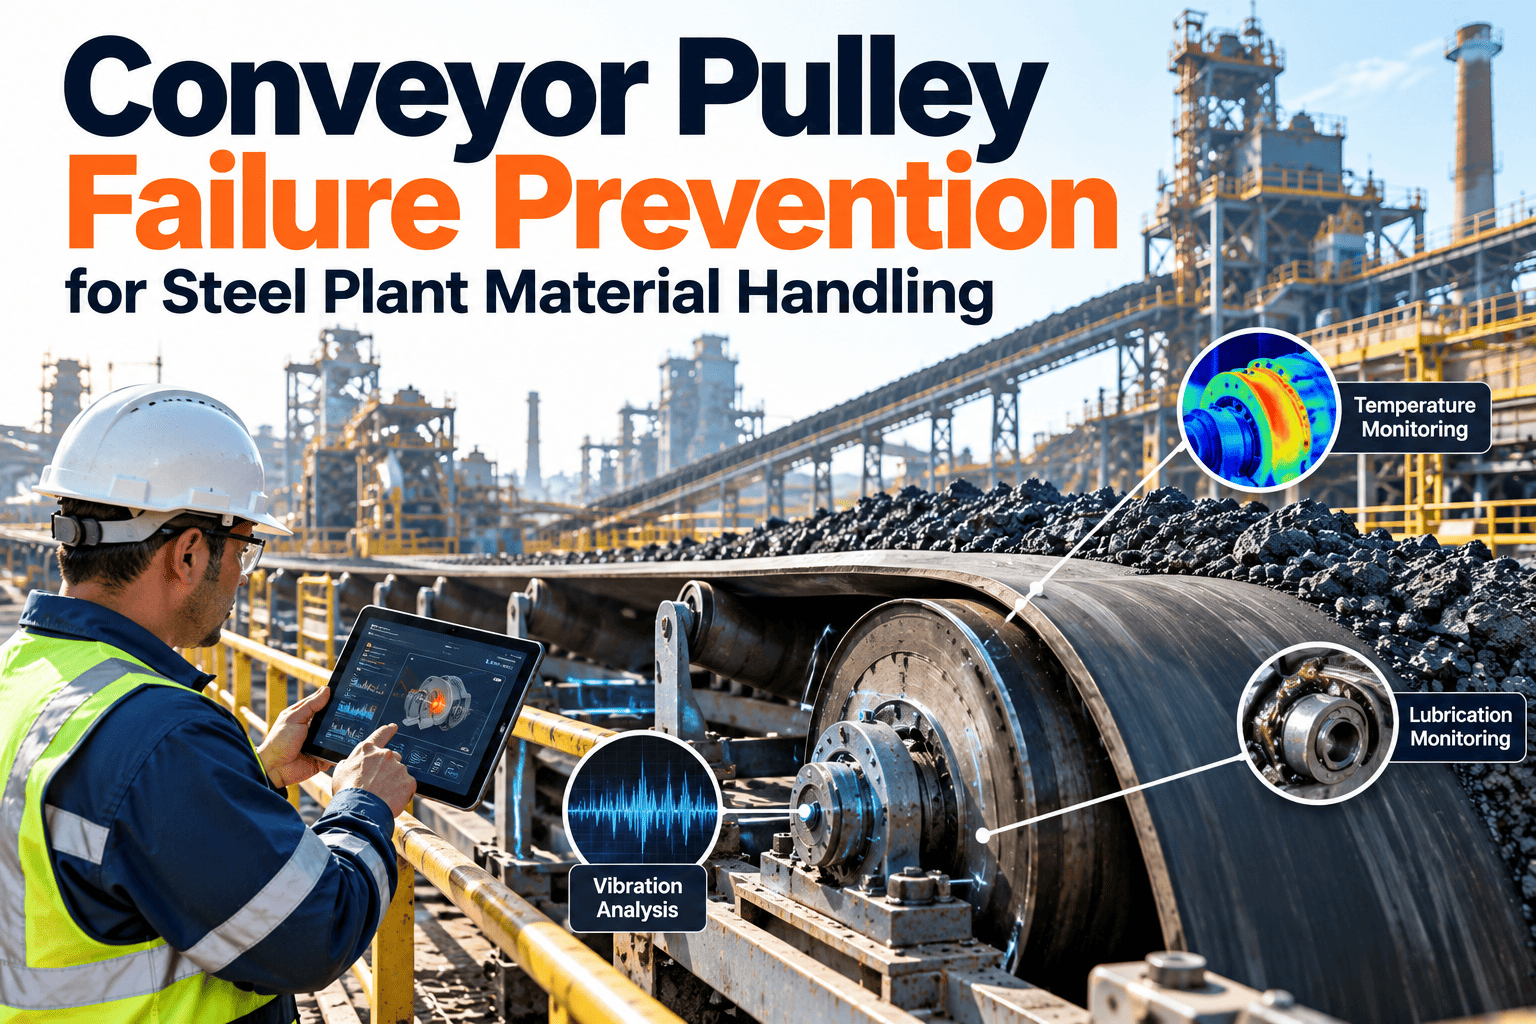
Bearing condition, alignment, shell wear, temperature and lubrication all point to the same failure. Oxmaint turns each reading into a scheduled task before the pulley stops the line.
Why Pulley Failures Cost So Much in a Steel Plant
A failed pulley is more than a part replacement. It stops the feed to a blast furnace stockhouse, sinter plant, coke handling line or raw material yard, and that stoppage spreads downstream.
The Steel Plant Operating Environment
Pulleys here work harder than in most industries. Abrasive fines, heat from sinter and coke, wet seasons and shock loads from large lumps all shorten component life.
- Abrasive ore, sinter and coke fines pack into bearing housings and onto lagging.
- Hot material raises bearing temperature and thins grease faster than planned.
- Wet or sticky material builds up on the shell and pushes the belt off track.
- Impact at transfer points loads the pulley unevenly and fatigues shafts.
- High-pressure washdown forces water past seals and into bearings.
How a Conveyor Pulley Actually Fails
Most pulley failures follow a few repeating patterns. The table links each failure mode to the early sign a technician can catch and the action that should follow.
| Component | Failure mode | Early sign | Inspection method | Maintenance response |
|---|---|---|---|---|
| Bearing | Overheating, spalling, seizure | Rising temperature, noise, vibration | Temperature trend, vibration route, ultrasound | Regrease, correct load, schedule replacement |
| Shaft | Fatigue crack, fretting at hub | Movement at the hub, rust-colored dust | Visual check, NDT during outages | Repair or replace shaft at planned shutdown |
| Shell | Wear, weld cracking, deformation | Thin spots, cracks near end discs | Thickness readings, visual inspection | Weld repair or pulley change-out |
| Lagging | Wear, debonding, buildup | Belt slip, shiny patches, lumps | Visual check, grip assessment | Clean, re-lag or replace lagging |
| Alignment | Pulley out of square | Belt tracking to one side, uneven wear | Laser or string alignment, belt edge check | Realign pulley and frame, adjust idlers |
| Seals and housing | Contamination ingress | Dirty or dry grease, leaks | Grease sampling, seal inspection | Replace seals, fix washdown practice |
The Failure Chain: From Small Misalignment to Seized Pulley
Failures are usually chains of events, not single faults. Breaking the chain early costs far less than repairing what sits at the end.
Each step offers a chance to intervene. Steps one to three are visible with simple inspections, which is why inspection discipline matters more than any single sensor.
Reactive vs Condition-Based Pulley Maintenance
What Usually Happens
- Hot bearings are noticed only when someone smells or hears them
- Greasing follows a loose route with no record of quantity
- Tracking problems are fixed by adjusting idlers, not finding the cause
- Pulley changes happen as emergencies with no parts staged
- History sits in notebooks and shift reports
What Good Looks Like
- Bearing temperature and vibration trends trigger inspections
- Lubrication tasks list grease type, quantity and interval
- Alignment is checked after any structural work or belt change
- Replacement pulleys and bearings are staged for planned outages
- Every finding and repair is logged against the pulley
Stop Finding Pulley Problems After the Belt Stops
Oxmaint links inspections, lubrication routes and work orders to each conveyor pulley, so early signs get an owner and a due date.
Building a Pulley Inspection Program
A workable program layers quick checks with deeper ones. Frequencies depend on duty, material and criticality, so treat the cadence below as a starting point to tune.
Bearing Condition Monitoring
The bearing is the most common starting point for pulley failure, and it gives the clearest early warning if someone is watching the trend.
Temperature
Absolute temperature matters less than change. A bearing that rises steadily above its own baseline, or runs much hotter than the opposite end, deserves an inspection even if it is under the alarm limit.
Vibration and Ultrasound
Periodic vibration readings reveal developing defects, and ultrasound can show lubrication starvation before heat appears. On slow-speed pulleys, trending matters more than a single reading.
Practical Bearing Checks
- Record a baseline when a new pulley or bearing goes into service.
- Use the same measurement point and method every time.
- Compare both ends of the same pulley, not only the alarm threshold.
- Check housing bolts and the condition of the locking device.
- Raise a work order when a trend moves, not when a limit is hit.
Alignment: The Hidden Driver of Pulley Wear
Many pulley bearing failures begin with alignment. A pulley that is not square to the belt line loads one bearing harder and pushes the belt to one side.
- Pulley shaft is square to the belt centerline within the plant standard
- Head and tail pulley faces are parallel to each other
- Frame and bearing pedestals show no cracks or loose anchors
- Belt tracks centered at both empty and loaded conditions
- Training idlers and return idlers turn freely and are not seized
- Loading chute delivers material to the belt center
- Alignment readings are recorded and compared with the previous check
If the belt keeps wandering after adjustment, look for the cause, such as off-center loading, buildup on the shell, a seized idler or a bent frame, before adjusting again.
Lubrication Discipline
Bearing life depends on the right grease, in the right amount, at the right interval. Both under-greasing and over-greasing cause damage.
Right grease
Match grease type and base oil viscosity to speed, load and temperature. Never mix incompatible greases.Right quantity
Record the amount applied per point. Excess grease raises temperature and can blow out seals.Right interval
Shorten intervals in hot, wet or dusty zones, and review them after every bearing failure.Shell, Lagging and Shaft Condition
The pulley body deserves the same attention as the bearings. Wear and damage here changes how the belt grips, tracks and loads the bearings.
- Lagging: Worn or debonded lagging causes slip and lowers drive efficiency, while buildup creates belt wander.
- Shell welds: Cracks near end discs indicate fatigue and call for engineering review rather than another patch.
- Shaft and hub: Fretting, loose locking assemblies and keyway wear signal movement that will worsen under load.
- Face crown: Uneven wear changes tracking behavior and should be compared with the original crown.
- Scrapers and cleaners: Poorly set cleaners let carryback reach the pulley and fill the face with material.
Prioritizing Pulleys by Criticality
Not every pulley deserves the same effort. Rank them by what happens if they fail and by how likely failure is, then set inspection depth to match.
| Pulley position | Typical consequence of failure | Likelihood drivers | Suggested focus |
|---|---|---|---|
| Drive (head) | Full loss of conveyor and feed | High torque, heat, lagging wear | Highest: condition monitoring and spares |
| Tail | Belt damage and spillage | Material ingress, buildup, impact | High: cleaning and alignment checks |
| Take-up | Belt tension loss, tracking issues | Dust, moving parts, uneven travel | Medium to high: travel and bearing checks |
| Bend and snub | Belt wander and wear | Contact with dirty belt surface | Medium: lagging and bearing route |
| Deflection | Local belt damage | Light load, buildup | Lower: routine walk-down |
KPIs That Show Whether Prevention Works
Track a short set of measures and review them with maintenance and operations together.
How Oxmaint Supports Pulley Failure Prevention
Inspection only prevents failure when findings turn into work. Oxmaint connects conveyor assets, routes and repairs in one record.
Inventory tracking also helps, since bearings, lagging and locking assemblies can be linked to the pulleys that use them and staged before an outage.
Frequently Asked Questions
Keep Every Conveyor Pulley Running Between Outages
Bring pulley inspections, lubrication, alignment checks and repairs into one maintenance system built for steel plant material handling.