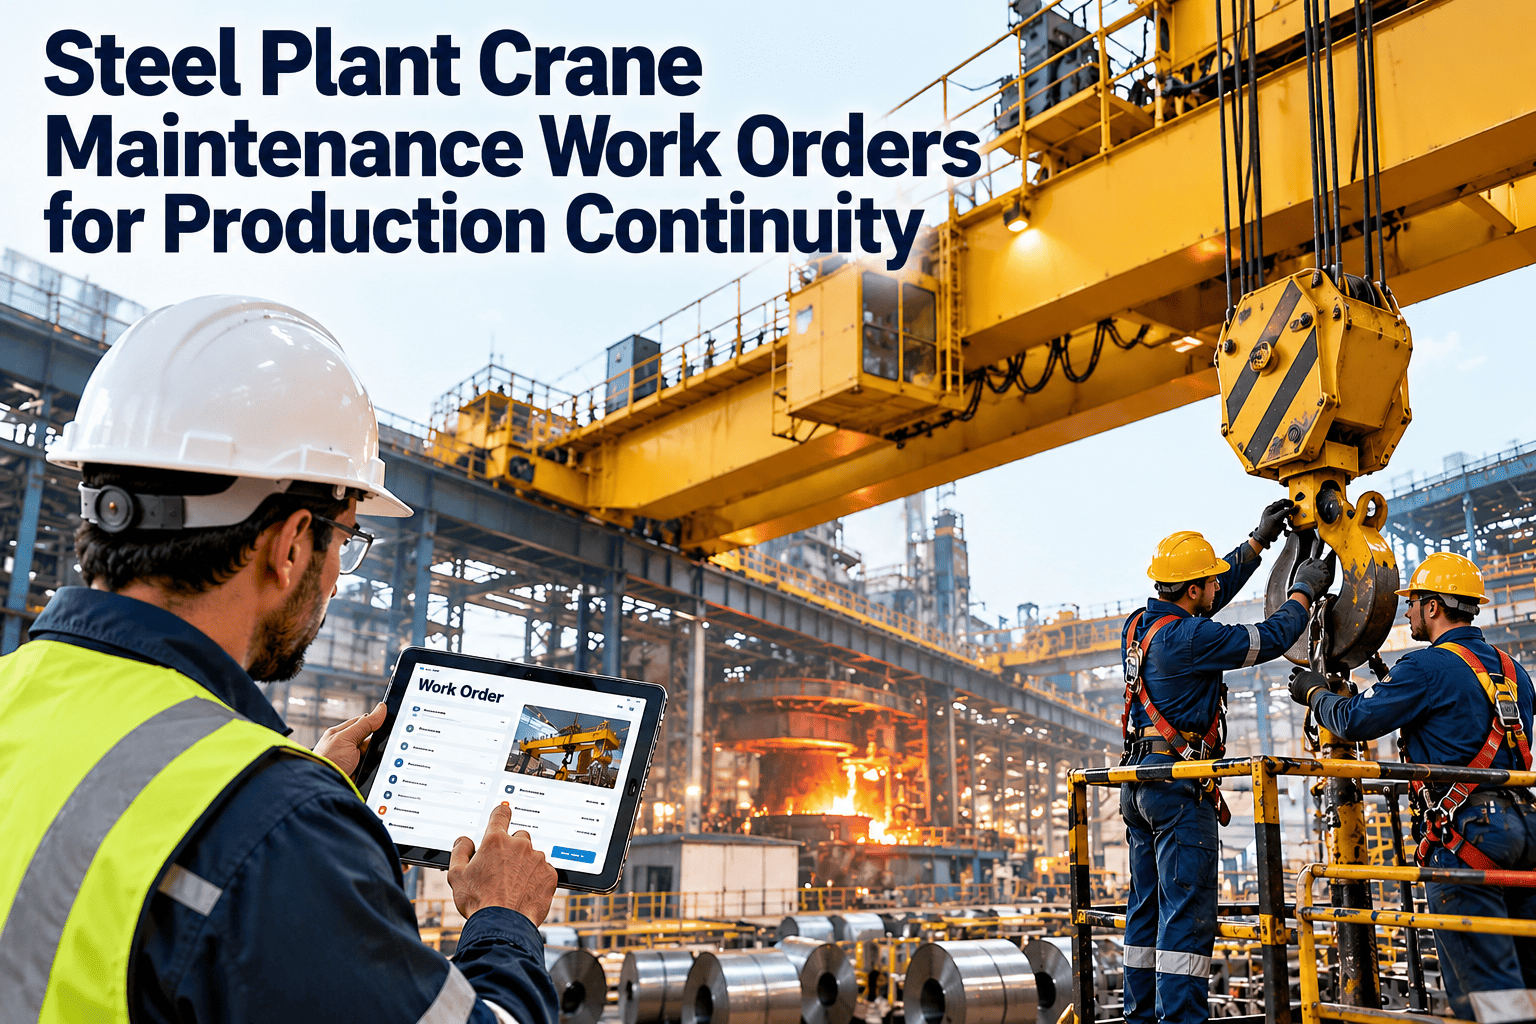
In a steel plant, overhead cranes are the connecting link between every process step, carrying hot metal, scrap, slabs, coils and heavy tooling across the shop floor. When one crane stops, the process downstream waits, and a ladle crane outage can idle a converter or caster within hours. Structured crane maintenance work orders turn inspections, wear checks and repairs into a traceable routine, and a connected crane maintenance management system keeps that routine visible to maintenance, operations and safety teams together.
Crane maintenance work orders that protect production continuity in steel plants
Link inspection findings, hoist and brake condition, runway checks and spare parts to work orders so crane problems are fixed in planned windows, not mid-pour.
Why a crane outage spreads through the whole plant
Cranes are rarely redundant in the way other equipment is. A bay may have one ladle crane, and the process depends on it for every heat.
Crane stops
A brake fault, rope issue, limit switch failure or power feed problem takes the crane out of service.
Handling halts
Ladles, scrap charges, slabs or coils can no longer be moved between stations on schedule.
Process waits
Furnaces, casters or mills hold material, break sequence or reduce rate while waiting.
Output and safety risk
Lost tonnage, rushed repairs and pressure to run a crane that should be inspected first.
Where steel plant cranes actually fail
Heat, dust, vibration, shock loads and continuous duty cycles concentrate wear in predictable places. Work order templates should reflect them.
| Component | Typical problem in steel service | What to inspect or measure | Typical maintenance response |
|---|---|---|---|
| Hoist brakes | Lining wear, heat fade, misadjustment, contamination | Lining thickness, air gap, braking response, brake wheel condition | Adjust or replace linings under a scheduled work order |
| Wire ropes | Broken wires, corrosion, flattening, heat damage, poor lubrication | Visual inspection by rope zone, diameter, lay length, end terminations | Lubricate, trend condition, replace at defined criteria |
| Gearboxes | Oil degradation, tooth wear, bearing damage, leaks | Oil condition, noise, vibration, temperature | Oil change, analysis-driven repair, planned rebuild |
| Wheels, rails and end trucks | Flange wear, rail misalignment, skewing, loose fixings | Wheel profile, gauge, alignment, fastener condition | Realign, regrind or replace during planned stops |
| Hooks and sheaves | Throat opening, wear, cracks, latch damage, sheave groove wear | Dimensional checks, crack detection, latch function | Replace out-of-limit parts, record inspection results |
| Electrical and controls | Contact wear, festoon cable damage, collector issues, limit switch faults | Insulation, connections, limit function, overload device, conductor condition | Test, repair and verify before return to service |
| Crane structure | Fatigue cracks, heat distortion, loose bolts, corrosion | Girder welds, end connections, runway beams, brackets | Specialist inspection and repair plan |
Inspection tiers that become scheduled work orders
Crane inspection is normally layered by frequency. Each tier should exist in the system as a recurring task with its own checklist and responsible role.
Operator pre-use check
Controls, brakes, limit devices, hooks, ropes in view and abnormal noise or movement. Defects are reported at once and can open a corrective work order.
Frequent inspection
Maintenance technicians check ropes, brakes, lubrication, hook condition, electrical connections and visible structural changes.
Periodic inspection
Detailed examination of components, measurements against limits, load testing where required and review by a competent person.
Special inspection
Triggered by overload, collision, repair, relocation or long idle periods before the crane returns to service.
Frequency depends on duty, not on habit
- Ladle cranes and other hot metal service typically justify tighter intervals than light-duty auxiliary cranes.
- Intervals should reflect manufacturer guidance, applicable regulations and the plant's own failure history.
- Findings that repeat on the same crane are a reason to shorten the interval or fix the root cause.
The crane work order lifecycle
A work order is more than a task. It carries the defect, the decision, the parts, the repair and the proof that the crane is safe to run again.
Detect
Operator report, inspection finding or condition alert identifies the issue.
Assess
Maintenance judges severity and decides if the crane must be tagged out of service.
Plan
Parts, tools, crew, lockout and access are arranged against the production schedule.
Repair
Technicians complete the job and record measurements, replaced parts and time.
Verify
Functional tests and sign-off confirm the crane can return to service.
Learn
History is reviewed for repeat faults and the inspection plan is adjusted.
Prioritising crane defects by risk
Not every defect needs the same response. A simple matrix helps technicians and planners agree quickly on urgency.
Defects that should always trigger a safety review
- Any brake performance problem on a hoist that carries molten metal.
- Broken rope strands or heat damage near a termination.
- Cracks in hooks, welds or primary load-carrying structure.
- Failed or bypassed limit switches and overload protection.
From calendar tasks to condition-based crane care
Calendar preventive maintenance is the foundation. Condition data refines it, so effort goes where the wear actually is.
- Same interval for every crane regardless of duty.
- Inspection notes kept on paper and rarely compared.
- Wear found at the next breakdown rather than at measurement.
- Spares ordered after the failure.
- Intervals adjusted for duty cycle and failure history.
- Measurements recorded and trended on the asset.
- Wear limits trigger planned repair before failure.
- Spares reserved when trends predict replacement.
| Condition signal | Possible source | Work order response |
|---|---|---|
| Rising gearbox vibration or temperature | Inspection route, handheld readings, installed sensors | Inspect gears and bearings, check lubrication, plan repair |
| Oil analysis showing wear metals or moisture | Scheduled oil samples | Change oil, locate ingress, schedule teardown if trending worse |
| Brake lining approaching limit | Measured thickness during frequent inspection | Reserve parts and schedule replacement in a planned stop |
| Increasing motor current or run time | Drive data, operator reports | Check mechanical resistance, alignment and electrical condition |
| Rope diameter reduction or broken wires | Rope inspection records | Increase checks, plan replacement before reaching the discard criteria |
Compliance records that work orders should capture
Regulations and standards differ by country, but auditors and incident investigators ask for similar evidence.
Inspection evidence
Who inspected which crane, on what date, using which checklist, with what findings and what follow-up. Requirements such as those in OSHA 1910.179 and ASME B30.2 describe inspection and maintenance expectations for overhead cranes, and local rules may add more.
Repair and test records
Replaced parts, measurements, load or function tests and sign-off by a competent person before the crane returns to service.
Operator and rigging records
Pre-use checks, reported defects and training status for operators, so safety and maintenance data tell one story.
Crane spare parts and planning for the next stop
A crane repair is only as fast as its slowest missing part.
Critical crane spares to review
- Brake linings, shoes, springs and thrusters.
- Rope sets, terminations and lubricants.
- Limit switches, contactors and collector shoes.
- Gearbox bearings, seals and couplings.
- Wheels, bearings and festoon cable components.
Planning practices that shorten stops
- Agree crane availability windows with production in advance.
- Kit parts, tools and permits before the crane is released.
- Bundle several tasks into one outage instead of many short ones.
- Use standard job plans for repeat repairs so crews follow proven steps.
- Record actual hours so future windows are sized realistically.
Measuring crane reliability and maintenance quality
Review a small set of indicators per crane and per bay.
Special attention for ladle and hot metal cranes
Cranes that carry molten metal operate under the harshest conditions in the plant and carry the highest consequence if something fails.
Why the duty is different
- Radiant heat accelerates wear on ropes, lubricants, cables and structural steel.
- Splash, slag and dust contaminate brakes, rails and electrical equipment.
- Loads are heavy, valuable and hazardous, so a hoist failure has severe consequences.
- Duty cycles are continuous, which leaves little time for maintenance without planning.
What the maintenance plan should reflect
- Tighter inspection intervals and clear acceptance limits for brakes and ropes.
- Redundant safety features checked and tested, not assumed to be working.
- Heat protection and cable condition included in routine checks.
- Competent-person review and documented sign-off after major repairs.
Making operators and maintenance work from the same record
Operators notice abnormal behaviour first. Maintenance fixes it. The link between them is the report that becomes a work order.
Operator notices
A change in sound, braking, swing or hoist speed is noticed during normal operation.
Defect logged
The report is entered with the crane, symptom and a photo where useful, instead of a verbal message that is forgotten.
Maintenance triages
A technician assesses severity, restricts or stops use if needed and plans the repair window.
Feedback returned
The operator sees the outcome, which encourages further reports and builds trust.
Habits that make reporting work
- Keep the reporting method simple enough to use with gloves and in a noisy bay.
- Respond visibly to early reports so operators see the value of raising them.
- Review repeated operator comments during reliability meetings, because they often precede failures.
A practical rollout path for crane work orders
Plants that digitise every crane at once often struggle. Start with the cranes that stop production and expand from there.
Rank cranes by production impact
Identify which cranes have no backup and which bays depend on a single lift for every heat or cycle.
Build the asset structure
Register each critical crane with its hoist, trolley, bridge, brakes, ropes and controls so work can be recorded at the right level.
Load inspection and preventive tasks
Convert existing paper checklists into recurring tasks with assigned roles and clear pass or fail criteria.
Review and refine
After a few months, study repeat defects, adjust intervals and add condition measurements where wear is most costly.
Gaps that undermine crane maintenance programmes
Audits and incident reviews tend to uncover the same weaknesses, and most are about records and follow-through rather than technical knowledge.
Questions to ask in a monthly crane reliability review
- Which cranes had unplanned stops, and did the same component fail more than once?
- Which inspections were overdue, and what stopped them from being completed?
- Which defects were raised by operators, and how quickly did maintenance respond?
- Which spare parts were missing or late during crane repairs?
- Do any inspection intervals need to be shortened or extended based on actual findings?
How Oxmaint supports crane maintenance workflows
Cranes combine inspection routines, mechanical wear and safety records, which suits a system that links assets, work orders and history.
Asset register by crane
Organise each crane with hoists, drives, brakes and ropes as components so history sits where the work was done.
Recurring inspection tasks
Schedule pre-use, frequent and periodic inspections with checklists and assigned roles.
Corrective work orders
Raise defects from the floor on mobile devices, with priority, photos and notes.
Spare parts linkage
Attach parts to tasks and check availability before the planned stop.
Records and reporting
Keep inspection and repair history available for audits and review reliability trends by crane.
Crane maintenance work orders: frequently asked questions
What should a crane work order include?
It should list the crane and component, defect or task, safety steps, parts, measurements, test results and sign-off.
How often should steel plant cranes be inspected?
Frequency depends on duty, manufacturer guidance and local regulation, with ladle and heavy-duty cranes usually needing closer attention.
Can operators raise defects directly?
Yes, mobile reporting lets operators log issues at once so maintenance can assess them quickly. You can schedule a demo to see the flow.
Is condition monitoring necessary for cranes?
It is not mandatory everywhere, but trending measurements and oil results helps focus planned work on real wear.
How do we start digitising crane maintenance?
Begin with your most critical crane and its inspection routines. You can sign up and load that asset first.
Keep every crane lifting when the plant needs it
Turn inspections, defects and repairs into one traceable workflow for steel plant material handling.