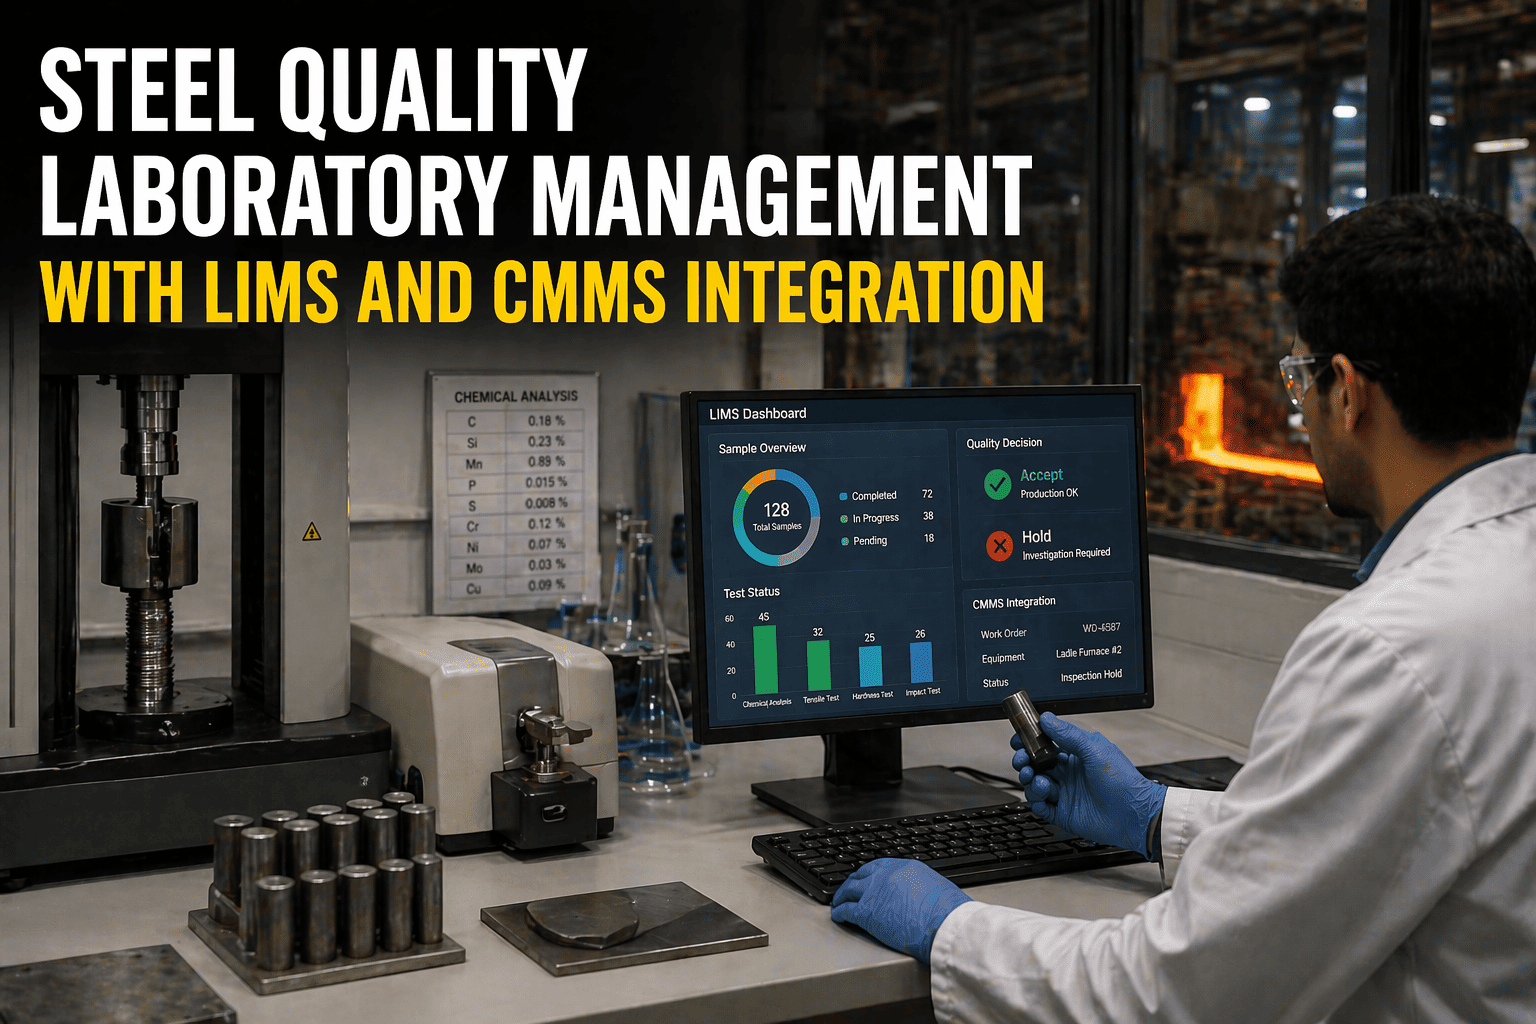
A quality nonconformance in a steel plant is rarely only a quality event. A surface defect, dimensional drift or chemistry deviation often traces back to a worn mold, a drifting sensor, a missed lubrication task or a roll that stayed in service too long. When quality and maintenance records sit in separate systems, the material is contained but the equipment cause stays open. This guide shows how to manage nonconformances from detection to closure, and how maintenance software ties each NCR and CAPA to asset history and corrective work.
Steel Plant Nonconformance Management That Reaches the Equipment Root Cause
Move every NCR through containment, investigation, corrective action, verification and closure, with maintenance evidence attached at each step.
- 1Detect
- 2Contain
- 3Investigate
- 4Correct
- 5Verify
- 6Close
Why the Same Nonconformance Keeps Coming Back
What the quality file usually holds
- Heat, lot and product identification
- Defect description and disposition
- Customer or internal complaint reference
- A corrective action that names a procedure change
What is often missing
- Equipment condition at the time of production
- Recent repairs, adjustments or deferred work
- Calibration status of the sensors involved
- Proof that the maintenance fix was completed
Typical consequences
- Root cause is recorded as operator error when the equipment drifted first.
- Corrective actions close on paper without a verified change on the asset.
- Similar defects across shifts are never connected to one worn component.
The NCR-to-CAPA Lifecycle, Step by Step
Detect and record
Log the nonconformance at the point of discovery with product identity, location, quantity, photos and measurements.Contain and disposition
Segregate suspect material, hold or reroute it, and decide rework, downgrade, scrap or customer concession.Investigate the cause
Review process data, asset condition, inspection results and maintenance history for the equipment involved.Correct and prevent
Separate the immediate correction from the corrective and preventive action, and raise work orders for equipment fixes.Verify effectiveness
Confirm the fix was completed and watch the defect rate over a defined period.Close with evidence
Close only when records show the cause, the action, the verification and any updated PM or inspection content.Defect Signals and the Equipment Questions Behind Them
| Nonconformance type | Equipment areas worth reviewing | Evidence to pull |
|---|---|---|
| Surface cracks or marks on cast product | Mold condition, oscillation, spray cooling, rolls and segments | Mold and segment inspection records, spray nozzle checks, oscillation maintenance history |
| Dimensional or gauge variation | Roll wear, mill stand condition, gauge sensors, hydraulic gap control | Roll change logs, sensor calibration, hydraulic maintenance records |
| Temperature or chemistry deviation | Furnace systems, probes, sampling equipment, ladle treatment equipment | Probe calibration, burner or electrode inspections, analyzer service records |
| Flatness or shape defects | Leveler, cooling beds, rolls, cooling water systems | Alignment checks, water flow and nozzle inspections, bearing condition |
| Weight or length errors | Scales, shears, measuring systems, conveyors | Calibration certificates, shear blade changes, encoder and sensor faults |
| Coating or finishing defects | Line rolls, baths, air knives, filtration, drives | Roll surface inspections, pump and filter records, process parameter logs |
Using the table responsibly
- These are lines of inquiry, not conclusions. Metallurgical and process causes must be investigated alongside equipment causes.
- Record when the equipment was ruled out, not only when it was confirmed.
Connect Every NCR to the Asset That Produced It
Raise corrective work orders from quality findings and keep the cause, action and verification in one traceable history.
Severity and Containment: Decide Response Before Debate
Critical
- Safety or regulatory impact
- Material already shipped or at risk of shipping
- Immediate containment and full investigation
Major
- Specification failure on active orders
- Repeat of a known defect
- Documented root cause and CAPA required
Minor
- Isolated deviation, internally corrected
- No customer impact
- Trend review and correction record
Choosing the Right Root Cause Method
| Method | Best used when | Watch out for |
|---|---|---|
| 5 Whys | A single failure chain and fast investigation are needed | Stopping at the first convenient answer |
| Fishbone diagram | Several causes across people, method, material, machine and measurement are possible | Listing causes without testing them |
| Fault tree analysis | A serious or repeated failure needs logic-based analysis | Time required and need for good data |
| FMEA review | A recurring defect suggests the failure mode was never analyzed | Updating the FMEA without updating inspections |
Traceability That Includes Maintenance Events
Events worth linking to the material path
- Roll, mold or blade changes and the date they were made
- Sensor calibration and instrument replacements
- Breakdowns, adjustments and temporary repairs during production
- Deferred defects that were open when the material was made
Why it matters
- Investigators can narrow the affected window instead of quarantining everything.
- Customer responses can show what changed on the equipment and when.
A CAPA Effectiveness Checklist
- The root cause is supported by data, not assumption.
- Correction and corrective action are recorded separately.
- Every equipment action has a work order with an owner and due date.
- PM tasks, inspection points or limits were updated where needed.
- Training or procedure changes are documented for affected crews.
- A verification period and measure are defined before closure.
- Recurrence is reviewed at a set interval after closure.
Measures That Show Quality and Maintenance Are Aligned
How Oxmaint Supports the Maintenance Side of Quality
- Corrective work orders: turn an investigation finding into a tracked repair with owner, parts and completion record.
- Asset history: show repairs, inspections and adjustments around the time a defect occurred.
- Preventive maintenance: update tasks and frequencies after a CAPA changes the maintenance strategy.
- Inspections: add check points that catch the condition behind a recurring defect.
- Reporting: review repeat failures and overdue actions by line or asset.
A note on scope
- Oxmaint manages the maintenance workflow that closes equipment-related actions. Your quality management processes and certified procedures still define how nonconformances are classified and approved.
Frequently Asked Questions
What is a nonconformance report in a steel plant?
How is CAPA different from correction?
Why involve maintenance in quality investigations?
Can corrective actions become work orders?
Can I see a workflow for my plant?
Close Quality Actions on the Equipment, Not Only on Paper
Link nonconformances to asset history, corrective work and verified results.