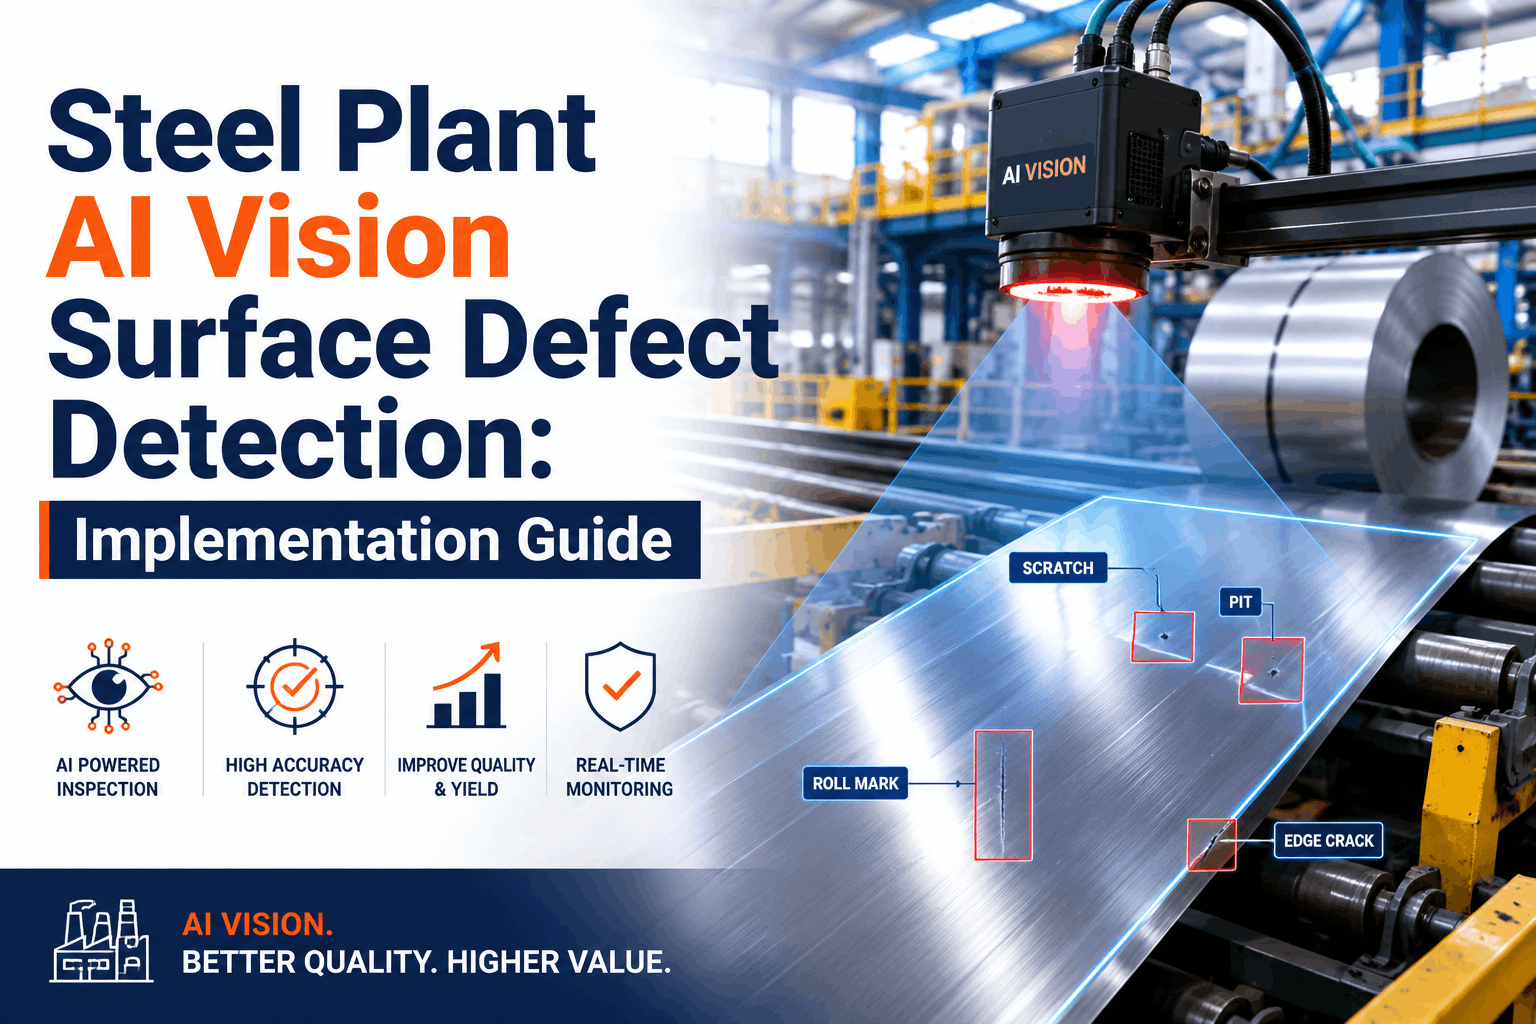
Zero-Defect Steel Manufacturing: How Vision AI Makes It Possible
By Lebron on March 11, 2026
Zero-defect manufacturing is not a theoretical aspiration in steel production — it is an operational reality achieved by the world's leading integrated steel mills through systematic defect elimination backed by AI-powered quality intelligence. A specialty steel producer in Germany targeting zero-defect delivery to aerospace customers deployed vision AI inspection across their finishing lines and discovered within six months that their defect escape rate had dropped from 2.3% to 0.08% — equivalent to recovering $18.7 million in annual revenue through eliminated customer claims, avoided downgrades, and market share retention in mission-critical applications where even a single defect can trigger aircraft grounding. The journey to zero-defect is not about inspection perfection — it is about connecting every defect detection back to its upstream root cause, triggering immediate corrective action, and building a closed-loop system where defects are prevented rather than detected.
Achieving zero-defect steel manufacturing requires three converging capabilities: AI vision systems that detect every surface anomaly at production speed without fatigue or subjectivity, root cause analysis workflows that trace each detected defect back to the specific equipment condition or process parameter that created it, and CMMS-driven corrective action systems that prevent the root cause from ever producing another defect. Most steel mills fail at the third capability — they detect defects accurately but lack the systematic machinery to connect detection to prevention. Oxmaint delivers the integrated quality-to-maintenance platform that transforms AI vision inspection from a passive quality reporting system into an active defect prevention engine — closing the loop from detection through analysis to permanent elimination. Start your free trial to begin your journey toward zero-defect steel manufacturing today.
Zero-Defect Excellence Framework 2026
Zero-Defect Steel Manufacturing: How Vision AI Makes It Possible
The complete framework for achieving zero-defect steel manufacturing through AI vision inspection, defect root cause analysis, and closed-loop CMMS-driven prevention. This guide covers the technology infrastructure required, the quality management workflows that eliminate defect root causes, the process improvements that prevent recurrence, and the measurable path from current-state quality escape rates to world-class zero-defect performance.
2.3%Baseline Defect Escape Rate
0.08%Achieved After AI Deployment
$18.7MRecovered Annual Value
6 moTime to Target Performance
The Three Pillars of Zero-Defect Steel Manufacturing
Zero-defect steel manufacturing is built on three interdependent pillars that must operate in perfect synchronisation. Each pillar addresses a critical stage in the defect elimination chain — from initial detection through analysis to permanent prevention. Missing any pillar degrades the entire system and prevents progression toward zero-defect performance.
Pillar 1: Detection Intelligence
AI vision systems achieve 95%+ detection accuracy across all surface defect types at full production speed — capturing every anomaly before it reaches the customer. Detection consistency 24/7 eliminates the fatigue and subjective judgment that degraded manual inspection. Real-time classification into 200+ defect types enables immediate root cause correlation.
Pillar 2: Root Cause Analysis
Every detected defect is automatically correlated with upstream equipment conditions, process parameters, and maintenance history. Pattern recognition identifies which specific root causes are generating which defect types. Machine learning reveals causal relationships invisible in manual analysis. The goal is not perfect root cause on every defect but systematic elimination of the pareto-critical causes driving 80% of escapes.
Pillar 3: Prevention Execution
Identified root causes trigger CMMS-driven corrective and preventive actions before they produce another defect. Equipment maintenance work orders, process parameter adjustments, operator training programmes, and design modifications are generated automatically and tracked to completion. Success is measured not by defect detection rates but by whether the same root cause ever produces another defect.
The Defect-Prevention Cascade: From Detection to Elimination
Zero-defect manufacturing is not achieved through flawless execution of every step — it is achieved through systematic elimination of the root causes that account for 80% of defects. The cascade below shows the complete journey a defect takes from detection through permanent elimination in a zero-defect programme. Discover how Oxmaint automates this entire cascade.
Detection
AI vision detects defect in real time — classified, sized, positioned, timestamped. Data immediately uploaded to CMMS with full image evidence and defect metadata.
Defect correlated with upstream equipment conditions at time of production — roll condition, tundish age, descaler performance, process temperature, operator on shift. Historical patterns analysed for similar defects and known root causes.
Root Cause Hypothesis
CMMS surfaces most likely root cause based on defect type, equipment state, and historical patterns. Analytics engine suggests corrective actions and links to previous successful solutions. Human engineer validates hypothesis.
Prevention Action
Corrective work order generated and tracked to completion — roll change, equipment calibration, process parameter lock-out, operator retraining, or design modification. All actions linked to the defect record.
Verification
Post-implementation monitoring of downstream production for recurrence of same defect pattern. If eliminated, defect is archived as "prevented." If recurrence detected, investigation re-escalated with new evidence.
Zero-Defect Performance Metrics and Thresholds
Zero-defect does not mean zero defects detected — it means zero defects escaping to customers and zero repetition of the same root cause. The metrics below define what world-class zero-defect performance looks like across the key quality dimensions that drive customer satisfaction and market position in mission-critical steel applications.
Defect Escape Rate
Current: 2–5%
Improving: 0.5–1%
Zero-Defect: <0.1%
% of shipped tonnes with customer-discoverable defects
Root Cause Identification Rate
Manual: 35%
AI + CMMS: 75%
Zero-Defect: 95%+
% of detected defects with confirmed root cause
Recurrence Prevention Rate
Reactive: 15%
Proactive: 60%
Zero-Defect: 95%+
% of identified root causes permanently eliminated
Detection-to-Action Cycle Time
Manual: 5–14 days
AI + CMMS: 2–4 hours
Zero-Defect: <60 min
Time from defect detection to prevention action initiation
Seven Countermeasures That Enable Zero-Defect Performance
Zero-defect performance is not achieved through a single initiative — it requires systematic deployment of seven complementary countermeasures that operate across detection, analysis, and prevention. Each countermeasure addresses a specific gap in typical steel mill quality systems. Deploying all seven in an integrated fashion enables progression from 2–5% escape rates to under 0.1%.
01AI Vision Inspection
Real-time 95%+ detection accuracy at production speed — replacing human visual inspection fatigue and subjectivity with consistent, documented defect capture across 200+ defect classes. Detection data immediately classified, measured, and geo-tagged for downstream correlation.
02Defect Pattern Recognition
Machine learning algorithms identify recurring defect patterns across all coils — scratches increasing in severity, inclusions clustering in specific areas, roll marks progressing over time. Patterns surface anomalies invisible in individual coil data and predict which root causes are producing multiple escapes.
03Automated Root Cause Hypothesis
CMMS automatically correlates detected defects with upstream equipment conditions, process parameters, and historical root cause patterns. System surfaces the most likely root cause with confidence scoring, acceleration of investigation from days to minutes, and enabling engineers to focus on validation rather than information gathering.
04CMMS-Triggered Preventive Action
Every confirmed root cause auto-generates CMMS work orders with assigned owner, deadline, and resource allocation. Actions tracked to completion with full audit trail. No prevention action falls through the cracks or stalls in the workflow. Completion tied to defect recurrence monitoring.
05Process Parameter Lock-out
Once a defect-causing process condition is identified, the production system is configured to prevent recurrence — roll speed limits, temperature windows, equipment parameter interlocks. Critical parameters are locked after root cause identification, preventing human operator deviation that might re-introduce the same defect.
06Continuous Verification Monitoring
Post-implementation AI vision monitoring confirms that the defect pattern has been eliminated. If identical defects recur, the work order is re-escalated with new evidence rather than closed as complete. Only after 50+ consecutive defect-free production units is the prevention action marked as verified.
07Knowledge Base & Standard Work
Every successfully eliminated root cause is archived in a searchable plant-wide knowledge base with complete documentation of the defect pattern, root cause investigation, proven solutions, and lessons learned. New operators, quality engineers, and maintenance teams access this institutional knowledge to accelerate learning and prevent knowledge loss through staff turnover.
12-Month Implementation Roadmap to Zero-Defect
The journey to zero-defect steel manufacturing follows a structured 12-month roadmap that builds capability sequentially — starting with detection infrastructure and AI model training, progressing through root cause analysis workflows and CMMS integration, and culminating in closed-loop prevention systems and continuous verification monitoring. Each phase has clear success metrics and gates before advancing to the next phase.
Q1: FoundationBaseline 2–3% Escape Rate
Deploy AI vision hardware on two production linesCollect 100,000+ labelled defect images from plant historyTrain AI models on plant-specific defect taxonomyEstablish baseline defect escape measurements and root cause trackingIntegrate CMMS with AI vision platform
Q2: Detection & Analysis1.2–1.8% Escape Rate
AI vision goes into production across all major linesDefect pattern recognition algorithms identify recurring causesRoot cause hypothesis engine deployed — auto-surfacing likely causesFirst 50 high-impact root causes formally analysedInitial corrective actions triggered via CMMS
Q3: Prevention & Action0.5–0.8% Escape Rate
Corrective actions from Q2 root cause investigations executed and verifiedProcess parameter lock-out implemented on critical processesKnowledge base established with first 100+ root cause solutionsVerification monitoring confirms 60%+ of implemented actions eliminated defectsRemaining escape rate pareto-analysed for next wave of improvements
Q4: Optimisation & Excellence<0.1% Escape Rate
Advanced analytics and predictive models deployed to forecast defects before occurrenceFull integration of quality data with equipment maintenance schedulesCustomer-specific quality thresholds locked into production controlsZero-defect culture embedded in operations — all teams understand their roleContinuous improvement cycle self-sustaining through knowledge base and automated workflows
Make Zero-Defect Your Operational Reality
Oxmaint connects AI vision detection, automated root cause analysis, CMMS-driven prevention, and verification monitoring into a single integrated system. Stop detecting defects — start preventing them. Transform your escape rate from 2–5% to under 0.1% and claim your position among the world's zero-defect steel manufacturers.
ROI and Business Impact: Zero-Defect Steel Manufacturing
Annual Economic Impact: Single Specialty Steel Production LineBaseline 2–5% escape rate vs zero-defect <0.1% achieved through AI vision and CMMS integration
Current State: 2–5% Escape Rate
Customer quality claims & returns$2.4M – $8.2M/yr
Downgrade & rework costs$1.2M – $4.8M/yr
Lost market premium from escapes$800K – $3.2M/yr
Manual inspection labour$400K – $900K/yr
Reactive root cause investigations$300K – $600K/yr
Market premium from zero-defect brand$1.2M – $3.6M gained
Eliminated rework & downgrade$900K – $3.6M saved
Automated root cause efficiency$240K – $480K saved
Net Annual Value: $3.6M – $13.4M+
Three Critical Success Factors for Zero-Defect Programmes
The difference between zero-defect programmes that succeed and those that stall is not technology capability — it is organisational discipline across three critical success factors. Missing any one factor predictably undermines the entire programme and prevents progression beyond the initial 1–2% escape rate improvement.
CSF 1
Closed-Loop CMMS Discipline
Every defect detected by AI vision must flow through CMMS into a root cause investigation and corrective action work order. No defects escape the system unanalysed. No prevention actions go untracked. The CMMS becomes the single system of truth for all quality data and linked equipment actions. Organisations that skip CMMS integration and try to manage quality data through spreadsheets or verbal communication invariably fail to achieve zero-defect performance because root causes identified in one shift are forgotten by the next shift.
CSF 2
Process Parameter Immutability
Once a defect-causing process condition is identified and its prevention action implemented, that condition must be locked into the process control system to prevent human operator deviation that might re-introduce the same defect. Critical parameters must be inter-locked so that an operator cannot accidentally override process controls that were put in place to prevent a known defect. Organisations that implement process changes without control-system lock-out routinely experience recurrence of the same defect patterns because new operators revert to old unsafe practices under production pressure.
CSF 3
Verification-Based Closure
No prevention action is marked as complete until post-implementation monitoring confirms that the root cause has been permanently eliminated. A defect-free period of 50+ consecutive production units is insufficient — the verification must continue for 4–8 weeks of continuous operation before the work order is closed. Organisations that close prevention actions after first success predictably experience 25–40% recurrence because the root cause was only partially addressed or conditions reverted after initial success monitoring ended.
Close the Loop: From Detection to Prevention to Verification
Oxmaint enforces the three critical success factors systematically: CMMS-integrated quality data flow, process parameter lock-out enforcement, and multi-week verification monitoring before closure. Build the operational discipline that zero-defect manufacturing demands.
Q. Is zero-defect manufacturing (0% escape rate) actually achievable in steel production?
True zero-defect (0% escape rate) is theoretically impossible due to random process variation — but zero-defect programmes target <0.1% escape rates, which is operationally equivalent to zero from a customer and business perspective. World-leading integrated steel mills routinely achieve 0.05–0.15% escape rates on specialty grades through systematic deployment of AI vision inspection, automated root cause analysis, and closed-loop CMMS-driven prevention. The distinction is important: zero-defect programmes do not expect to eliminate every single defect occurrence — they expect to eliminate every defect category that has ever been root-caused and prevent those specific defect types from ever recurring. Defects that arise from novel root causes not previously encountered may still occur, but the programme has zero recurrence of known causes.
Q. How does zero-defect manufacturing integrate with lean and continuous improvement methodologies?
Zero-defect programmes are fundamentally aligned with lean and kaizen principles because they target systematic elimination of waste (defects and rework) and continuous incremental improvement through systematic root cause analysis and prevention. The key difference is that traditional lean focuses on process flow and efficiency, while zero-defect programmes focus specifically on quality loss elimination. The strongest implementations combine both: lean methodology manages the process flow and capacity optimisation, while zero-defect programmes focus specifically on quality loss and prevention of customer escapes. Both use the same CMMS platform for tracking, both follow Plan-Do-Check-Act cycles, and both rely on cross-functional teams and operator engagement. An integrated programme attacks both flow losses and quality losses simultaneously.
Q. What is the typical progression timeline from 2–5% escape rates to <0.1% zero-defect performance?
A realistic zero-defect progression follows this timeline. Months 1–3: detect all defects accurately through AI vision deployment — baseline escape rate may initially appear to increase because human inspection was missing defects. Months 3–6: root cause analysis on top 30–50 pareto-critical defect patterns and implementation of initial prevention actions. Escape rate typically improves to 1–2%. Months 6–9: continue prevention action implementation and verification on remaining pareto-critical causes. Escape rate typically reaches 0.3–0.6%. Months 9–12: advanced analytics, process lock-out implementation, and continuous verification monitoring. Target <0.1% escape rate achievable by 12 months. Sign up for Oxmaint to start your zero-defect journey with an integrated platform.
Q. How do you prevent recurrence of the same defect type after a prevention action is implemented?
Preventing recurrence requires three systematic controls. First, the root cause must be correctly identified — which requires comprehensive data analysis linking defects to upstream conditions rather than assumption. Second, the prevention action must address the root cause rather than just the symptom — replacing a roll addresses roll surface defects but rolling at higher speed may reintroduce the defect; the root cause is the roll surface condition, the prevention action is replacing the roll, and the control is locking the new roll into service and preventing speed increases. Third, post-implementation verification must continue for 4–8 weeks of continuous operation before the action is marked complete — not just 5 defect-free units. Organisations that fail at any of these three stages experience 25–40% recurrence rates. The best programmes use CMMS-enforced verification gates that prevent closure until multi-week monitoring is complete.
Q. What is the relationship between zero-defect programmes and customer quality specifications?
Zero-defect programmes align with customer-specific quality specifications through automated comparison of AI-detected defects against each customer's acceptance thresholds. Mission-critical applications like aerospace demand <0.05% escape rates — triggering maximum prevention action on any defect. Standard applications may accept <0.3% — allowing slightly higher thresholds for less critical defect types. The zero-defect programme customises its prevention urgency based on which customer the production is targeted for. Additionally, zero-defect performance becomes a market differentiator — ability to guarantee <0.1% escape rates enables premium positioning and access to mission-critical markets where competitors operating at 1–2% escape rates cannot compete. Book a demo to see how Oxmaint manages customer-specific quality thresholds.