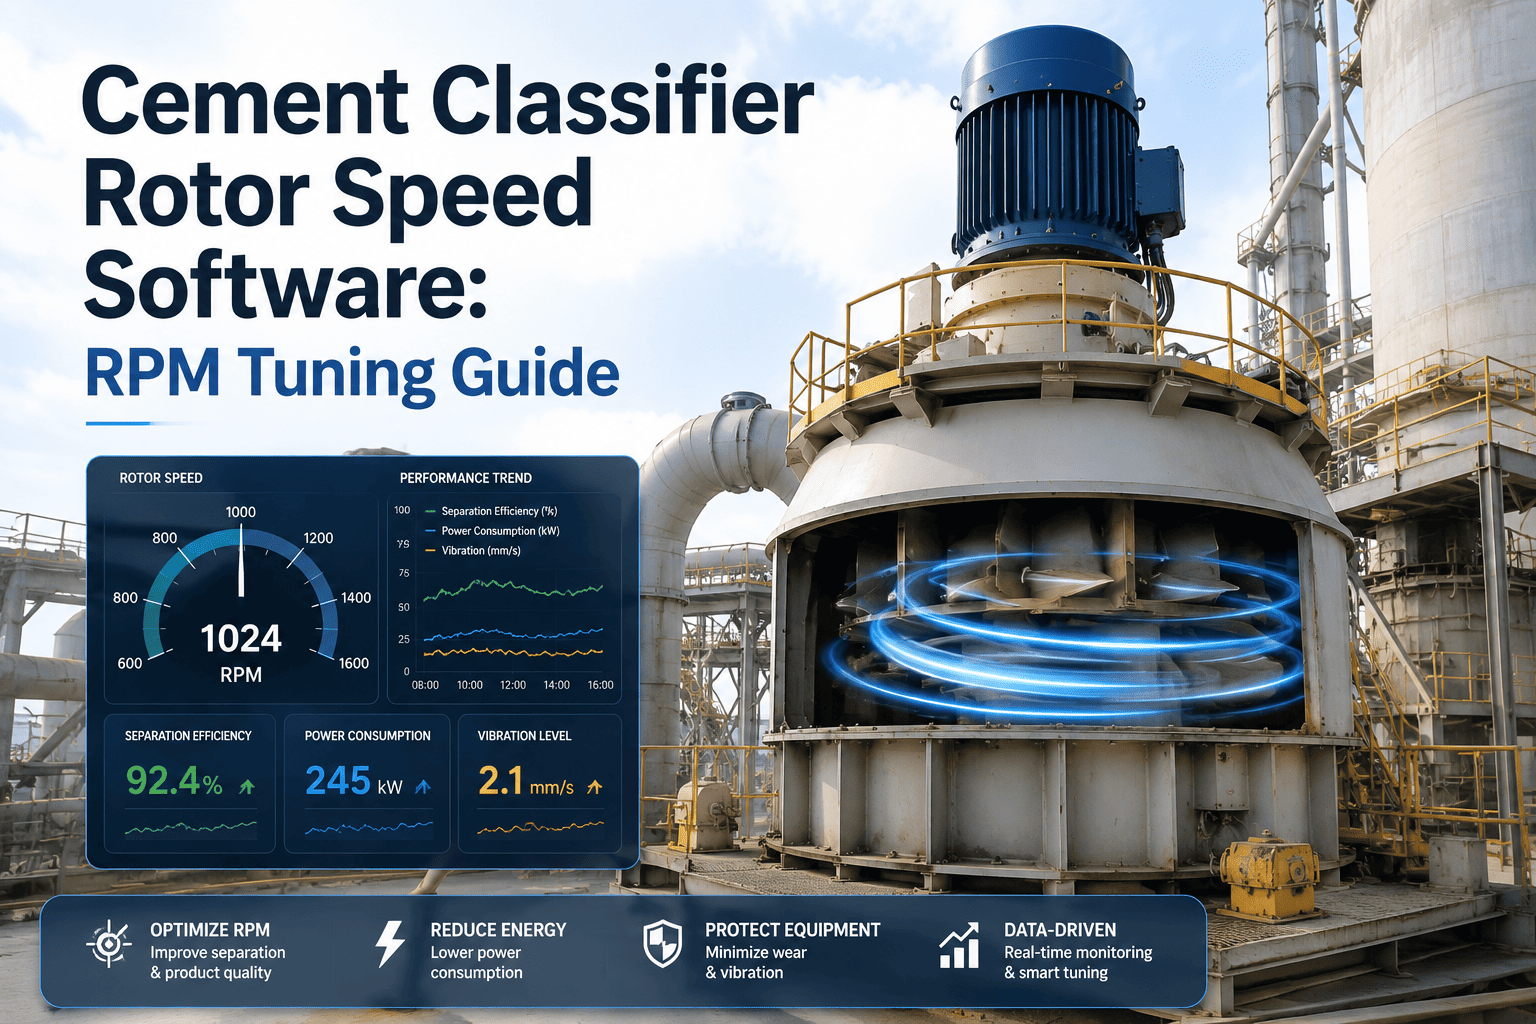
A cement classifier rotor spinning at 53 RPM and the same rotor spinning at 65 RPM produce two different plants. One ships cement at 3,300 Blaine and burns 22 kWh/t doing it. The other hits 3,900 Blaine, satisfies the lab, and quietly adds 2.6 kWh/t to every tonne ground for the next six months because nobody walked the setpoint back down once the order was filled. Classifier rotor speed is the single dial that decides cut size, circulating load, and specific power draw on a vertical roller mill or high-efficiency separator, yet on most cement plants it is set once by the OEM commissioning team and never revisited by RPM, only nudged by feel during a shift change. Grinding teams that tune rotor speed against actual Blaine, residue, and power data instead of habit routinely give back 3 to 5% of mill specific power without touching a single mechanical component. Book a demo to see how Oxmaint tracks rotor RPM against Blaine, residue, and kWh/t for every cement type you grind.
Cement classifier rotor speed software is a CMMS-based system that logs rotor RPM setpoints against Blaine, residue, circulating load, and specific power for every cement type ground, then flags when a setpoint drifts from its proven operating window. Because rotor speed directly sets the cut size in a dynamic separator, tracking RPM against actual lab and power data lets operators hold target fineness at the lowest possible kWh/t instead of running every product at the same conservative setpoint.
Why Rotor Speed Deserves Its Own Tracking Discipline
Rotor speed is not a maintenance parameter in the traditional sense. It does not wear out on a schedule and it will not trigger an alarm when it is wrong. It sits on an inverter, gets set once during commissioning, and then drifts by operator habit rather than by data. That makes it the most under-managed variable in the entire grinding circuit, even though it has more direct influence over product fineness than almost any other control point.
Rotor RPM sets the centrifugal force acting on particles inside the cage. Higher RPM rejects more coarse material back to the mill, lowering d50 cut size and raising Blaine. Every classifier has a distinct RPM-to-Blaine curve that shifts with wear, air volume, and feed rate.
A finer cut demands more recirculation through the mill. Running rotor speed higher than the product actually requires adds kWh per tonne with no strength benefit, since cement beyond its target Blaine gains little additional 28-day strength.
Higher RPM increases the reject fraction sent back to the mill inlet, raising circulating load. Above a certain point the mill floods, table pressure drops, and throughput falls even though the classifier is doing exactly what it was told to do.
45-micron residue tracks closely with rotor RPM once air volume is fixed. Cement type changeovers that do not adjust rotor speed either over-grind low-strength products or under-grind high-early-strength orders and fail lab residue targets.
See Your RPM-to-Blaine Curve Built From Your Own Mill Data
Oxmaint plots rotor speed against Blaine, residue, and specific power for every cement type your plant grinds, then locks in the setpoint that hits spec at the lowest kWh/t.
Why RPM Tuning Fails Without Structured Tracking
Rotor RPM for each cement type is passed down by word of mouth across shifts. When an experienced operator leaves, the plant reverts to one conservative setpoint for every product, quietly raising specific power on every low-Blaine order.
Blaine and residue results sit in the QC system while rotor speed sits on the DCS trend. Without a link between the two, nobody can tell whether a failed residue result came from RPM drift, feed rate change, or worn classifier vanes.
Mill specific power reports roll up daily or monthly, long after a rotor speed change. A 12 RPM overshoot that adds 2.6 kWh/t for three weeks disappears into the noise of feed rate and grindability variation before anyone notices.
As classifier vanes wear, the same RPM setpoint produces a coarser cut over time. Plants that never log vane condition against RPM performance keep running an outdated setpoint that no longer matches the current mechanical state.
How Oxmaint Manages Classifier Rotor Speed
Every cement type gets a recorded rotor speed range built from actual production data rather than a single OEM default. OPC, PPC, PSC, slag cement, and low-heat orders each carry their own proven RPM window, feed rate, and air volume combination.
Rotor speed readings from the inverter, Blaine and residue results from the lab, and specific power from the mill motor feed into one record per production run. Oxmaint calculates the actual kWh/t cost of every RPM point above the minimum required setpoint.
When rotor speed runs outside its recorded window for the current cement type for longer than a configured period, an alert routes to the shift supervisor with the current Blaine trend and estimated power penalty attached.
Classifier vane and cage inspections are scheduled against actual RPM-to-Blaine curve flattening rather than a fixed calendar interval, so recalibration happens when the classifier genuinely needs it. Book a demo to see setpoint tracking configured for your mill.
Rotor RPM Windows by Cement Type
- Rotor Speed Range53 to 58 RPM
- Target Blaine3,200 to 3,500 cm2/g
- Residue at 45 microns10 to 14%
- Specific Power ImpactBaseline reference
- Rotor Speed Range58 to 63 RPM
- Target Blaine3,600 to 3,900 cm2/g
- Residue at 45 microns6 to 9%
- Specific Power ImpactPlus 1.4 to 1.9 kWh/t vs OPC
- Rotor Speed Range62 to 65 RPM
- Target Blaine3,900 to 4,300 cm2/g
- Residue at 45 microns4 to 6%
- Specific Power ImpactPlus 2.4 to 2.8 kWh/t vs OPC
- Rotor Speed Range50 to 54 RPM
- Target Blaine2,800 to 3,100 cm2/g
- Residue at 45 microns14 to 18%
- Specific Power ImpactMinus 1.1 to 1.6 kWh/t vs OPC
From Lab Result to RPM Adjustment
Operator confirms the cement type, and the classifier loads its proven rotor speed window and target Blaine range for that product.
Blaine and residue from the on-line or physical lab test attach automatically to the current RPM reading and feed rate for that hour.
Oxmaint compares the result against the target window. Off-spec results trigger a suggested RPM correction with the estimated power cost.
The operator applies or overrides the correction. Either way, the outcome is logged, sharpening the RPM-to-Blaine curve for that cement type.
Stop Running Every Cement Type at the Same Rotor Speed
Get a setpoint library, drift alerts, and specific power reporting for every classifier in the plant, live in under three weeks.
Structured RPM Tracking vs Operator Memory
| Metric | CMMS-Tracked RPM Program | Operator Memory / No Tracking |
|---|---|---|
| Setpoint Consistency Across Shifts | Same recorded RPM window every shift, every operator | Varies by whoever is running the panel that day |
| Specific Power Excess | 0.3 to 0.6 kWh/t above minimum required setpoint | 2 to 4 kWh/t above minimum on blended and low-heat orders |
| Residue Failures per Month | 1 to 2 across all cement types | 6 to 12, concentrated at changeovers |
| Time to Detect RPM Drift | Under 2 hours via automated alert | Discovered at next lab result or monthly power review |
| Vane Wear Visibility | Tracked against RPM-to-Blaine curve flattening | Only noticed once residue fails consistently |
What the Platform Tracks
A recorded rotor speed range per cement type, built from real production runs rather than the single default written in the OEM manual.
A live plot of rotor speed against Blaine and residue for each classifier, updated with every lab result so the curve reflects current vane condition.
Every kWh/t above the minimum required setpoint is calculated and attributed to the RPM decision that caused it, by shift and by cement type.
Automatic notification when rotor speed runs outside its proven window for the current order, before it turns into a residue failure or a power spike.
Classifier internals are inspected against curve flattening rather than a fixed calendar, catching wear before setpoints stop matching reality.
Every cement type changeover pulls its recorded RPM, feed rate, and air volume automatically, removing the guesswork from the first hour of a new order.
Where Most Plants Stand Today
Outcomes After Oxmaint Deployment
Investment vs Return
| Component | Cost | Annual Savings | Payback |
|---|---|---|---|
| RPM-to-Blaine Curve Setup | $9K one-time configuration | $140K from power excess reduction | Under 3 weeks |
| Drift Alert Monitoring | $11K per year platform cost | $95K from fewer residue failures and reworks | Under 5 weeks |
| Vane Wear Scheduling | $5K per year | $60K from extended vane and cage life | Under 6 weeks |
| Full Rotor Speed Program | $25K per year | $295K+ combined avoidance | Under 4 weeks |
Frequently Asked Questions
Every 12 RPM Costs 2.6 kWh/t. Know Which 12 RPM You're Paying For.
RPM-to-Blaine curves, drift alerts, specific power attribution, and vane wear scheduling built from your own mill data. Live in under three weeks.