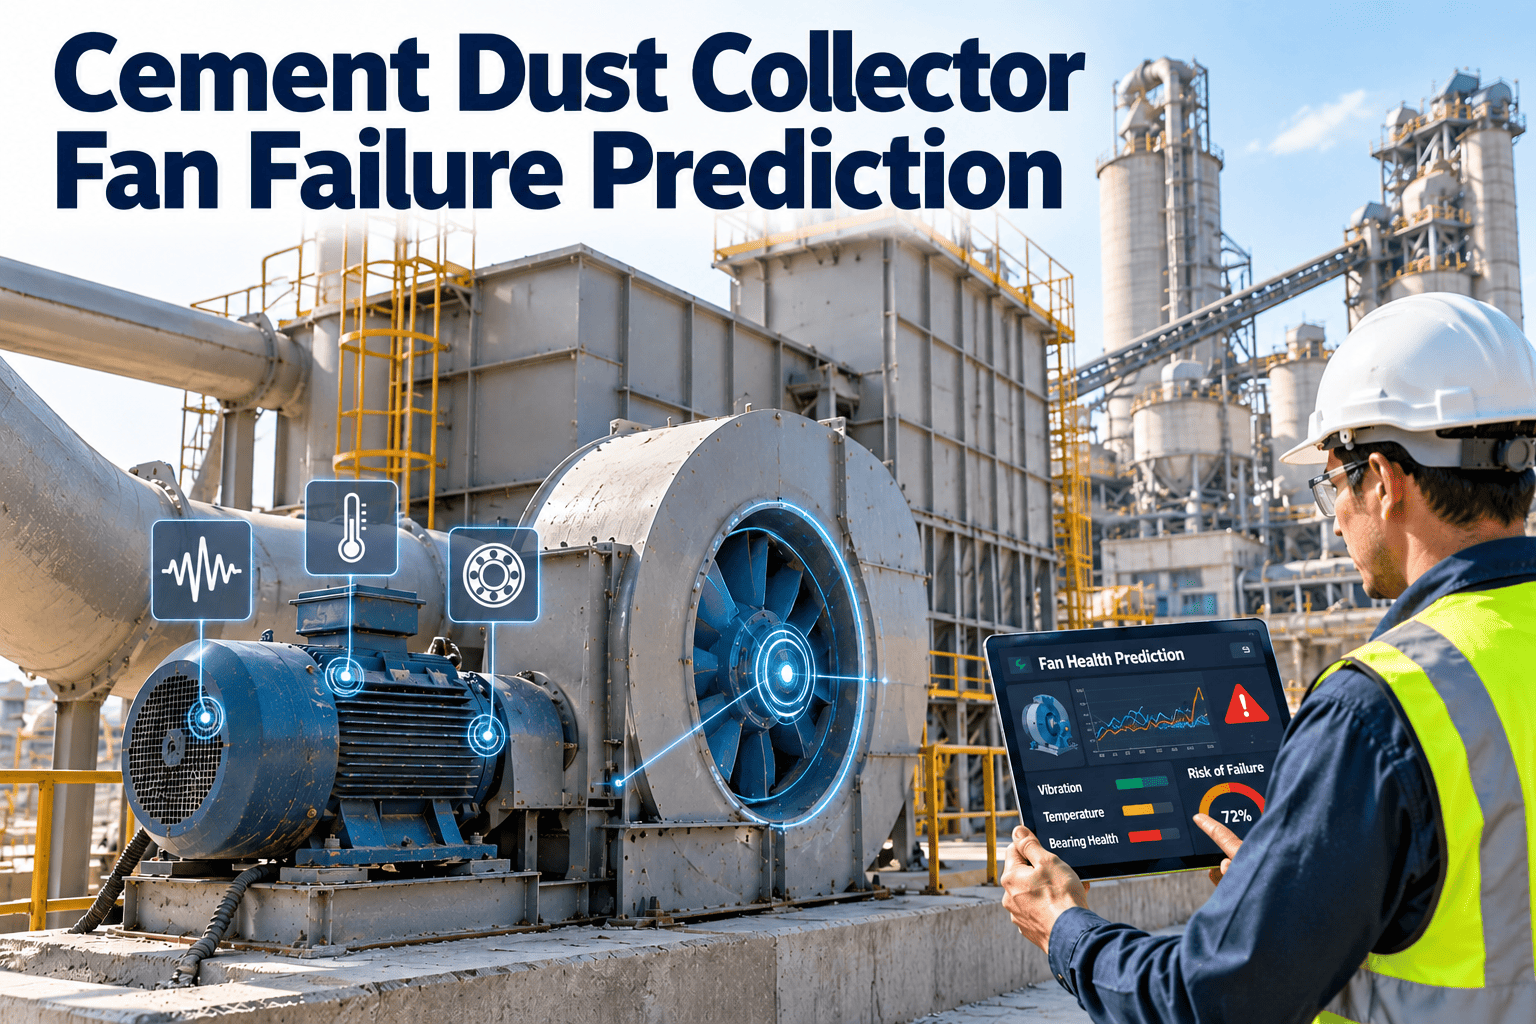
The fan behind a cement dust collector rarely fails without warning, but the warning is easy to miss. Dust builds on impeller blades, bearings warm up slowly and vibration creeps upward over weeks while operators focus on kiln and mill alarms. When the fan finally trips, the process stops or runs with uncontrolled emissions. Predicting failure means turning those small signals into scheduled actions, and a CMMS with inspection and condition workflows gives teams a place to record readings and act on them.
Cement Dust Collector Fan Failure Prediction
Spot imbalance, bearing wear and airflow loss early enough to plan the repair instead of reacting to a trip.
Normal readings
Trend rising
Alert and inspect
Plan repair window
What actually fails on a dust collector fan
| Failure mode | Typical early signal | Plant-level consequence |
|---|---|---|
| Impeller dust buildup and imbalance | Rising vibration at running speed | Bearing damage, structural stress |
| Blade erosion | Falling airflow, changing vibration pattern | Reduced capture at transfer points |
| Bearing wear or poor lubrication | High-frequency vibration, rising temperature | Seizure and unplanned stop |
| Misalignment or loose mounting | Vibration at multiples of running speed | Coupling and seal damage |
| Belt or coupling wear | Noise, speed loss, belt dust | Reduced flow, sudden drive failure |
| Motor winding or drive issues | Current imbalance, motor heating | Trips and restart cycles |
The warning window between first signal and failure
Stage 1
Fault starts. Only trained analysis or trending shows it.
Stage 2
Condition readings clearly deviate. This is the planning window.
Stage 3
Heat, noise or smell appear. Time to act is short.
Stage 4
Functional failure. Fan stops or performs poorly.
The goal is to find faults in stage 2, when parts, people and a stop window can be arranged.
Signals worth capturing for each fan
Vibration
Overall velocity at both bearings, plus spectrum checks where analysts are available. Compare against manufacturer limits and ISO guidance for the machine class.
Temperature
Bearing and motor temperature trends show lubrication and load problems before alarms trip.
Electrical
Motor current and drive data indicate load changes, blocked ducts and impeller condition.
Process
Duct pressure, damper position and baghouse differential pressure help separate fan faults from filter faults.
Turn fan readings into scheduled work
Record inspection results and trigger work orders when trends cross your limits.
Reactive versus predictive fan maintenance
Reactive
- Repair after trip or visible damage
- Spare bearings ordered at failure
- Cleaning when airflow is already poor
- Emissions risk during unplanned stops
Predictive
- Repair planned from trended readings
- Spares reserved before the stop
- Impeller cleaning scheduled by vibration and current
- Fewer surprise stops on dust-critical lines
A prediction workflow in six steps
1
Rank dust collector fans by process and emissions criticality.
2
Set baseline readings after a healthy overhaul or alignment.
3
Define alert limits per signal, with owners for each response.
4
Collect readings on routes or from installed sensors.
5
Raise work orders when limits are crossed, with job plans attached.
6
Record findings and adjust limits after each repair.
Fan duty in dusty cement service
Dirty-side fans
Fans handling dust-laden gas face erosion and buildup on the impeller, so balance and wall thickness change over time.
Clean-side fans
Fans after the filter see less abrasion but still suffer from bearing wear, belt problems and motor issues.
Variable speed drives
Speed changes can move the fan through resonance ranges, so vibration limits should be checked at the speeds actually used.
Dampers and ducts
Stuck dampers and duct blockages change airflow and load, which can look like fan faults in current and pressure data.
Lubrication, belts and couplings
Common lubrication problems
- Over-greasing that raises bearing temperature
- Wrong grease type or mixed greases
- Missed intervals on remote bearings
- Contamination from dust entering seals
Practical controls
- Define grease type, quantity and interval per bearing
- Record each lubrication task in the asset history
- Inspect belts for tension, wear and alignment
- Check coupling guards, elements and fasteners at routine stops
Responding when a reading crosses its limit
| Reading | First response | Follow-up work |
|---|---|---|
| Vibration trending up at running speed | Inspect impeller for buildup and check mounting | Clean and balance at the next stop window |
| Bearing temperature rising | Check lubrication and cooling, compare both bearings | Replace bearing if trend continues |
| Motor current falling | Check dampers, belts and impeller condition | Repair drive or clear restriction |
| Motor current rising | Check duct blockage and baghouse pressure | Clean ducts or filters, then recheck fan |
| Unusual noise or smell | Inspect immediately, following site safety rules | Raise a priority work order |
Alert limits should come from manufacturer data, applicable standards and your own baseline history, not from generic numbers.
Planned balancing and repair in four steps
1
Prepare job plan, isolation, access and parts before the stop starts.
2
Clean the impeller, inspect for erosion and cracks, and measure wear.
3
Balance, align and torque fasteners, then record all values.
4
Restart, take new baseline readings and update alert limits.
A 90-day plan to start fan condition tracking
- Days 1 to 20: list all dust collector fans, rank them, and capture nameplate and drive details.
- Days 21 to 45: take baseline vibration, temperature and current readings and set review intervals.
- Days 46 to 70: run the routes, record every reading and open work orders when limits are crossed.
- Days 71 to 90: review repeat faults, adjust limits and plan spares for the highest-risk fans.
Choosing the right condition monitoring method
| Method | Best for | Limitation |
|---|---|---|
| Route-based portable vibration | Low-cost trending on many fans | Only catches what happens on the route day |
| Permanent vibration sensors | Critical fans with fast-moving faults | Higher cost, needs alarm management |
| Thermography | Bearings, motors, electrical connections | Needs consistent conditions and access |
| Motor current and drive data | Load changes, blockage and impeller condition | Does not locate mechanical faults precisely |
| Lubrication and grease inspection | Bearing condition and contamination | Depends on sampling quality |
| Operator inspection | Noise, leaks, dust buildup, guards | Subjective unless checklists are used |
How to rank fans before spending on monitoring
Criticality questions
- Does a stop force the process line to stop?
- Would emissions or dust exposure rise during an outage?
- Is there a spare fan or standby drive?
- How long would a repair or replacement take?
What the ranking decides
- Which fans receive permanent sensors or frequent routes
- Which fans keep critical spares on site
- Which fans justify planned overhauls
- Which can run to failure with minimal risk
Controlling impeller buildup and erosion
Buildup causes
Moisture, sticky dust and low gas temperature can bind material to blades, which gradually unbalances the rotor.
Erosion causes
High dust loading after bag failures can wear blades and casing, so filter faults often become fan faults.
Inspection practice
Use inspection doors at planned stops, measure blade thickness and photograph findings for comparison next time.
Repair options
Cleaning, wear plates, hardfacing or replacement can be planned once wear trends are recorded against the asset.
Avoiding false alarms
- Check whether a vibration rise follows a known process change such as a new speed set point or damper position.
- Confirm sensor mounting and cable condition before assuming the machine has changed.
- Compare both bearings and both directions, because a real fault rarely appears in only one reading.
- Require a second confirmation, such as temperature or current, before opening a high-priority job.
- Record every false alarm and its cause so limits and sensors can be improved.
Spares and lead times for fan repairs
| Item | Planning consideration |
|---|---|
| Bearings and housings | Keep matched sets for critical fans, because they fail more often than other parts |
| Spare or reconditioned impeller | Long lead time, so decide early whether to hold one for the most critical fans |
| Belts, couplings and guards | Low cost and easy to stock, so avoid delays caused by missing small parts |
| Motor and drive components | Check whether motors are interchangeable across similar fans |
| Seals and shaft sleeves | Dust ingress shortens bearing life, so include seals in every repair kit |
Fan KPIs worth tracking each month
Unplanned stops per fan
Share of alerts that led to confirmed faults
Time from alert to inspection
Planned versus reactive fan work
Repeat bearing failures
Reading fan data together with baghouse data
Pattern points to the filter
- Differential pressure rises while fan vibration stays steady
- Motor current falls as airflow drops
- Dust capture complaints rise at transfer points
Pattern points to the fan
- Vibration or bearing temperature rises with steady filter pressure
- Motor current changes without any change in duct conditions
- Noise changes or drive components show visible wear
Electrical and drive checks that belong on the route
- Motor terminal box condition, cable entries and visible heating at connections.
- Drive cooling, filters and alarm history for variable speed units.
- Motor current balance across phases and comparison with the baseline.
- Earthing and shaft grounding condition where bearing currents are a known risk.
- Overload and trip settings, recorded and compared after any drive change.
Operator rounds that add real value
Look and listen
Note noise changes, visible dust leaks, loose guards and oil or grease leaks, and record them in a short checklist.
Compare with normal
Use baseline photos and readings so operators can judge whether a fan looks and sounds different from its healthy state.
Report quickly
Provide a simple way to raise a work request from the floor with the asset already identified.
Close the loop
Tell operators what was found, which builds trust and improves the quality of later reports.
Repair or replace: deciding at the overhaul
Signs a repair is enough
- Wear is localized and measurements are inside manufacturer limits
- No cracks in welds, hub or shaft
- Failure came from lubrication or alignment, not material fatigue
- Balance can be restored and held
Signs replacement needs discussion
- Repeated repairs on the same component
- Wear beyond the repairable limit or cracking found
- Rising maintenance cost with falling reliability
- A better-suited blade or material option exists
Documents to keep for each critical fan
- Datasheet, drawings, balancing reports and alignment records.
- Baseline vibration, temperature and current readings after each overhaul.
- Repair history with parts used, findings and photographs.
Skills and handover practices that keep predictions reliable
- Train technicians to take readings the same way every time, with the same points, direction and operating condition.
- Give analysts access to repair history, so each reading is interpreted with context instead of in isolation.
- Include fan status, open alerts and planned work in shift handover notes.
- Review a sample of closed alerts monthly to learn what was found and whether the response was timely.
- Share findings with operators so they know why a fan was stopped or cleaned.
How Oxmaint supports fan failure prediction
Asset records for each fan, motor, drive and bearing set
Mobile inspection routes for vibration, temperature and current
Condition-based work orders and preventive schedules
Spare parts inventory linked to repair jobs
Dashboards for repeat failures and downtime by fan
Frequently asked questions
What is the most common early sign of fan trouble?
Rising vibration at running speed often points to dust buildup or imbalance. Trend it against a healthy baseline.
Do we need online sensors to predict failure?
Not always. Regular route-based readings recorded consistently can reveal trends for many fans.
How do we tell a fan fault from a filter fault?
Compare fan vibration and current with baghouse differential pressure and damper position.
Can a CMMS trigger work from readings?
Yes, through inspection thresholds and condition workflows. You can book a demo to see an example.
Where should we begin?
Start with the three most critical fans and get started with baseline readings.
Plan the repair before the fan decides for you
Give your team trended readings, clear limits and work orders that act on them.