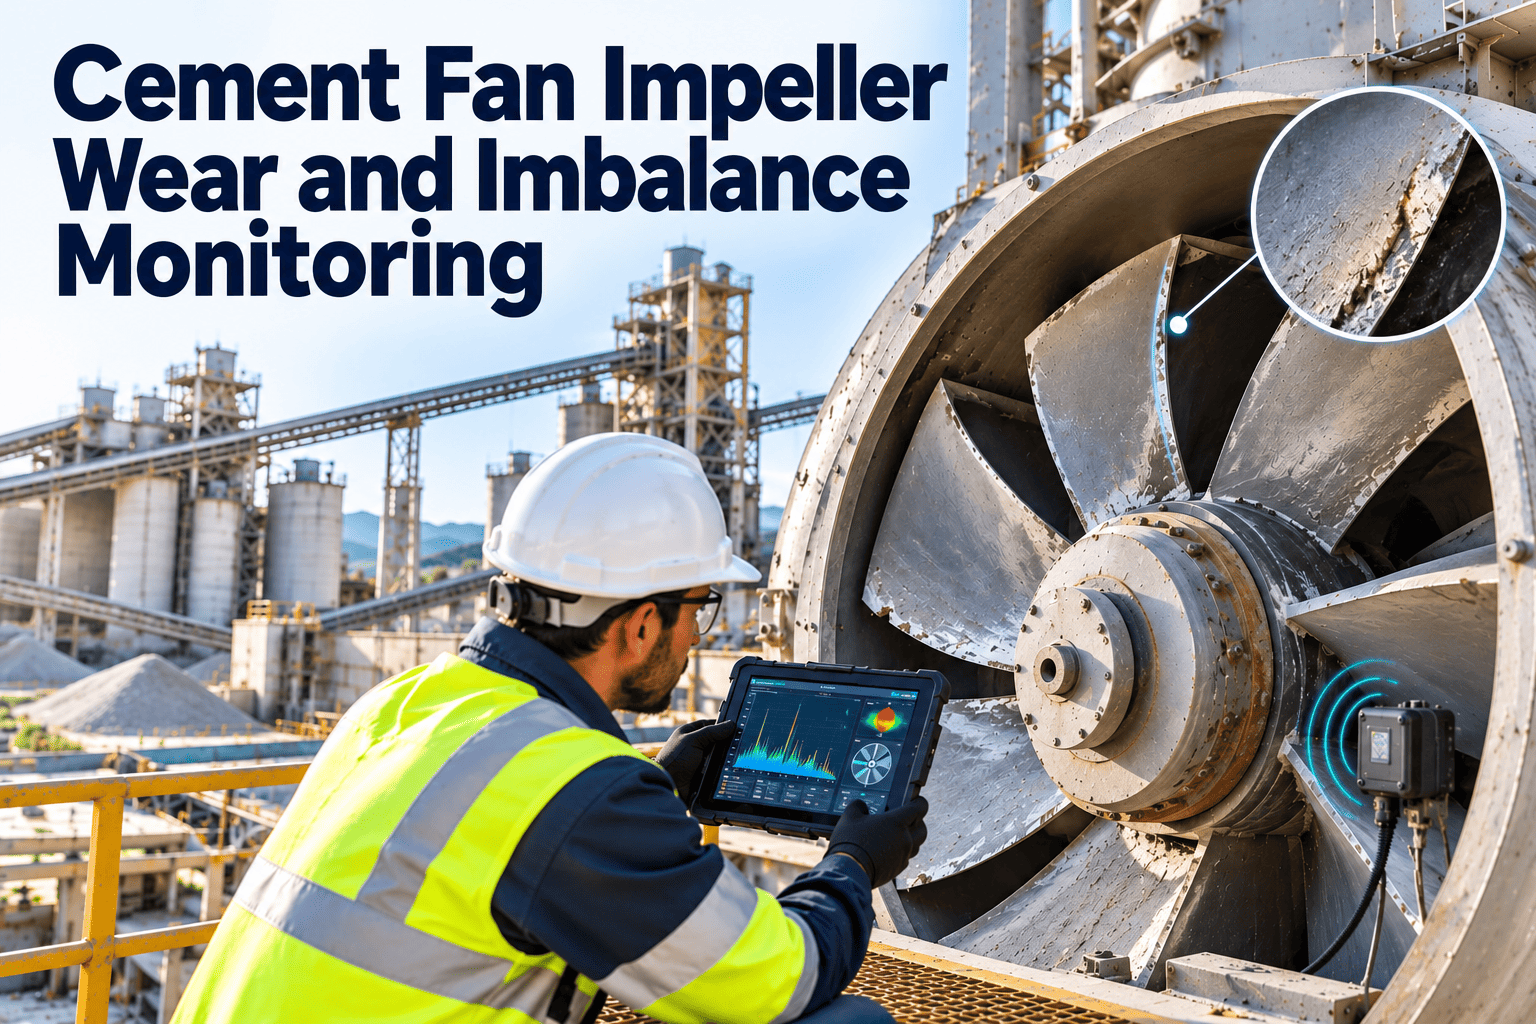
Cement fans move the gas that keeps a kiln line running. Kiln ID fans, raw mill fans, cooler vent fans, separator fans, and baghouse fans all work in abrasive, dust-laden gas. Over months, that dust erodes impeller blades unevenly, mass shifts, and vibration climbs. The same wear also cuts efficiency, so power draw rises while airflow quietly falls. This guide shows how to detect wear and imbalance early, set practical alarm limits, and convert readings into planned work using a cement plant maintenance management system.
Catch Impeller Wear and Imbalance Before the Fan Limits Your Kiln
A single worn impeller can force operators to open dampers, raise speed, and burn extra kilowatts for the same gas flow. Track wear, vibration, and power in one maintenance record and act while repairs are still planned.
Typical impeller degradation path: relative 1X vibration trend
Stage 1: HealthyBaseline
Stage 2: Surface erosionWatch
Stage 3: Uneven mass lossPlan repair
Stage 4: Cracks or buildup shedAct now
The Problem
Why Fan Degradation Stays Hidden Until It Becomes Expensive
Fans rarely fail suddenly. They drift, and the drift is easy to misread as a process issue.
What the control room sees
- Damper position creeping open over weeks
- Motor current rising for the same draft
- Higher fan speed needed to hold kiln pressure
- Occasional vibration alarms that clear after a process change
What is actually happening
- Blade leading edges and wear plates thin unevenly
- Dust buildup grows on some blades and sheds from others
- Rotor mass distribution shifts away from the balanced condition
- Bearings carry rising dynamic load and run hotter
Because airflow loss is gradual, plants often compensate with speed or damper changes instead of inspecting the rotor. That hides the cause and raises energy cost every shift.
Failure Chain
From Abrasive Gas to Unplanned Fan Stop
Each link in this chain gives a measurable signal. Missing the early links is what turns a planned repair into a kiln stop.
1Abrasive dust in gas streamSignal: dust loading, gas velocity
2Blade and liner erosionSignal: thickness readings
3Uneven mass loss or buildupSignal: 1X vibration and phase
4Bearing and foundation stressSignal: bearing temperature
5Efficiency loss and trip riskSignal: kW per unit airflow
Where to Look
Wear Mechanisms by Cement Fan Type
Different fans wear differently, so monitoring depth should follow service conditions and criticality.
| Fan | Main wear or imbalance driver | Early symptom | Priority check |
|---|---|---|---|
| Kiln ID fan | Dust erosion plus temperature and chemical effects | Rising speed for same draft | Online vibration, blade thickness, bearing temperature |
| Raw mill fan | Fine abrasive raw meal and buildup | Vibration swings with mill load | Route vibration, buildup inspection |
| Cooler vent fans | Clinker dust and hot air exposure | Reduced undergrate airflow | Power trend, impeller condition |
| Separator and mill fans | Fine cement dust and coating | Fluctuating airflow | Vibration and amperage trend |
| Baghouse and bypass fans | Sticky or abrasive dust, moisture | Gradual differential pressure change | Impeller cleaning and wear check |
Diagnosis
Reading Vibration to Separate Imbalance From Other Faults
Imbalance is the most common reason for rising fan vibration, but it is not the only one. Confirm before you balance.
| Fault | Typical vibration pattern | Confirming clue |
|---|---|---|
| Imbalance | Dominant 1X running speed, mostly radial | Stable phase, amplitude changes with speed |
| Misalignment | 1X and 2X, often high axial | Phase difference across coupling |
| Looseness | Multiple harmonics, unstable readings | Soft foot or loose bolts found |
| Bearing defect | Bearing frequencies, rising high-frequency energy | Temperature and envelope trend up |
| Aerodynamic issue | Blade pass frequency, number of blades times speed | Changes with damper or flow |
Phase readings matter. A changing 1X amplitude with a shifting phase angle often points to buildup breaking away or a blade losing material, which a single overall vibration value cannot show.
Reference standards commonly used by plants include ISO 20816 for machine vibration severity and ISO 14694 for industrial fan balance and vibration. Always check the fan manufacturer's limits for your machine.
Energy Impact
How Wear Turns Into Energy Waste
Fan power rises roughly with the cube of speed, so small speed increases to compensate for lost performance carry a large energy penalty.
Worn or imbalanced impeller
- Rougher blade surfaces and changed profile reduce efficiency
- Larger clearances increase internal leakage
- Operators open dampers or raise speed to hold flow
- Higher vibration shortens bearing and seal life
Monitored and restored impeller
- Wear repaired on a planned shutdown window
- Balance restored to the specified quality grade
- Speed and damper settings return toward design duty
- Bearings see lower dynamic load and run cooler
Tracking kilowatts against airflow or kiln draft over time gives a simple efficiency indicator. A rising trend with no process change is a strong reason to inspect the rotor.
Root Causes
Why Impellers Wear Faster Than Expected
Wear rate is rarely random. These causes explain most cases of premature impeller wear and repeat imbalance in cement plants, and each one can be logged and trended against fan readings.
A
Gas velocity above design
Higher velocity raises particle impact energy, so blades erode faster. Check whether process changes or false air increased velocity.
B
Dust load and particle size
Weak upstream collection or cyclone performance sends more abrasive dust to the fan, accelerating leading edge wear.
C
Fuel and raw material changes
Shifts in ash, chloride, or alkali content can change deposit formation on kiln line fans. Log fuel mix changes next to vibration trends.
D
Moisture and condensation
Wet dust sticks to blades, forms uneven buildup, and promotes corrosion under the coating.
E
Operation away from design point
Heavily throttled dampers create turbulence and uneven blade loading, which adds fatigue to wear.
F
Repair quality
Poor weld repair or a missing post-repair balance brings imbalance back within weeks and hides the true wear rate.
Balancing Practice
Field Balancing That Actually Holds
Balancing is only worthwhile when the rotor is sound and the diagnosis is correct. Follow a repeatable sequence so results can be compared from outage to outage.
Step 1
Confirm the fault
Verify imbalance using phase and speed response. Rule out looseness, misalignment, and resonance, then record the baseline reading.
Step 2
Clean and inspect
Remove buildup and inspect welds and blade roots. A cracked rotor must be repaired or replaced, never balanced around.
Step 3
Run trial weights
Fit a trial weight, measure the change in amplitude and phase, and calculate the correction. Attach final weights using approved methods.
Step 4
Verify and record
Check vibration at operating speed, note gas temperature and damper position, and save residual values in the asset history.
Hot fans can read differently from cold ones because of thermal growth and deposit changes. Record operating conditions with every balance so later readings are comparable.
Records
What to Record for Reliability Review and Audits
Without operating context, a vibration number is hard to interpret. Damper position, speed, and gas temperature explain many apparent changes and prevent unnecessary repairs.
With every reading
- Date, technician, and instrument used
- Fan speed, load, and damper position
- Gas and bearing temperature
- Probe location, direction, amplitude, and phase
With every repair
- Findings, photos, and thickness measurements
- Parts used and welding procedure reference
- Balance weights and residual vibration
- Follow-up actions and next inspection date
See Fan Health Trends Next to Every Work Order
Keep vibration readings, inspection findings, and repair history on the same asset record so fan decisions rest on data instead of memory.
Monitoring Program
A Three-Tier Approach to Fan Monitoring
Not every fan needs a permanent sensor. Match the method to the consequence of failure.
Tier 1
Online monitoring for critical fans
Permanent vibration sensors and bearing temperature on kiln ID fans and other fans whose stop halts clinker production.
Continuous with alarm limits
Tier 2
Route-based vibration and thermal checks
Handheld vibration readings and infrared checks on raw mill, cooler, and separator fans, logged on a fixed route.
Weekly to monthly by criticality
Tier 3
Operator rounds and shutdown inspection
Visual checks for noise, buildup, and casing leaks on smaller fans, with full impeller inspection at planned stops.
Each shift and each shutdown
Alarm Strategy
Building an Alert Ladder That Operators Trust
Too many nuisance alarms teach crews to ignore them. Tie each level to a defined response.
Level 1: Baseline deviationAdd the fan to next route review and compare with last shutdown readings
Level 2: Sustained upward trendRaise an inspection work order and shorten the reading interval
Level 3: Alert limit exceededPlan balancing or repair and confirm spare impeller and bearing availability
Level 4: Trip or danger limitFollow the operating procedure, reduce load, and prepare an immediate corrective work order
Set limits from the manufacturer's data, the applicable standard, and your own baseline after a good balance. Review them after each repair.
Repair Decisions
Choosing the Right Corrective Action
The best repair depends on how much material is lost and whether the rotor has cracked.
| Condition found | Typical action | Planning note |
|---|---|---|
| Dust buildup only | Clean and re-check vibration | Investigate why buildup is occurring |
| Light, even erosion | Field balance and continue monitoring | Record wear rate for life prediction |
| Localized blade wear | Hardfacing or wear plate repair, then balance | Allow time for welding and stress control |
| Cracks or severe thinning | Replace impeller or blades | Needs spare impeller, rigging, and crane booking |
Cracks in welds or blade roots should never be treated as a balance problem. Replace or repair them under qualified supervision and confirm with a post-repair vibration check.
Maintenance Workflow
How Oxmaint Connects Fan Monitoring to Work
Condition data only saves money when it triggers the right job at the right time. Oxmaint can help structure that workflow for cement fans.
01
Asset records for every fan
Store impeller type, bearing data, motor details, and drawings against each fan in the asset hierarchy.
02
Mobile inspections and readings
Technicians record vibration, temperature, and visual findings on a phone or tablet along a defined route.
03
Preventive and condition-based schedules
Combine calendar tasks with condition triggers so inspections tighten when trends worsen.
04
Work orders with history
Raise corrective work orders from findings, attach photos, and keep balancing results with the asset.
05
Spares and shutdown planning
Link impellers, bearings, and wear plates to inventory so parts are ready before the planned stop.
06
Dashboards and reports
Review overdue inspections, repeat fan faults, and repair cost by asset in one view.
Measure Results
KPIs That Show Whether Fan Monitoring Is Working
Pick a small set and review it monthly with maintenance and operations together.
Fan specific energy
kWh per unit of gas or product handled, trended against a post-repair baseline
Unplanned fan stops
Number and duration of stops traced to impeller, bearing, or vibration causes
Condition work found early
Share of fan repairs that began as an inspection or trend alert
Overdue fan inspections
Open route and shutdown tasks past due on critical fans
Impeller service life
Operating hours between replacement or major repair, by fan
Shutdown Checklist
Impeller Inspection Checklist for Planned Stops
Use the same checklist every outage so findings are comparable from year to year.
Rotor and casing
- Measure blade and wear plate thickness at set points
- Inspect blade roots and welds for cracks
- Photograph buildup patterns before cleaning
- Check casing liners and inlet cone clearance
Drive and support
- Check shaft runout and bearing fits
- Verify coupling alignment and foundation bolts
- Inspect seals and lubrication condition
- Record balance weights and final vibration
Technology Trends
Where Fan Condition Monitoring Is Heading
Cement plants are adding more measurement points and connecting them to maintenance systems, but the value still comes from acting on the data.
| Development | What it adds | Practical caution |
|---|---|---|
| Wireless vibration sensors | Lower-cost coverage of fans that were only checked by hand | Confirm mounting quality, battery plan, and sampling rate |
| Trend-based alerting | Warnings from rate of change, not only fixed limits | Needs a clean baseline after each repair |
| Power and flow correlation | Efficiency tracking next to vibration | Use consistent operating conditions for comparison |
| Automatic work order creation | Faster response when a limit is crossed | Define who reviews and approves each alert |
Start with your most critical fans, prove the workflow, then extend coverage. A small program that triggers real work beats a large one that nobody reviews.
FAQ
Cement Fan Monitoring Questions
How often should cement fan vibration be measured?
Critical fans suit continuous monitoring, while others are often read weekly or monthly. Shorten intervals when trends rise. Set up routes in Oxmaint.
Does high 1X vibration always mean imbalance?
No. Misalignment, looseness, and resonance can also raise 1X. Check phase, direction, and speed response before balancing.
Can impeller wear be tracked without sensors?
Yes. Thickness readings, buildup photos, and power trends logged each outage still show wear rate. Book a demo to see the inspection forms.
Why does fan power rise as the impeller wears?
Efficiency drops, so operators raise speed or open dampers to hold flow, and power climbs steeply with speed.
What should a fan work order include?
Include readings, photos, findings, parts used, and post-repair vibration so future decisions have history. Get started with a template.
Turn Fan Readings Into Planned Repairs, Not Surprise Stops
Bring impeller inspections, vibration trends, spares, and work orders into one maintenance system for your cement plant.