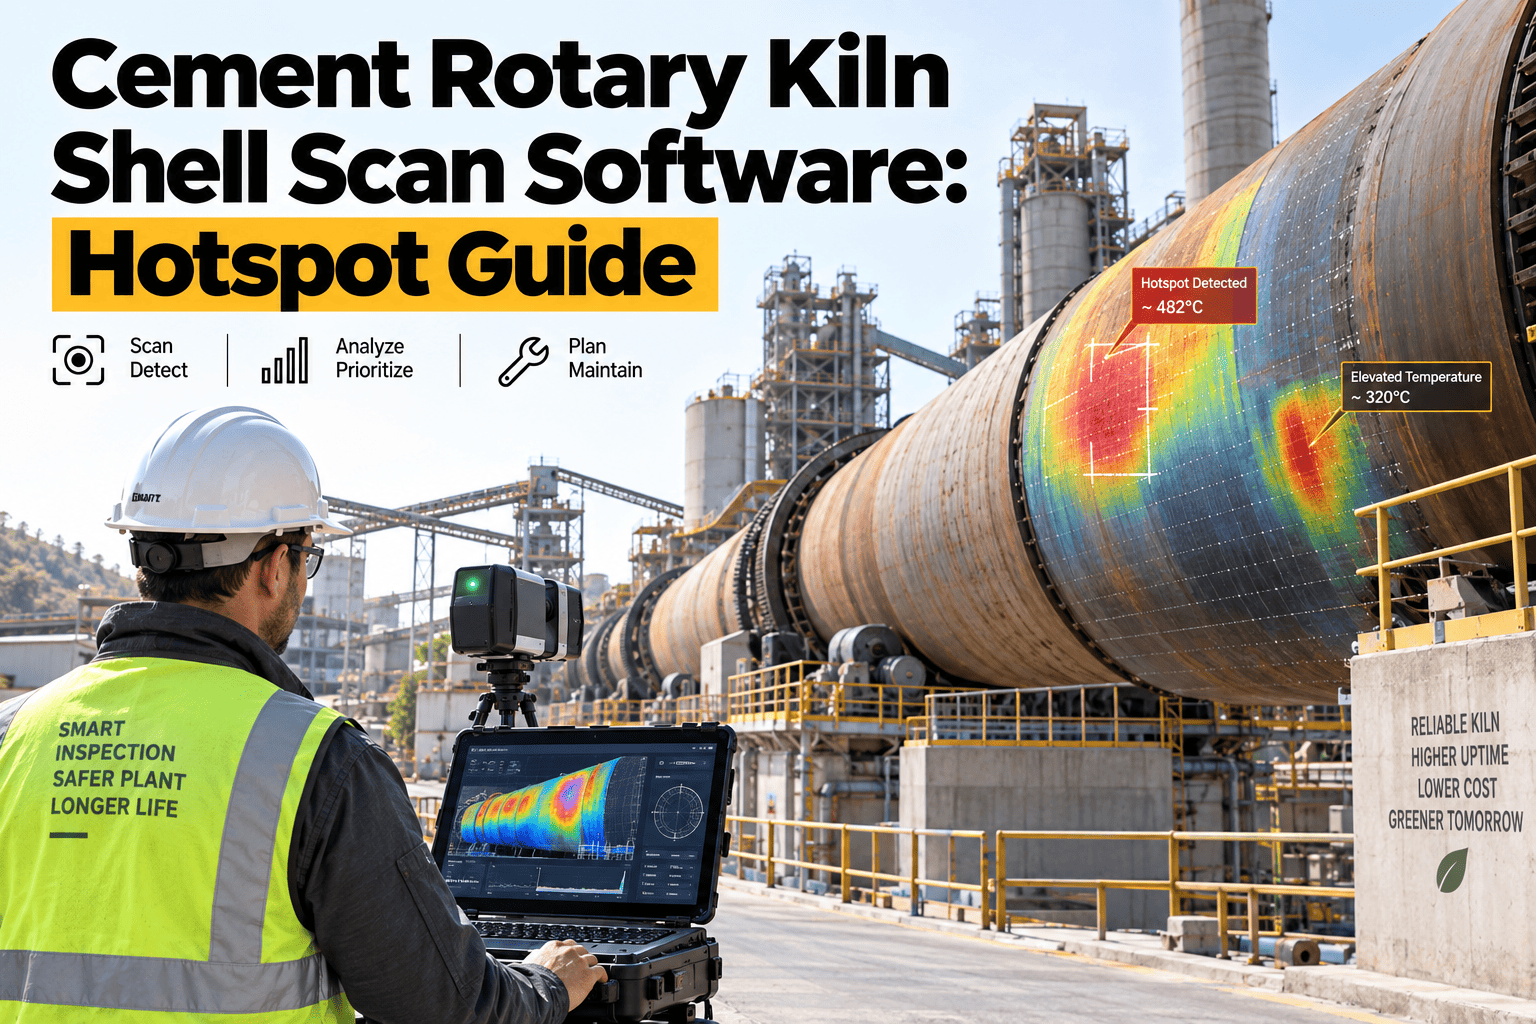
A cement kiln hot spot rarely announces itself politely — one shell scan reads 180°C, the next reads 310°C, and now the reliability engineer on shift has minutes, not days, to decide whether this is a scheduled patch or an emergency shutdown. Hot spots form when refractory brick thins, cracks, or falls away, exposing bare steel shell to burning-zone process temperatures that can push past 380°C within 48 to 72 hours if the response is slow or undocumented. The gap between a routine gunning repair and a 45-day forced outage that permanently warps the shell almost always comes down to how fast the protocol fires and how well each step is logged. This guide breaks down the first-30-minutes decision tree, the cooling rules that prevent thermal shock, and the patch-repair sequence that turns a red-alert hot spot into a scheduled stop instead of a catastrophe. See how Oxmaint coordinates that entire response from alarm to closed work order.
EMERGENCY RESPONSE GUIDE · CEMENT KILN HOT SPOTS
Your shell scanner just flagged 340°C. What happens in the next 30 minutes decides everything.
A hot spot left unmanaged can climb from a warning reading to a critical shell temperature in under three days. Handled correctly, the same hot spot becomes a two-hour gunning repair and a note in the maintenance log. This guide is the difference between the two outcomes.
THE FIRST 30 MINUTES
Four decisions that happen before anyone picks up a gunning lance
A hot spot alarm is not a repair instruction — it is the start of a triage sequence. Skipping any of these four steps is how a manageable patch turns into an unplanned reline. Work through them in order, every time, regardless of shift or plant.
Confirm the reading is real
Rule out a sensor fault, sun glare on a fixed IR array, or dust coating throwing off emissivity before treating the number as truth. Cross-check against a handheld pyrometer reading at the same rotation angle.
Locate the exact zone
Burning zone, transition zone, or inlet — each has a different critical threshold. A burning zone reading above roughly 340°C, a transition zone reading above 300°C, or an inlet reading above 250°C all point to a spall depth of 80mm or more.
Check the rate of rise, not just the reading
A steady 320°C is a different problem than a spot that jumped 60°C in four hours. Rate of climb tells you whether coating simply shed or whether brick is actively falling away — and how much time is actually left.
Decide: monitor, patch, or shut down
Any confirmed hot spot needs a 24-hour recheck scan at minimum. If the reading persists past 48 hours, plan a shutdown window within 72 hours for inspection and repair — do not let it run to failure on hope.
COOLING PROTOCOL
The cooling mistake that turns a hot spot into a shell deformation
Cooling buys time until a proper patch can be applied — but the wrong cooling method adds thermal shock on top of an already-stressed shell. Get this wrong and you can warp the very steel you were trying to protect.
RIGHT APPROACH
Localized, punctual water cooling
Direct a controlled water spray or targeted air jet only at the hot zone, not the full circumference. Localized cooling reduces the mechanical tension in that one segment without shrinking the entire shell ring around it.
AVOID
Full-circumference blower cooling
Running a blower across the entire shell cools the healthy sections along with the hot spot, shrinking the whole segment and adding stress to refractory that was never damaged in the first place.
RIGHT APPROACH
Gradual, monitored cooling rate
Track shell temperature during cooling, not just before and after. A controlled drop keeps expansion and contraction inside a range the steel can absorb without permanent set.
AVOID
Aggressive rapid quenching
Dumping maximum water flow onto a glowing hot spot feels decisive, but a too-fast cooling rate is one of the fastest ways to crack surrounding brick and lock in shell distortion.
Put the decision tree in the hands of whoever is on shift
A hot spot does not wait for the day-shift reliability engineer. Configure the escalation logic once and every shift responds the same way.
REPAIR METHOD SELECTION
Hot-gunning, cold patch, or plate reinforcement — which repair fits the situation
Not every hot spot needs the kiln stopped. Matching the repair method to the severity is what keeps a plant running clinker instead of running a 21-day outage.
| Repair Method | Kiln Status | Best For | Typical Downtime | Campaign Life Added |
|---|---|---|---|---|
| Hot-gunning patch | Running or brief stop | Localized brick loss, single hot spot | 2–8 hours | Bridges to next annual shutdown |
| Cold patch (cooled section) | Kiln stopped, section cooled | Wider spall area, multiple adjacent hot spots | 1–3 days | 6–12 months |
| Steel plate reinforcement | Kiln stopped, shell inspected | Early-stage shell deformation, ovality drift | 2–4 days | Structural, not refractory-driven |
| Zone reline | Planned annual shutdown | Recurring hot spots in same zone across cycles | 5–10 days | 8–10 years (full campaign) |
Hot-gunning with a magnesite or spinel-based refractory concrete is the standard stopgap: it lets the kiln keep running while stabilizing the damaged area until the next planned reline, rather than forcing an immediate cold shutdown for a single localized spot.
ESCALATION LADDER
From first alarm to closed work order — the 72-hour window
Every confirmed hot spot follows the same clock. Treat these windows as hard checkpoints, not loose guidelines — this is the sequence that keeps a hot spot from becoming a shell failure.
Confirm, locate, log
Verify the reading, identify the zone and rotation angle, and open a tracked incident record with the initial temperature, rate of rise, and shift lead sign-off.
Apply punctual cooling, rescan
Begin localized cooling if temperature exceeds the zone threshold. Run a mandatory 24-hour recheck scan to see whether the spot is stable, cooling, or still climbing.
Stage the gunning crew and materials
If the hot spot persists, pre-position refractory gunning material, lance equipment, and a repair crew so the repair window can open the moment conditions allow — no waiting on procurement mid-emergency.
Execute repair or plan the shutdown
Persisting past 48 hours means committing to a shutdown window within 72 hours for inspection and either a hot-gunning patch or a cooled cold-patch repair, depending on spall size.
Close the loop and trend the zone
Log repair method, material, and downtime against the asset record, then flag that zone for tighter scan frequency — a hot spot that recurs in the same location signals a coating or firing issue, not just a bad brick.
Stop running hot spot response from memory and a group chat
Every minute the escalation sits in someone's head instead of a system is a minute closer to a shell that cannot be un-warped.
CMMS COORDINATION
What a maintenance system actually needs to do during a hot spot event
A hot spot response touches operations, maintenance, safety, and sometimes a refractory contractor — all at the same time. The software layer either coordinates that or becomes another thing someone has to manage by hand.
Auto-escalating work orders
A confirmed hot spot above zone threshold should generate a work order automatically, with severity and required response time already attached — not wait for someone to remember to raise a ticket.
Zone-level asset history
Every kiln zone carries its own temperature trend, last reline date, and repair history, so a repeat hot spot in the transition zone is instantly visible as a pattern, not a surprise.
Repair crew and materials checklist
Digitize the gunning repair checklist — material batch, lance time, thickness applied, cooling rate logged — so nothing gets skipped under the pressure of an active incident.
Contractor and spares coordination
Track refractory material stock and preferred contractor contacts against the asset, so staging a gunning crew at hour 24 does not start with a phone tree.
Shift-to-shift handoff log
A hot spot that started on night shift needs the exact same response on day shift. A shared incident record with timestamps removes the guesswork from every handoff.
Post-incident audit trail
When the reading, the cooling method, the repair, and the sign-off are all timestamped in one record, closing out an emergency for insurance or corporate reporting takes minutes, not a week of reconstructing events.
"
We used to find out a hot spot had been sitting at 360°C for two shifts because nobody escalated it past the control room log. Now the moment a zone crosses threshold, a work order fires with the repair checklist attached and the on-call refractory contractor gets notified. Our last hot spot was a six-hour gunning patch instead of a shutdown.
FREQUENTLY ASKED
Cement kiln hot spot emergency response — straight answers
What shell temperature counts as a hot spot emergency?
A burning zone reading above roughly 340°C, a transition zone reading above 300°C, or an inlet reading above 250°C all indicate significant refractory spall and require immediate escalation and a 24-hour recheck scan.
Can a kiln keep running with an active hot spot?
Often yes, with localized cooling and a hot-gunning patch applied while running or during a brief stop. A hot spot that persists past 48 hours should not be left running — plan a shutdown window within 72 hours instead.
Why is full-circumference cooling risky?
Cooling the entire shell instead of just the hot zone shrinks the whole segment and adds mechanical stress to refractory that was not damaged, increasing the risk of new cracking rather than fixing the original spot.
How much does an emergency hot spot failure typically cost?
Industry figures put emergency refractory failures at $800,000 to $2.5 million in direct repair and expedited procurement costs, plus a 12- to 21-day forced outage. Book a Demo to see how faster escalation shrinks that window.
How does a CMMS actually speed up hot spot response?
By auto-generating a severity-tagged work order the moment a zone crosses threshold, attaching the repair checklist, and logging every step for handoff and audit. Start Free Trial to configure escalation thresholds for your kiln zones.
Turn the next hot spot alarm into a scheduled repair, not a crisis
Configure zone thresholds, auto-escalating work orders, and a repair checklist your whole shift rotation can follow — before the next alarm fires.
Free 14-day trial · No credit card