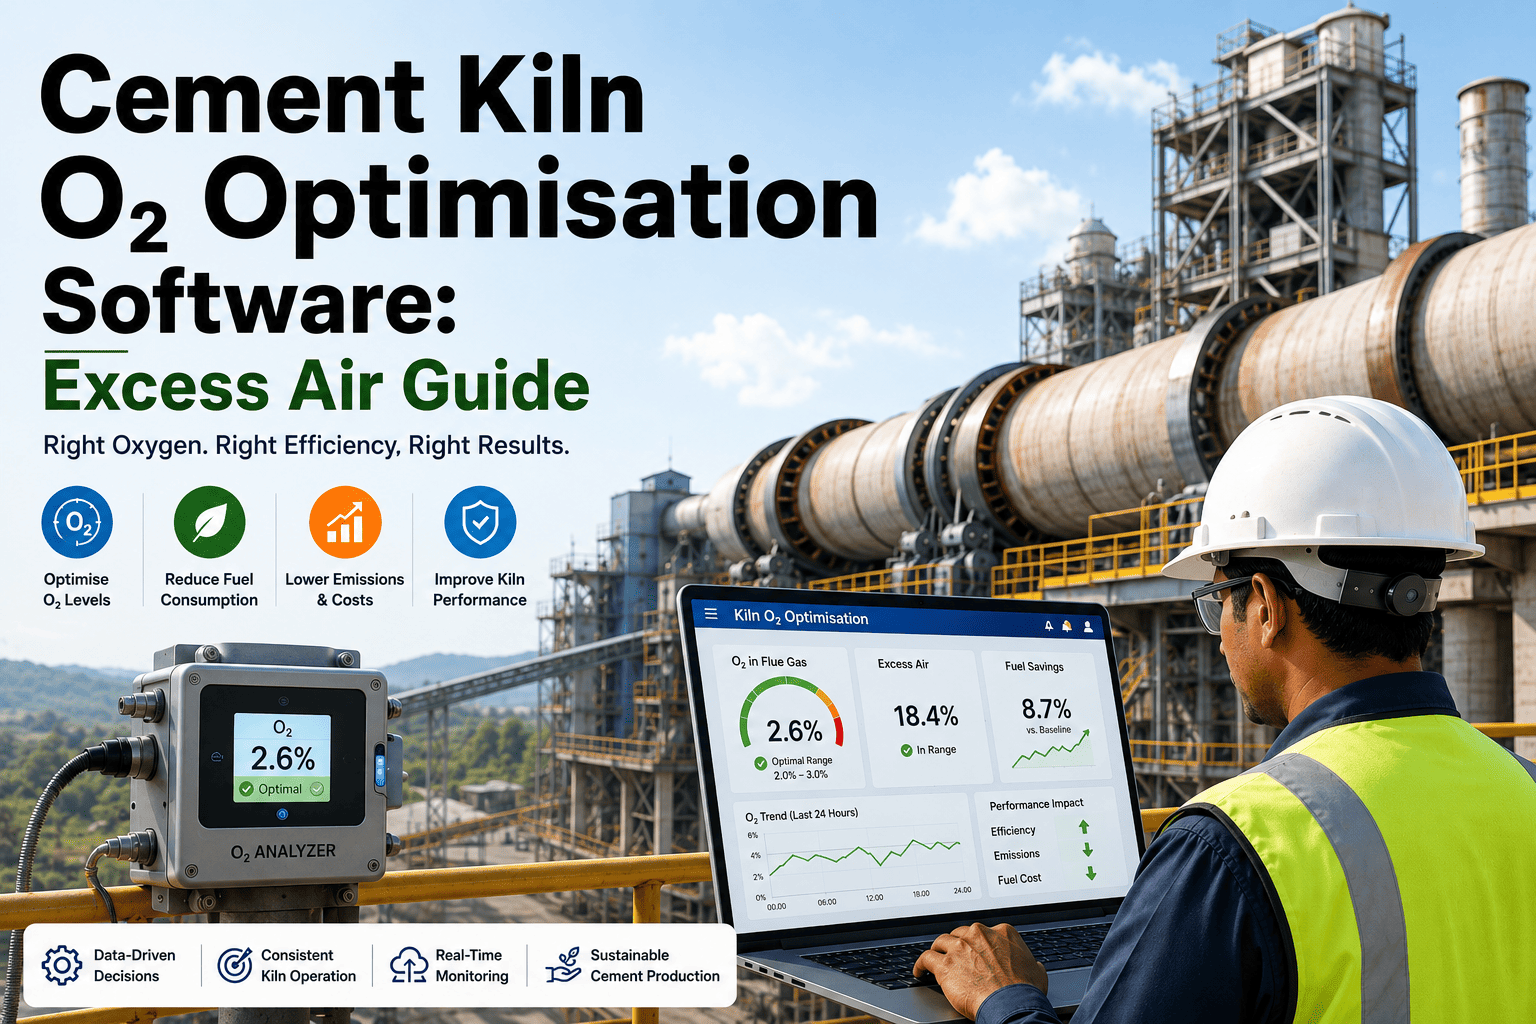
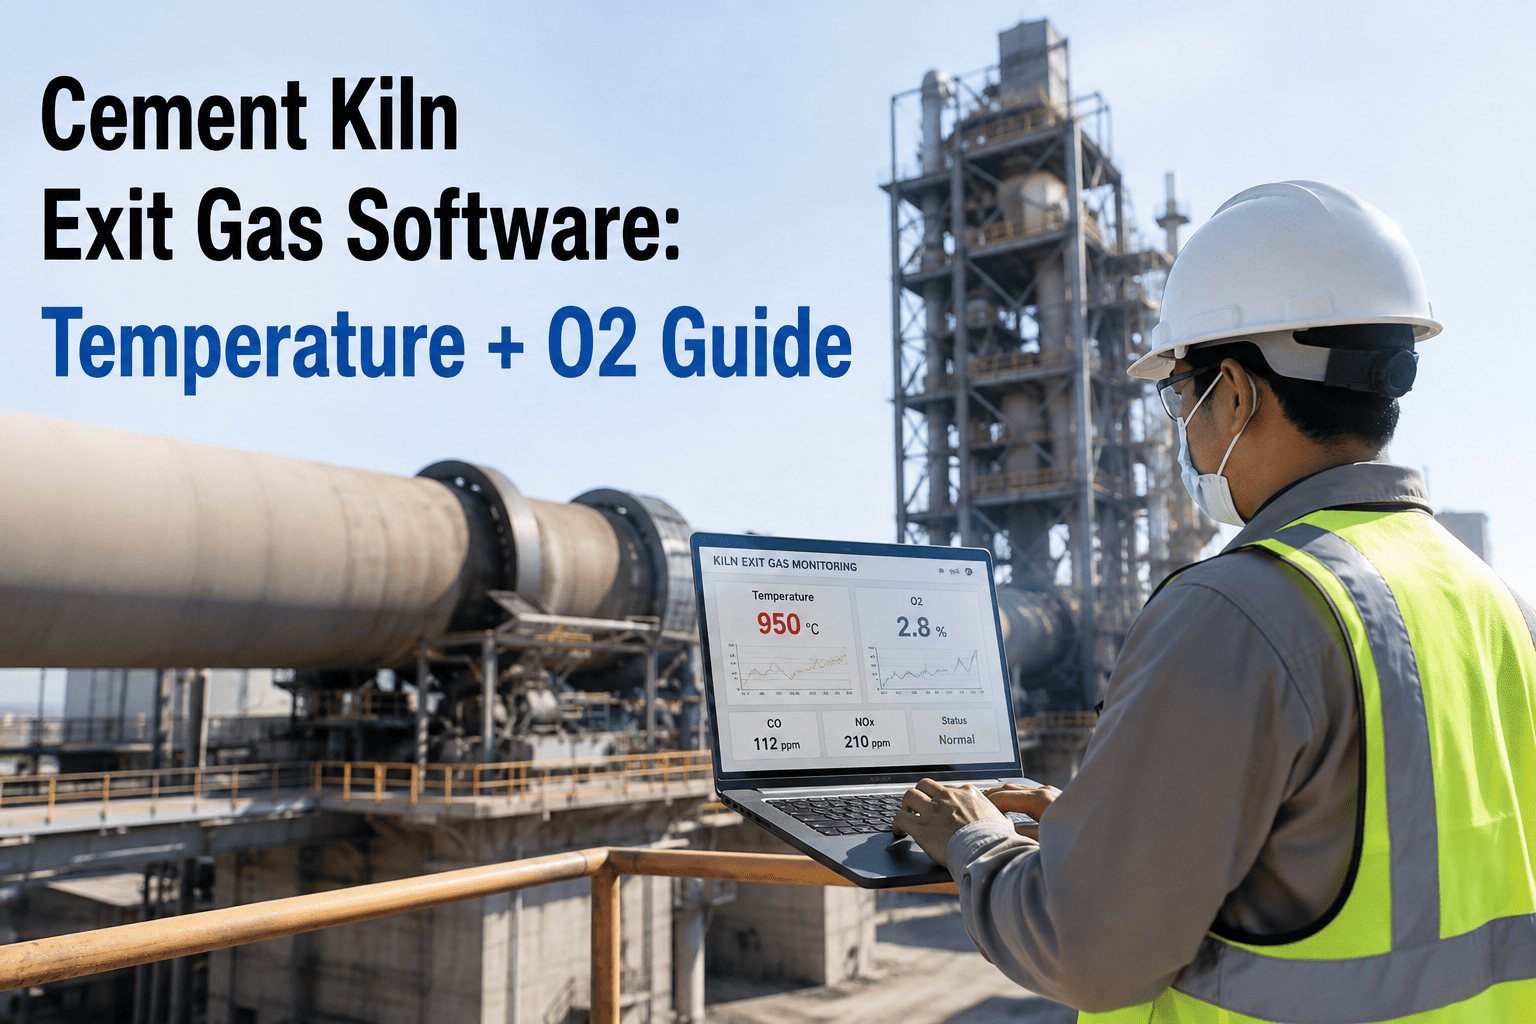
Every kiln has an oxygen setpoint sitting between two expensive mistakes, and most operators split the difference with more excess air than the process actually needs. Run kiln inlet O2 too low and CO climbs past 0.1 percent, signaling incomplete combustion and flame instability that no shift wants to explain at handover. Run it too high — which is where most kilns actually sit, closer to 4 or 5 percent than the 2 to 4 percent optimum — and every extra point of excess oxygen burns fuel just to heat air that carries no benefit out the stack. The plants that hold a tight O2 band do it by tracking false air ingress, damper position, fan speed and burner alignment as maintenance parameters instead of leaving the number to whichever operator is on console that week. Oxmaint turns that tracking into a documented maintenance record — see how at app.oxmaint.ai.
Kiln Combustion · CMMS-Tracked O2
Cement Kiln O2 Optimisation Software
A kiln running 5 percent excess oxygen instead of 3 percent is not burning cleaner — it is paying a fuel penalty for margin nobody is actively managing. Oxmaint tracks kiln inlet O2, CO and the mechanical parameters behind them — seals, dampers, fan speed, burner alignment — so excess air stays close to setpoint without operators trading combustion stability for thermal efficiency.
The O2 Balance
Three Zones Every Kiln Inlet O2 Reading Falls Into
Kiln inlet oxygen is not a number to minimise or maximise — it is a number to hold inside a narrow band, shift after shift, regardless of who is on console. Everything below that band risks combustion, and everything above it wastes fuel that has already been paid for by the tonne. The spectrum below shows where the line actually sits, and why the middle band is the only one a well-run kiln should live in.
CO Risk Zone
Oxygen below roughly 2 percent leaves too little margin for combustion swings caused by fuel quality changes or feed variation. CO readings above 0.1 percent at the kiln inlet signal unburnt fuel escaping the flame — an early warning of flame instability and, in the worst case, an afterburning risk further up the preheater that can damage refractory and ductwork.
Optimal Combustion Zone
Cement kilns are typically designed to run in a 2 to 4 percent excess oxygen band at the kiln inlet — enough margin for complete, stable combustion across normal fuel and feed variation without paying a thermal penalty for air the flame does not actually need.
Fuel Waste Zone
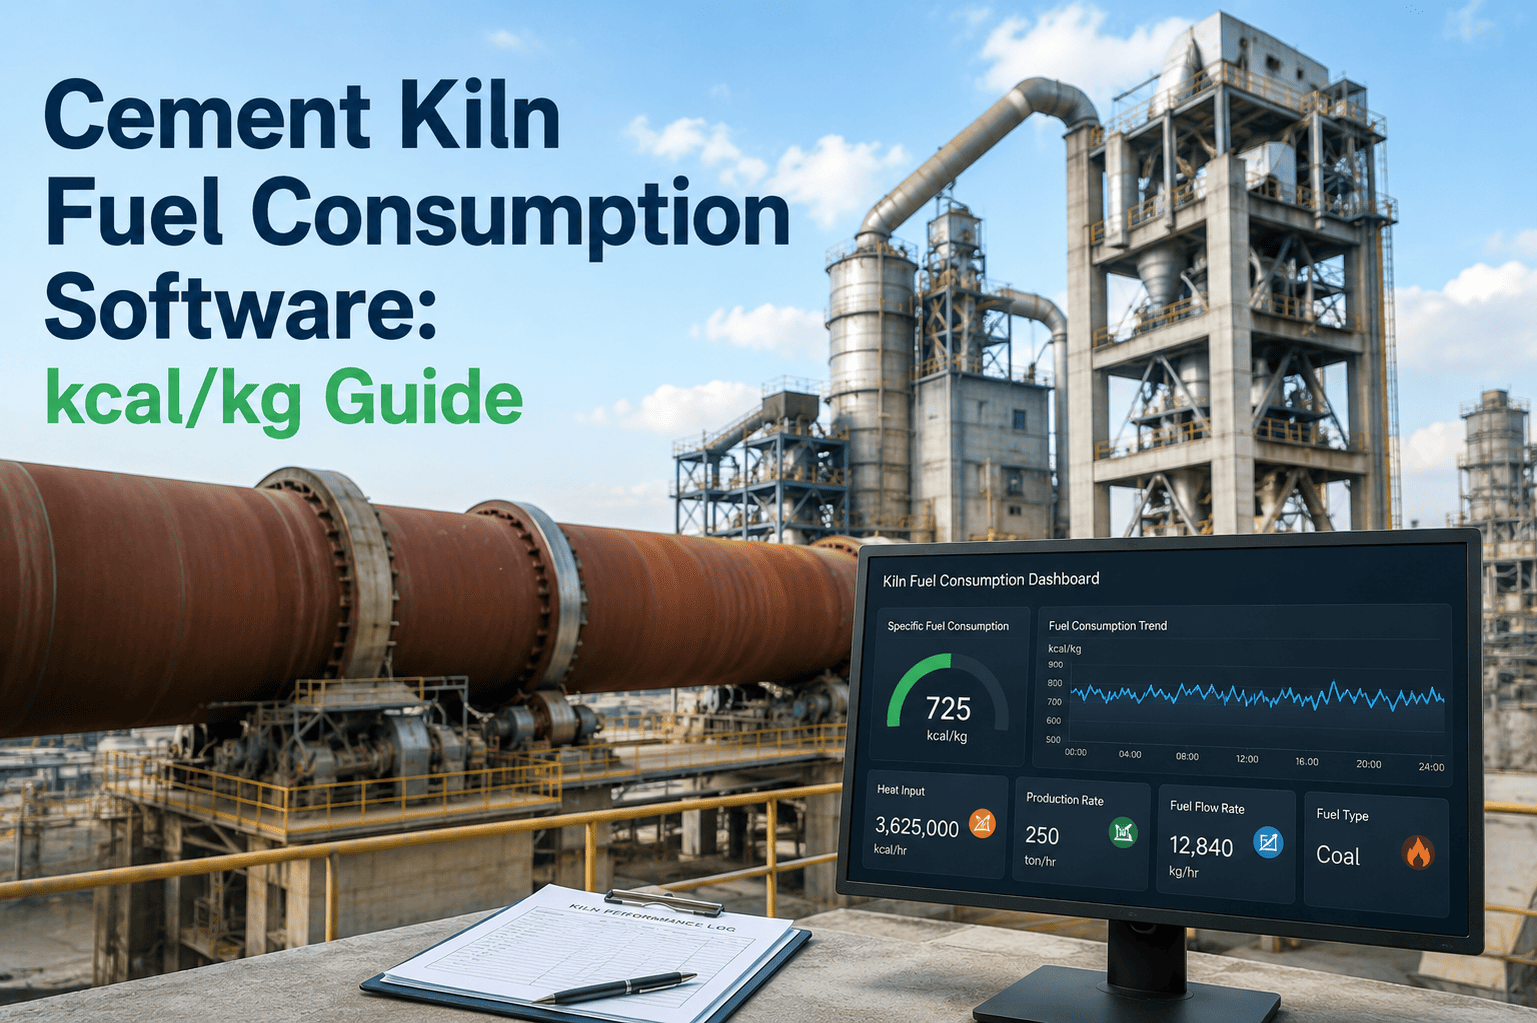
Each percentage point of excess oxygen carried above the optimum increases fuel consumption by roughly 0.5 to 1 percent, since the flame is heating air that carries no combustion benefit and simply exits through the stack. In practical terms, every 1 percent the excess O2 reading is trimmed back toward setpoint is worth an estimated 4 to 6 kcal/kg reduction in thermal specific energy consumption — a saving that compounds across every tonne of clinker produced that day.
2–4%
Design excess oxygen band at the kiln inlet for stable, efficient combustion on a modern dry-process kiln
4–6 kcal/kg
Thermal SEC reduction typically achieved for every 1 percentage point of excess O2 trimmed back toward setpoint
3 kcal/kg
Heat loss added for every 1 percent of false air infiltration diluting the O2 reading at the kiln inlet or preheater exit
$600K–$1.5M
Typical annual fuel cost swing between shift teams running the same kiln without a documented, tracked O2 setpoint
See Your Own O2 Gap
Find Out How Many kcal/kg Are Sitting in Your Excess Air Reading
Most kilns are running further from their optimum O2 band than the shift log suggests, and the gap usually traces back to a seal, a damper or a fan speed nobody has revisited since commissioning. Oxmaint puts kiln inlet O2, CO and the mechanical parameters that drive them side by side, so the gap between actual and optimum stops being a guess.
Root Causes
What Actually Pushes Excess O2 Off Target
An O2 reading drifting upward is rarely a combustion problem on its own — it is usually a mechanical condition somewhere in the kiln system showing up as a process number weeks or months after the underlying wear started. These four causes account for most of the drift reliability teams chase, and three of the four are directly visible in maintenance data long before the fuel bill reflects them.
01
False Air Infiltration
Worn kiln inlet seals, leaking preheater cyclone doors and degraded expansion joints all pull ambient air into the gas stream, diluting the O2 reading and forcing the kiln to compensate with additional fuel to hit the same clinker output. Each 1 percent of false air adds roughly 3 kcal/kg in heat loss, and it also masks the true combustion state from the operator reading the analyser, making the O2 trend look more stable than the actual flame condition really is.
02
ID Fan Speed Mismatch
An induced draft fan running faster than the current production rate actually requires pulls more total air through the entire system than combustion needs, raising excess oxygen even when every seal and damper is in good working condition. Fan speed left uncorrected as throughput ramps up or down is one of the most common — and most fixable — sources of O2 drift, since correcting it requires a calibration adjustment rather than a shutdown repair.
03
Damper Position Drift
Dampers set correctly for one production rate rarely stay correct as load, fuel mix or raw meal moisture shift through a campaign. A damper left in a stale position quietly biases the air balance toward excess, and the drift accumulates for weeks before anyone notices the O2 trend has moved, because the change happens gradually rather than as a single obvious event.
04
Burner Alignment and Primary Air
A misaligned burner or excessive primary air axial momentum stretches the flame and pushes it off-centre, sometimes far enough to impinge on the kiln shell, forcing operators to run higher total excess air just to keep combustion stable and CO under control. Correcting axial and swirl air settings has taken kilns from 4.8 percent excess oxygen down to 2.6 percent in documented combustion audits, without raising CO above safe limits.
Where False Air Gets In
False Air Leak Points and Their Heat Loss Impact
False air does two things at once — it wastes heat directly, and it dilutes the O2 reading so the true combustion state is hidden from whoever is watching the panel. That combination is what makes it dangerous: an operator staring at a stable-looking O2 trend has no way to know part of that reading is diluted air rather than genuine combustion margin. Tracking these leak points as maintenance assets, not just process symptoms, is what keeps the O2 reading honest and gives the reliability team a defensible reason to schedule the repair.
| Leak Location | Typical Failure Point | Impact |
| Kiln inlet seal |
Nose ring and inlet seal wear |
Each 1% false air adds roughly 3 kcal/kg heat loss |
| Preheater cyclone doors |
Worn inspection door gaskets |
Dilutes O2 reading, masks true combustion state |
| Duct expansion joints |
Bellows cracking or seal failure |
Cools exhaust gas, reduces heat recovery |
| Meal feed and riser pipes |
Loose duct connections |
Uneven gas distribution, localised cooling |
CMMS Integration
How an O2 Drift Becomes a Scoped Work Order
Spotting excess oxygen on a trend chart only helps if it turns into a scoped inspection before the fuel bill reflects it. Oxmaint's maintenance planning layer converts a drifting O2 or CO reading into a work order with the trend data attached, so the response is documented rather than dependent on a shift note that may or may not get read by the next crew.
| Signal | Parameter Monitored | CMMS Action Triggered | Lead Time |
| O2 trending above 4.5% with stable fuel rate |
Kiln inlet excess oxygen |
False air survey work order for seals and dampers |
3–7 days |
| CO periodically spiking above 0.1% |
Kiln inlet CO concentration |
Combustion and burner alignment audit |
2–5 days |
| ID fan speed inconsistent with production rate |
Fan speed vs throughput trend |
Fan speed calibration work order |
5–10 days |
| Seal wear approaching replacement interval |
Kiln inlet seal thickness |
Scheduled seal replacement PM, parts reserved |
10–18 days |
From The Field
What Process Engineers Say About Tracking Excess Air
We were running close to 5 percent excess oxygen and calling it a safety margin, the way it had always been described to new operators coming onto the console. Once we started tracking false air survey results alongside the O2 trend, we found two leaking expansion joints nobody had flagged in over a year. Fixing them alone brought us down to 3.2 percent without touching a single burner setting.
The variance between our day and night shift O2 setpoints was costing us more than we realised until we saw it laid out as an actual fuel-cost number instead of a general impression that "night shift runs a bit rich." Locking the band into a tracked parameter instead of operator judgment closed most of that gap within one quarter.
Book a demo and ask about shift-variance tracking specifically.
Lock In Your O2 Band
Turn False Air Surveys and Fan Speed Into Tracked Maintenance Parameters
Every kcal/kg saved by trimming excess air starts with knowing exactly which seal, damper or fan is driving the drift. Oxmaint connects your combustion analyser data to the maintenance record that actually fixes it.
Performance Benchmarks
Kiln O2 Optimisation — Before vs After CMMS Tracking
These figures reflect the typical range plants report within two to three quarters of moving from periodic combustion checks to continuously tracked O2, CO and false-air parameters across every shift and every kiln zone. The excess oxygen and CO improvements tend to show up first, while false air survey compliance and shift variance take longer to fully close as the tracked-parameter habit becomes routine across every crew.
| Metric | Without O2 Tracking | With Oxmaint O2 CMMS | Change |
| Kiln inlet excess oxygen |
4.5–5.5% |
2.5–3.2% |
-2 to -2.5 pts |
| Thermal specific energy consumption |
760–790 kcal/kg |
700–720 kcal/kg |
-7% average |
| CO excursions above 0.1% per month |
9 average |
2 average |
-78% |
| False air survey compliance |
41% |
89% |
+48 pts |
| Shift-to-shift O2 variance |
1.8 pts average |
0.6 pts average |
-67% |
Common Questions
What Process Teams Ask Before Tracking Kiln O2 in a CMMS
What excess O2 reading should our kiln inlet actually be running?
A modern dry-process kiln should hold roughly 2 to 4 percent excess oxygen at the kiln inlet. Readings sitting consistently above that band are usually paying a fuel penalty for margin the process does not need, while readings below it risk incomplete combustion, rising CO and flame instability that shows up as quality variance in the clinker.
Can we just cut excess air directly without addressing false air first?
Not safely — trimming damper or fan settings without first correcting false air infiltration can push CO above 0.1 percent and destabilise the flame, because the true air-to-fuel ratio is being masked by the leak diluting the reading. A false air survey should always come before any setpoint change is made on console.
How does Oxmaint turn an O2 drift into a maintenance action automatically?
Live O2, CO and fan-speed data feed into Oxmaint against defined control bands built around the 2 to 4 percent optimum. When a reading drifts outside its band, Oxmaint opens a scoped work order — a false air survey, a burner alignment check, a fan calibration — with the trend chart attached so the technician knows exactly what to inspect.
Sign up free to see your own O2 trend mapped against maintenance history.
Can we connect existing combustion analysers without new instrumentation?
Yes — Oxmaint reads existing O2 and CO analyser tags through your SCADA, PI historian or OPC-UA connection rather than requiring new sensors or a control system change. The analysers already installed on the kiln become the data source for the maintenance layer, so nothing on the process side needs to be touched.
How quickly does a false air survey typically pay for itself?
Given that 1 percent of false air adds roughly 3 kcal/kg in heat loss on a large kiln, closing even a single leaking expansion joint or seal often recovers its repair cost within weeks, well before the next planned shutdown arrives.
Book a demo to estimate the payback for your own kiln's fuel spend.
Start Tracking Kiln O2 Today
Bring Excess Air, CO and False Air Surveys Into One CMMS
Process and reliability teams at leading cement groups use Oxmaint to hold kiln inlet O2 near its optimum band instead of leaving it to shift-to-shift judgment. Drifting readings become work orders. Survey data trains better decisions. Plant leadership gets a real kcal/kg number tied to a documented cause instead of a rounded estimate on a monthly report.