Compressed air is one of the most expensive utilities in a cement plant, and a large share of it never does any work. It escapes through worn couplings, failed pulse valve diaphragms, cracked hoses and open drain valves, then reappears as extra compressor hours and a power bill nobody can explain. Leaks are quiet in a noisy plant, so they survive for years unless someone owns them. This guide shows how to find, size, repair and verify them using a workflow built on Oxmaint maintenance management software.
Cement plant compressed air leak detection and maintenance: stop paying to make air that escapes
Unmanaged compressed air systems commonly lose 20 to 30 percent of compressor output to leaks, while a well-run system holds that under 10 percent. Turn leak surveys, repairs and verification into scheduled maintenance work instead of an occasional energy project.
Where a cement plant actually uses compressed air
Air is generated in one place but consumed in dozens, and every branch drop is a chance to lose it. Mapping the path from compressor to end use shows where leak surveys should concentrate.
Generation
Treatment
Distribution
Area drops
End use
Why leaks hide so well in cement manufacturing
A packaging line can sometimes hear a leak. A cement plant rarely can, and the environment works against every manual method.
- Dust coats everything. Fine dust covers fittings and hides the weeping joints that would otherwise be visible.
- Noise masks hissing. Mills, fans and blowers drown out the sound of a small leak at the ear.
- Access is awkward. Pipe racks run through hot, elevated and confined spaces that surveys tend to skip.
- Vibration loosens joints. Fittings near mills, crushers and fans work loose and start leaking again after repair.
- Moisture corrodes lines. Poor drying turns small pinholes into larger leaks over time.
Common leak sources by plant area
| Plant area | Typical leak sources | Detection tip |
|---|---|---|
| Baghouses and dust collectors | Pulse valve diaphragms, stuck solenoids, manifold unions | Scan between pulses; a valve that hisses while idle is bleeding continuously |
| Preheater and kiln area | Air cannon valves, tank fittings, hoses to cleaning ports | Check after cannon firing sequences and after hose changes |
| Pneumatic conveying | Pump feed valves, flexible hoses, hose clamps | Scan under load; leaks open up under flexing |
| Mill and separator circuits | Instrument air tubing, actuator seals, regulators | Walk instrument air branches with the mill running |
| Silo discharge and aeration | Aeration lines, isolation valves, branch drops | Survey during discharge and during idle periods |
| Packing plant | Cylinder seals, hoses, filter regulator lubricators, open blow-offs | Tag every open-ended blow-off for review, not just leaks |
| Compressor room | Drain valves, relief valves, couplings, receivers | Check automatic drains that never close |
The cost math every maintenance team should be able to run
Leaks become fixable when they carry a dollar figure. The calculation is simple enough to attach to every tagged leak.
| Leak size at 100 psig | Approx. flow | Power wasted | Annual cost (illustrative) |
|---|---|---|---|
| 1/16 inch | 6.5 cfm | 1.2 kW | About $1,025 |
| 1/8 inch | 26 cfm | 4.7 kW | About $4,100 |
| 1/4 inch | 104 cfm | 18.7 kW | About $16,400 |
How to use these numbers honestly
- Replace the electricity rate and specific power with your own metered values.
- Treat flow figures as estimates; flow through a leak rises and falls with line pressure.
- Remember the Pareto effect: repairing the largest fifth of leaks typically recovers most of the recoverable loss.
- Count the secondary cost too, because leaks push compressors to run longer and wear faster.
Leak detection methods compared
Several methods work, but they differ sharply in how well they cope with a loud, dusty plant.
| Method | How it works | Strength | Limit in a cement plant |
|---|---|---|---|
| Listening and feeling | Inspector hears or feels escaping air | No equipment needed | Misses small leaks; plant noise defeats it |
| Soapy water | Bubbles form at the leak point | Confirms a suspected joint | Slow, messy and hard to use on dusty or elevated pipe |
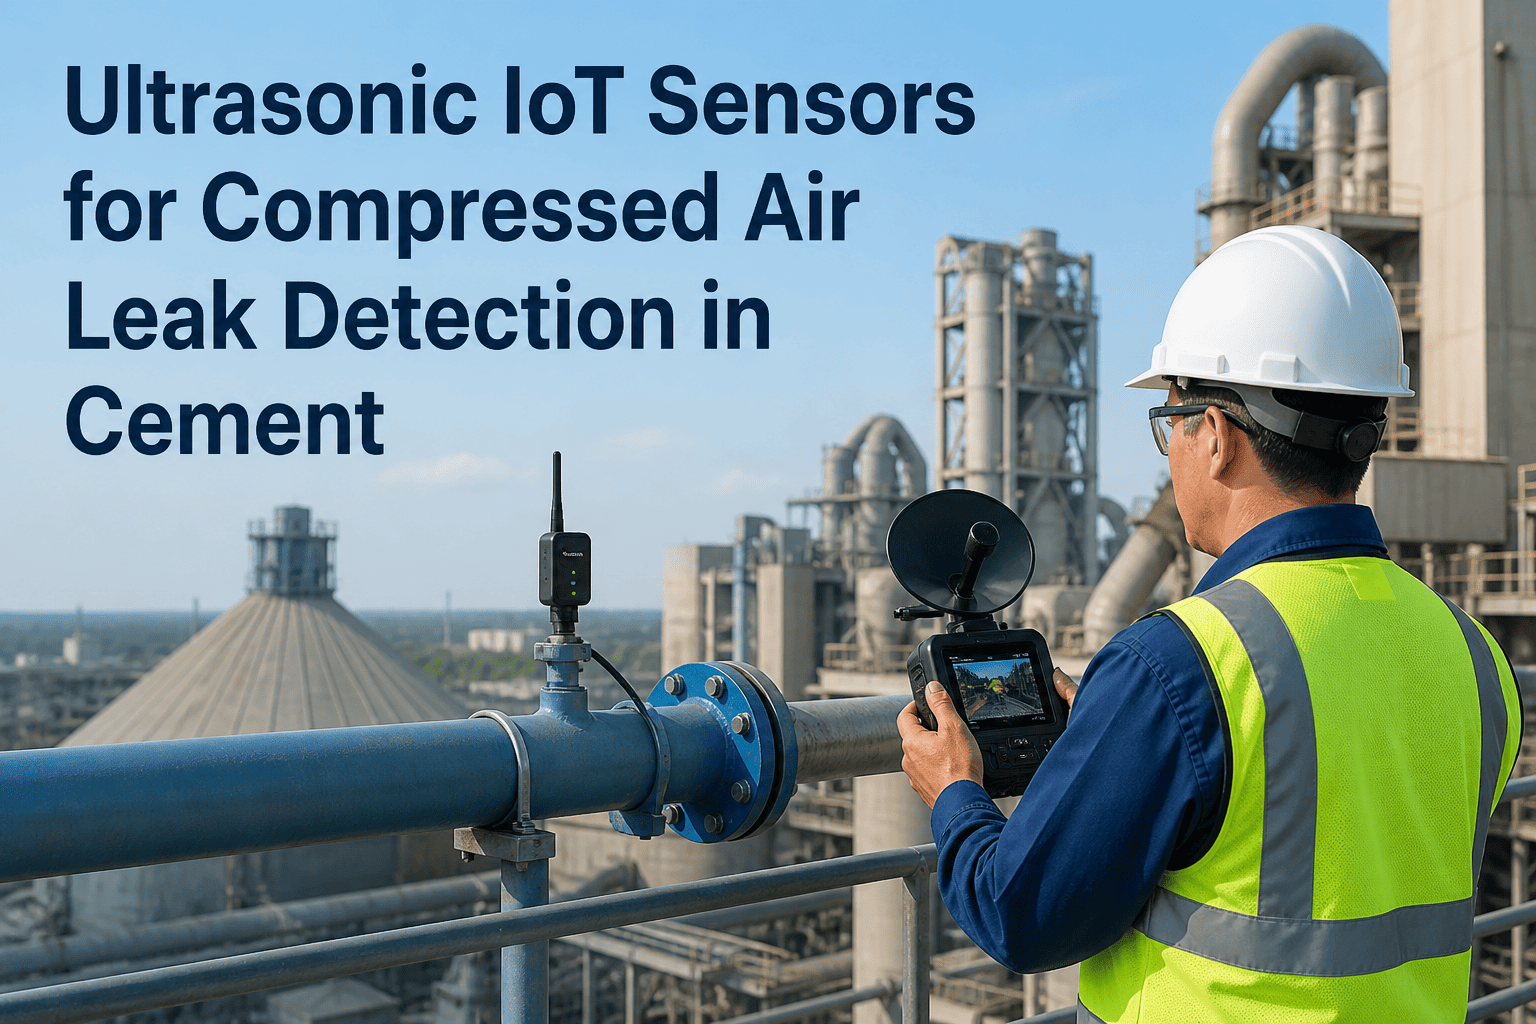
| Ultrasonic detection | Handheld instrument picks up the high-frequency sound of turbulent flow | Directional, works while the plant runs, can estimate flow | Needs trained operators and a consistent route |
| Load and unload test | With demand off, time how long the compressor loads and unloads | Gives a whole-system leak percentage | Needs a quiet period and does not locate leaks |
| Flow metering | Continuous measurement of air flow on headers | Shows leak trends between surveys | Requires installed meters and baselines |
Why ultrasonic survey belongs in the maintenance calendar
- It finds leaks while the plant is running, so no outage is needed.
- It can be repeated on the same route every quarter and compared to the last result.
- It produces a tagged list that converts directly into work orders.
Put every compressed air leak on a work order, not a wish list
Schedule surveys, track tagged leaks, assign repairs and confirm closure from one maintenance system your whole team can use on a phone.
A leak management loop that keeps savings from fading
One-time surveys save energy for a few months and then decay. A repeating loop is what holds the leak rate down.
Survey on a fixed route
Tag and photograph
Grade and cost
Repair through work orders
Verify and trend
Grading leaks so the right ones get fixed first
Treating every hiss equally floods the work queue. A simple grading rule sends effort where the money and risk are.
| Grade | Example criteria | Typical response |
|---|---|---|
| Grade A | Large flow, or leak on a critical actuator or instrument air line | Repair within days; isolate if safe to do so |
| Grade B | Moderate flow on a common fitting, hose or valve | Repair within the next planned work window |
| Grade C | Small flow, hard-to-reach location, or needs a shutdown | Bundle into a planned outage and monitor |
Thresholds are a site decision
- Set cfm and dollar thresholds from your own electricity rate and compressor efficiency.
- Escalate any leak that returns within a set period as a repeat failure.
- Review the Grade C list every outage planning cycle so it does not become permanent.
Reactive air system versus managed air system
The difference shows up in how leaks are found, owned and measured.
Reactive air system
- Leaks found when someone happens to hear them
- Compressors added or run longer to hold pressure
- Repairs done without cost or flow records
- Same fittings fail repeatedly with no history
- Savings claimed once and never verified
Managed air system
- Scheduled ultrasonic surveys on fixed routes
- Leak percentage tracked against a target
- Every leak tagged, costed and tied to a work order
- Repeat leaks flagged by asset and location
- Re-scan confirms each repair before closure
Three controls that decide whether savings stick
Repairing leaks is only part of the system. These three controls determine whether the saved air actually becomes saved electricity.
Pressure setpoint
Compressor sequencing
Air treatment and drains
Compressed air PM checklist for a cement plant
Use this as a starting task list and adjust frequencies to your plant, duty cycle and compressor manufacturer guidance.
Weekly
- Check automatic drain operation on receivers and filters
- Review compressor load and unload hours
- Walk compressor room for oil, noise and heat changes
- Check dust collector pulse valves for continuous bleeding
Monthly
- Inspect hoses and quick couplers in high-traffic areas
- Check filter differential pressure and dryer performance
- Close out open tagged leaks and re-scan repairs
- Review header pressure against actual demand
Quarterly
- Run a full ultrasonic leak survey on the fixed route
- Run the load and unload leakage test in a quiet window
- Compare leak count, cost and percentage with last quarter
- Review repeat-leak locations and fix root causes
Dust collector pulse valves: the biggest single leak target
Baghouses and dust collectors are often the largest consumers of compressed air in a cement plant, so a stuck valve or worn diaphragm here is worth chasing first.
Warning signs of a bleeding valve
- Continuous hiss from a valve between pulses
- Manifold pressure that sags during cleaning cycles
- Rising differential pressure across the collector
- Repeated diaphragm replacement on the same row
- Compressor load hours climbing with no production change
Maintenance response
- Raise a corrective work order tagged to the collector and valve position
- Replace the diaphragm and check the solenoid and pilot line
- Confirm air quality and drain operation upstream
- Review pulse pressure, duration and interval settings
- Re-scan after repair and record the result
Common mistakes that let leaks return
- Repairing leaks but never re-scanning, so failed repairs stay on the books as fixed.
- Leaving open-ended blow-offs and unused branch lines pressurized.
- Using cheap fittings in high-vibration areas, then repeating the same repair every quarter.
- Skipping the Grade C list, which quietly becomes the permanent leak load.
- Reporting savings without comparing compressor hours or kWh before and after.
- Assigning the survey to one person with no backup, so the route stops whenever they are away.
- Ignoring leaks on lines that feed critical actuators because they are hard to reach, rather than planning them into an outage.
KPIs that prove the program is working
Pick a small set and review it monthly with maintenance and energy owners.
How Oxmaint supports the compressed air program
Oxmaint does not replace the ultrasonic detector. It keeps the work around it organized and visible.
Compressed air leak detection FAQs
How often should a cement plant survey for compressed air leaks?
Is ultrasonic detection accurate in a loud cement plant?
What leak rate should we aim for?
Why do the same dust collector valves keep leaking?
Can a CMMS help reduce compressed air waste?
Make compressed air leaks a scheduled job with a measurable result
Build your survey route, tag and cost each leak, and track repairs to closure so air savings show up in your energy numbers.