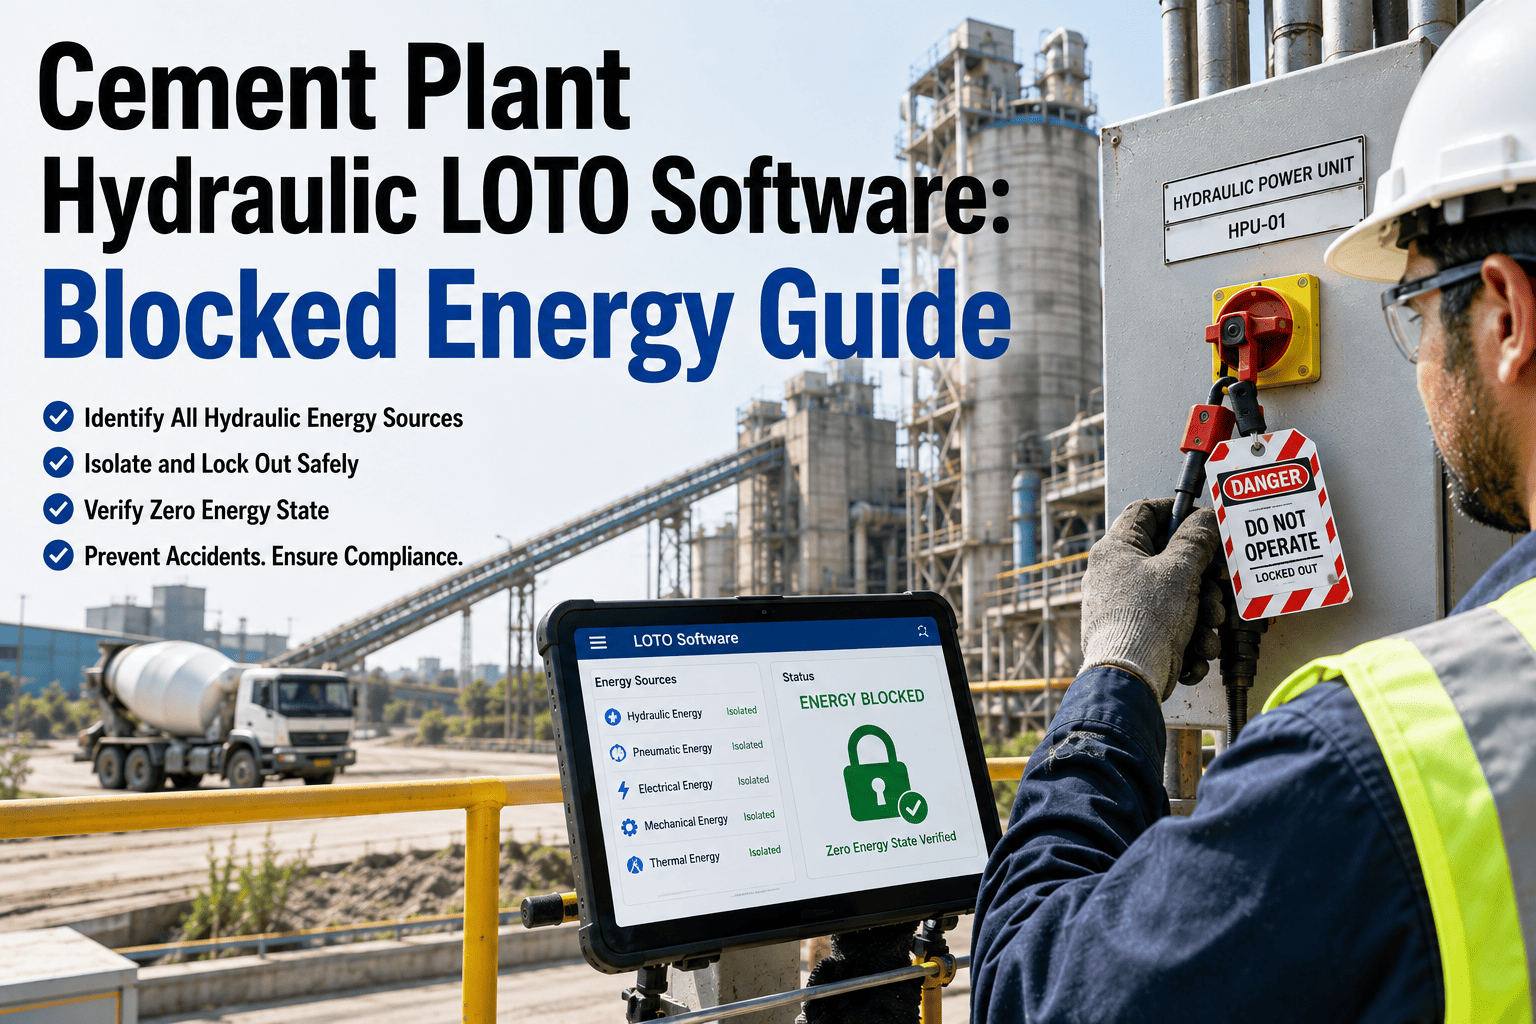
Hydraulic energy is the one lockout/tagout gap that keeps showing up in cement plant incident reports, and it rarely announces itself the way electrical energy does. A clinker cooler grate segment held by a hydraulic ram, a raw mill roller pressed down by 1,200 kN of hydraulic clamping force, or a kiln inlet gate cylinder can all stay charged with stored pressure long after the pump is switched off and the breaker is locked out. That residual pressure is what OSHA 1910.147 classifies as blocked or stored energy, and it accounts for a disproportionate share of caught-in and struck-by injuries during cement plant maintenance work. This guide maps where hydraulic and blocked energy hides across cooler, mill, and kiln inlet assets, how to verify a true zero-energy state before anyone steps inside the equipment, and how a CMMS-based digital LOTO permit closes the gap paper tags leave open. Start a free trial to see the verification workflow mapped to your own asset register.
Your breaker is locked. Is the hydraulic ram behind that cooler plate still holding 200 bar?
Electrical lockout stops a motor. It does nothing to a hydraulic cylinder, accumulator, or spring-loaded gate that was already charged before the pump shut down. Plants that skip a dedicated blocked-energy verification step are the ones that get caught by a cylinder that "settles" mid-repair, a gate that drifts closed on a hand, or a mill roller that drops the moment the last retaining pin is pulled. The gap is rarely a missing lock — it is a missing verification step for the energy that a lock was never designed to control in the first place.
Four hydraulic energy points that survive electrical lockout
Across cooler, mill, and kiln inlet assets, hydraulic circuits are built to hold position without continuous pump power — which is exactly why they stay dangerous after the drive motor is isolated and tagged. A cylinder that holds a load steady during production is, by design, still holding that load the instant the pump stops. Each of the four points below needs its own bleed-down and verification step inside the permit, not a blanket "hydraulics off" checkbox that treats every circuit on the asset the same way.
Clinker cooler grate hydraulic rams
Pusher and walking-floor grate segments are driven by hydraulic cylinders holding several tonnes of push force against a hot clinker bed. When the drive pump stops, the accumulator and cylinder can still carry full system pressure, and a segment can lurch forward the moment a fitting is loosened without a proper bleed-down. Technicians replacing worn grate plates are working directly in the segment's travel path, which is what makes this the highest-frequency blocked-energy exposure on a cooler deck.
Vertical roller mill hydraulic clamping
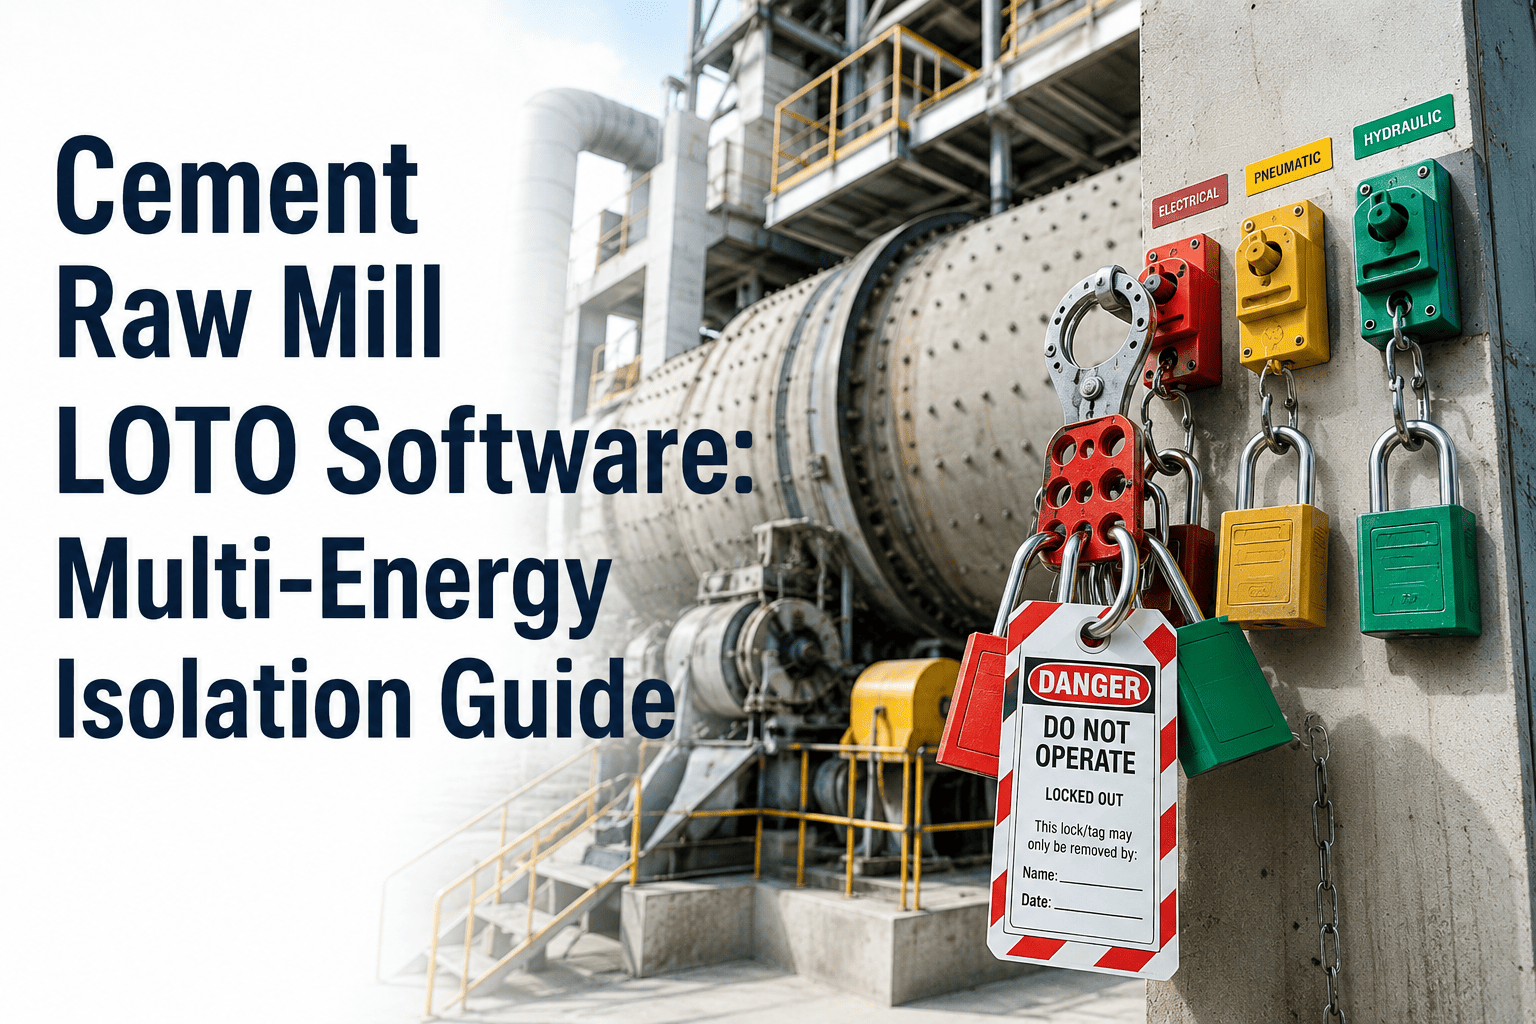
VRM grinding rollers are held onto the table by hydraulic cylinders running up to 1,200 kN of clamping force. Releasing this pressure the wrong way — or working under a roller before the cylinder is mechanically blocked — is one of the highest-severity blocked-energy exposures on a cement mill floor, since a dropped roller has enough mass to crush a limb or fatally strike a technician working in the grinding zone.
Kiln inlet and outlet gate cylinders
Inlet seal and outlet gate cylinders hold their set position with residual line pressure so the gate does not drift under process pressure swings. A gate that appears "parked" can still close or shift once a hose is disconnected for inspection unless the circuit is bled to atmosphere first, and the confined, high-heat location of most inlet gates leaves very little room to react if it does move.
Roller press hydraulic accumulators
Roller press frames use nitrogen-charged hydraulic accumulators to absorb shock loading between the two counter-rotating rolls. These accumulators store energy independently of the main pump circuit and require a dedicated discharge valve sequence — a step that is frequently missing from generic LOTO procedures because the accumulator sits outside the main hydraulic power unit that most written procedures were built around.
What a blocked-energy incident actually costs a cement plant
Blocked-energy injuries are rarely minor. Because the release involves stored mechanical force rather than a slow drift, the resulting injuries tend toward amputation, crush trauma, or fatality — and the downstream costs extend well past the medical claim.
OSHA and MSHA citation exposure
A confirmed blocked-energy violation under 1910.147 is treated as a serious or willful citation depending on whether the gap was known, with penalties compounding when the same isolation point has been flagged in a prior audit and never corrected.
Line stoppage during the investigation
A reportable incident typically halts the affected line — and often the surrounding process area — until the investigation team, insurer, and safety authority sign off on a return-to-service plan, adding days of unplanned downtime on top of the incident itself and the resulting clinker production loss.
Contractor and insurer confidence
Multi-site cement groups increasingly tie contractor eligibility and insurance premiums to safety performance data, so a single blocked-energy incident can raise renewal costs, restrict which contractors are willing to bid the next outage, and follow the plant into group-level safety scorecards.
The step that was actually missing
Post-incident reviews in cement plants consistently trace blocked-energy events back to the same root cause: a written procedure that covered electrical isolation in detail but treated hydraulic and gravitational energy as a single, unverified checkbox with no gauge or sign-off requirement attached.
Give every hydraulic point its own line item on the permit.
OxMaint builds asset-specific LOTO procedures that separate electrical, hydraulic, and gravitational energy into individually verified steps — not one generic checkbox.
Four checks before anyone reaches into the equipment
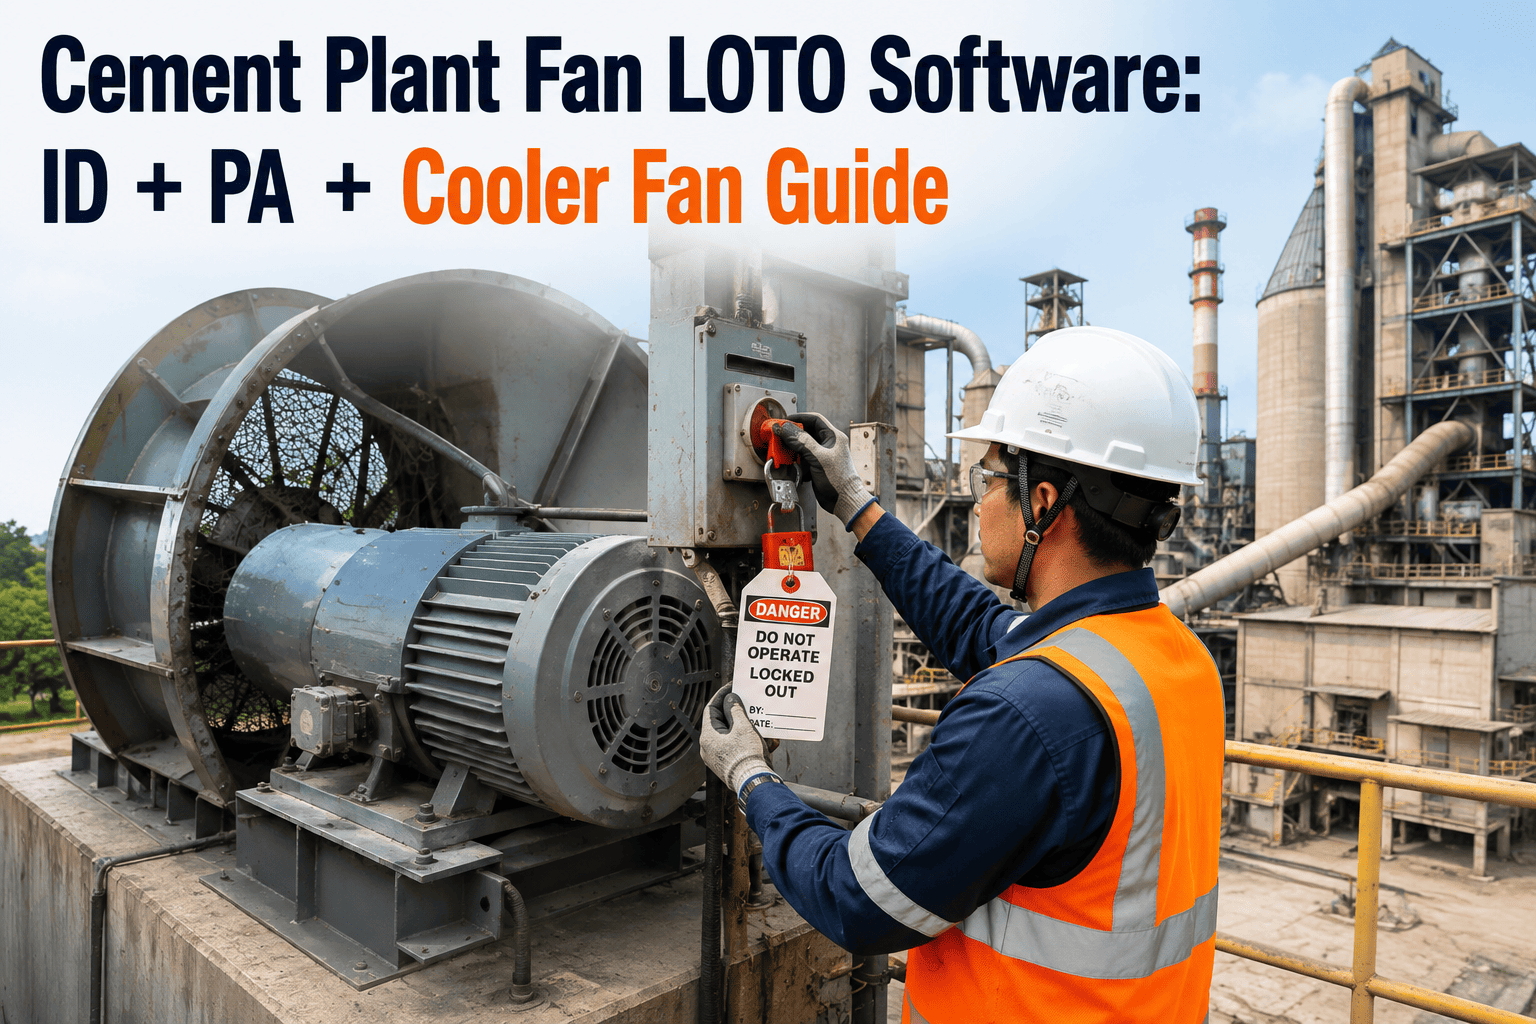
A lock on the breaker only proves electrical isolation. Confirming a true zero-energy state on hydraulic and blocked-energy points takes a separate, sequenced verification — the same four checks every time, regardless of which asset is being opened. Skipping the order, or treating any single check as optional on a "quick job," is how a routine inspection turns into a reportable incident.
Confirm pressure gauges read zero on every circuit
Before any hose or fitting is loosened, the technician reads and logs the pressure gauge on the cylinder, accumulator, and supply line. Anything above zero means the bleed-down step was skipped or incomplete, and work does not proceed until it reads clean and the reading is recorded on the permit for later review.
Install a physical block, not just a closed valve
A closed isolation valve can leak or be bumped open. For any load that could move under gravity or spring return — a mill roller, a raised gate, a cooler segment — a mechanical prop, pin, or blocking bar is installed as the primary restraint before hands go near it, and the block itself is load-tested by hand before anyone trusts it.
Try the normal start controls to prove isolation holds
With locks applied and blocks installed, the authorized employee attempts a normal start from the control panel. A failed start attempt is the final proof that electrical, hydraulic, and mechanical isolation are all holding together, not just individually correct, and the controls are immediately returned to the off position afterward.
A second authorized employee signs off independently
A second qualified person re-checks the gauges and blocks and signs the permit independently of the first technician, without simply relying on the first employee's word. This second signature is what turns a single point of human error into a two-person control, and it is the record an auditor will ask for first.
Isolation method and verification check, by asset
Every asset on the plant carries a different mix of energy types, and each mix demands its own isolation method and its own verification check. This isolation map is the starting point for building an asset-specific written procedure rather than relying on one generic hydraulic LOTO form for the whole site — a form that inevitably drifts out of date as equipment is modified, replaced, or retrofitted.
| Asset | Primary Energy Type | Isolation Method | Verification Check |
|---|---|---|---|
| Cooler grate ram | Hydraulic + gravity | Bleed valve + segment prop | Gauge zero, prop load-tested |
| VRM roller clamp | Hydraulic (high pressure) | Discharge valve + mechanical pin | Gauge zero, pin engaged |
| Kiln inlet/outlet gate | Hydraulic + spring return | Line bleed to atmosphere | Gauge zero, gate chocked |
| Roller press accumulator | Hydraulic + nitrogen charge | Dedicated discharge sequence | Pressure log, valve tagged |
| Conveyor incline section | Gravitational | Belt tension pin + chock | Chock load-tested by hand |
| Preheater cyclone shell | Thermal | Cool-down period + fuel isolation | Contact thermometer under 50°C |
What a digital hydraulic LOTO permit catches that paper misses
The difference between a paper hydraulic LOTO form and a digital, asset-specific permit rarely shows up on a normal day. It shows up the day a gauge reading was skipped, a block was never load-tested, or a second verifier signed off without actually walking the equipment — and there is no record to show which step failed.
A generic hydraulic LOTO box gets checked once for the whole asset, gauge readings are written from memory after the fact, and there is no record of which specific accumulator or cylinder was actually bled down before the second signature was collected. When an auditor or investigator asks which point was verified and when, the paper trail usually cannot answer.
Each hydraulic point on the asset is a separate step with a required gauge-reading entry and a mandatory second-verifier signature before the permit can close. The completed record attaches to the work order and the asset, ready for an OSHA or MSHA audit request, and the app will not let the permit close if any step is left blank.
The gap between the two is not effort — a well-run paper process can still get every step right on any given day. The gap is consistency across every shift, every crew, and every asset, which is exactly what a digital permit is built to hold steady even when the day is busy and the crew is short.
Replace the generic hydraulic checkbox with a real verification trail.
Build asset-specific isolation steps for every cooler, mill, and kiln inlet point, with gauge readings, blocks, and second-verifier sign-off captured in the mobile app.
Rolling out hydraulic LOTO across a multi-line plant
Moving from a generic hydraulic checkbox to asset-specific, verified permits does not have to happen all at once. Most plants sequence the rollout by risk, starting with the assets that carry the highest stored-energy exposure and the most maintenance hours.
Inventory every hydraulic and blocked-energy point
Walk each line with maintenance and safety together, and map every hydraulic cylinder, accumulator, spring return, and gravity-loaded component to its asset record — including points that current written procedures may not mention at all.
Rank assets by exposure and maintenance frequency
Cooler grate rams and mill roller clamps typically rank highest, since they combine large stored forces with frequent, hands-on maintenance work performed directly in the load path — while lower-frequency assets can follow in a later phase.
Build the asset-specific digital permit in the CMMS
Convert each mapped point into its own verification step with a required gauge entry, a mechanical block confirmation, and a second-verifier signature field, so the permit simply cannot be closed until every step is complete.
Train, pilot, and review the first outage cycle
Run the new permit on one line during a scheduled outage, review every completed record with the safety team, and correct any step that technicians found unclear or slow before extending it plant-wide across every remaining line.
Hydraulic and blocked energy LOTO — answered
What counts as blocked energy under OSHA 1910.147?
Blocked energy is any stored hydraulic, pneumatic, spring, or gravitational energy that remains in a system after the primary power source is isolated. A locked-out breaker does not release it, so it needs its own bleed-down and gauge-verification step written into the permit as a separate task. Start a free trial to build this into your permits.
Why is a locked hydraulic valve not enough on its own?
A closed valve can leak internally or be bumped open, and it gives no visible confirmation that pressure has actually dropped to zero. A gauge reading plus a mechanical block or chock is what turns a closed valve into a verified isolation the crew can actually trust.
How often do cooler grate hydraulics need a dedicated bleed-down step?
Every time a technician opens a grate segment for plate replacement or inspection, regardless of how routine the task feels or how many times it has been done before. Skipping the bleed-down because "it's just a quick check" is how residual ram pressure causes a segment lurch.
Can a digital LOTO permit be tailored per asset instead of one generic form?
Yes — a CMMS-based permit can carry a separate step, gauge field, and block confirmation for each energy point on that specific asset, so a cooler ram and a mill roller clamp are never covered by the same generic checkbox. Book a demo to see it configured for your asset register.
What should a hydraulic LOTO audit trail include?
At minimum: the specific isolation points identified, gauge readings logged at zero, the mechanical block or chock confirmed, an attempt-to-start test result, and a second authorized employee's independent sign-off, all retained per OSHA recordkeeping requirements for at least three years.
Stop letting hydraulic pressure hide behind an electrical lock.
Deploy asset-specific hydraulic and blocked-energy LOTO permits across your cooler, mill, and kiln inlet points in under two weeks.
Free 14-day trial — no credit card