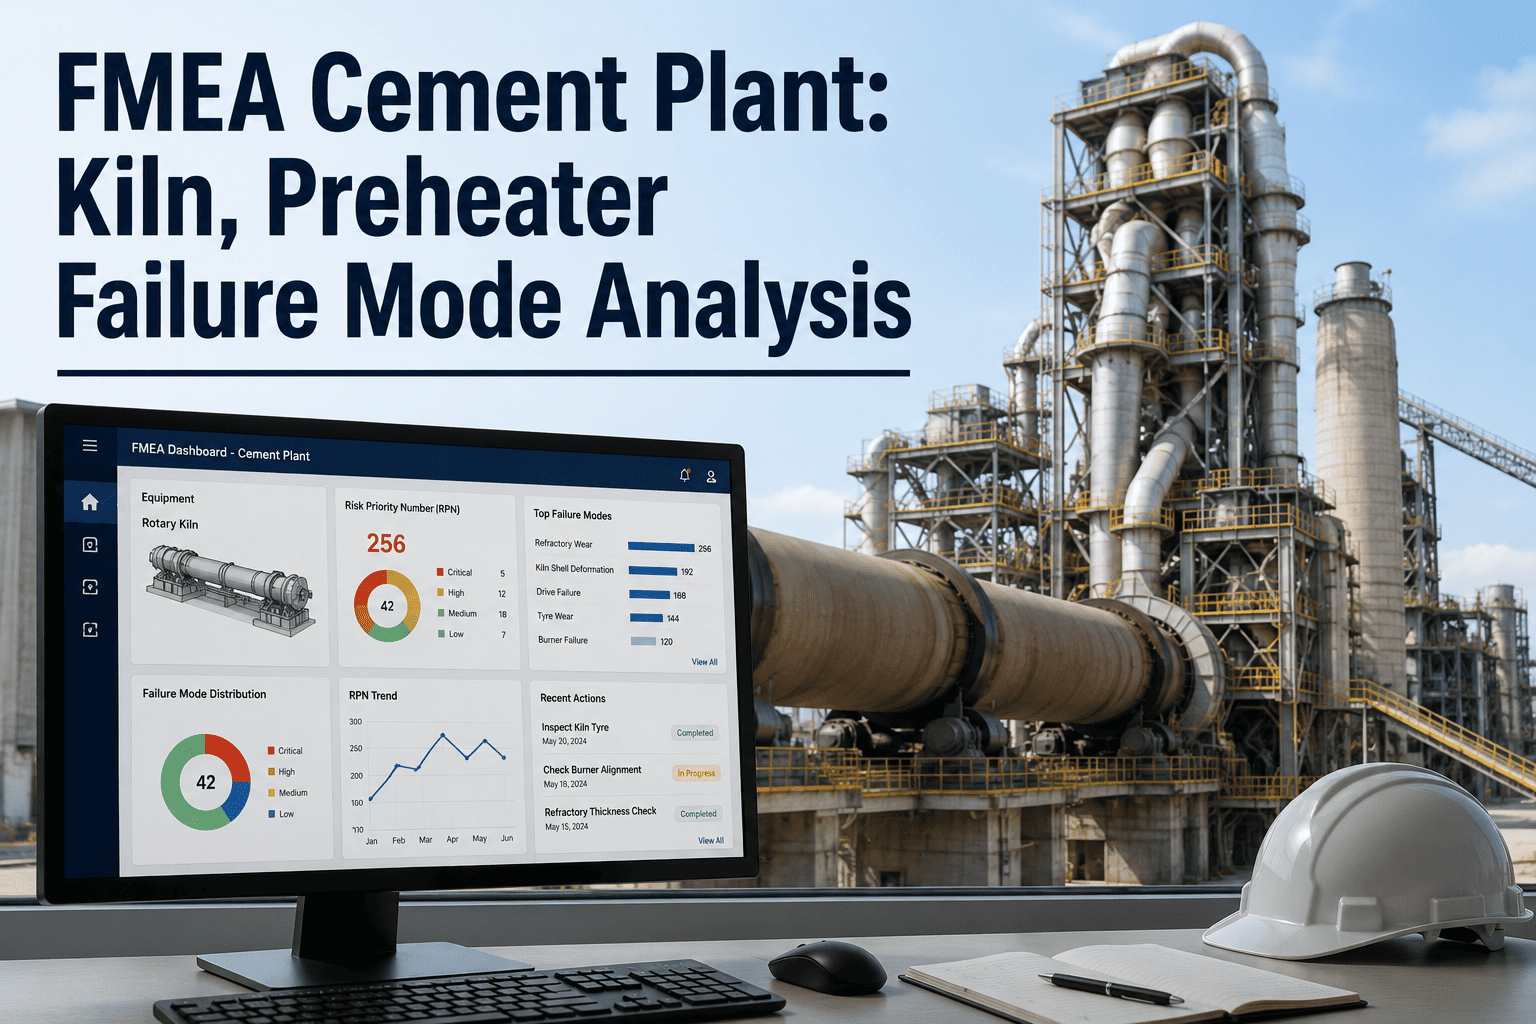
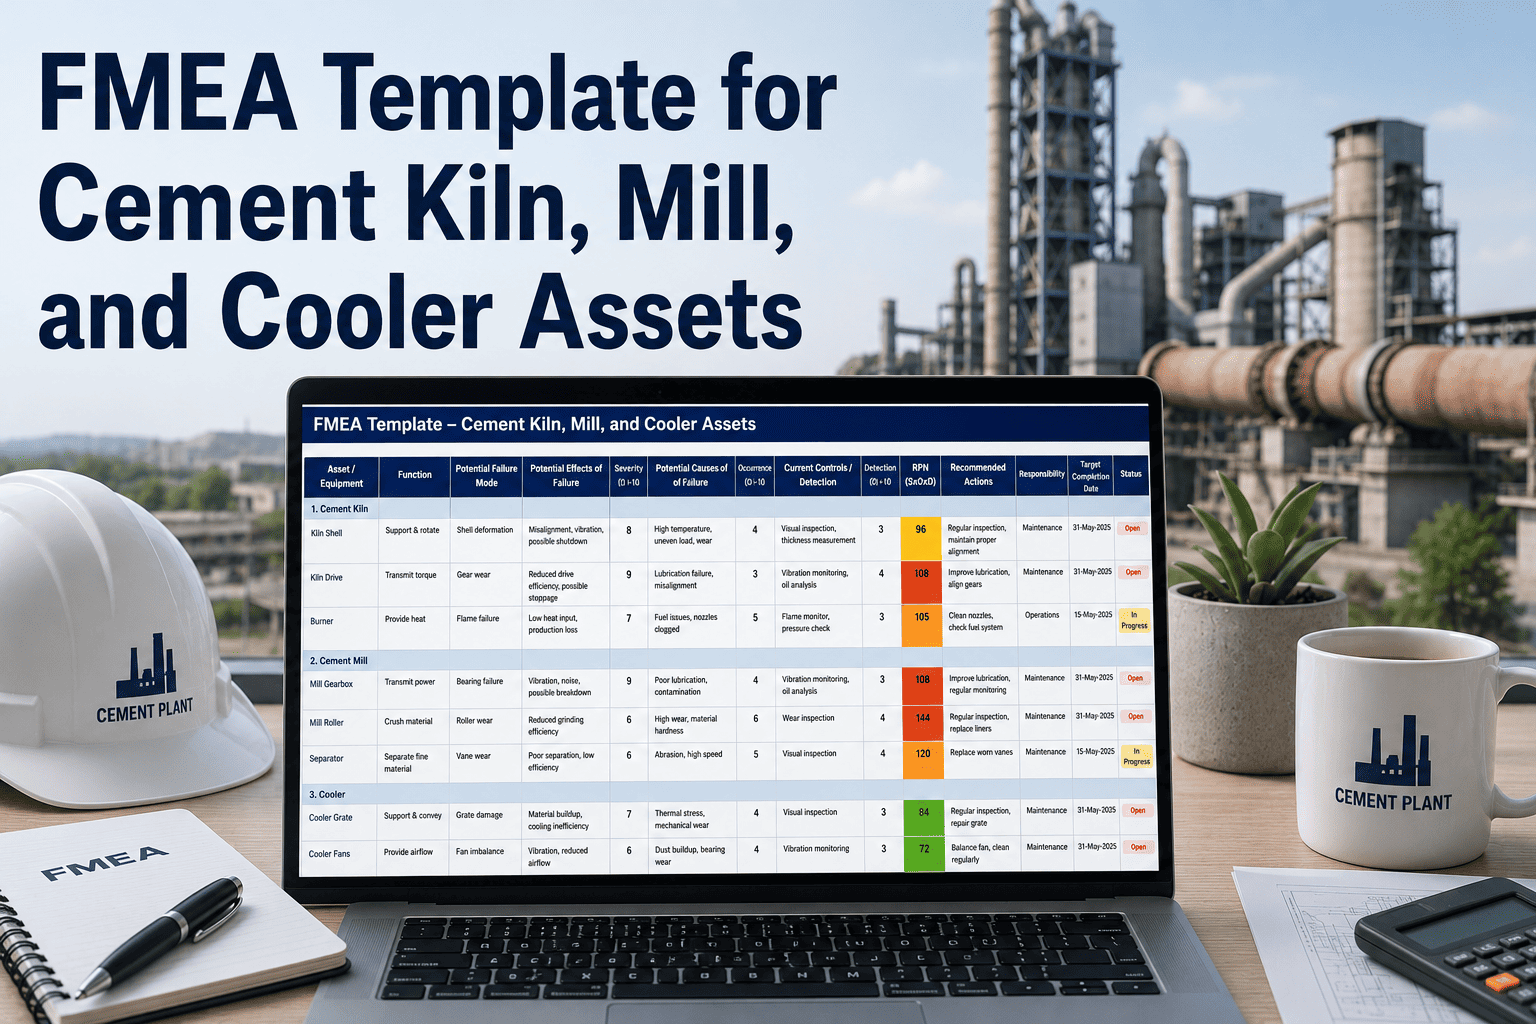
A cement plant FMEA is the difference between a reliability programme that prevents the next $540,000 unplanned outage and a binder of paperwork that gets dusted off after the kiln has already stopped. Done right, Failure Mode and Effects Analysis turns tribal knowledge about which bearings, refractory zones, grate plates, and cyclone walls fail most painfully into a scored, prioritised, CMMS-routed action list that your reliability engineer, maintenance planner, and plant manager all read the same way. Done wrong, it produces a beautiful spreadsheet that changes nothing on the shop floor — because the high-RPN actions never become work orders and the document goes stale within six months. Oxmaint anchors the entire FMEA lifecycle inside the CMMS so every mitigation is a live work order, not a forgotten cell in a workbook.
FMEA · CEMENT PLANT ASSETS
Severity × Occurrence × Detection — built for kilns, mills, coolers, and preheaters
A complete cement-plant FMEA framework with RPN scoring rubrics, asset-by-asset failure mode worksheets, mitigation routing into CMMS work orders, and the audit trail your reliability programme actually needs.
WHY FMEA IS A CEMENT PLANT NECESSITY
The cost of getting prioritisation wrong on a 5,000 TPD kiln line
Cement assets do not fail democratically. A trunnion bearing failure on the rotary kiln stops the entire plant for 5 to 14 days. A grate plate breakthrough in the cooler creates red rivers that damage downstream equipment within hours. A cyclone wall coating that goes untracked builds 5 to 15 mm a week and chokes preheater gas flow in 3 to 6 weeks. Without FMEA, every failure mode looks equally urgent — and the team spends two hours fixing a $200 issue while a $540,000 failure brews next door. The RPN ranking forces objective triage: the highest-consequence, highest-frequency, lowest-detection failures get the work order first, every time.
$18K–$45K
Hourly loss from a cooler-driven kiln trip
270 RPN
Highest scored kiln failure in published FMECA studies
80% of bearings
Of ball mill bearing failures preventable with structured FMEA
12 months
Review cycle world-class reliability teams enforce
SCORING RUBRIC
Calibrate Severity, Occurrence, and Detection the same way every time
The fastest way to break an FMEA programme is to let three different reliability engineers score the same failure mode three different ways. The rubric below is the cement-plant-specific anchor your team scores against, every session, every asset.
| Score |
Severity (S) |
Occurrence (O) |
Detection (D) |
| 9–10 |
Catastrophic kiln stop, safety event, regulatory exposure |
Almost certain within a campaign cycle |
Cannot detect before failure occurs |
| 7–8 |
Multi-day production loss, major equipment damage |
High likelihood within annual cycle |
Detected only by manual inspection at shutdown |
| 5–6 |
Single shift production loss, recoverable repair |
Occasional, seen once every 2–3 campaigns |
Detected by operator rounds or periodic checks |
| 3–4 |
Minor degradation, throughput or quality impact |
Rare, isolated event in plant history |
Detected by continuous condition monitoring |
| 1–2 |
Negligible operational impact |
Highly improbable in this asset configuration |
Detected automatically by sensor with alert routing |
Critical rule: any failure mode with Severity 9 or 10 demands an action regardless of total RPN — because the consequence is unacceptable even at low frequency or with strong detection.
FMEA WORKSHEETS — FOUR CEMENT ASSETS
Top failure modes scored across the four highest-impact asset families
Every cement plant FMEA programme starts here: the rotary kiln, the raw and cement mills, the clinker cooler, and the preheater tower. The worksheets below capture the highest-RPN failure modes our reliability research consistently surfaces across cement plants, with the mitigation work order that closes each one out.
01
ROTARY KILN
Heart of the pyroprocessing line
Refractory brick burning-zone failure
RPN 270
Mitigation: Shell scanner thermal trending, zone-by-zone thickness logging, scheduled reline at 65% original thickness.
Trunnion bearing seizure
RPN 240
Mitigation: Vibration sensor with auto-alert to CMMS, weekly lubrication PM, oil analysis quarterly.
Girth gear tooth wear
RPN 168
Mitigation: Quarterly backlash measurement, lubricant spray pattern verification, alignment check each campaign.
02
RAW & CEMENT MILL
Grinding circuit reliability
Mill bearing lubrication starvation
RPN 252
Mitigation: Bearing temperature alarm at 65°C, lube system flow sensors, monthly oil sampling with ISO 4406 cleanliness check.
Liner bolt fatigue and loosening
RPN 192
Mitigation: Torque verification at every liner change, shell sound check weekly, mill vibration trending.
Gearbox lubrication failure
RPN 144
Mitigation: Sight glass checks per shift, oil temperature continuous logging, semi-annual filter replacement PM.
03
CLINKER COOLER
Grate, fans, and heat recovery
Grate plate breakthrough — Zone 1
RPN 245
Mitigation: Wear-depth measurement every shutdown, undergrate pressure trending, RUL projection from AI wear model.
Cooling fan bearing failure
RPN 224
Mitigation: Monthly vibration analysis, amp-draw trending, blade wear inspection quarterly.
Hydraulic drive system pressure loss
RPN 175
Mitigation: Monthly pressure and flow check, hydraulic oil sampling, accumulator nitrogen verification.
04
PREHEATER TOWER
Cyclones, ducts, and precalciner
Cyclone wall coating and blockage
RPN 256
Mitigation: Weekly internal camera survey, air-cannon firing log, draft pressure differential trending.
Riser duct refractory spalling
RPN 168
Mitigation: Shell scanner thermal anomaly alerts, scheduled patch repair during minor outages, alkali analysis quarterly.
Tertiary air duct erosion
RPN 140
Mitigation: UT thickness scans at access ports, dust loading measurement, refractory grade audit each campaign.
PRIORITY MATRIX
From RPN score to CMMS work order — the routing logic that keeps actions alive
EMERGENCY
RPN ≥ 200 OR S = 9–10
Immediate work order with planner ownership, daily standup tracking, completion target within 14 days.
HIGH
RPN 121 to 199
Work order generated, prioritised in next planning cycle, mitigation closed within current campaign window.
MEDIUM
RPN 80 to 120
Scheduled into upcoming PM cycle, condition-monitoring task added to operator rounds.
LOW
RPN below 80
Logged in FMEA register, reviewed at the annual update, no immediate work order required.
FROM FMEA SPREADSHEET TO LIVE CMMS
Stop letting high-RPN mitigations die in a workbook nobody opens
Oxmaint turns every FMEA worksheet row into a tracked work order with an owner, a due date, and a closeout record. Severity, Occurrence, and Detection scores live on the asset record alongside vibration data, refractory thickness, and shutdown history.
FMEA PROGRAMME LIFECYCLE
Six checkpoints that keep a cement-plant FMEA alive year after year
01
Asset hierarchy scoping
Define the boundary — by asset family, by line, by criticality — and load the structured hierarchy into CMMS. Every FMEA row anchors to a real equipment record.
02
Cross-functional team session
Reliability engineer, maintenance technicians, operators, and process specialists score every failure mode together. Field knowledge fills the gaps engineering drawings miss.
03
RPN calculation and ranking
Multiply S × O × D for each mode, sort the worksheet by descending RPN, and flag every Severity 9 or 10 line regardless of total score.
04
Mitigation work order generation
Every action above the RPN threshold becomes a CMMS work order with named owner, target completion date, and acceptance criteria. No floating Excel actions.
05
Post-mitigation re-score
Once each action is closed, re-score the failure mode and document the RPN reduction. This is the evidence trail that proves the programme is working.
06
Annual review and trigger updates
Refresh the FMEA every 12 months and after any unplanned failure event. New equipment, new fuels, new throughput rates all change the scoring.
PROGRAMME PITFALLS
Four ways a cement plant FMEA quietly stops working
PITFALL 01
No technicians in the scoring room
An FMEA built only by reliability engineers misses the failure modes that show up in actual operation. Operators and technicians carry the field memory engineering drawings cannot.
PITFALL 02
Actions live in Excel, not CMMS
If the mitigation column is a workbook cell instead of a work order, nothing happens. The action needs an owner, a due date, and a closeout record inside the maintenance system.
PITFALL 03
Severity 9 ignored because RPN is low
A rare but catastrophic event still needs action. Any failure mode with Severity 9 or 10 requires mitigation regardless of how low the occurrence or detection scores push the total RPN.
PITFALL 04
Document goes stale within six months
Throughput changes, alternative fuels are introduced, new equipment is installed — and the FMEA does not update. Annual review with event-driven refresh keeps the worksheet accurate.
RELIABILITY QUESTIONS
What cement reliability engineers ask before they restart their FMEA programme
How do we calculate RPN in cement plant FMEA?
Multiply Severity × Occurrence × Detection, each rated 1 to 10, giving a 1 to 1,000 range. Most plants set the action threshold at 80 to 100, plus any failure mode with Severity 9 or 10 regardless of total score.
Start a free trial to build the scoring sheet inside your CMMS.
Which cement plant assets should be FMEA'd first?
Start with the rotary kiln, raw and cement mills, clinker cooler, and preheater tower. These four asset families drive 80% of unplanned downtime and 100% of campaign-ending failures.
How often should we update a cement plant FMEA?
Annual full review, plus an event-driven refresh after every unplanned failure of significance. Plant conditions change — fuels, throughput, equipment age — and a stale FMEA misleads the planning team.
How does FMEA connect to actual maintenance work orders?
Every mitigation above the RPN threshold becomes a CMMS work order with owner, due date, and acceptance criteria. The FMEA worksheet and the work order list reference the same asset record.
Book a demo to see this routing live on a cement asset.
Who should be in the FMEA scoring session?
A cross-functional team: reliability engineer, maintenance planner, lead technicians, operators familiar with the asset, and a process specialist. Without field operators the scoring drifts toward theoretical failure modes that rarely actually occur.
YOUR FMEA, BACKED BY A CMMS
Run your next FMEA cycle inside the platform that already manages your cement assets
Oxmaint gives reliability teams asset hierarchies pre-built for cement plants, RPN scoring fields on every failure mode, automatic mitigation work order generation, and post-action re-scoring with full audit trail. The same CMMS that runs your daily work orders runs your FMEA programme.