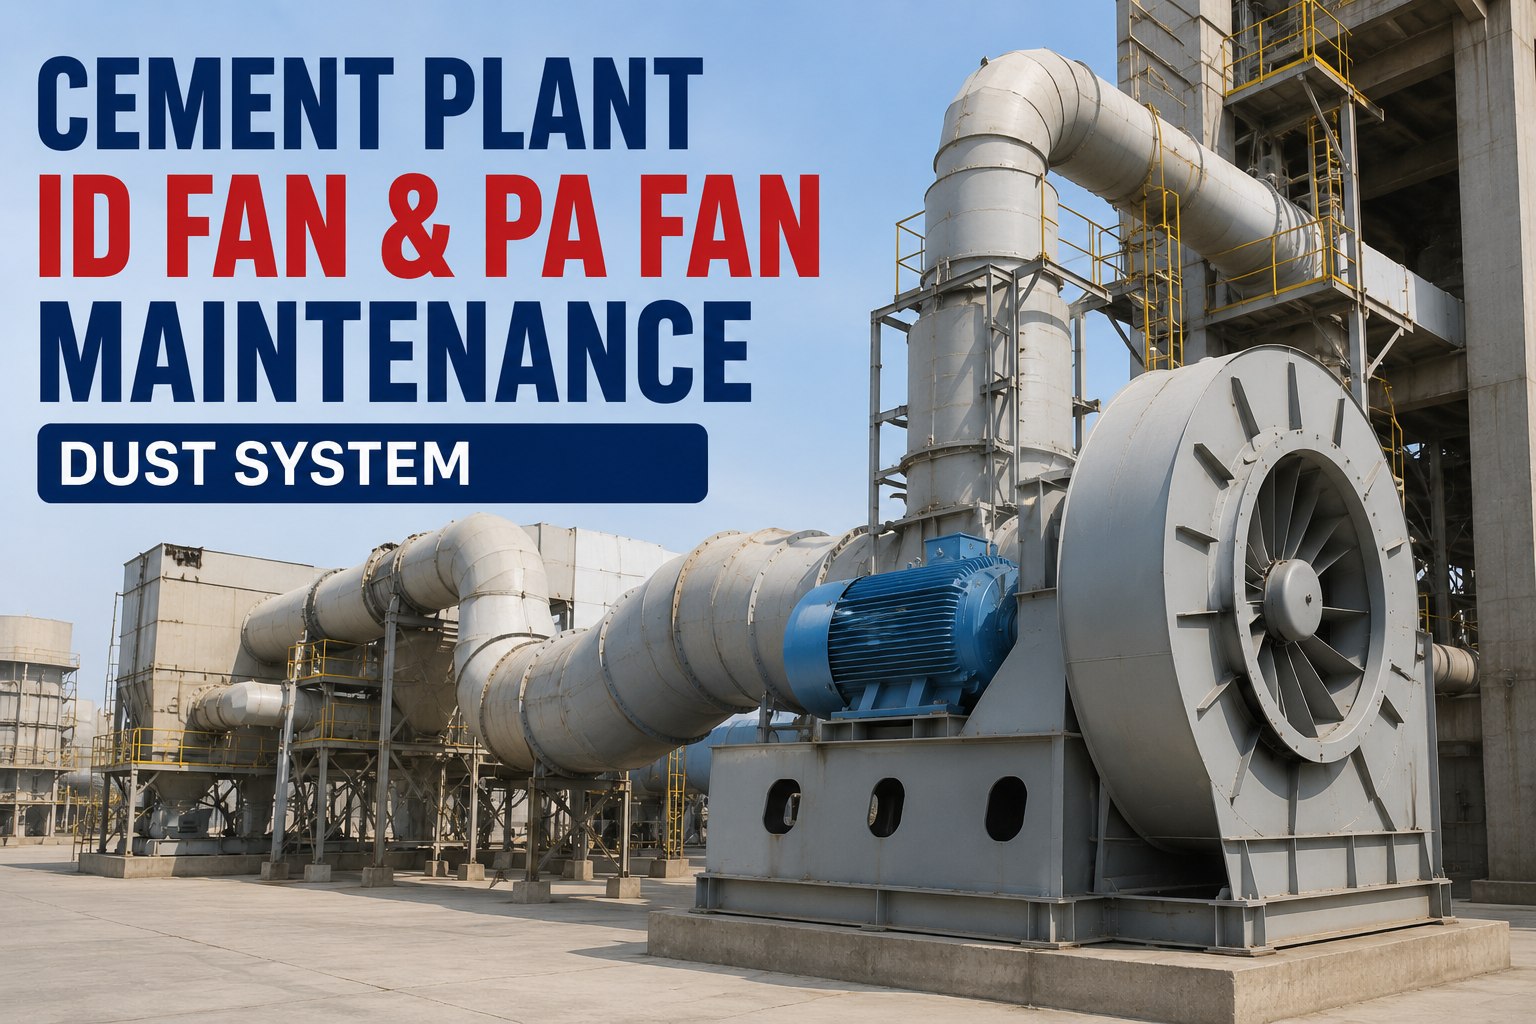
Cement plants lose an estimated 8–12% of annual clinker capacity to unplanned fan outages, with ID fans and PA fans accounting for the majority of critical air-handling failures across the kiln and cooler systems. When an ID fan trips on vibration or a PA fan loses clearance due to blade erosion, the entire combustion draft balance collapses within minutes — stalling kiln production, choking dust collection, and wasting heat recovery surface. A structured cement plant ID fan and PA fan maintenance program, anchored in CMMS-driven preventive tasks, dynamic balancing, and wear-plate replacement cycles, can extend mean time between fan failures from 9 months to over 30 months. Build your reliability program with our Start Free Trial and convert fan maintenance from reactive firefighting into a planned, measurable asset.
Are your ID and PA fans quietly killing kiln draft — one gram of imbalance at a time?
ID fans and PA fans move the largest air volumes in any cement plant. A single gram of dust buildup on an impeller can spike vibration by 20%, cut bearing life in half, and shut down kiln draft within a shift. This guide turns fan PM into a controlled, CMMS-driven reliability program.
The hidden cost of fan neglect in cement dust systems
In a typical 5,000 TPD kiln, the ID fan handles 600,000–900,000 m³/h of hot, dust-laden gas at 280–350°C. Every hour of unplanned fan downtime translates to roughly $18,000–$35,000 in lost clinker production.
A 2-million-TPA cement plant in Gujarat was replacing two kiln ID fan impellers every 14 months and logging 6 vibration trips per quarter. After implementing a CMMS-scheduled PM cycle — 30-day bearing inspections, 90-day dynamic balancing, and annual wear-plate replacement — impeller life extended to 38 months, quarterly trips dropped to zero, and the plant recovered an estimated $340,000 in avoided downtime costs in year one alone.
ID fan and PA fan PM checklist by frequency
Tiered preventive maintenance is the backbone of fan reliability. Schedule these tasks in your CMMS to capture 80% of failure modes before they escalate.
Walk-down & condition check
- Log vibration readings at drive and non-drive bearings; flag any trend exceeding 4.5 mm/s RMS
- Record bearing temperature; alarm if above 80°C for ID fan or 75°C for PA fan
- Inspect inlet damper position and actuator response time — must reach full open in under 12 seconds
- Check for abnormal acoustic signatures, blade-pass frequency changes, or housing resonance
Lubrication & sealing
- Re-grease bearings with correct NLGI-3 lithium complex grease — typically 30–60g per bearing per cycle
- Inspect shaft seal condition and clearance; target leakage below 2% of design flow
- Inspect coupling alignment using laser alignment — angular tolerance under 0.05 mm/100 mm
- Drain and inspect oil-lubricated bearing housings for water contamination and particulate
Balancing & erosion inspection
- Perform in-situ dynamic balancing — target residual unbalance below ISO 1940 G2.5 grade
- Measure wear-plate thickness with ultrasonic gauge; replace if wall loss exceeds 40% of original
- Inspect blade leading edges for erosion, pitting, and dust buildup — clean and re-profile as needed
- Verify inlet box and housing inspection doors seal properly — no false air ingress above 5%
Major overhaul & rebuild
- Remove impeller, perform NDT crack testing on blades and hub welds — dye penetrant or MPI
- Replace wear plates and apply hardfacing overlay on blade leading edges (WC-Co or chromium carbide)
- Replace both bearings, seals, and labyrinth rings; shop-balance impeller to ISO 1940 G1.0
- Realign full drive train, run acceptance test at full load, and archive baseline spectra in CMMS
ID fan vs PA fan maintenance comparison
ID fans and PA fans operate under very different dust loads, temperatures, and pressure profiles — their PM schedules must reflect that. Use this reference table to calibrate your CMMS task intervals.
| Maintenance Task | ID Fan (Kiln) | PA Fan (Raw Mill / Coal) | CMMS Trigger |
|---|---|---|---|
| Vibration monitoring | Continuous (online sensor) | Weekly walk-down + monthly handheld | Auto-alarm at 4.5 mm/s RMS |
| Bearing lubrication | Every 2,000 running hours | Every 3,000 running hours | Runtime meter trigger |
| Dust buildup cleaning | Quarterly (during kiln stop) | Monthly (high dust load) | Calendar + stop-window sync |
| Dynamic balancing | Every 90 days in-situ | Every 180 days in-situ | Calendar + vibration trend |
| Wear plate replacement | 12–18 months | 18–24 months | Ultrasonic thickness reading |
| Impeller NDT & rebuild | Every 24 months | Every 36 months | Calendar + performance decay |
| Bearing full replacement | Every 36–48 months | Every 48–60 months | L10 life + vibration history |
The payback formula of a CMMS-driven fan program
Quantify the return on preventive maintenance before you commit budget. The formula below models the annual savings of moving a critical fan from reactive to CMMS-scheduled PM.
Building the CMMS-driven fan reliability program
A fan reliability program lives or dies on the quality of its CMMS backbone. These four numbered workstreams convert scattered tasks into a closed-loop system aligned with ISO 55000 asset management principles.
Asset hierarchy & criticality ranking
Register every ID fan, PA fan, and auxiliary dust-system fan in the CMMS with a structured hierarchy: plant → kiln line → fan system → component. Rank criticality by production impact — kiln ID fans typically score A1, raw mill PA fans A2, cooler exhaust fans B1. Criticality drives PM frequency, spare-parts stocking, and condition-monitoring depth.
Condition-based triggers & sensors
Wire vibration, temperature, and bearing-shock sensors into the CMMS as live data streams. Configure auto-generated work orders when vibration crosses 4.5 mm/s RMS or bearing temperature exceeds 80°C. This converts time-based PM into condition-based maintenance, cutting unnecessary inspections by 35% while catching real defects earlier.
Standardized PM checklists & procedures
Attach digital checklists to every PM work order — bearing grease quantity, torque specs, balancing acceptance grade, wear-plate thickness thresholds. Eliminate paper SOPs. Field technicians complete tasks on mobile devices, capture photos of erosion or damage, and feed findings back into the asset record for trend analysis.
Spare parts & rebuild planning
Link impellers, wear plates, bearings, and seals to the fan asset record with min/max stock levels and lead times. A CMMS triggers reorder when stock hits minimum, ensuring a spare impeller is always available for annual overhaul. Plan major rebuilds 90 days ahead using performance-decay trends rather than reacting to failures.
What a disciplined fan PM program delivers
Plants that implement CMMS-driven ID and PA fan maintenance consistently report measurable gains across availability, cost, and safety. Here is what the data shows.
"After 14 months on the CMMS fan program, our kiln ID fan vibration trips dropped from 6 per quarter to zero. The 90-day dynamic balancing cycle paid for itself in the first saved outage."
"Wear-plate replacement was always reactive for us. Now the ultrasonic thickness readings trigger automatic work orders at 40% wall loss. We have not had an unplanned PA fan failure in 22 months."
Cement plants that run CMMS-scheduled fan PM achieve 92%+ availability on critical ID and PA fans, compared to 78% industry average for reactive programs.
Ready to stop fan failures before they stop your kiln?
Deploy a CMMS-driven PM program for your ID fans and PA fans in days — not months. Start your free trial or book a 30-minute demo with a cement reliability expert.
Cement plant ID fan and PA fan maintenance — answered
The five questions cement maintenance teams ask most about fan PM, balancing, dust buildup, and CMMS integration.
How often should I dynamically balance an ID fan impeller in a cement plant?
For kiln ID fans operating in dust-laden gas, perform in-situ dynamic balancing every 90 days and after every impeller cleaning or blade repair. Target ISO 1940 grade G2.5 for acceptance. If vibration trends above 3.5 mm/s RMS between scheduled cycles, trigger an interim balance. Plants following this protocol typically extend impeller life from 14 to 36+ months.
What is the acceptable vibration limit for cement plant ID and PA fans?
Per ISO 10816-3, rigidly mounted cement fans should stay below 4.5 mm/s RMS in zone B (acceptable for long-term operation). Above 7.1 mm/s RMS, shut down immediately. PA fans on coal grinding duty often run slightly higher due to rotor dust load — set your CMMS alarm at 4.0 mm/s to catch buildup early before it becomes a trip. You can configure these thresholds in a CMMS like Start Free Trial with auto-triggered work orders.
How do I remove dust buildup from fan blades without removing the impeller?
Schedule cleaning during planned kiln stops every 30–90 days depending on dust load. Open inspection doors, use compressed air lances at 6–8 bar, and manually scrape accumulated buildup from blade concave surfaces and wear plates. Always re-check dynamic balance after cleaning — removing uneven buildup shifts the center of gravity and can introduce 1x RPM vibration if left uncorrected.
When should wear plates be replaced vs. hardfaced?
Measure wear-plate thickness with an ultrasonic gauge quarterly. If wall loss is under 25%, apply chromium-carbide or tungsten-carbide hardfacing overlay to extend life. If wall loss exceeds 40% of original thickness, replace the wear plate entirely — hardfacing on thin plates risks warping and bond failure. Stock replacement plates in your CMMS spare-parts register with a 12-month lead time for custom impellers.
Can a CMMS really prevent fan failures, or is it just a scheduling tool?
A modern CMMS does far more than scheduling. It captures vibration and temperature trends, auto-generates work orders when thresholds are breached, tracks bearing grease cycles against runtime hours, and maintains a complete failure history per asset. Plants using CMMS-driven fan PM report 40–50% fewer unplanned fan outages. To see the workflow in action, Book a Demo and we will map it to your fan inventory.
Turn fan maintenance into measurable kiln uptime
Join cement plants using CMMS-driven PM to extend ID and PA fan life by 3×, cut vibration trips to zero, and recover hundreds of thousands in avoided downtime — every year.
Free 14-day trial · No credit card