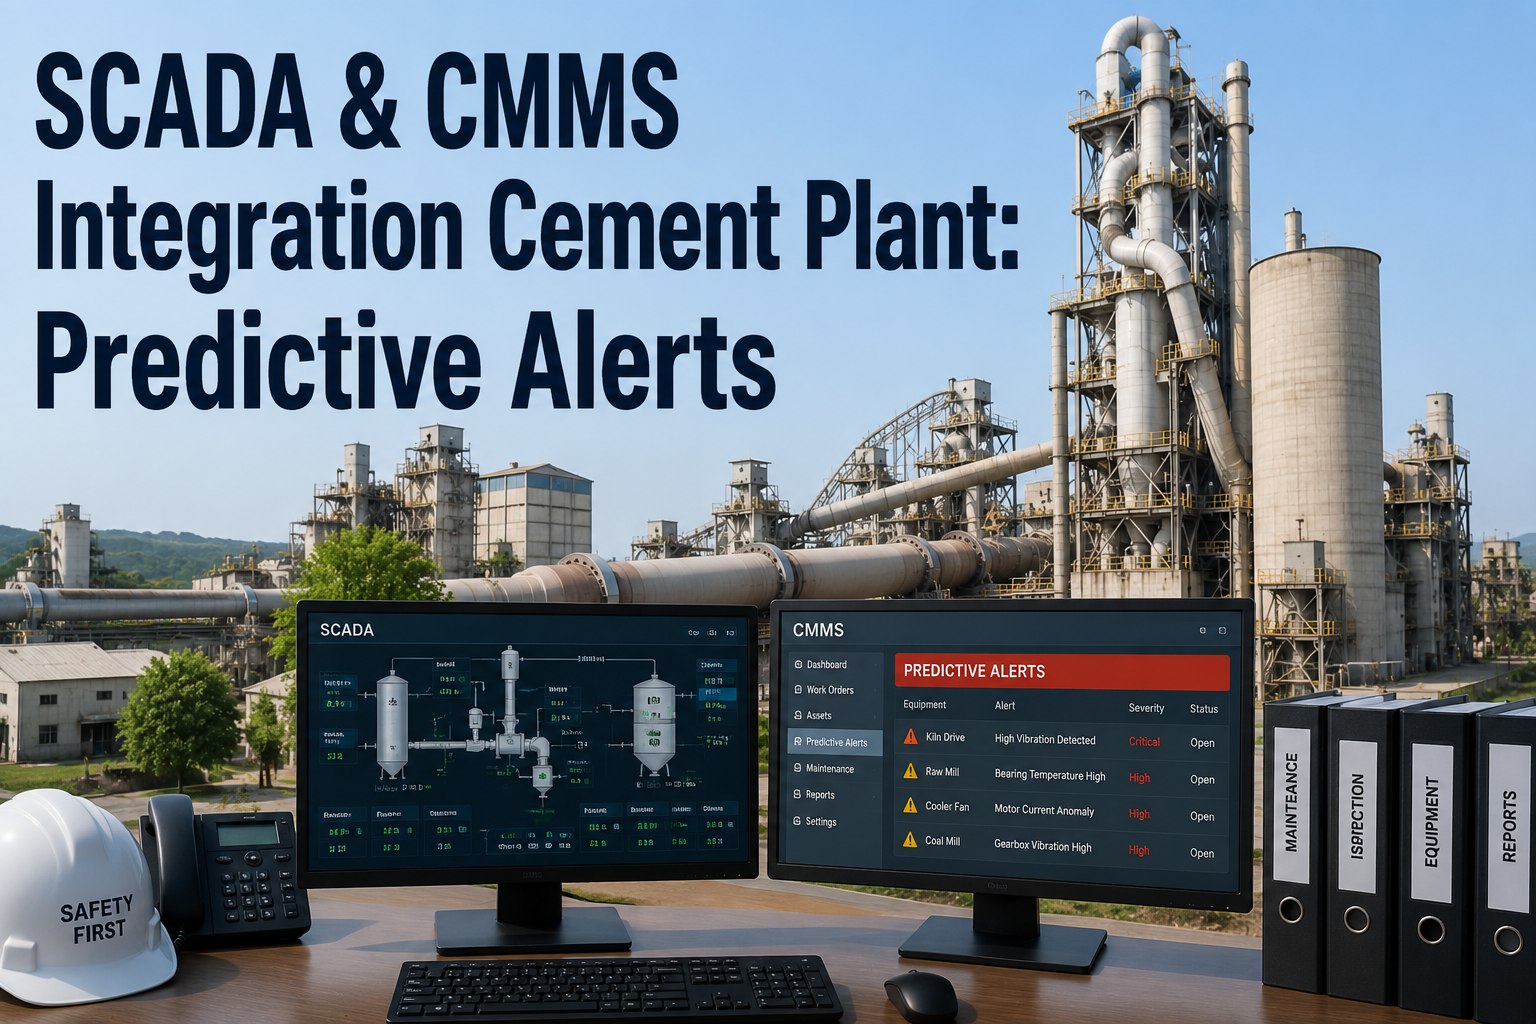
A cement plant predictive maintenance pilot is the inflection point where PdM either earns its budget or quietly becomes another shelf project. Industry data consistently shows that cement producers lose 5–7% of annual revenue to unplanned downtime, with a single kiln outage often costing $80,000–$120,000 per day in lost clinker output. The pilots that succeed share a common architecture: a tightly scoped asset, the right sensor mix, a clear 12-week evaluation window, and KPIs the CFO can verify without an engineering translator. This guide lays out the exact pilot setup that has repeatedly produced the proof case for enterprise-wide PdM investment — and you can put it into motion today by signing up for a Start Free Trial of the Oxmaint CMMS platform.
Will your 12-week pilot produce a defensible ROI — or quietly die on the shelf?
A well-structured cement PdM pilot detects the one bearing, one fan imbalance, or one refractory hot-spot that pays for the entire program. Here is the setup that gets plant managers, reliability engineers, and finance aligned before the first sensor ships.
Pick one critical asset — not the whole plant
The pilots that scale begin with a single high-criticality asset where downtime is expensive, failure modes are measurable, and the operations team already trusts the instrumentation. In cement, that is almost always the kiln or its closest support equipment.
Rotary Kiln · Main Drive & Tire
A kiln stoppage idles the entire pyro line, the cooler, and frequently the raw mill. One shell-tire creep anomaly or girth-gear vibration trend caught early can prevent a 24–48 hour unscheduled outage.
Clinker Cooler Grate
High vibration, heavy dust, and repeated grate-plate failures make the cooler the second-most common pilot target. Portable tri-axial sensors catch bearing wear 3–6 weeks before seizure.
Cement Mill · Slide Shoe Bearing
Lubrication degradation and shoe-temperature drift are textbook PdM wins. Oil debris plus temperature trend catches 70%+ of failure modes before white-metal damage.
Preheater ID Fan
Fan imbalance from dust buildup and bearing wear shows in spectral data long before vibration alarms. A 200 kW fan running at 1,180 RPM is a low-cost, high-signal pilot scope.
Match each failure mode to the right sensor signal
Pilot failures usually trace back to the wrong transducer on the wrong failure mode — accelerometers where oil analysis belonged, or thermography where acoustics would have caught the bearing. Use the map below before placing a single purchase order.
| Failure Mode | Primary Sensor | Sampling | Detection Lead Time | Indicative Cost / Point |
|---|---|---|---|---|
| Bearing spall / inner-race fatigue | Tri-axial accelerometer | Continuous, 25.6 kHz | 3–8 weeks | $180–$420 |
| Girth-gear tooth wear / pitting | Wireless vibration + acoustic emission | Hourly snapshots | 6–12 weeks | $600–$1,100 |
| Refractory hot-spot / brick thinning | Infrared line-scanner + shell thermocouples | Continuous, 1 Hz | 4–10 weeks | $2,400–$5,800 |
| Lube oil degradation / debris | Online particle counter + ferrous density | 15-min intervals | 2–6 weeks | $900–$2,200 |
| Motor stator winding fault | Electrical signature (MCSA / ESA) | Daily 60-second capture | 4–12 weeks | $1,500–$3,400 |
| Fan rotor imbalance / buildup | Wireless tri-axial + tachometer | Continuous, 12.8 kHz | 1–4 weeks | $240–$520 |
For a 12-week pilot, do not exceed 12–16 monitored points. Anything wider and the reliability team cannot investigate every alert to the depth needed for a CFO-grade proof case.
The four-phase pilot clock that produces a verdict
Pilots that run open-ended lose executive sponsorship by week six. Lock the timeline below before kickoff — each phase has a hard exit deliverable that feeds the next.
Baseline Data Capture
Mount sensors, configure the CMMS asset hierarchy, and collect steady-state baselines under normal kiln load (75–95% of rated throughput). Tag every data gap and exclude start/stop transients.
Deliverable: Baseline vibration & thermal signatures for all 12–16 points.Threshold Tuning
Set ISO 10816 alarm bands, train the anomaly-detection model on baseline variance, and tune alerting so false-positive rate stays under 10%. Inspect every yellow alert within 48 hours.
Deliverable: Calibrated alarm matrix approved by reliability lead.Live Detection & Intervention
PdM-driven work orders go live in the CMMS. Every triggered inspection, oil change, or planned outage is logged with cost avoidance calculated against the prior 12-month reactive baseline.
Deliverable: 3–5 verified early-warning catches with documented savings.ROI Verdict & Scale Plan
Compile the pilot scorecard: MTBF delta, unplanned downtime hours avoided, maintenance cost per tonne, and verified cost avoidance. Present the enterprise rollout roadmap with a 24-month payback projection.
Deliverable: CFO-ready pilot report + expansion budget request.Five KPIs that make or break the pilot verdict
If the pilot report shows only vibration trends and alarm counts, finance will not fund Phase 2. Every KPI below is tied to a dollar figure or a tonnes-per-hour figure the plant already tracks.
Unplanned Downtime Avoided
Hours of unplanned kiln/mill stoppage prevented by early-warning interventions, benchmarked against the trailing 12-month average for the same asset.
Mean Time Between Failures
Delta between pilot-period MTBF and the prior 12-month baseline on the pilot asset. Target a 15–30% improvement by week 12.
Maintenance Cost / Tonne
Total maintenance spend on the pilot asset divided by clinker or cement tonnes produced. The single number a plant manager will quote in the next ops review.
Verified Cost Avoidance
Dollar value of prevented outages calculated from lost-production rate, labor, and spare-parts rush premiums. Requires sign-off from operations and finance.
False-Positive Rate
Percentage of PdM alerts that produced no actionable finding on inspection. Above 10% the team loses trust; above 20% the pilot is effectively dead.
Work-Order Compliance
Share of PdM-generated work orders completed within the prescribed response window. Tracks whether the maintenance team is actually acting on the data.
The payback formula pilots live or die by
Before sensors ship, plant leadership should agree on the calculation below. It removes the "is PdM worth it?" debate at week 12 and replaces it with a number.
A 180-asset plant, $42K/yr reactive spend on one kiln line
- $42,000 reactive maintenance spend on kiln #1
- 38 hrs unplanned downtime, prior year
- $312K lost production at $8.2K/hr
- 2 major in-situ repairs (pinion + slide shoe)
- $19,500 projected maintenance spend (−54%)
- 11 hrs unplanned downtime (−71%)
- $90K production loss avoided
- 5 planned interventions, zero reactive
Launch your cement PdM pilot in days, not quarters
Spin up the Oxmaint CMMS, configure your asset hierarchy, and start baseline capture this week — your 12-week clock starts the moment sensors are live.
Cement PdM pilot — five questions plant managers ask first
The answers below address the most common objections raised during pilot kickoff meetings at cement plants across North America and the Gulf region.
Why 12 weeks — isn't that too short to prove anything in cement?
Twelve weeks is deliberately the minimum window in which a kiln or mill will generate enough steady-state operating hours, load variations, and at least one detectable degradation trend to validate the alarm model. Plants that extend to 16 weeks see marginally more catches, but the executive sponsorship curve drops sharply after week 14. Lock 12 weeks, present the verdict, then fund expansion.
Which single asset should we pick if we can only instrument one?
Choose the asset with the highest combination of criticality rank, downtime cost per hour, and existing instrumentation coverage. For 70%+ of cement plants that is the rotary kiln main drive or the clinker cooler grate drive. Avoid choosing an asset simply because it is "easy to reach" — low-criticality assets produce low-impact catches that will not fund a Phase 2 rollout.
How much should a 12-week pilot cost in hardware and software?
A focused 12–16 point pilot on one critical asset typically runs $18,000–$32,000 in sensors, gateways, and CMMS licensing combined. Wireless vibration sensors account for 40–55% of hardware spend; the rest is installation labor, thermal sensors, and the platform license. You can scope and price the exact package when you Book a Demo with the Oxmaint team.
What happens if the pilot produces zero early-warning catches?
A clean 12 weeks with no catches is still valuable data — it means the baseline alarm thresholds are correctly calibrated and the asset is healthy. However, zero catches across two consecutive pilots usually indicates the sensor placement or sampling rate is wrong for the dominant failure mode. Re-audit the FMEA and confirm the transducer type matches the failure physics before declaring PdM a poor fit.
Can we run the pilot using our existing CMMS, or do we need a new platform?
Most legacy CMMS installations in cement were built for scheduled preventive maintenance and cannot ingest continuous sensor streams or run anomaly-detection models. A pilot is the right time to evaluate a modern PdM-native CMMS. You can stand up the Oxmaint platform on a Start Free Trial alongside your existing system and migrate only the pilot asset's work-order history.
Your 12-week pilot starts with one asset, one platform, one decision
Join the cement producers who turned a single kiln pilot into an enterprise PdM program. Configure your asset hierarchy, deploy sensors, and capture the baseline that funds your Phase 2.
Free 14-day trial · No credit card