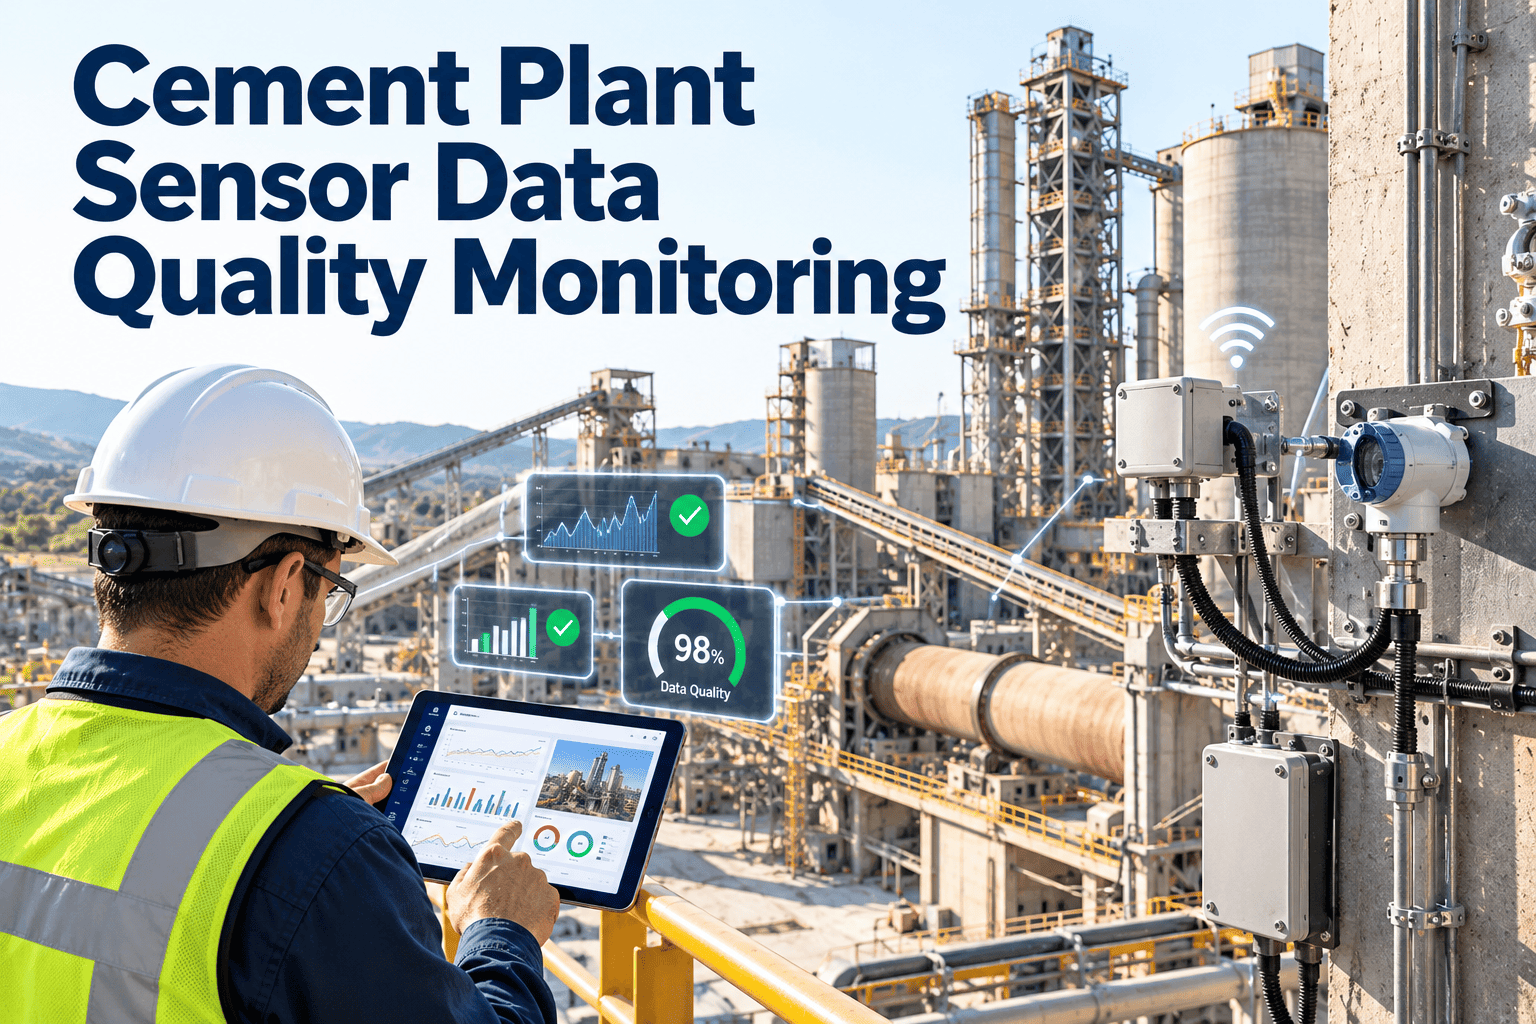
A vibration alarm on a kiln fan can mean a failing bearing, or it can mean a loose sensor cable. In a cement plant, where sensors live in heat, dust, moisture and vibration, bad data is common and expensive. Technicians chase false alarms, then start ignoring real ones. Sensor data quality monitoring checks the signal itself before anyone trusts it, and routes faulty instruments into maintenance like any other asset. This page shows how, using Oxmaint maintenance software to connect data health to work orders.
AI and Data for Cement Plant Reliability
Cement Plant Sensor Data Quality Monitoring
Separate real equipment problems from instrument problems, so condition monitoring, alerts and predictive maintenance run on signals you can trust.
Kiln ID fan vibrationTrusted
Raw mill bearing temperatureReview
Bag filter differential pressureFaulty
The Hidden Cost of Bad Sensor Data
Illustrative examples of how poor signals cascade through a cement maintenance workflow.
Nuisance alarmsA drifting temperature sensor raises alerts every shift. Operators acknowledge without checking.
Alarm fatigueWhen most alarms are false, the one real bearing alarm is treated the same way.
Wasted maintenanceCrews inspect healthy equipment while real degradation continues unseen.
Bad modelsAnalytics trained on faulty data learn false patterns and lose credibility.
Lost trustTeams abandon condition monitoring and return to run-to-failure.
Seven Ways a Sensor Signal Goes Wrong
Most data problems follow recognisable patterns. Detecting these patterns automatically is the core of data quality monitoring.
| Signal fault | What it looks like | Cement plant example | Typical cause |
|---|---|---|---|
| Flatline | Value does not change for an abnormal period | Kiln inlet temperature stuck at one value | Failed transmitter, frozen signal, broken cable |
| Drift | Slow shift away from true value | Pressure transmitter on preheater reads high over months | Sensor ageing, blocked impulse line, calibration loss |
| Spikes | Sudden jumps that reverse immediately | Vibration spikes on a mill motor | Electrical noise, loose connector, interference |
| Dropouts | Missing data or bad-quality status | Gaps in motor current history | Network issue, power loss, gateway fault |
| Out of range | Value outside physical limits | Negative flow reading, temperature above sensor range | Wiring fault, scaling error, wrong units |
| Timestamp error | Data arrives late or out of order | Alarm appears to follow the failure it should precede | Clock mismatch, buffering delay |
| Contamination | Noisy or erratic readings in dusty or hot zones | Dust-coated probe on a cooler or bag filter | Dust build-up, heat exposure, moisture ingress |
Bad Data or Bad Equipment? A Decision Path
When an alert fires, the first question is whether the machine or the measurement is at fault. A simple decision path prevents unnecessary shutdowns and missed faults.
- Check signal healthIs the value flatlined, out of range or marked bad quality by the system?
- Cross-check related signalsDo temperature, vibration, motor current and process load agree with each other?
- Compare with a peerDoes a similar asset, such as a twin fan or parallel drive, show the same behaviour?
- Verify in the fieldSend a technician with a handheld meter, thermal camera or portable vibration tool.
- Raise the right work orderInstrument fault goes to the instrumentation team; equipment fault goes to mechanical or electrical maintenance.
Sensor-by-Sensor Priorities for Cement Plants
Not every tag deserves the same attention. Start with signals that drive decisions on critical equipment.
Vibration on fans and mills
Check for flatlines, spikes and mounting looseness. Confirm the sensor is attached to the right bearing housing and orientation.Bearing and winding temperature
Watch for slow drift and sudden step changes. Compare to ambient and load before concluding the bearing is deteriorating.Motor current and power
Validate against feed rate and speed. Unexplained changes may indicate mechanical problems or measurement faults.Differential pressure on filters
Impulse lines block with dust. A frozen reading and a genuinely clean filter look identical without checks.Kiln shell and refractory scanning
Confirm scanner alignment and calibration. A dirty window or misaligned optics can hide hot spots or invent them.Oil and hydraulic pressure
Pressure sensors on lubrication and hydraulic circuits protect large drives. Validate against pump status and known operating ranges.Stop Chasing False Alarms. Fix the Signal First.
Turn data quality issues into tracked work orders in Oxmaint, so faulty sensors are repaired and recalibrated before they undermine reliability decisions.
A Signal Trust Score
Give every important tag a trust level that analytics and alerts can read. This keeps questionable signals from triggering automatic actions.
TrustedPasses all checks. Eligible for alerts, trending and model input.
ReviewMinor anomalies such as noise or drift suspicion. Alerts allowed but flagged for verification.
FaultyFlatline, out of range or missing data. Excluded from models; instrument work order raised.
BypassedIntentionally disabled for maintenance or testing. Tracked with owner and expiry date.
Checks that feed the score
- Completeness: percentage of expected samples actually received
- Validity: values within physical and configured limits
- Variability: signal moves as expected for the operating state
- Consistency: agreement with related sensors and similar assets
- Timeliness: data arrives within the expected delay
- Calibration status: last verified date against the schedule
Calibration and Instrument Maintenance
Sensors are assets. Treat transmitters, probes, scanners and analysers with the same discipline as the equipment they protect.
Preventive tasks for instruments
- Scheduled calibration with recorded as-found and as-left values
- Impulse line purging on dusty pressure measurements
- Cleaning of probe windows, lenses and optical surfaces
- Cable, junction box and gland inspection in hot or wet areas
- Mounting and torque checks on vibration sensors
Records to keep per instrument
- Instrument ID, range, type and installation location
- Calibration history and certificates
- Replacement and repair history
- Linked process tag and monitored asset
- Criticality, since safety and emissions sensors need tighter control
Special Attention: Emissions and Safety Instruments
Some instruments carry regulatory or safety weight. Continuous emissions monitoring systems, gas analysers on coal mills and kiln inlet gas measurement need stricter verification and documented evidence.
- Follow the calibration and quality assurance requirements set by your permit and local regulator
- Keep records of each verification, fault and repair, with dates and technician names
- Track availability of emissions analysers so data gaps are explained and corrected quickly
- Link instrument faults on safety systems to immediate work orders with clear priority
- Maintain evidence that interlocks and alarms have been tested, not just that they exist
From Data Alert to Closed Work Order
Detecting a bad signal is only useful if someone fixes it. The loop below keeps data quality inside the maintenance process.
AQuality rule detects a flatline, drift or dropout on a tag
BAlert reaches the instrumentation planner with asset and tag details
CWork order created with checklist: inspect, test, calibrate or replace
DTechnician records findings, cause and any parts used
ETrust score restored once the signal passes checks again
FRecurring causes trigger a design or preventive plan change
KPIs for Data Quality
| KPI | Meaning | Use |
|---|---|---|
| Critical tags rated trusted | Share of key signals passing all checks | Overall data health indicator |
| Mean time to repair a faulty sensor | Speed of instrument recovery | Check instrumentation response and spares |
| False alarm share | Alerts traced to sensor faults | Prioritise instrument improvements |
| Calibration compliance | Calibrations completed on time | Audit readiness |
| Data availability | Percentage of expected samples received | Spot network and gateway issues |
| Repeat sensor failures | Same instrument failing often | Decide on relocation or upgrade |
Implementation in Four Steps
SelectPick 30 to 50 critical tags across fans, mills, kiln drives and filters.
DefineSet expected ranges, sampling rates and operating-state rules for each.
ConnectLink tags to assets and instruments so a fault opens the right work order.
ReviewCheck trust scores weekly, tune rules and extend coverage gradually.
Context Matters: Start-Ups, Stops and Load Changes
Many false data alarms are really context errors. A cement kiln, mill or fan produces very different signals during start-up, steady running, reduced feed and stoppage. Rules that ignore those states produce noise.
Stopped equipment
A flat vibration trace on a fan that is switched off is normal. Link rules to running status so stopped assets do not raise flatline alerts.Start-up transients
Temperatures and vibration rise quickly during ramp-up. Apply a delay or separate limits until the machine stabilises.Load and feed changes
Motor current and power follow feed rate. Compare readings against expected load rather than fixed limits alone.Seasonal ambient shifts
Bearing and cabinet temperatures move with weather. Include ambient temperature in comparisons for outdoor equipment.Designing Alerts That People Act On
Data quality alerts compete for attention with process alarms. Keep them few, specific and routed to the person who can fix them.
- Name the tag, the asset, the fault type and the time the problem started in every alert
- Route instrument faults to instrumentation and equipment alerts to mechanical or electrical teams
- Escalate only if a critical tag stays faulty beyond an agreed window
- Suppress repeats while an open work order exists for the same tag
- Show the last known good value and a short signal history to speed up diagnosis
- Review the alert list monthly and retire rules that never lead to action
Escalation example
A flatlined temperature sensor on a non-critical conveyor can wait for the next planned round. A flatlined bearing temperature on a main fan should create a same-shift work order, since the plant is effectively blind on that asset until the instrument is repaired.
Where the Data Comes From: Plant Architecture Notes
Cement plants usually combine several data sources, each with its own failure points. Knowing where a fault can occur narrows the search quickly.
| Layer | Typical components | Common data problem | First check |
|---|---|---|---|
| Field instrument | Transmitters, probes, vibration sensors | Drift, contamination, damage | Inspect and compare with a handheld device |
| Wiring and junction | Cables, glands, terminals | Intermittent contact, moisture, noise | Check connections and shielding |
| Control system | DCS, PLC, I/O cards | Scaling errors, bad quality status | Verify configuration and card health |
| Gateway and network | OPC UA servers, edge devices, switches | Dropouts, delays, buffering | Review connectivity and logs |
| Historian | Time-series storage | Compression artefacts, gaps | Check compression and retention settings |
| Maintenance system | CMMS asset and tag mapping | Tags linked to the wrong asset | Audit mapping after control changes |
Common Mistakes in Sensor Data Quality Programmes
Avoid
- Monitoring thousands of tags before proving value on a few
- Using one threshold for all equipment regardless of state
- Letting bypassed sensors stay bypassed with no expiry
- Treating data quality as an IT issue only
- Fixing a sensor without recording what was wrong
Prefer
- Starting with critical assets and expanding by evidence
- Rules tied to operating state and related signals
- Bypass records with owner, reason and review date
- Shared ownership between operations, maintenance and automation
- Closing every instrument job with a cause code
Using Findings to Improve the Plant
Data quality records reveal where instruments are poorly specified or badly located. Over a year, the pattern of faults guides investment better than anecdotes.
- If dust repeatedly blocks a pressure tap, change the tapping design or add automatic purging
- If vibration sensors keep loosening on one fan, review mounting method and torque practice
- If a scanner window fouls quickly, adjust cleaning frequency or air purge
- If a gateway drops data every night, investigate network or power events
- If certain sensor models fail often, standardise on a more suitable type
Roles and Responsibilities
Data quality fails when everyone assumes someone else owns it. Agree the roles at the start so every faulty signal has a clear next step.
| Role | Responsibility |
|---|---|
| Reliability engineer | Chooses critical tags, defines rules and reviews trust scores and repeat faults |
| Instrumentation technician | Diagnoses, calibrates, repairs or replaces faulty instruments and records findings |
| Automation engineer | Maintains scaling, tag mapping, gateways and historian configuration |
| Maintenance planner | Schedules calibration tasks, reviews instrument work orders and manages spares |
| Operations supervisor | Confirms running states, reports suspected instrument problems and approves bypasses |
Spares for instrumentation
Keep critical spares such as vibration sensors, thermocouples, pressure transmitters and cables in stock, linked to the instrument records. A faulty sensor on a main fan should not wait weeks for a part while the plant runs without condition data.
Verifying Data Quality After Shutdowns
Major shutdowns are when sensors are removed, cables disturbed and tags remapped. They are also the best moment to restore data confidence before the plant restarts.
- Include a signal verification checklist in the shutdown scope for every critical monitored asset
- Confirm each replaced sensor reports the right unit, range and direction before restart
- Compare readings against handheld measurements during warm-up and record the result
- Check that tags still point to the correct asset after any control system change
- Review trust scores in the first week after restart and clear any new faults quickly
Frequently Asked Questions
Does a CMMS monitor sensor signals directly?
A CMMS manages the work, assets and records. Signal checks come from your monitoring layer and connect to work orders.
How do we avoid too many data quality alerts?
Start with critical tags and clear rules, and use trust levels so minor issues are flagged without creating urgent jobs.
Who should own faulty sensor repairs?
Usually the instrumentation or automation team, with the work order visible to reliability and operations.
Can data quality records support audits?
Yes. Calibration, fault and repair histories create traceable evidence. You can book a demo to see the records.
Is this required before predictive maintenance?
Reliable inputs are essential. Predictive models are only as good as the signals feeding them.
Build Predictive Maintenance on Signals You Can Trust
Bring sensor health, instrument maintenance, alerts and work orders together in Oxmaint, and give your cement plant condition monitoring that teams believe.