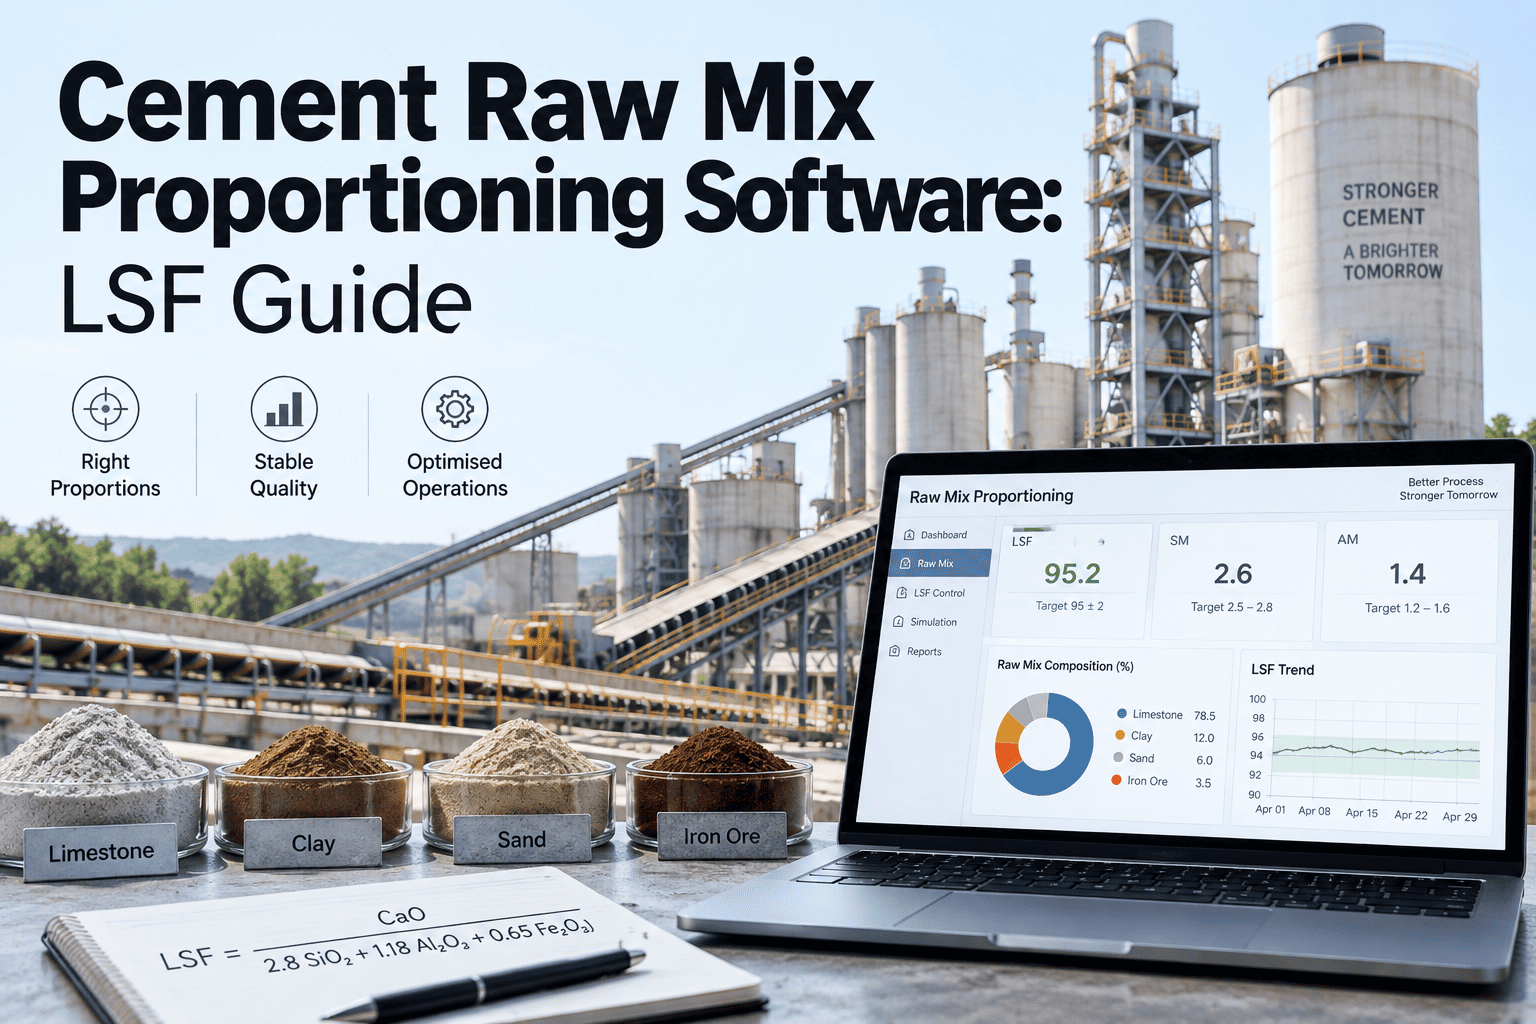
Cement raw mix proportioning demands extreme precision where even minor deviations in Lime Saturation Factor trigger cascading failures across the pyroprocessing system. Traditional spreadsheet calculations and delayed laboratory feedback loops leave kiln operators adjusting to stale data, resulting in unstable burnability and unpredictable strength development. The gap between a raw mill sample and a corrective action is where profit burns away, but OxMaint closes this latency by integrating real-time raw mix moduli tracking into your core maintenance and reliability workflows. Transform your raw mill control from reactive guesswork into predictive chemistry discipline by starting your free OxMaint trial or booking a 30-minute specialist demo.
Cement Raw Mix Proportioning: Mastering LSF for Clinker Stability
Eliminate LSF deviations, stabilize silica and alumina moduli, and prevent unstable burnability before they force kiln stops or degrade clinker quality — with OxMaint AI monitoring and automated corrective workflows.
The Hidden Cost of LSF Fluctuations in Cement Kilns
Raw mix proportioning is the chemical foundation of cement manufacturing. When Lime Saturation Factor drifts outside the 90-98% target window, the physical consequences inside the kiln are immediate and severe, driving up thermal energy consumption and degrading clinker mineralogy, which directly impacts the structural integrity of the final product and the economic viability of the plant.
Excess lime forces the burning zone to drive significantly harder to combine free CaO, demanding much higher flame temperatures and extended residence time. This creates massive fuel waste, rapid refractory degradation from overcoating, and elevated clinker free lime content that threatens late concrete expansion and fatal volume instability in downstream structures. Correcting an over-limed mix requires rapid dilution with silica sources, often forcing the raw mill to operate at reduced capacity while the homogenization silo chemistry slowly rebalances over hours of production time, during which the kiln continues to burn fuel inefficiently.
Insufficient lime leaves silica and alumina unsaturated, failing to form the essential alite crystals responsible for early strength. The resulting clinker is dust-heavy, mechanically weak, and fails to meet 28-day compressive strength standards, forcing expensive, high-power grinding in the cement mill to achieve the required fineness. Under-limed clinker also produces excessive belite, which is highly resistant to grinding and dramatically increases specific power consumption. Re-liming the silo requires careful addition of high-grade limestone, but the delayed laboratory turnaround often means the kiln consumes thousands of tonnes of off-spec raw feed before the adjustment takes physical effect.
SM dictates the ratio of solid silicate phases to the liquid melt at burning zone temperatures. High SM reduces the liquid phase, causing poor nodulization, excessive dust carryover, and unstable coating adherence. Low SM creates an excessive melt, leading to thick, difficult-to-control coating, severe ring formation at the burning zone exit, and dangerous kiln shell overloads that halt production entirely. Because SM controls the structural matrix of the clinker, deviations here are often more disruptive to kiln mechanics than LSF deviations, yet they are frequently overlooked in standard operational procedures that focus solely on lime saturation.
AM controls the viscosity of the kiln liquid phase. Low AM produces a fluid, low-viscosity melt that washes out protective coating and destabilizes the burning zone thermodynamic profile. High AM creates a stiff, viscous melt that traps uncombined free lime inside dense, impermeable nodules, preventing complete mineralization regardless of fuel input. Alumina fluctuations are commonly driven by clay feeder inconsistency or raw material moisture variations that alter bulk density. Without continuous, automated tracking of AM alongside LSF, operators frequently misdiagnose the root cause of coating instability, applying thermal corrections when chemical proportioning adjustments are the true solution.
The Three Moduli Controlling Clinker Phase Formation
Clinker quality is entirely determined by the relative proportions of oxides in the raw feed. Mastering LSF, SM, and AM is the only path to consistent alite formation and predictable 28-day mortar strength. A failure in any single modulus degrades the entire pyroprocessing chain downstream, compromising product quality and increasing operational expenditures across the grinding and burning circuits.
LSF measures the degree to which lime saturates the silica, alumina, and iron oxide. An LSF of 100 represents theoretical maximum saturation. Operating near 95% provides optimal burnability without leaving uncombined free lime that destroys volume stability. OxMaint continuously tracks CaO against acidic oxides to flag saturation drift instantly, preventing the thermal punishment required to force combination of excess lime and protecting the refractory lining from thermal overload.
SM defines the ratio of silica to the combined alumina and iron. It governs the balance between solid silicate minerals and the liquid phase. Maintaining SM within tight limits ensures proper coating formation and prevents the dust rings or melt surges that force operators to reduce kiln speed. OxMaint flags feeder speed anomalies that threaten the delicate silicate balance, maintaining the liquid phase volume required for dense, high-density clinker nodulization.
AM represents the ratio of alumina to iron oxide, controlling liquid phase viscosity and the ratio of C3A to C4AF. This dictates early setting characteristics and sulfate resistance. OxMaint alerts when alumina or iron feeder variations threaten the liquid phase properties, preventing the sudden viscosity swings that cause catastrophic coating failure and unstable burning zone conditions that lead to unplanned kiln stops.
OxMaint AI monitors raw mix chemistry, correlates XRF lab results with feeder speeds, and generates prioritized proportioning work orders automatically — so your team stabilizes moduli on the first adjustment, not after kiln thermal damage.
How OxMaint Closes the Raw Mix Correction Loop
Laboratory data without immediate corrective action is just expensive reporting. OxMaint bridges the gap between the XRF analyzer and the raw mill feeders, ensuring every chemical deviation triggers a calibrated, trackable response before off-spec material reaches the homogenization silo and destabilizes the kiln feed chemistry.
XRF results and online analyzer data flow directly into OxMaint. The system logs CaO, SiO2, Al2O3, and Fe2O3 percentages against the active raw mix recipe, eliminating manual spreadsheet transfers and preventing transcription errors that cause disastrous feeder miscalculations and prolonged off-spec production runs that severely impact clinker silo levels.
OxMaint instantly recalculates LSF, SM, and AM with every sample update. The current moduli are compared against the plant-specific target windows. Trend vectors are analyzed to identify gradual drifts that point to weigh feeder calibration loss or limestone quarry face chemistry changes before they exceed control limits and cause irreversible clinker quality shifts.
When LSF or SM breaches control limits, OxMaint generates a priority alert. The alert includes the specific oxide causing the shift, the magnitude of the deviation, and the recommended feeder setpoint adjustment, removing guesswork from the raw mill control room and standardizing the chemical correction process across all operating shifts.
Critical chemistry deviations automatically generate work orders for feeder calibration, bin level verification, or material diversion. Operators receive exact instructions on which feeder to adjust and by what percentage, ensuring the homogenization silo receives corrected feed immediately without supervisory delays that prolong kiln instability.
After the raw mix adjustment, the next lab sample verifies the correction. OxMaint logs the entire deviation event, the corrective action taken, and the verification result against the asset record, building a historical database for raw mix reliability tracking and feeder performance analysis over time to optimize future preventive maintenance schedules.
Cement Raw Mix Proportioning Control Parameters
Effective raw mix control requires monitoring both chemical moduli and individual oxide limits. The table below defines standard proportioning targets and the operational consequences when limits are breached in the rotary kiln system, impacting everything from flame stability to cement mill specific power consumption.
| Parameter | Target Range | High Deviation Impact | Low Deviation Impact | OxMaint Action |
|---|---|---|---|---|
| Lime Saturation Factor | 93% – 97% | Free lime, hard burning, fuel waste | Dusty clinker, low 28-day strength | Auto WO for feeder recalibration |
| Silica Modulus | 2.2 – 2.6 | Poor nodulization, dust loss | Ring formation, heavy coating | Alert with silica source adjustment |
| Alumina Modulus | 1.3 – 1.8 | Stiff melt, free lime entrapment | Fluid melt, coating washout | Priority WO for alumina/iron balance |
| MgO Content | < 3.0% | Delayed expansion, unsound clinker | Minimal impact if low | Quarantine alert if > 2.5% |
| Alkali (Na2Oeq) | < 0.6% | Alkali-silica reaction in concrete | Minimal impact if low | Alert with bypass damper recommendation |
| Free CaO | < 1.5% | Unsound cement, volume expansion | Optimal if low | High-priority WO for kiln thermal review |
| LOI (Loss on Ignition) | 34% – 36% | Incomplete calcination suspicion | Over-calcined raw feed | Trend monitoring against preheater exit |
Linking Raw Mix Proportioning to Clinker Phases
The entire purpose of raw mix proportioning is to control the quantitative formation of the four major clinker minerals. LSF, SM, and AM directly dictate the Bogue calculation outputs, which in turn govern the physical properties of the final cement. Precision in the raw mill is the only path to consistency in the cement mill and predictable concrete performance downstream.
The primary strength-giving phase in clinker, responsible for early 1- to 28-day strength. High LSF and moderate SM favor alite formation. When LSF drops below 92%, alite formation plummets, and belite takes over, resulting in slow-setting, low-strength cement. OxMaint ensures CaO availability remains sufficient to saturate the silica completely, maximizing the alite yield and minimizing the grinding energy required to achieve target mortar strengths.
Belite contributes to late strength beyond 28 days but is highly undesirable in high-early-strength cements. Low LSF and high SM promote belite formation at the expense of alite. Persistent belite-rich clinker forces cement mills to grind finer, consuming excessive power and reducing throughput. OxMaint LSF tracking prevents under-liming that starves alite formation, ensuring the burning zone produces dense, readily grindable alite nodules.
C3A controls flash setting and early hydration heat. High AM and low SM drive excessive C3A formation, which causes severe rheology issues in concrete, requiring high gypsum dosage to control workability. In sulfate-resisting cements, C3A must be strictly limited below 5%. OxMaint monitors alumina oxide closely to prevent C3A excursions, ensuring consistent setting times and reliable sulfate resistance across all product grades.
Ferrite acts as a flux during burning and contributes minimally to cement strength but significantly to liquid phase viscosity. Low AM increases the C4AF ratio, stiffening the melt and making free lime combination harder. OxMaint tracks iron oxide feeder stability to maintain the delicate liquid phase balance required for dense, low-porosity nodules that cool properly and grind efficiently in the downstream finishing circuit.
The Financial Impact of Raw Mix Instability
Raw mix deviations are not just technical chemistry problems; they are massive financial drains. Every percent of LSF deviation translates directly to increased fuel consumption, reduced kiln throughput, and escalated grinding costs. OxMaint stabilizes the chemistry to protect the plant operating margin and ensures that thermal energy is used to drive clinkering reactions, not to force combination of improperly proportioned raw feed.
A 2% deviation in LSF above target forces the burning zone temperature up by approximately 50°C to combine the excess free lime. This requires significantly higher fuel injection rates, increasing thermal energy consumption per tonne of clinker by up to 5%. Over a monthly production cycle, this fuel penalty represents a massive, avoidable operational expense that directly erodes profitability and increases the plant carbon footprint per tonne of product manufactured.
Under-limed clinker produces excessive hard-burning belite that is highly resistant to comminution. To achieve the same Blaine fineness, the cement mill must increase recirculation load and grinding time, driving specific power consumption up by 10-15%. This not only wastes electricity but severely limits cement mill throughput, creating a production bottleneck that prevents the plant from meeting dispatch schedules during peak demand periods.
Fluctuating LSF and SM cause alternating coating formation and shedding inside the burning zone. Each coating loss event exposes the refractory brick to direct flame radiation, accelerating chemical attack and thermal spalling. Unstable raw mix chemistry is a primary driver of premature refractory failures, forcing expensive, unplanned kiln stops for relining that eliminate hundreds of hours of production time annually.
When free lime remains uncombined due to high LSF, the clinker must be downgraded to lower-strength cement classes or stored in emergency silos. This destroys product value and creates logistical nightmares in clinker yard management. OxMaint alerts operators to free lime excursions instantly, preventing the production of unsound clinker and protecting the market reputation of the cement brand from structural liability risks.
Frequently Asked Questions
How does OxMaint integrate with existing XRF analyzers and online bulkers?
Can OxMaint adjust raw mix targets based on different cement product grades?
What happens when an online analyzer detects a sudden raw mix deviation?
Does OxMaint track the historical reliability and calibration drift of weigh feeders?
How quickly can a cement plant deploy OxMaint for raw mix monitoring?
Your Next Clinker Quality Failure Is Still Preventable. Control the Chemistry, Not the Aftermath.
OxMaint gives cement plant teams AI-driven raw mix deviation detection, automated Bogue calculations, and priority work orders — closing the gap between the lab result and the feeder correction that prevents unstable clinker. Deploy in under two weeks.