A separator that has lost efficiency does not stop the mill, which is exactly why the loss goes unnoticed. Coarse particles leak into the product, fines return to the mill and are over-ground, circulating load climbs, and specific energy per tonne drifts upward month after month. Most of this comes from worn internals, air leaks and drifting settings that can be measured and scheduled for repair. This guide explains how to measure separator performance, which components wear first, how airflow and drives affect results, and how to build a maintenance plan that protects efficiency rather than reacting when fineness complaints arrive.
Cement Separator Efficiency and Maintenance Guide
Separator performance links directly to mill throughput, cement fineness, strength development and kWh per tonne. This guide shows which efficiency indicators to trend, which parts wear first, and how to convert inspection findings into planned work instead of silent energy losses.
What the separator does in a closed grinding circuit
In a closed circuit, the mill grinds material and the separator decides what is fine enough to leave and what must return. Its performance therefore controls how hard the mill must work for each tonne of finished cement.
Cut size and product fineness
The separator sets the cut size, the particle size at which material is equally likely to go to product or return. Fineness targets such as Blaine or residue on a sieve are the result of this cut and the shape of the distribution around it. A stable cut size makes the product consistent and helps strength and setting behaviour remain predictable.
Circulating load and mill efficiency
If separation is poor, material that is already fine returns to the mill, raising circulating load and over-grinding. This cushions the mill charge, wastes energy and can reduce throughput. If circulating load climbs without a change in feed or fineness target, separator condition is one of the first things to investigate.
Energy consumption
Grinding is one of the largest electrical consumers in a cement plant. Better separation lets the mill produce the same fineness with less total grinding work. Even modest improvements in sharpness of separation can show up in kWh per tonne, so it is worth establishing a baseline and measuring any change after repairs or adjustments.
Quality, water demand and strength
A broad particle size distribution, with too many very coarse or very fine particles, can affect water demand, early and late strength and workability. Customers notice these effects before the plant sees them in averages, so keeping separation sharp is as much a quality topic as an energy topic.
How to measure separator performance reliably
You cannot manage what you do not measure. Separator efficiency calls for a small number of well-chosen indicators and disciplined sampling.
The Tromp or partition curve
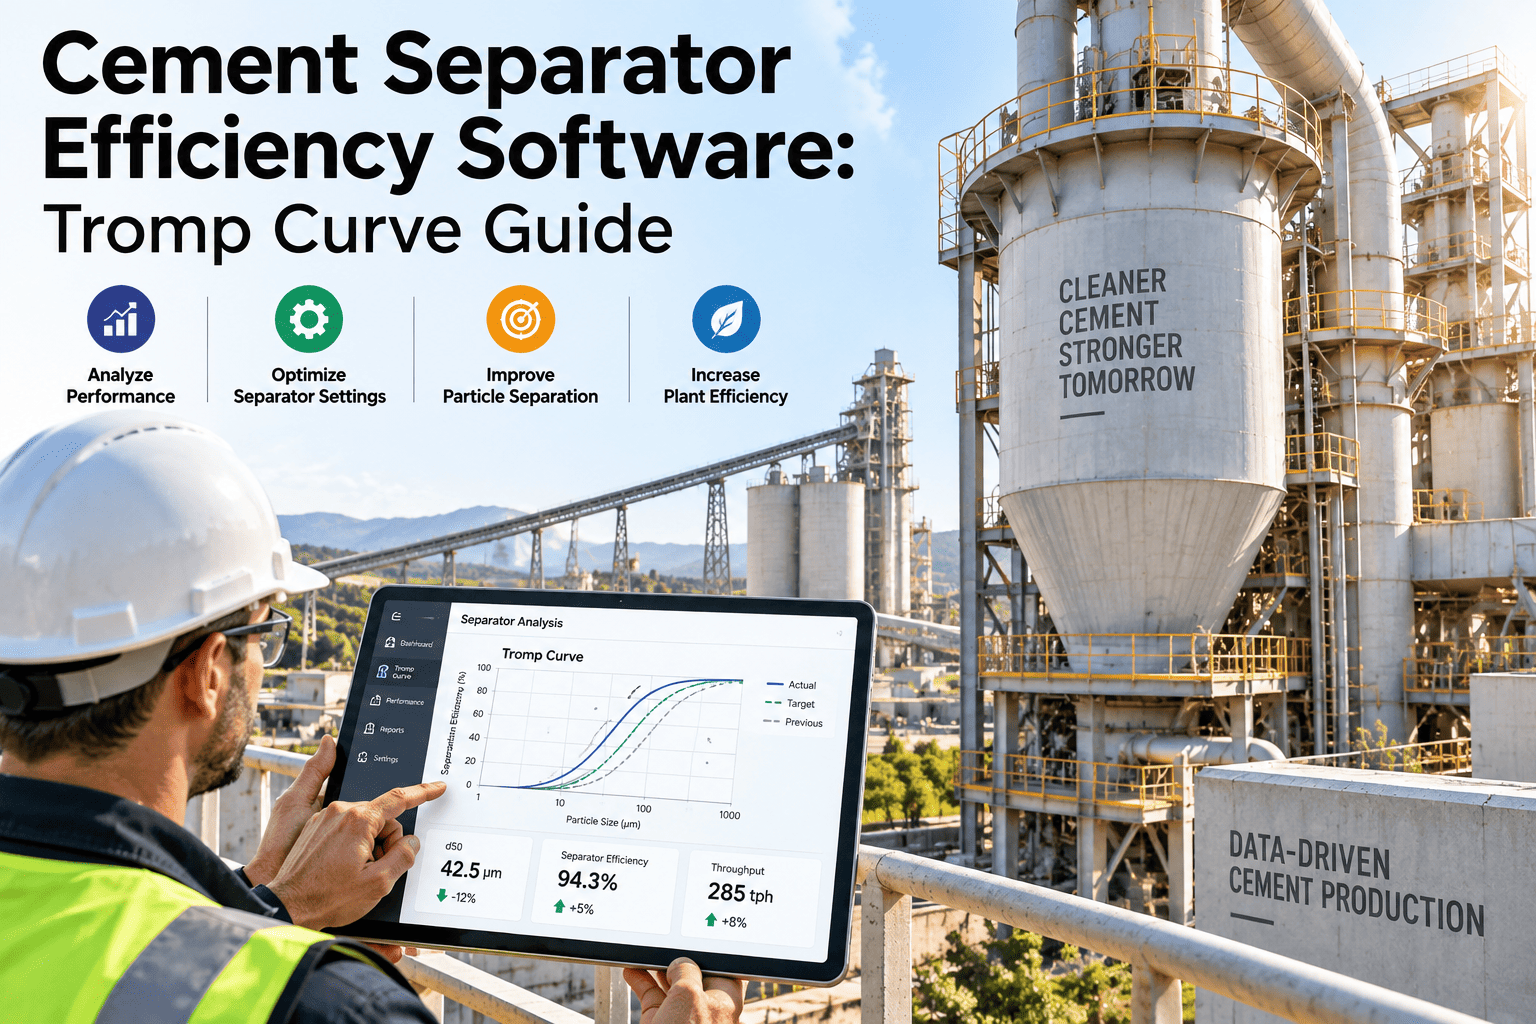
The partition curve shows the fraction of each particle size in the separator feed that is returned as rejects. A steeper curve means sharper separation. It is the most informative single indicator, but it requires samples of feed, product and rejects taken at the same time and analysed by laser particle size or sieving. Run it periodically and after major repairs.
Bypass fraction
Bypass is the share of fine material that is carried to the rejects rather than to product, shown as the curve not reaching zero at the fine end. High bypass indicates poor dispersion or leakage and is a common sign of worn feed distribution parts or airflow problems. Track it as a number over time rather than a one-off result.
Cut size and sharpness of separation
Calculate the cut size and a sharpness index from the partition curve and compare them with earlier tests under similar conditions. A gradual shift in cut size at constant settings points to wear or leakage. Record operating conditions with each test, such as rotor speed, airflow and feed rate, so comparisons are valid.
Sampling discipline and data quality
Poor samples produce misleading curves. Use consistent sampling points, representative sampling devices, sufficient sample mass and consistent preparation. Log results in the same place as maintenance records, so a drop in performance can be traced to specific inspections, repairs or setting changes.
Separator losses show up as higher kWh per tonne long before a breakdown. OxMaint combines inspection readings, wear history, vibration trends and process indicators, so reliability teams can plan separator repairs against actual condition and prove the benefit afterwards.
The parts that wear and what they do to performance
Separators handle abrasive, fine material at high velocity. Wear is inevitable, and its effect on performance is gradual enough to hide in daily variation.
Rotor cage and blades
Cage blades or bars create the classifying field. Erosion changes blade geometry and gaps, which alters cut size and allows coarse particles to pass. Broken or missing blades can also create imbalance and vibration. Inspect for thickness, edge condition and cracks at every opportunity and record measurements, so wear rate can be forecast.
Guide vanes and air inlet
Guide vanes direct the air stream into the classifying zone. Worn, bent or misadjusted vanes distort the air pattern, reducing sharpness of separation. Check vane angles and condition, and confirm that adjustment mechanisms still move freely and hold position.
Feed distribution and dispersion plate
The material must be dispersed evenly into the airstream. Worn distribution plates or chutes cause agglomerates to pass through unseparated, which raises bypass. Wear patterns on these parts also reveal feed segregation and should be photographed and logged at each inspection.
Seals, casing and rejects cone liners
Labyrinth seals, expansion joints and access doors leak air if worn or poorly closed, disturbing the airflow balance. Liners in the rejects cone and casing wear through, risking leaks and structural damage. Include a leak walk-down in regular rounds and schedule liner replacement based on measured thickness.
Air balance, fans and dust collection
Separation is an aerodynamic process. Even if internals are in good shape, an unbalanced airflow will undermine results.
Air balance and dampers
Dampers control how much air enters through the main inlet, tertiary air and vanes. Sticking or worn dampers, with positioners that no longer match their commanded position, create hidden changes in airflow. Verify damper travel against the control signal on a schedule and fix mismatches promptly.
Fan condition and vibration
The separator fan or system fan moves the product-laden air. Dust build-up on blades, erosion and bearing wear cause imbalance and drop in airflow. Trend vibration, bearing temperature and motor current, and compare them with baseline values after cleaning or blade repair.
Ducting, cyclones and filters
Blocked or leaking ducts and worn cyclone parts change pressure drop and allow fines to escape or fall out. Differential pressure across filters and cyclones provides a cheap indicator. A creeping increase is a prompt to inspect before capacity and efficiency suffer.
Instrumentation that supports control
Pressure, flow and temperature sensors feed control loops and operator decisions. Plugged impulse lines or drifting transmitters can lead operators to compensate for the wrong problem. Include these instruments in calibration and cleaning schedules.
Rotor drives, bearings and lubrication
Mechanical failures in the drive train cause unplanned stops and often damage the rotor and cage, so the cost of failure is high.
Drive, gearbox and coupling
Monitor motor current, gearbox temperature and oil condition, and inspect couplings for wear and misalignment. A change in current at constant feed can indicate increased friction or buildup. Oil analysis can detect gear and bearing wear before audible symptoms appear.
Main bearings and rotor balance
Bearings carry the rotor load and are sensitive to imbalance caused by uneven wear or material build-up. Vibration trends, bearing temperature and visual checks of lubrication reveal developing issues. Balance the rotor after blade replacement and verify vibration against acceptance limits.
Lubrication routes and contamination control
Missing or contaminated lubrication is a major cause of premature failure. Define each lubrication point, grease type, quantity and interval, and assign them to recurring tasks. Keep clean storage and handling of lubricants, since contamination from dust is common in cement plants.
Condition monitoring and alarm limits
Set alarm and trip limits for vibration and temperature using manufacturer guidance and plant history. Review alarms regularly to separate genuine deterioration from instrument issues, and use the review to tighten or relax limits with evidence.
Building a separator maintenance plan that protects efficiency
Technique matters, but consistent execution matters more. A simple, well-run plan beats a sophisticated one that is not followed.
Inspection routes and checklists
Create routine checks for leaks, vibration, noise, temperatures, lubrication and operating parameters, and a deeper internal inspection during planned stops. Use checklists with defined measurements, not just comments, so findings can be trended and compared between inspectors.
Wear tracking and replacement forecasting
Record thickness or dimensional measurements of cage blades, vanes, liners and distribution parts against operating hours or tonnes. Extend the trend to the replacement limit to estimate when each part will need changing and order materials with enough lead time.
Planned outages and spare parts
Align separator repairs with scheduled mill stops. Hold critical spares such as blade sets, seals, bearings and key liner sections, based on lead time and consequence of failure. Prepare work packages in advance, including tools, lifting plans and safety permits, so that the outage is short and predictable.
KPIs and continuous improvement
Track circulating load, specific energy, fineness stability, partition curve results, vibration alarms and unplanned stops. Review them together with maintenance actions to see which repairs delivered measurable gains, and use the evidence to justify future investments.
Separator condition: indicators and maintenance actions
The table links common indicators to likely causes and the first maintenance response.
| Indicator | What It Reveals | Typical Cause | Recommended Action |
|---|---|---|---|
| Bypass fraction rising | Coarse or fine leakage to the wrong stream | Worn feed distribution parts, seal leakage | Inspect distribution plate, cage and seals |
| Cut size shifting at constant settings | Airflow or classifying field change | Vane wear, damper fault, blade erosion | Check vanes, damper calibration and cage condition |
| Circulating load increasing | Over-grinding and wasted energy | Reduced sharpness of separation | Run partition curve test and plan internal inspection |
| Fan vibration increasing | Imbalance or bearing wear | Dust build-up, blade erosion | Clean, balance, check bearings and mounting |
| Rotor drive current rising | Increased friction or build-up | Bearing fault, material accumulation | Inspect bearings, lubrication and rotor |
| Differential pressure creeping up | Blockage or fouling in ducts and filters | Dust build-up, damaged filter | Clean ducts, inspect and replace filter media |
Frequently Asked Questions
How do I know if my separator is inefficient?
Look for rising circulating load, higher specific energy, unstable fineness and a flatter partition curve. A sampling programme with results logged against maintenance dates makes these patterns visible and shows whether recent repairs helped.
Which separator parts wear fastest?
Rotor cage blades, guide vanes, feed distribution parts, rejects cone liners, seals and dusty ductwork see the highest abrasion. The rate depends on raw material hardness, airflow velocity and operating hours, so measure your own wear rate rather than relying on generic life figures.
How often should a partition curve test be run?
There is no single answer, but many plants test after major repairs, when product quality shifts, and at regular intervals such as annually. Recording results in your maintenance system alongside inspection findings makes the trend meaningful.
Can separator maintenance be predictive?
Yes. Wear measurements, fan vibration, motor current and process efficiency data can forecast the point at which repair becomes more economical than continued operation. Predictive methods work best when readings are collected consistently and compared with a healthy baseline.
How much energy can be saved by restoring separator efficiency?
It varies widely between plants and depends on the starting condition. The saving comes from reducing circulating load and over-grinding, so measure your baseline kWh per tonne and circulating load before the repair and compare after. Do not rely on generic percentages.
What spare parts should be kept on site?
Prioritise parts with long lead times or high failure consequences, such as rotor bearings, seal sets, cage blades or bars, critical guide vanes, couplings and key liner sections. A criticality ranking in the maintenance system helps justify stock levels and prevents both shortages and excess inventory.
How do operating settings such as rotor speed and airflow affect results?
Rotor speed mainly shifts the cut size, with higher speed giving a finer product, while airflow influences loading and the sharpness of the separation. Changing one setting alters the others, so adjust gradually, record the change and its effect, and verify with a partition curve before treating a new setting as the standard. Unrecorded setting changes are a frequent reason performance seems to drift when maintenance is not the cause.
How should we prove the value of separator repairs to management?
Capture a baseline before the outage: circulating load, kWh per tonne, fineness stability, partition curve and throughput. Repeat the same measurements under comparable conditions after the repair, then convert the energy and throughput difference into cost. Linking the work order, parts cost and the measured gain in one record turns a maintenance expense into a documented return that supports the next request.
Keep Separator Efficiency from Slipping Away
OxMaint links wear inspections, vibration data and process indicators, so separator repairs are planned on evidence, efficiency is restored before energy costs creep up, and every improvement can be measured.
Free 14-day trial · No credit card