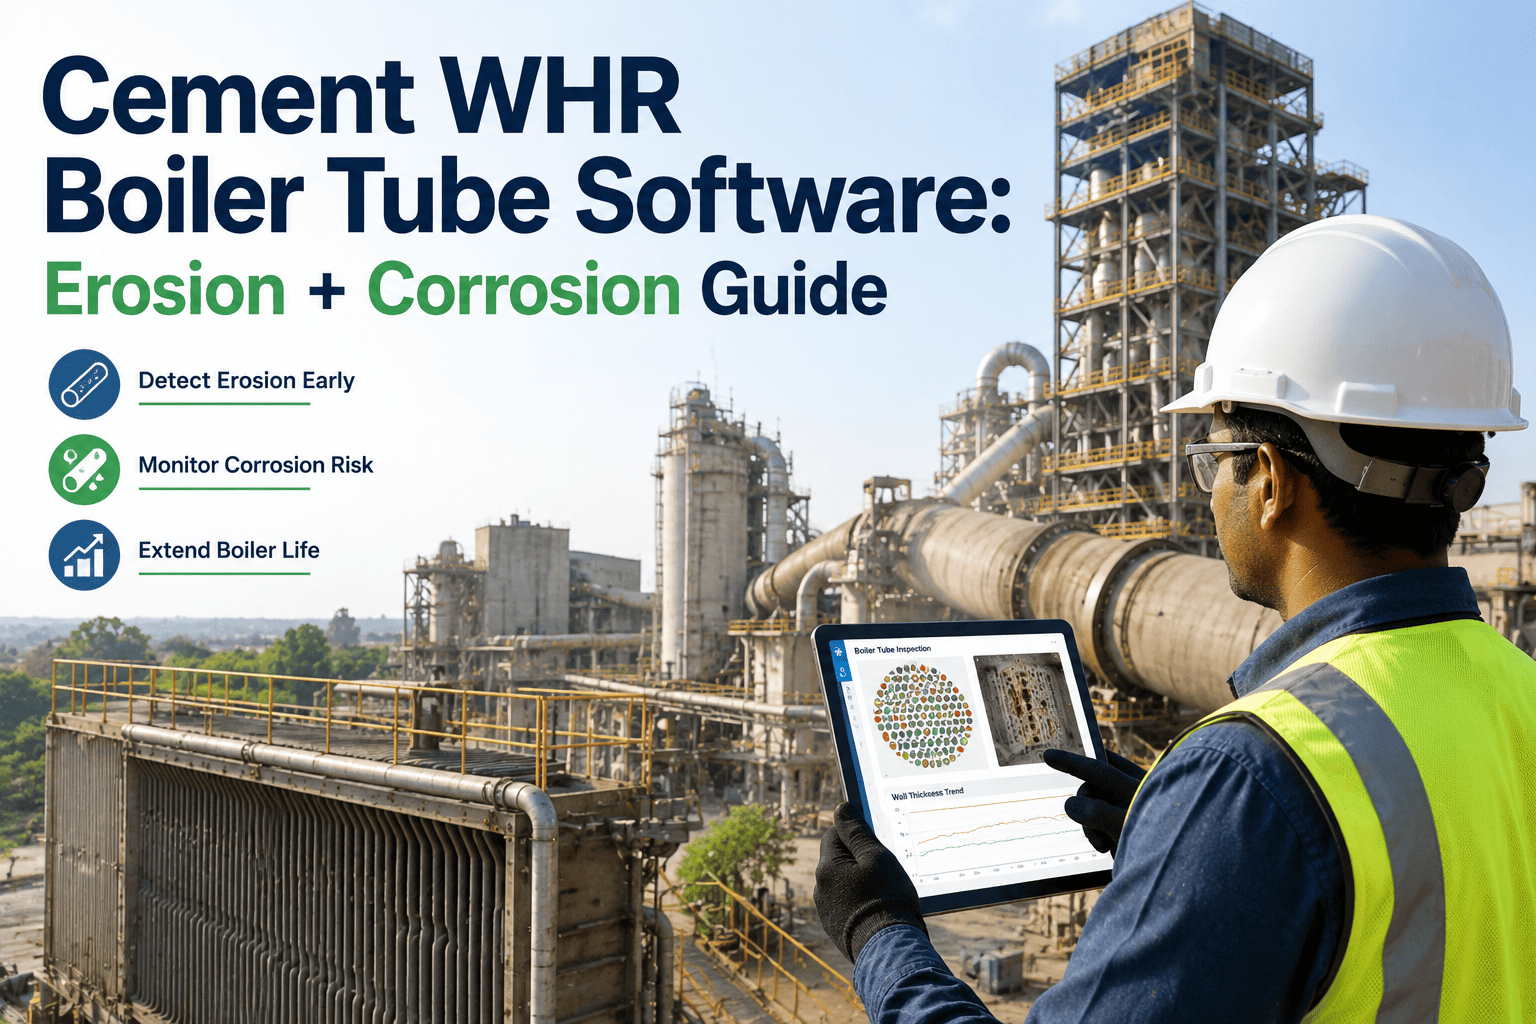
Waste heat recovery boilers are one of the best energy paybacks a cement plant can make, but the PH and AQC boiler tubes inside them absorb constant abuse from kiln exhaust and clinker cooler air. Dust-laden gas carries abrasive raw meal and clinker fines that erode tube walls year-round, while cooling that same gas below its acid dew point condenses sulfuric and sulfurous acid straight onto cold-end tube metal. Left untracked, erosion and corrosion compound each other — thinning walls faster than any single mechanism would on its own — and can cut tube life to a fraction of the 15 to 20 year design window, forcing forced outages and expensive retubing years ahead of schedule. This guide walks through the specific failure modes hitting cement WHR tube banks, the inspection cadence that catches wall loss before it becomes a leak, and the CMMS setup that keeps thickness data working for you instead of sitting in a filing cabinet. To see it running against your own boiler data, start a free trial today.
CEMENT WHR BOILER RELIABILITY GUIDE
Is fly-ash erosion thinning your PH boiler tubes below minimum wall right now?
A cement kiln preheater carries 60–120 g/Nm³ of dust into the PH boiler bank. Every pass over an unshielded leading-edge tube removes a few microns of steel — invisible daily, catastrophic by year three if nobody is tracking it. Pair that with acid dew-point attack at the cold end and you have the two mechanisms responsible for most unplanned WHR boiler outages in cement plants.
FAILURE MODES
Four ways a cement WHR boiler tube actually dies
PH and AQC boiler tubes rarely fail from one clean cause. They fail from a combination of abrasive dust, cold-end chemistry, and deposit buildup working on the same few millimeters of steel. Knowing which mechanism is active in which zone is the difference between a routine repair and an unplanned trip.
Fly-ash and dust impingement erosion
Raw meal and clinker dust entrained in preheater exhaust strike leading-edge tubes and tube-to-baffle transitions at high velocity. Wall loss concentrates on the gas-facing side, producing a characteristic wedge or horseshoe wear pattern that thins the tube long before the rest of the bank shows wear.
Acid dew-point corrosion
As flue gas cools past roughly 130–150°C at the cold end, sulfur and chlorine compounds condense into sulfuric and sulfurous acid on tube metal. This attack is worst during startup and shutdown, when gas temperature swings through the dew point repeatedly and re-wets the same surfaces.
Under-deposit corrosion
Sticky dust and ash cake onto low-velocity tube surfaces and trap moisture and corrosive salts against the metal underneath. The scale hides the attack from a simple visual walk-down, so wall loss is often discovered only when a thickness gauge is actually placed on the spot.
Soot-blower and SRU steam erosion
Shock pulse and steam soot removal units clear dust cake, but mis-aimed or over-frequent blowing erodes a localized band on the tube directly in the jet path. Tubes nearest the blower lance almost always show the deepest wall loss in the bank.
WORKED EXAMPLE · 4,500 TPD KILN LINE
What untracked wall loss costs across a PH + AQC boiler pair
A 4,500 TPD kiln line running a PH boiler and an AQC boiler in series loses roughly 0.15–0.3 mm of wall thickness a year in high-erosion rows when nobody is trending it, against a design allowance built for 0.05–0.08 mm a year. Here is what that gap actually costs when it turns into an unplanned retubing.
| Tube Zone | Gas Temp Range | Dominant Mechanism | Typical Wall Loss | Inspection Priority |
|---|---|---|---|---|
| PH inlet bank, leading rows | 750–900°C | Dust impingement erosion | 0.15–0.3 mm/yr | High |
| PH mid bank | 400–650°C | Erosion + light fouling | 0.08–0.15 mm/yr | Moderate |
| PH / AQC cold end | 130–220°C | Acid dew-point corrosion | 0.1–0.25 mm/yr | High |
| Soot-blower lane rows | Varies by zone | Localized steam erosion | Up to 0.35 mm/yr | High |
| AQC low-velocity pockets | 200–350°C | Under-deposit corrosion | 0.1–0.2 mm/yr | Moderate |
Stop finding tube wall loss the hard way — with a leak
A CMMS that trends thickness data by tube ID turns wall loss into a planned repair instead of an unplanned trip. Build your PH and AQC boiler asset hierarchy once and let inspection data do the flagging from there on.
INSPECTION CADENCE
A 12-month tube monitoring plan that actually catches wall loss early
Erosion and corrosion on WHR boiler tubes rarely announce themselves. Catching them ahead of a leak means combining routine walk-downs with scheduled ultrasonic thickness surveys at fixed grid points, not waiting for a visual clue that may never come.
Dust loading and gas temperature log
Track inlet dust loading and gas temperature at the PH and AQC boiler inlet against baseline. A rising dust load or a gas temperature dropping toward the acid dew point on either boiler is an early signal to schedule a targeted inspection before wall loss accelerates.
Visual walk-down of leading-edge rows
Walk the accessible leading-edge tube rows during a planned stop and look for polished or wedge-shaped wear, exposed base metal, and soot-blower lane streaking. Log findings against the tube ID, not a general "bank looks fine" note.
Ultrasonic thickness survey at fixed grid points
Run a UT survey at the same marked grid points every quarter across high-risk rows — inlet bank, soot-blower lanes, and cold-end economizer. Trending the same point over time is what turns a single reading into a wall-loss rate you can act on.
Soot-blower alignment and dosing audit
Verify soot-blower and SRU lance alignment, steam pressure, and cleaning frequency against OEM setpoints. Over-aggressive or misaligned blowing is one of the most common self-inflicted causes of localized tube erosion in cement WHR boilers.
Shutdown-window full bank survey and shield replacement
During the annual kiln stop, run a full-bank UT survey, replace worn erosion shields on leading-edge tubes, and re-weld or sleeve any row approaching minimum retirement thickness before it becomes next year's emergency repair.
CMMS CONFIGURATION
How a CMMS turns thickness readings into a tube life forecast
The plants that get 15-plus years out of a WHR boiler bank are not running a different boiler — they are running the same UT gun against a system that remembers every reading by tube ID and flags the trend automatically. Here is the setup that makes that possible.
Asset hierarchy by bank, row, and tube ID
Model the PH and AQC boiler as parent assets, tube banks as children, and individual tube rows as grandchildren so a thin-wall reading maps to an exact location, not "somewhere in the PH boiler."
Thickness-trend triggered work orders
Bind UT survey results to each tube ID and auto-generate an inspection or repair work order once a row's projected wall loss rate puts it within one shutdown cycle of minimum retirement thickness.
Digitized grid-point checklists
Replace paper UT logs with a digital checklist tied to marked grid points, so every reading lands against the same spot every quarter and nothing gets lost between inspection cycles or technicians.
Shield and spare-tube forecasting
Track erosion shield wear and tube age per row so the CMMS forecasts shield and spare-tube demand well ahead of the annual shutdown window, instead of a scramble once the survey results come in.
Soot-blower and dosing correlation
Log soot-blower frequency, steam pressure, and dew-point margin alongside thickness data so you can see directly whether a cleaning setting is protecting tubes or quietly eroding them.
Audit-ready failure history
Every UT reading, repair, and shield replacement is timestamped and exportable by tube ID, giving reliability and insurance audits a complete wall-loss history in one report instead of a filing cabinet search.
Our AQC boiler cold-end bank was leaking every 14 to 16 months and we kept treating each one as a surprise. Once we started logging quarterly UT readings by tube ID in the CMMS and let it flag rows approaching minimum thickness, we planned the next three repairs around our annual shutdown instead of an emergency stop. We have not had an unplanned WHR trip from tube wall loss since.
FREQUENTLY ASKED
Cement WHR boiler tube erosion and corrosion — straight answers
What causes tube erosion in a cement plant WHR boiler?
Erosion comes mainly from raw meal and clinker dust entrained in kiln exhaust striking leading-edge tubes and soot-blower lanes at high velocity. Wall loss concentrates in a wedge pattern on the gas-facing side and accelerates if dust loading rises or blower aim drifts off target.
How do you prevent acid dew-point corrosion in an AQC boiler?
Keep cold-end gas temperature above the acid dew point during steady-state running and minimize the number of startup and shutdown cycles that pass through it repeatedly. Tracking dew-point margin alongside thickness readings in a CMMS makes the risk visible before pitting starts. Book a demo to see how this is configured.
How often should WHR boiler tubes be thickness-tested?
Run ultrasonic thickness surveys on high-risk rows — inlet bank, soot-blower lanes, and cold-end economizer — quarterly at fixed grid points, with a full-bank survey during the annual shutdown. Consistent grid points are what let you trend a wall-loss rate instead of a single snapshot.
What is under-deposit corrosion and why does it matter in PH boilers?
Sticky dust and ash trap moisture and corrosive salts against the tube surface underneath, hiding active wall loss beneath a layer of scale. A visual walk-down alone will miss it, which is why UT readings need to be taken through cleaned sections, not just on visibly bare metal.
Can a CMMS actually extend WHR boiler tube life?
Yes — by tying every UT reading to a tube ID, trending wall-loss rate over time, and auto-generating repair work orders before a row hits minimum retirement thickness. Plants that do this typically move unplanned tube leaks to planned shutdown repairs and add years to bank life. Start a free trial to configure your own tube asset hierarchy.
Give your WHR boiler tubes the tracking they were designed to need
Set up your PH and AQC boiler asset hierarchy, quarterly UT grid checklists, and shield-spares forecasting in one sitting — then let the trend data flag the next repair before it becomes a leak.
Free 14-day trial · No credit card